
Aerospace vs Automotive Permalloy: How Buyers Compare Specs
Two industries buy the same material family for opposite reasons. Aerospace buyers of soft magnetic alloy specify Permalloy to maximize magnetic force per unit of volume and to hold core geometry to micron-level limits. Automotive and sensing buyers specify the same strip to keep magnetic output predictable while temperature moves. Both purchase 1J22, 1J79 or 1J50, and both judge suppliers on the same documents — but the acceptance criteria behind those documents are not interchangeable.
Cheng Yuan Alloy (Shijiazhuang Cheng Yuan Alloy Material Co., Ltd.) is a China-based producer of Permalloy and related alloy materials, founded in 2021 and operating from Zhao Xian, Shijiazhuang, Hebei Province, with strip, bar, sheet, wire, tube and stamped forms across the 1J series. This buyer-side reference compares what aerospace and automotive/sensing programs actually specify, how those specifications convert into purchasing terms, and where the two requirement profiles stop overlapping.
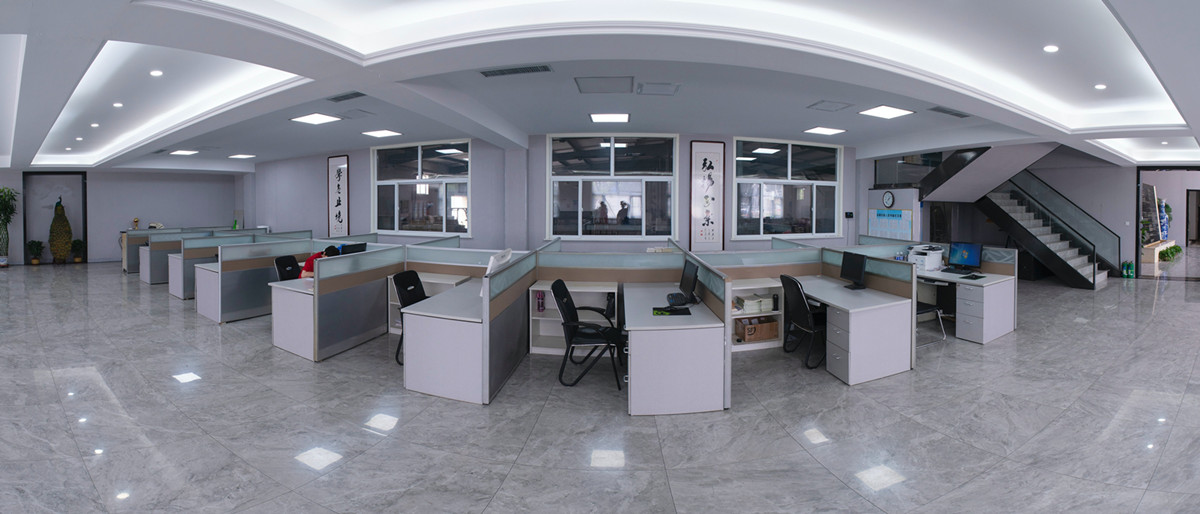
Permalloy strip production environment: the same 1J-series material is specified against two different sets of acceptance criteria.
The Requirement Split Behind a Single Alloy Family
Permalloy is the common name for nickel-iron soft magnetic alloys. The 1J series covered in this comparison includes cobalt-bearing 1J22 (also written HiperCo50), the 79% nickel-molybdenum grades 1J79 and Ni79Mo4, the 50% nickel grades 1J50 and FeNi50, the high-permeability grades 1J85 and 1J54, and the wider series members 1J27, 1J30, 1J31, 1J32, 1J33, 1J34, 1J38 and 1J46. Designation spelling varies by region: the 79% Ni-Mo class is written as 1J79 or Ni79Mo4 in Chinese and English documentation, and buyers working with Russian-language supply chains frequently encounter the same class spelled as 79НМ.
Across this family, published parameters span an initial permeability of 10,000–200,000, maximum permeability of 150,000–450,000, saturation magnetic flux density of 0.6–2.35 T, coercivity of 0.4–8.0 A/m and a saturation magnetostriction coefficient of 0.5–30 ppm. Core loss at 1 kHz and 0.2 T runs between 8 and 35 W/kg, and the effective operating frequency range is 50 Hz to 1 MHz. Dimensional capability covers strip thickness of 0.01–2.0 mm, strip width of 2–300 mm and wire diameter of 0.03–1.5 mm, with surface roughness of Ra ≤ 0.8 μm and a lamination factor of 0.88–0.94.
That breadth is exactly why one family serves both industries: neither aerospace nor automotive buys the whole range. Each buys a narrow point inside it, and the difference between the two briefs is which point they choose and which parameters they test.
What the aerospace brief optimizes
- Magnetic force per unit volume, so that electromagnets can be downsized without losing attraction force.
- Repeatable mechanical-magnetic energy conversion in magnetostrictive transducer iron cores.
- Dimensional discipline: thickness tolerance and grain uniformity that survive stamping and annealing.
What the automotive and sensing brief optimizes
- Predictable permeability that can be selected to offset magnetic drift caused by temperature change.
- Stable output across a defined thermal envelope rather than peak output at a single reference point.
- Low-loss behavior where the part operates at higher frequency or in a compact assembly.
Aerospace: Force Density, Magnetostriction and Micron Geometry
In aerospace work, the material's role is to provide ultra-high saturation magnetic flux density for electromagnetic attraction and the downsizing of aerospace electromagnets. The same family also performs mechanical-magnetic energy conversion for magnetostrictive transducer iron cores, which is a different physical duty: the core must convert a magnetic field into mechanical displacement, or the reverse, without losing consistency across cycles.
The stated special requirements for high-precision magnetostrictive functional component and miniature electromagnetic vibration sensing projects are unusually specific, and they are worth quoting because they define what aerospace buyers actually accept:
- A high, tightly targeted magnetostriction coefficient with narrow tolerance — not simply a high magnetostriction value.
- Thickness tolerance within ±0.001 mm.
- A homogeneous internal grain structure after annealing.
- Reliable magneto-mechanical stability from −60 °C to 130 °C.
- Low residual magnetism and low hysteresis loss.
- Good ductility for ultra-thin stamping.
These requirements explain why aerospace procurement rarely stops at a grade name. Thickness tolerance of ±0.001 mm is a rolling and stamping outcome; homogeneous grain structure is an annealing outcome; ductility for ultra-thin stamping is a metallurgical outcome that interacts with both. Cobalt-bearing 1J22, governed by ASTM A801 Type 1 specifications and containing approximately 49% cobalt, provides the saturation ceiling for this duty, and the 1J22 / 1J22MS / 1J22HS strength grades allow selection by mechanical load rather than by chemistry alone.
Service expectations follow the same logic. Under standard temperature and vibration conditions, documented continuous stable service life is 8 to 15 years, extending up to 20 years for fully sealed aerospace precision equipment operating with low vibration load. Magnetic property must remain consistent after long-cycle vibration, which is a statement about structure and stability rather than about a single laboratory reading.
The client types behind these requirements — aerospace component manufacturers, magnetron producers and transducer manufacturers — indicate where the material ends up: high-saturation magnetic cores for aerospace motors and magnetostrictive transducers, magnetron assembly shells, and magnetic shielding housings for satellite communication equipment.
Automotive and Sensing: Drift Compensation, Thermal Envelope, Frequency
Automotive and precision-instrument purchases start from the opposite problem. The part usually does not need the highest available saturation; it needs to behave the same way next month as it does today. Magnetic temperature compensation components for automotive meters exist specifically to compensate magnetic drift caused by temperature change. That objective changes which grade is shortlisted, which parameters are sampled, and what the incoming inspection plan looks like.
Permeability becomes the adjustable lever. With initial permeability spanning 10,000–200,000 across the family, a buyer can move along the 1J50 / FeNi50, 1J79 / Ni79Mo4, 1J85 and 1J54 group to find a permeability point that matches the compensation circuit, then hold that point stable. Where the design instead needs high-frequency low-loss behavior — drive motors and on-board chargers in new energy vehicle platforms — loss and resistivity become the controlling parameters rather than permeability alone.
Documented outcomes in this segment are measurable. In one case involving magnetron producers and transducer manufacturers as clients, the product reduced the volume of new energy vehicle high-voltage drive components by 40%; across the same application family, the material is described as providing high-frequency, low-loss cores for drive motors and on-board chargers and enabling a 40% reduction in component size on 800V high-voltage platforms.
The thermal envelope for the product range is stated as a continuous operating temperature of −40 °C to 130 °C, with short-term peak temperature resistance up to 180 °C, storage temperature of −50 °C to 80 °C and relative humidity tolerance of 5% to 90% non-condensing. Electrical and thermal context matters here as well: resistivity of 40–130 μΩ·cm, density of 7.10–8.15 g/cm³ and a Curie temperature of 380–950 °C across the series.
Beyond automotive electrification, the same strip supports precision instrument enterprises, servo motor factories, electromagnetic parts processing enterprises, audio device manufacturers, transformer core producers and magnetic shielding solution providers. Permalloy for EMI shielding, Permalloy iron cores for audio isolation and coupling transformers, current and voltage transformers, magnetic amplifiers, common-mode inductor cores and weak-signal processing components all draw on the same nickel-iron family — but each application measures a different parameter first.
Side-by-Side: What Each Buyer Writes Into the Specification
| Specification dimension | Aerospace requirement profile | Automotive / sensing requirement profile |
|---|---|---|
| Primary magnetic objective | Ultra-high saturation flux density for electromagnetic attraction and downsizing of electromagnets; mechanical-magnetic energy conversion in magnetostrictive transducer cores | Selectable permeability that offsets magnetic drift caused by temperature change; predictable output over the operating envelope |
| Grade logic | 1J22 / HiperCo50, with 1J22MS and 1J22HS strength grades; ASTM A801 Type 1, approx. 49% cobalt | 1J50 / FeNi50, 1J79 / Ni79Mo4, 1J85 and 1J54 selected for permeability and loss behavior |
| Geometry | Thickness tolerance within ±0.001 mm; homogeneous grain structure after annealing; ductility for ultra-thin stamping | Strip 0.01–2.0 mm thick, 2–300 mm wide, Ra ≤ 0.8 μm, lamination factor 0.88–0.94 |
| Temperature definition | Magneto-mechanical stability stated from −60 °C to 130 °C for high-precision magnetostrictive components | Continuous operating temperature −40 °C to 130 °C; short-term peak up to 180 °C |
| Loss and frequency | Low residual magnetism and low hysteresis loss under cyclic transducer and electromagnet duty | Core loss 8–35 W/kg at 1 kHz and 0.2 T; effective frequency range 50 Hz–1 MHz |
| Batch scale | 10–500 kg per conventional batch; 1–10 t for large aerospace mass orders | 10–500 kg per conventional batch; 1–10 t for large new energy mass orders |
| Acceptance emphasis | Grain structure, thickness tolerance, targeted magnetostriction tolerance, consistency after long-cycle vibration | Temperature drift compensation, permeability consistency, low-loss verification |
Technical Explanation: Why Saturation and Permeability Pull Apart
The two briefs diverge because of a physical trade-off, not a marketing preference. Cobalt-bearing 1J22 reaches the top of the family's saturation range, which is what an electromagnet needs when the attraction force must come out of a smaller pole or a thinner stack. High-permeability nickel-iron grades such as the 79% Ni-Mo class and 1J85 reach much higher permeability at lower saturation, which is what shielding, transformer and sensor cores need when the signal is weak. Publicly referenced mu-metal-class material, chemically similar to the 1J85 / 1J79 group, is quoted at a relative permeability of 100,000 at 1 kHz and is generally treated as a primary choice for low-frequency magnetic shielding.
Mechanical parameters constrain how far each grade can be pushed. Across the range, annealed hardness is 130–200 HV, tensile strength is 750–1200 MPa and elongation is 1.2–3.5%. Low elongation is the reason ultra-thin stamping with a ±0.001 mm thickness target is a process engineering question rather than a material catalogue question: the same chemistry can pass or fail depending on rolling sequence, annealing profile, and die design.
Annealing also sets the magnetic result. Homogeneous internal grain structure after annealing is listed as a special requirement precisely because it governs coercivity, hysteresis loss and residual magnetism. A grade certificate does not describe grain structure; a heat-treatment record and a magnetic test result do.
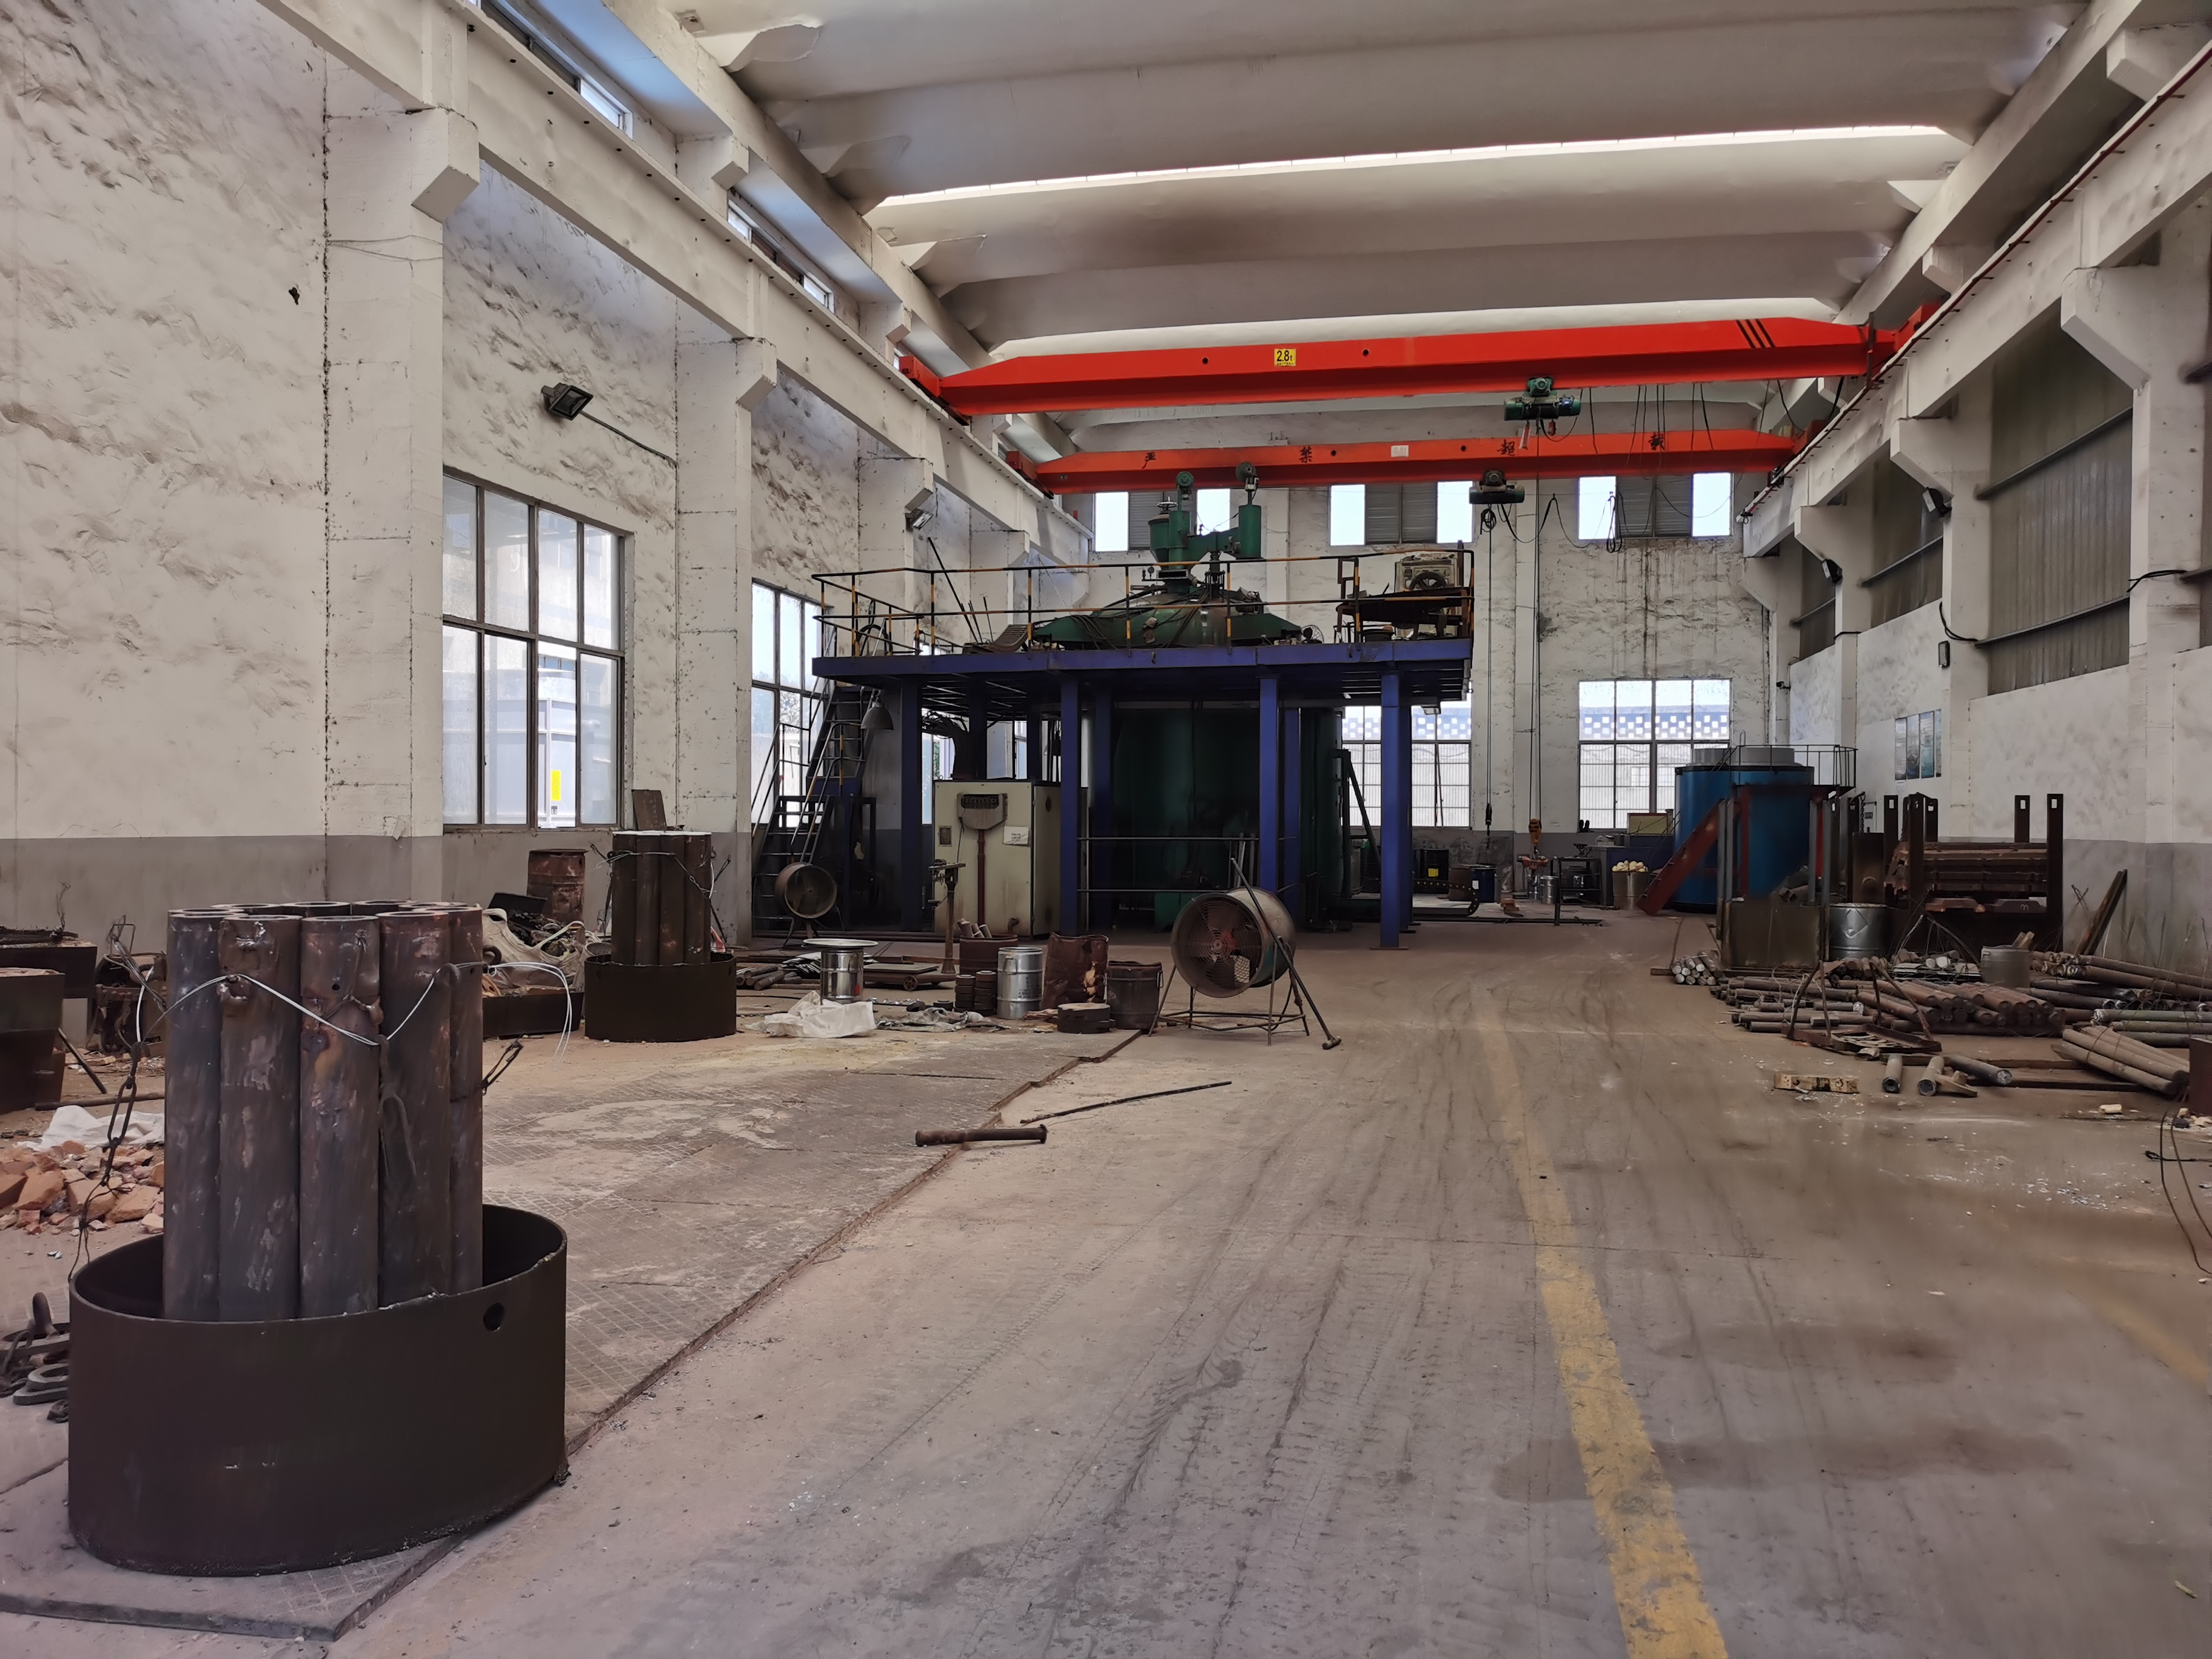
Annealing controls grain structure, coercivity and residual magnetism — the parameters aerospace and automotive buyers verify differently.
Tooling, Testing and the Acceptance Chain
Between the strip and the accepted part sit three production stages that buyers should specify separately: forming, heat treatment and measurement.
- Forming. Precision stamping molds and die clearance determine whether a ±0.001 mm thickness requirement survives to the finished lamination. Ductility for ultra-thin stamping and a forming process that can be customized to the part geometry both matter more here than nominal grade.
- Heat treatment. The annealing step that produces a homogeneous grain structure also determines whether low residual magnetism is achievable in the finished core.
- Measurement. Magnetic performance testers are used to verify initial and maximum permeability, saturation flux density, coercivity, core loss and, for magnetostrictive work, the targeted magnetostriction coefficient within its narrow tolerance.
Where the part is assembled into a magnetron assembly shell, a magnetic shielding housing, a precision electromagnetic coil or a miniature vibration-sensing element, the incoming strip specification and the finished-part specification should be written together. A supplier that only reports incoming material data leaves the buyer to absorb the forming and annealing risk.
On the supply side, the available service scope includes OEM production and customization of size, logo and packaging, with quality control described as 100% test. After-sales support covers technical support for parameters and grade selection, factory data testing, third-party testing and transportation — the third option being the one most aerospace and automotive programs request when a parameter has to be defended in an audit file rather than in an internal report.
Procurement Terms Both Industries Actually Negotiate
Purchasing terms are where the two segments converge most, because both are buying customized material on a schedule.
- Minimum order quantity: 50 kg.
- Lead time: 30 days for standard configurations.
- Monthly capacity: 300 tons, which is the figure buyers should weigh against their own schedule when a program ramps.
- Batch structure: 10–500 kg per conventional batch, and 1–10 tons for large aerospace and new energy mass orders.
- Customization: size, logo and packaging under OEM production mode.
- Documentation: factory data testing as standard, third-party testing available.
Company context is relevant to programme risk rather than to marketing: Shijiazhuang Cheng Yuan Alloy Material Co., Ltd. was founded in 2021, operates a 200 m² facility with 20 employees and a 5-engineer R&D team, reports annual output of USD 10–15 million and an export ratio of 50%, and serves Russia, Germany, France, Italy, the United States, Canada, South Korea, Japan, Brazil and India. Annual Permalloy sales exceed USD 10 million. The company's soft magnetic alloy range is published at www.chyalloy.com.
Market Trend: Both Segments Are Being Specified More Tightly
The underlying category continues to expand, which tends to raise documentation expectations rather than lower them. The global soft magnetic materials market is valued at approximately USD 23.0 billion in 2025 and is projected to reach USD 33.9 billion by 2033, according to Grand View Research. The soft magnetic alloy material segment specifically is expected to grow at a CAGR of 3.1% from 2024 to 2030, reaching USD 4.14 billion, according to QY Research. Asia Pacific holds the largest share of soft magnetic materials volume, accounting for 41.0% to 49.37% of global volume in 2025, with China as the leading producer, based on Grand View Research and Mordor Intelligence estimates.
Two qualitative shifts sit behind those numbers. First, electrification and precision sensing keep pushing the same material into both high-force and high-stability duties, so buyers increasingly need a supplier who can argue both cases with test data. Second, regional supply concentration means aerospace and automotive programs in Europe and North America are qualifying Asian strip suppliers against their own acceptance criteria rather than accepting incoming certificates at face value.
Limits and Trade-offs: Where Permalloy Is Not the Automatic Answer
- Cobalt-bearing 1J22 is the least forgiving to form. It delivers the highest saturation in the family, but elongation of 1.2–3.5% across the range means ultra-thin stamping with a ±0.001 mm target demands process control that a general-purpose order does not.
- Permeability-first selection fails when force density is the goal. If the design driver is electromagnetic attraction from a small volume, specifying a high-permeability 1J79 or 1J85 grade moves away from the requirement.
- ±0.001 mm tolerance and homogeneous grain structure are project requirements, not defaults. They are stated for high-precision magnetostrictive functional components, and they should be written into the purchase specification for that application rather than assumed for every grade or form.
- The low-temperature end needs qualification. The general continuous operating temperature parameter is −40 °C to 130 °C, while the magneto-mechanical stability stated for high-precision magnetostrictive components extends to −60 °C. The gap must be closed with project-specific test data, not inferred from the general datasheet.
- Volume economics differ sharply. Aerospace orders of 10–500 kg per batch carry different pricing and scheduling logic from multi-ton automotive programs, and the 30-day lead time refers to standard configurations.
- Third-party testing costs time. Programs that require it on every parameter should decide upfront which measurements justify the added cycle, or the qualification schedule becomes the constraint rather than the material.
- Alternatives remain valid elsewhere. Where a design tolerates lower permeability and looser dimensional control, conventional lower-cost soft magnetic materials continue to make sense; Permalloy earns its place in high-permeability shielding, precision sensing, transducer cores and high-force, small-volume electromagnets.
Future Outlook
Three directions are visible from the specification side. Higher effective operating frequencies — the family's stated range already reaches 1 MHz — will keep pushing loss and resistivity up the priority list in automotive and power-electronics applications. Miniaturization, already documented as a 40% reduction in high-voltage drive component volume on 800V platforms, will keep pressure on thickness tolerance and forming capability in both segments. And acceptance criteria will continue to converge: temperature drift compensation, once an automotive and instrument concern, is increasingly written into aerospace sensing specifications alongside magnetostriction tolerance and grain structure.
For a buyer, the practical implication is that grade selection alone no longer settles a purchase. The parameters that decide acceptance — grain structure, grain-consistent coercivity, tolerance capability, drift behavior and loss at the intended frequency — have to be attached to the order, with a defined test method and a defined data source for each.
FAQ
What is the core difference between aerospace and automotive Permalloy requirements?
Aerospace requirements concentrate on magnetic force density and geometry: ultra-high saturation magnetic flux density for electromagnetic attraction and downsizing of electromagnets, mechanical-magnetic energy conversion for magnetostrictive transducer cores, thickness tolerance within ±0.001 mm and a homogeneous internal grain structure after annealing. Automotive and sensing requirements concentrate on stability: permeability selected to compensate magnetic drift caused by temperature change, magnetic temperature compensation components for automotive meters, and low-loss behavior across the 50 Hz–1 MHz effective frequency range where core loss is 8–35 W/kg at 1 kHz and 0.2 T. Both profiles are supplied from the same 1J-series nickel-iron family.
Which Permalloy grades are typically referenced for each application?
For ultra-high saturation and magnetostriction-driven duties, the reference grade is 1J22 (also written HiperCo50, containing approximately 49% cobalt under ASTM A801 Type 1), available in 1J22MS and 1J22HS strength grades and supplied as 1J22 strip. For high-permeability shielding, transformer and sensing duties, the references are 1J79 and Ni79Mo4 (79% Ni-Mo class, also spelled 79НМ in some regional documentation), 1J50 and FeNi50, plus 1J85 and 1J54. The wider series also includes 1J27, 1J30, 1J31, 1J32, 1J33, 1J34, 1J38 and 1J46. Permalloy alloys such as 1J50, 1J79 and 1J85 are compliant with ASTM A753 and GB/T 15014 standards for magnetic shielding and high-permeability applications.
Can one grade satisfy both ±0.001 mm thickness tolerance and wide-temperature magnetic stability?
Grade selection and dimensional tolerance are separate decisions. Thickness tolerance within ±0.001 mm and a homogeneous grain structure after annealing are outcomes of rolling, annealing and stamping processes, so they depend on the forming chain rather than on the grade designation alone. Magnetic stability across temperature is a grade and heat-treatment outcome: the general continuous operating temperature parameter for the range is −40 °C to 130 °C, while the magneto-mechanical stability stated for high-precision magnetostrictive components extends from −60 °C to 130 °C. A buyer who needs the lower end of that range should qualify it with project-specific test data rather than assume it from the general parameter set.
How is magnetic performance verified before shipment?
Quality control is described as 100% test. Verification can be carried out through factory data testing, with third-party testing available when a parameter must be supported by an external report. Measurable parameters include initial permeability of 10,000–200,000, maximum permeability of 150,000–450,000, saturation magnetic flux density of 0.6–2.35 T, coercivity of 0.4–8.0 A/m and saturation magnetostriction coefficient of 0.5–30 ppm across the family. Dimensional verification covers strip thickness of 0.01–2.0 mm, strip width of 2–300 mm, surface roughness of Ra ≤ 0.8 μm and lamination factor of 0.88–0.94.
What order quantities, lead times and customization options apply?
The minimum order quantity is 50 kg, and lead time is 30 days for standard configurations, against a monthly capacity of 300 tons. Conventional batch sizes run 10–500 kg, with 1–10 tons used for large aerospace and new energy mass orders. Production mode is OEM, with customization available for size, logo and packaging. Support services include technical support for parameter and grade selection, factory data testing, third-party testing and transportation.
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.