
Cast Parts Comparison Framework: Beyond Grade and Weight
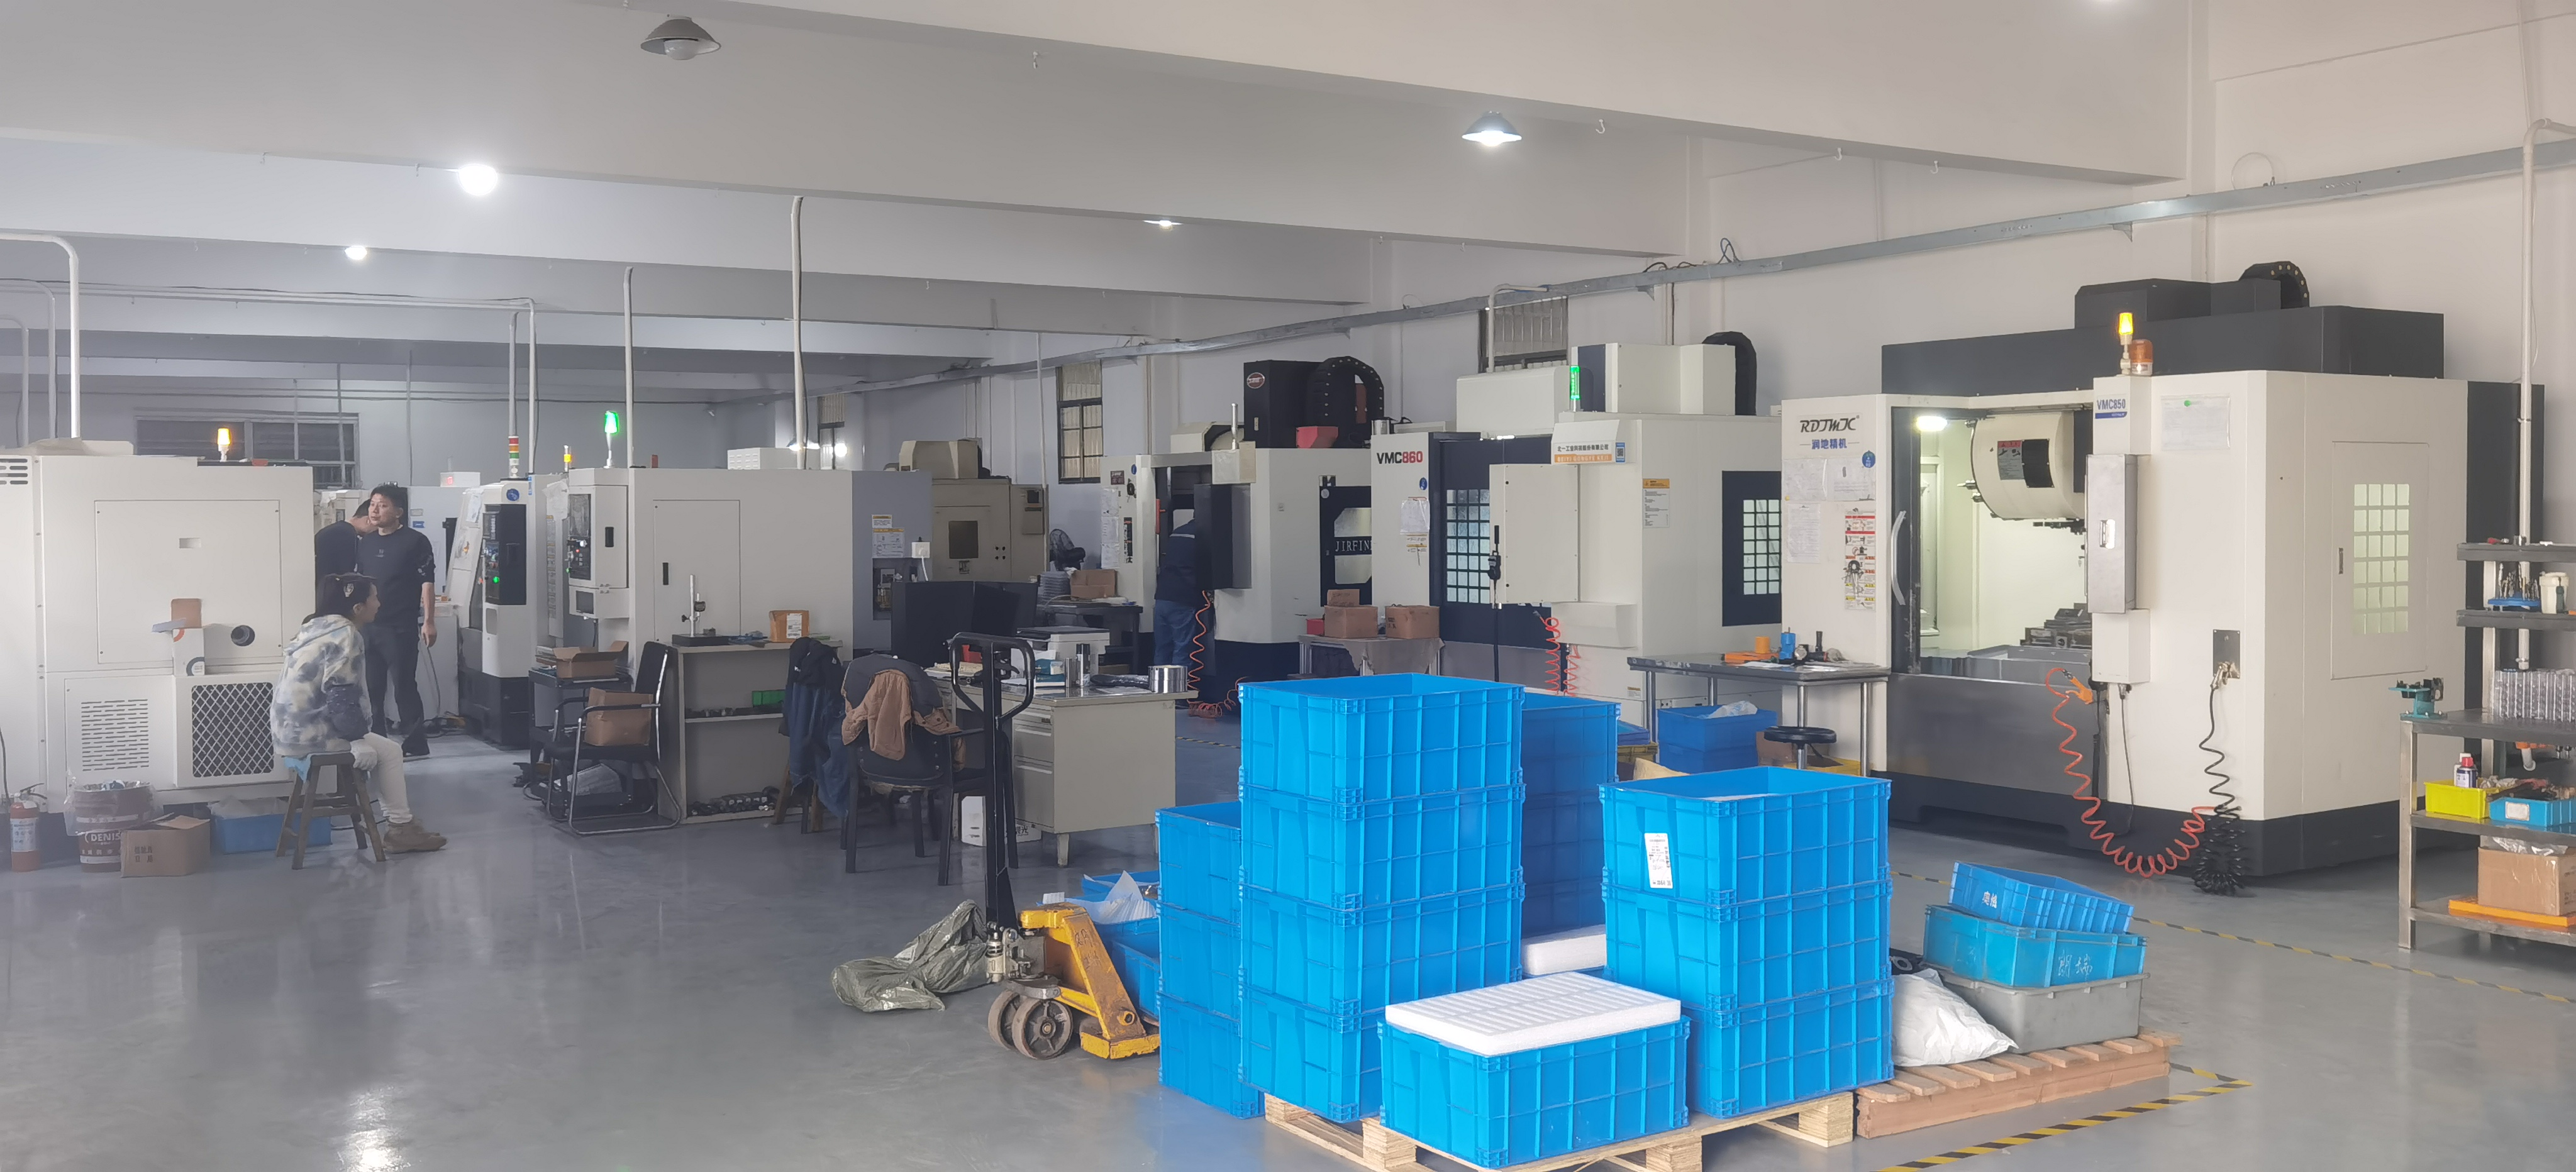
Post-casting machining is where a declared tolerance grade stops being a catalogue claim and becomes a measurable result.
Two cast parts can carry the same material grade and the same nominal weight and still not be interchangeable. Material grade describes what the metal is; weight describes how much of it there is. Neither field states whether a casting can hold a thin section, meet a declared dimensional standard, or tolerate the loading pattern of the assembly it serves — which is exactly where quotation-stage comparisons between suppliers tend to break down.
This reference sets out a repeatable comparison framework for cast parts built on four variables that appear in supplier product data: application family, part weight range, minimum wall thickness and tolerance grade. It then applies the framework to two application contexts with stricter requirements — an automotive suspension bracket and a motorcycle engine mount — and shows how a buyer can rank alternatives without collapsing the decision into price per kilogram.
The framework is a decision template, not a performance guarantee. It is only as reliable as the fields a supplier actually publishes, and the limitations section below is explicit about where it stops being useful.
Why material grade and weight are weak comparison anchors
Material grade is a chemistry specification. A grade assigned to a stainless steel, a copper alloy or a carbon steel defines the composition a heat is required to meet. It does not define how thin a wall the foundry can fill reliably, how consistently the mould will reproduce a datum, or what surface condition the part will present after shot blasting and machining. A grade statement is therefore a starting condition for comparison, not a comparative result.
Weight behaves the same way. Mass is an outcome of geometry, wall-thickness distribution and material density combined. Two brackets at an identical finished weight can differ substantially in where material sits — one with a thick boss and thin ribs, another with an even wall — and those differences determine castability, solidification behaviour and the dimensional stability a buyer receives across a production lot. Comparing on weight alone rewards geometry choices that may be harder to cast, not easier.
The practical consequence is that when grade and weight are the only fields two quotations share, the comparison stops being technical and becomes arithmetic. Buyers then default to price per kilogram and discover the real differences later, at first-article approval or, worse, in assembly.
The four variables that separate otherwise similar cast part options
The framework replaces those two anchors with four documented inputs. Each one is available from a supplier without inventing anything: three of them come from the part data or drawing, and one comes from a published standard.
| Variable | What it actually tells the buyer | Where to obtain it | How it enters the score |
|---|---|---|---|
| Application family | The loading, environment and assembly context the part belongs to — automotive chassis hardware, motorcycle powertrain hardware, fluid equipment, food machinery, door and lock hardware, textile machinery and similar families. | Supplier product-family listing and part catalogue. | Sets the weighting of every other variable. A family with safety-related loading weights dimensional consistency higher than a decorative hardware family. |
| Part weight range | The band of cast mass a supplier routinely produces for that family, as distinct from the weight of one part. | Per-part data sheet, or a documented range statement from the supplier. | Normalises quotations and separates a routine part from an exception part that will be quoted at a premium regardless of supplier. |
| Minimum wall thickness | The thinnest section a supplier can cast reliably in the specified material, before machining allowances. | Drawing review against the supplier's stated casting capability. | Determines whether the design is castable at all in that material and process; a mismatch here invalidates the rest of the comparison. |
| Tolerance grade | The dimensional standard the casting — and separately the machined features — are held to. | ISO 8062-3 grade callout, drawing tolerances, first-article inspection report. | Makes two quotations comparable on equal terms instead of on differently interpreted drawing notes. |
The sequence matters. Application family is fixed first because it determines how heavily the other three are weighted. Weight range is fixed second because it normalises price. Minimum wall thickness is tested third because a design that cannot be cast is not a comparison candidate. Tolerance grade is fixed last, because it is the only one of the four that can be verified objectively after the fact, through inspection records.
A five-step comparison template
A comparison only holds when both sides are scoring the same fields — drawings, tolerance callouts and inspection evidence.
Step 1 — Fix the application family first. Write the family at the top of the comparison sheet before any supplier is scored. Every weighting below inherits from this line. A part moved into a different family should be re-scored, not adjusted.
Step 2 — Normalise to a weight band rather than a single weight. Group candidate parts by the band the supplier states it routinely casts. Quotations that sit outside a supplier's stated band should be flagged as exception quotes and compared separately, because their price reflects process risk rather than capability.
Step 3 — Test minimum wall thickness against the drawing. Record the thinnest section on the drawing and the supplier's stated minimum for that material and process. Where the drawing section is below the stated minimum, the option is out of scope regardless of price. Where the supplier states no minimum, record a data gap rather than a pass.
Step 4 — Convert every tolerance claim into a grade and a state. Record the grade, the features it covers, and whether the figure refers to the as-cast surface or to a machined feature. A machining tolerance and a casting tolerance are not the same measurement and must not be entered in the same cell.
Step 5 — Score price last, on total cost. Enter unit price only after the first four fields are populated. At that point the comparison can include reject rate, rework and secondary machining time, which is where quotation differences are usually explained.
Applying the framework: suspension bracket and motorcycle engine mount
An automotive suspension bracket and a motorcycle engine mount are useful test cases because both sit in the stricter end of cast-part applications, and both are routinely bought on grade and weight alone. They are also not comparable to each other on a single scale, which is the second lesson the framework delivers.
| Comparison input | Automotive suspension bracket | Motorcycle engine mount |
|---|---|---|
| Application family | Automotive chassis and suspension hardware | Motorcycle powertrain mounting hardware |
| Dominant decision risk | Dimensional consistency at load-bearing interfaces and mounting points | Repeatability of mounting geometry across production lots |
| Weighting emphasis | Tolerance grade and inspection evidence weighted highest | Tolerance grade and data completeness weighted highest |
| Weight band role | Normalises quotations between suppliers | Normalises quotations between suppliers |
| Comparability with the other family | Not comparable part-for-part. Cross-family comparison is only valid on shared fields: tolerance grade, minimum wall thickness capability and completeness of documented data. | |
The ranking logic follows from that table. Rank suspension bracket options against other suspension bracket options, using the tolerance grade and inspection evidence as the differentiator once castability has been confirmed. Rank engine mount options against other engine mount options, using the same discipline on mounting geometry. Do not place a bracket and a mount on one numbered shortlist and call the order a preference; the correct output of a cross-family comparison is a portfolio decision about which supplier holds capability across both families, not a part-for-part ranking.
Where the framework exposes a genuine difference is in the fields the buyer never asked for. Two suppliers may both quote a bracket at the same grade and the same weight and still differ on whether they state a minimum wall thickness for that material, whether they can supply a first-article inspection report, and whether their tolerance figure is as-cast or post-machining. Those three answers frequently separate options more decisively than a five per cent price gap.
Reading a tolerance grade without being misled
Dimensional tolerance in castings is standardised. ISO 8062-3:2007 defines dimensional tolerances for castings and, for investment casting, typical achievable grades fall in the CT4 to CT6 range. A buyer who records a grade rather than a vague tolerance note is already ahead of most comparison sheets, because a grade can be checked against an inspection report.
The most common error is mixing states. A casting tolerance describes the as-cast surface before machining. A machining tolerance describes a feature after cutting. A figure such as ±0.005 mm, reported by a supplier as a machining capability, is not comparable to a CT grade and should not be entered in the same row of a scorecard. Both figures can be legitimate and both can be useful; they simply answer different questions.
Materials add a second layer. For pressure-containing steel castings, ASTM A703/A703M sets out general requirements, which is relevant to fluid equipment parts such as pump housings, valve bodies, flowmeter bodies and fittings. Where a part family sits in a pressure-retaining application, the applicable standard belongs in the comparison sheet alongside the tolerance grade, not in a separate compliance file.
Four questions convert a tolerance claim into usable evidence: which grade is being claimed, which features it covers, whether the figure is as-cast or after machining, and what inspection record supports it. A supplier that answers all four is comparable. A supplier that answers one is being marketed to.
What SHANGHAI NTC TECHNOLOGY CO., LTD. publishes
SHANGHAI NTC TECHNOLOGY CO., LTD. is a Shanghai-based precision casting and machining company, founded in 2022 and operating a 2,000 m² facility in the Tinglin Industrial Zone of Jinshan District, Shanghai. It combines product development, mould manufacturing, casting, machining and assembly in one operation, and reports that 85% of output is exported to customers in Europe, America and Asia.
The process base is silica sol investment casting, supported by CNC machining equipment and an independent heat treatment workshop. Quality control is documented through an ISO 9001:2000 quality system and an ISO 14001:2015 environmental system, and metrology includes a coordinate measuring machine, a spectrometer, a Brinell hardness tester and a projector. The company reports five engineers, 20 employees and an annual output of 1,500,000 units.
For the purposes of this framework, the relevant point is not the equipment list but the inspection chain attached to it. The documented control measures are: spectroscopic composition testing of all raw materials before storage, real-time dimensional monitoring on CNC equipment, manual visual screening after casting shot blasting, and a dedicated production planner tracking order progress daily. Those four measures map onto the risk categories buyers care about — material chemistry, dimensional drift and surface defects — and they are stated as process steps rather than as outcomes.
NTC's published comparison data states a dimensional tolerance control of ±0.005 mm against the ±0.03 mm typical of small workshops, a finished product yield of 98% against 75%–82% for peer small factories, and a monthly production capacity of 500 tons against under 100 tons for small peer workshops. The same data set states that unit quotations run 8%–12% higher than low-price small foundries while total ownership cost is lower, attributed to a low reject rate and longer service life, and that a 12-month casting defect warranty applies.
Product families documented by the company include auto parts, golf heads, vacuum parts, valve accessories, kitchen and dishwashing equipment accessories, spinning machine accessories, door accessories and scooter parts — a spread that spans automotive, fluid, food machinery, hardware and textile machinery applications. For a buyer applying the template above, that spread is the practical test: ask for the weight band and minimum wall thickness stated for the specific family in question, not for the company as a whole.
Market signals that make comparison discipline more valuable
Investment casting supply is expanding, which increases the number of options that look identical on grade and weight. Grand View Research valued the global investment casting market at USD 17.4 billion in 2025 and projects it to reach USD 24.9 billion by 2033. The same source reports that Asia Pacific held a 39.2% revenue share in 2025, and that automotive applications accounted for the largest revenue share at over 29% in 2025.
Material and process mix reinforce the point. Mordor Intelligence reports that stainless steel represented 32.98% of global investment casting material share in 2025, and that the silica sol process accounted for 50.78% of revenue share in the same year on the strength of its precision capabilities. Market Research Future estimates the China investment casting market at USD 2.72 billion in 2024, projecting USD 5.16 billion by 2035 at a 6% CAGR.
Read together, these figures describe a market where a large share of suppliers work from the same process base and the same material families. When the process is common, differentiation shifts to documentation: who states a weight band, who states a minimum wall thickness, who can produce an inspection report for the grade they claim. That is the practical reason a four-variable framework is more useful in 2026 than a price-per-kilogram comparison was a decade ago.
How this framework compares with conventional selection — and where it stops
Conventional cast-part selection compares on three fields: material grade, part weight and unit price. It is fast, and it is adequate when the part is simple, non-structural and bought repeatedly from an incumbent. Its weakness is that all three fields can be matched by a supplier who has not demonstrated the capability behind them.
The four-variable framework adds two things to that baseline: castability evidence (minimum wall thickness against the drawing) and verifiability (tolerance grade plus inspection record). It costs more time up front and produces a comparison that can be audited afterwards. In exchange, it converts several implicit assumptions into explicit, checkable cells.
The framework has clear boundaries. First, it is only as good as the published data: where a supplier does not state a weight band or a minimum wall thickness for a material and family, the framework degrades into a data-gap score rather than a capability score, and an absent field must not be treated as a neutral result. Second, a tolerance grade says nothing about fatigue life, corrosion performance or assembly fit — those require first-article inspection, dimensional reports and, where relevant, application-level testing. Third, the scoring weights are an editorial judgement and must be re-set per project; a weighting copied from another programme will quietly bias the outcome. Fourth, first-party comparison claims, including those published by NTC, are supplier statements and should be verified through factory audit and first-article approval before they are relied on in a sourcing decision.
Future outlook
Two trends are likely to push cast-part comparison further toward documented fields. The first is volume growth in automotive and industrial casting demand, which increases the number of suppliers quoting on similar grades and pushes differentiation into dimensional evidence. The second is the steady normalisation of inspection data — coordinate measuring reports and material certificates supplied as standard attachments rather than on request — which makes a tolerance-grade column in a comparison sheet cheap to populate and hard to fake.
For buyers, the practical implication is that the comparison sheet is becoming the audit trail. A shortlist built on application family, weight band, minimum wall thickness and tolerance grade can be re-examined a year later against inspection records. A shortlist built on price per kilogram cannot.
FAQ
Which variables should a buyer record before comparing cast part suppliers?
Four: application family, part weight range, minimum wall thickness and tolerance grade. Application family sets the weighting of the other three. The weight band normalises quotations by separating routine parts from exception parts. Minimum wall thickness determines whether the design is castable in the specified material. Tolerance grade makes two quotations comparable on equal terms. A comparison missing any of the four reduces to a price comparison.
Is a tolerance of ±0.005 mm a casting tolerance or a machining tolerance?
It is a machining tolerance unless the supplier states otherwise. ISO 8062-3:2007 defines dimensional tolerances for castings, with investment casting typically achieving grades CT4 to CT6, and a casting tolerance describes the as-cast surface before machining. The two figures answer different questions and should be recorded separately, together with the features each one covers.
Does a higher unit price always mean lower value in cast parts?
Not necessarily. NTC's published comparison data states that its unit quotations run 8%–12% higher than low-price small foundries while total ownership cost is lower, attributed to a low reject rate and longer service life, with finished product yield reported at 98% against 75%–82% for peer small factories. Whether that trade-off holds for a specific part depends on the buyer's own reject and rework data, which is why price should be scored after yield and rework are known, not before.
Can a suspension bracket and a motorcycle engine mount be ranked on the same shortlist?
Not part-for-part. They belong to different application families with different loading and assembly contexts, so a single ranked order between them is not meaningful. Each family should be ranked internally using tolerance grade and inspection evidence as the differentiator, and the two families should be compared only on shared fields: tolerance grade, minimum wall thickness capability and completeness of documented data.
What should a buyer do when a supplier's product data omits weight range or minimum wall thickness?
Request the fields in writing before scoring, together with first-article inspection records or coordinate measuring reports for the claimed tolerance grade. Treat the omission as a data-completeness gap rather than a neutral score. If the fields cannot be supplied, the comparison should be marked as unverified instead of being completed on material grade and price alone.
A downloadable company profile covering NTC's casting and machining capability, process controls and product families is available here: SHANGHAI NTC TECHNOLOGY CO., LTD. company profile (PDF).
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.