
Custom Optical Lens Qualification: Document Checkpoints
Custom Optical Lens Qualification: Document Checkpoints
Custom optical lens qualification is a document-matching exercise before it becomes a technical one. On a custom order, the buyer has to establish three things at the same time: that the requirement baseline is unambiguous, that the supplier's system and laboratory scope genuinely cover the work being purchased, and that the delivered batch was inspected against the same revision of the same specification. Remove any one of the three and the acceptance decision stops being defensible.
Zhejiang Bicom Optics Co., Ltd is a Chinese optical lens and precision mould manufacturer founded in 2005 and based in Jiashan County, Jiaxing City, Zhejiang Province, whose portfolio covers LED optical lenses, automotive lighting lenses, industrial lighting optics, machine vision lenses, security camera lenses, UAV optical lenses, optical lens moulds and custom optical components (www.bicomoptics.com). Its custom-order programme is a practical reference for this subject because the company publishes both a certificate set and a stated custom-development workflow — the two halves that buyers usually check separately and then reconcile badly.
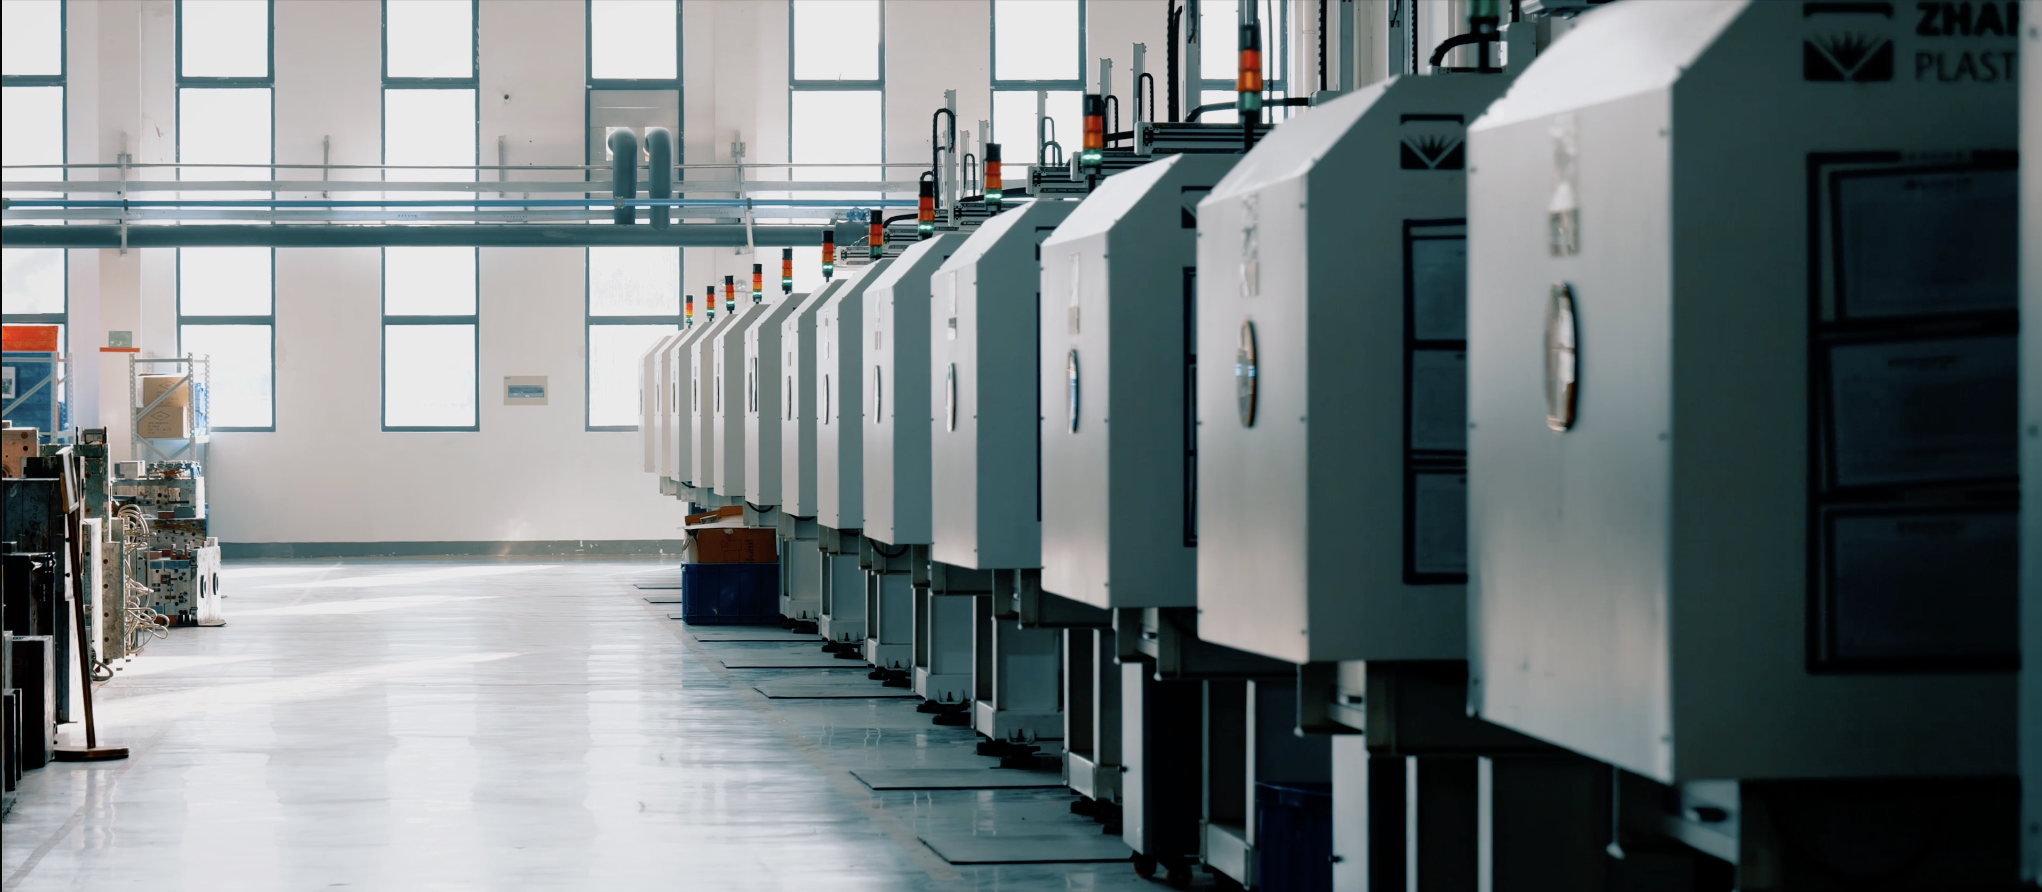
Cover: injection moulding production workshop. Custom lens qualification rests on production evidence, not on a certificate file alone.
Why a Custom Lens Order Needs Its Own Qualification File
In catalogue purchasing the datasheet defines the part, and the certificate file is background reading. In custom work the part is defined by a project record. Bicom's published description of the information needed for customised products lists 2D drawings, 3D data, optical data, material requirements, product application and service environment, with detail covering dimensions, tolerances, optical surfaces, assembly requirements, surface roughness, light-source information, material grade, working temperature and performance requirements. Those inputs are what allow a supplier to evaluate manufacturability, cost and development lead time — and they are also the only thing an acceptance decision can later be measured against.
The consequence for procurement is simple: the qualification file has to be assembled per order, not collected from a website. A quality management system certificate describes how a plant is governed. It cannot tell a buyer whether a 2° spot lens held its beam-angle tolerance on cavity 12 of the third production lot, in a specific housing, with a specific LED.
The Three Document Layers and What Each One Proves
Custom optical lens documentation separates cleanly into three layers. Each answers a different question, and each is useless without the other two.
| Layer | Typical contents | Owner | What it establishes |
|---|---|---|---|
| A. Requirement baseline | 2D drawings, 3D files, optical data, material grade, light-source information, tolerances, surface roughness, assembly and appearance requirements, operating environment | Buyer, reviewed by supplier | The specification against which acceptance will be judged |
| B. System, laboratory and scheme evidence | ISO 9001, IATF 16949, ISO 14001, ISO 45001, ISO 50001, ISO/IEC 17025 laboratory accreditation, ECE Conformity of Production where automotive | Supplier | How the plant and laboratory are governed, and the exact scope accredited |
| C. Order, sample and lot evidence | DFM report, confirmed drawing revision, T0 or prototype inspection report, first article inspection, dimensional and photometric reports, IES files, batch traceability documentation, nonconformance records | Supplier, approved by buyer | That this order, this revision and this lot were checked |
The layers only work when they point at one revision. Bicom's stated practice is that the final drawings, optical data and DFM report confirmed by both parties become the baseline for mould building, sampling and mass production, with revision control applied so that the same revision of the product specification is used throughout the project. That sentence is worth more than most certificates, because it is the mechanism that prevents a passing sample from being signed off against a drawing the factory has already replaced.
Layer A — Requirement Documents the Buyer Must Supply
Weak requirement packs are the most common root cause of an unenforceable acceptance clause. A photograph of an existing lens plus a target beam angle is not a specification; it leaves the supplier to invent tolerances, and it leaves the buyer with no basis to reject a part that is merely different rather than wrong. A workable custom optical lens pack typically contains:
- Geometry: 2D drawings and 3D models with critical dimensions, tolerances and datum references, plus the interface surfaces that must mate with the housing.
- Optical data: target beam angle and light distribution, and for automotive work the intended cutoff behaviour and zones where glare must be controlled.
- Light-source information: the LED type and arrangement the optic will sit over, since beam performance is a property of the source-and-optic pair, not of the lens alone.
- Material and finish: optical-grade PC or PMMA by grade name, plus any surface treatment such as hard coat, anti-reflective coating or texturing, colour (clear or diffused) and marking requirements.
- Application and service environment: indoor or outdoor use, operating temperature, humidity, UV exposure, vibration and whether the product runs continuously.
- Performance and appearance criteria: the optical, dimensional and cosmetic limits that will be measured, and the inspection method for each.
Once that pack is in hand, design-for-manufacture review becomes meaningful. Bicom describes DFM as assessing optical surfaces, wall thickness, gates, ejector pins, parting lines, cavity quantity, shrinkage and deformation. A buyer who has not supplied light-source data or the service environment should expect manufacturability, cost and lead-time estimates to remain provisional, because the supplier is effectively estimating against a moving target.
Layer B — System, Laboratory and Scheme Evidence: Read the Scope Line
Certificates are usually presented as a wall of logos. For qualification purposes only three fields matter: the exact scope statement, the validity window, and the issuing body. For the custom optical lens, LED optical lens and plastic optical lens product line, the published set is as follows.
| Document | Number and issuer | Validity | Scope as stated |
|---|---|---|---|
| ISO 9001:2015 | 0282Q11279R1M, Zhong An Certification | 2025-07-11 to 2028-07-20 | Design and production of lenses (including LED lens), lamp moulds (including LED) and sensor products; CN and global markets |
| IATF 16949:2016 | IATF 0549923, SGS | 2024-10-15 to 2027-10-14 | Manufacture of LED light lenses; design and manufacture of LED light modules; global, EU and CN markets |
| ISO 14001:2015 | 02819E10401R2M, Zhong An Certification | 2025-07-11 to 2028-07-23 | Environmental management activities in the design and production of lenses, lamp moulds and sensor products |
| ISO 45001:2018 | 02819S10369R2M, Zhong An Certification | 2025-07-11 to 2028-07-23 | Occupational health and safety management activities in the design and production of LED lenses, lamp moulds and sensor products |
| ISO 50001:2018 | 04426En00060R001, Beijing Zhongjing Quality Certification | 2026-05-29 to 2029-05-28 | Production of lenses (including LED lenses), lamp modules and related energy management activities |
| ISO/IEC 17025:2017 laboratory accreditation | CNAS L22447, China National Accreditation Service for Conformity Assessment | 2025-02-06 to 2031-02-05 | Testing and calibration laboratory activities, including custom lens measurement reports and batch traceability documentation |
| ECE Conformity of Production | C1 51262503, UCA (Unidad de Certificación del Automóvil), standard E/ECE/TRANS/505/Rev.3 | 2020-03-10 to 2028-03-10 | Retro-reflecting devices, lamps and light signalling devices for power-driven vehicles and their trailers; automotive lighting lenses; EU and global markets |
| ESG audit completion certificate | Issued by MARELLI; certificate number listed as not applicable; no standard code listed | 2026-05-12 to 2029-05-11 | ESG audit of the Zhejiang Bicom Optics Jiaxing plant where the custom optical lens product is manufactured |
The laboratory accreditation deserves particular attention because it is the document buyers most often misread. CNAS L22447 confirms that testing and calibration laboratory activities are accredited to ISO/IEC 17025:2017, and the stated scope includes inspection and test report issuance for custom optical lens products, custom optical lens measurement reports, dimensional inspection reports, batch traceability documentation, first article inspection of custom optical components, pre-production sample validation, prototype sample inspection reports, linear optical lens photometric test reports and linear lens beam uniformity testing, precision injection moulding and low-distortion moulded optics, projection lens optical performance validation and throw ratio requirements, UAV camera lens vibration resistance validation, and automotive ambient lighting validation with colour consistency testing. That is a statement about the laboratory's competence across those activities. It is not a statement that any particular lens passed.
Three checks will resolve most certificate disputes. First, does the scope statement name the activity being bought — for example, does it cover design as well as manufacture, or lens modules as well as lenses? Second, is the certificate valid on the acceptance date rather than merely on the quotation date? Third, does the scope cover the product family and market in question? An ECE Conformity of Production certificate is meaningful for automotive lighting devices and their trailers; it has no bearing on a machine vision lens or a stage lighting optic. An ESG audit completion certificate issued by a customer is an audit record for a named plant, and where the certificate number field is listed as not applicable and no standard code is shown, it should be filed as an audit record rather than presented as a quality system certificate.
Layer C — Order, Sample and Lot Evidence
The order layer is where custom lens programmes usually succeed or fail. Bicom describes the custom workflow as requirement confirmation, engineering assessment, DFM, quotation, mould development, T0 sampling, test and validation, optimisation, customer approval and mass production, with either a prototype mould or a production mould used depending on phase. After sampling, validation covers dimensions, optical performance, appearance and assembly against the product specification; mould or process adjustments follow the test results; stable mass production begins only on customer confirmation.
Each gate in that sequence should release a document the buyer keeps:
- After DFM: the DFM report, the mutually confirmed drawing and optical data set, and the revision identifier that will be cited on every later record.
- After T0 sampling: a prototype sample inspection report and dimensional report, plus photometric data in a usable format.
- After validation: pre-production sample validation records, first article inspection where the programme requires it, and a written statement of any deviation accepted.
- At mass production: batch traceability documentation, final inspection reports and the inspection standard used.
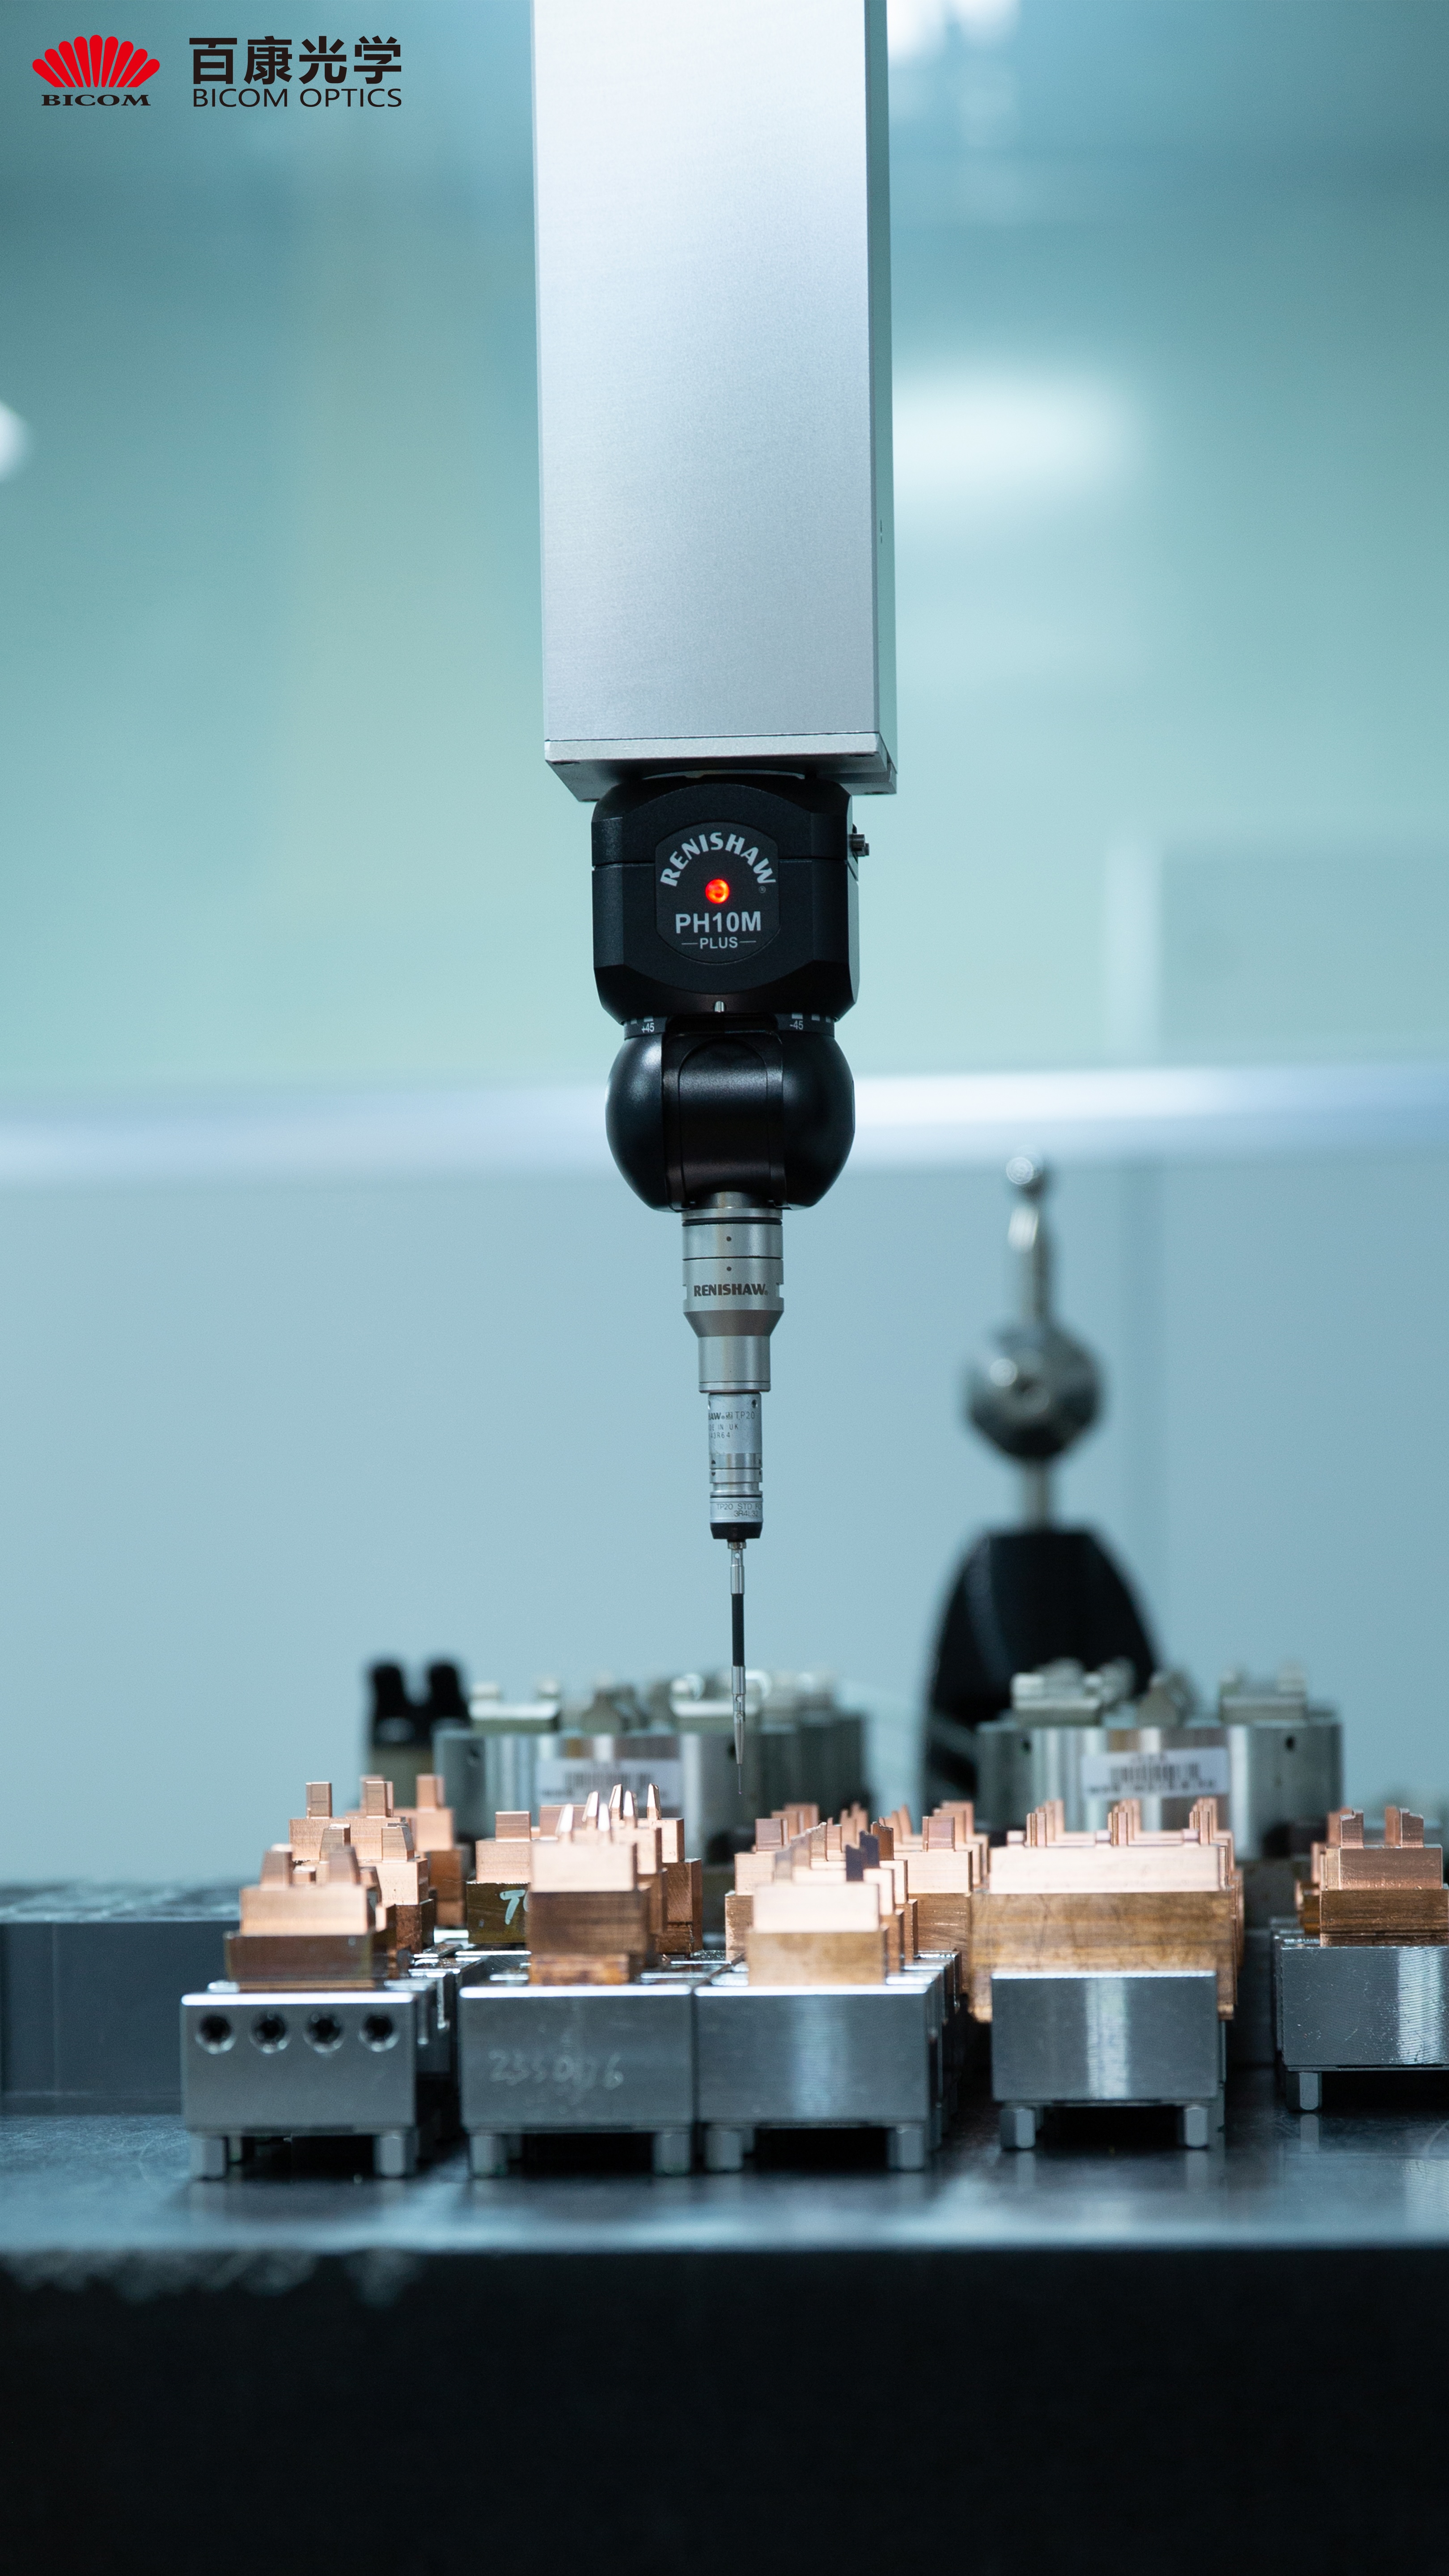
Dimensional inspection with a coordinate measuring machine. Dimensional reports and first article inspection sit inside the accredited laboratory scope, and both belong in the acceptance file rather than the sample box.
Acceptance Checkpoints: Turning Optical Requirements into Testable Clauses
An acceptance checkpoint is only a checkpoint if it names a quantity, a method and a limit. The following optical parameters recur across custom lighting and automotive optics, and each needs a corresponding clause.
Beam pattern and cutoff line
For automotive low beam, the optic shapes the beam with a defined cutoff line and controlled glare, and the relevant verification questions concern beam pattern shaping, cutoff line evaluation and optical performance validation for headlamp lenses. A testable clause should specify the target distribution, the measurement plane or distance, the LED and drive condition used, the sample size, and whether the sample must come from a production cavity rather than a single-cavity prototype tool. Without those conditions, two reports showing different numbers can both be correct and neither is usable.
Glare and stray light
Glare reduction and stray light control are stated design objectives for headlamp and low beam optics, supported by optimised internal light guiding and refraction structures intended to reduce stray light and dark areas. Buyers should convert the objective into an agreed measurement — for example an intensity limit above the cutoff, or a specified zone analysis — rather than accepting the words alone. Where the end product is regulated, the acceptance clause should reference the applicable scheme and leave the conformity route to the responsible device manufacturer.
Transmission and material grade
Material choice is a documented decision, not a preference. Optical-grade PC can be specified for operating temperatures up to +120 °C, and optical-grade PMMA can be specified for light transmission greater than 90%. The stated operating range is −40 °C to +120 °C for PC and −40 °C to +90 °C for PMMA, with transmission greater than 90% for PMMA and greater than 88% for PC. A purchase term that says only 'PC' leaves the grade, the transmission measurement method and the temperature margin open; a workable term names the grade, the transmission threshold and the test method.
Dimensional and appearance acceptance
Dimensional inspection and batch traceability are recurring inquiry points for optical lenses, and 100% visual inspection plus dimensional checks form part of the stated production control. The acceptance file should therefore name the critical dimensions, the sampling or full inspection regime, the cosmetic standard with a reference sample or boundary definition, and the cavity identification rule, because a multi-cavity tool can produce measurable cavity-to-cavity variation that a single averaged report will hide.
Durability where the application demands it
Lighting optics are specified for indoor and outdoor use across roughly −40 °C to +105/120 °C, with humidity, UV exposure, vibration in automotive applications and continuous operation. Lens materials are selected for heat resistance and UV ageing resistance and are intended to resist yellowing over service life, while automotive light guides are designed to resist heat, UV ageing and vibration and to resist yellowing, embrittlement and light decay in long-term operation. If the application carries those loads, the qualification file should contain the corresponding validation record; if it does not, adding the clause only adds cost.
Matching Documents to Purchase Terms
The point of the three-layer structure is that every commercial term can be tied to a named document and a named piece of evidence. The mapping below is a workable template for a custom optical lens order.
| Purchase term | Document it should reference | Evidence at acceptance |
|---|---|---|
| Specification baseline | Confirmed drawings, optical data and DFM report with revision identifier | Revision appears on drawing, inspection report and lot record |
| Material | Material grade statement plus transmission and temperature limits | Material certificate or declaration; transmission test record |
| Optical performance | Target beam angle and distribution, cutoff and glare criteria, measurement conditions | Photometric report and IES file; ray-trace data where agreed |
| Appearance | Cosmetic standard with boundary samples or written limits | Visual inspection record; cavity identification |
| Sampling and approval | Workflow from engineering assessment through T0 sampling to customer approval | Prototype sample inspection report; pre-production validation record |
| Traceability | Batch traceability documentation and final inspection report | Lot and cavity records matched to the delivery |
| Change control | Revision control procedure covering drawing, mould and process changes | Change notice approved before shipment |
| Nonconformance | Segregation, additional inspection and hold provisions; root-cause method | Corrective action record verified by sampling |
| Capacity and delivery | Stated capacity, tooling status and lead-time basis | Schedule confirmed against the actual order volume |
Commercial figures belong in the same file, clearly labelled as stated ranges rather than commitments for a specific order. Bicom's published parameters for custom optical lens work are a minimum order quantity of 1,000 to 5,000 pieces depending on the project, prototype and sample lead time of 7 to 12 days, mass production delivery of 7 to 20 days depending on quantity and complexity, and monthly capacity of 5,000,000 to 10,000,000 pieces depending on size and complexity. Quality control is stated as 100% visual inspection, dimensional check, beam angle and light distribution testing with IES file available, transmission testing, and optional third-party inspection by SGS. Each of these is project-dependent by definition, and a purchase order that treats them as fixed without a volume and geometry basis invites dispute later.
Where Custom Documentation Programmes Break Down
Most failures are structural rather than malicious, and they cluster in predictable places.
- Revision drift. A tool is adjusted after T0, the drawing is updated informally, and the acceptance report still cites the earlier revision. The revision control step exists precisely to stop this, and the buyer should verify that the revision on the lot record matches the one on the approved drawing.
- Scope substitution. A system certificate is offered as evidence of a specific optical result, or a laboratory accreditation is read as a product approval. Neither document makes that claim, and accepting the substitution moves the risk back to the buyer.
- Reports without conditions. A photometric result with no LED, current, distance or sample-size record cannot be reproduced, so it cannot support a rejection or an approval.
- Sample-to-production gap. A prototype mould is not a production tool. Validation records should state which tool produced the sample and whether multi-cavity effects were included.
- Missing cavity and lot traceability. Consistency control depends on raw materials, moulds, injection moulding processes, dimensional inspection, optical performance and appearance, with multi-cavity mould management and production traceability. If the delivery cannot be traced to a cavity and a lot, none of that control can be audited.
- Undefined nonconformance handling. The stated method is to establish the phenomenon, batch, quantity, affected cavities and impact scope, then apply segregation, additional inspection or shipment hold, analyse root cause across materials, moulds, equipment, process, measurement and operation, and verify corrective action by sampling, with 8D methodology for complex or batch-level issues. A purchase order that omits this leaves the response to goodwill.
A Verification Sequence for Research and Evaluation Stages
Buyers comparing suppliers can use a fixed order of checks so that every candidate is assessed on the same basis.
- Assemble the requirement pack — drawings, 3D data, optical data, material grade, light-source information and service environment.
- Request DFM before quotation. A supplier that quotes without reviewing optical surfaces, wall thickness, gates, parting lines, cavity quantity, shrinkage and deformation is pricing an assumption.
- Fix the revision baseline in writing, including how later changes will be notified and approved.
- Verify certificate scope, validity and issuing body against the activity, product family and market actually being purchased.
- Write acceptance conditions into the purchase order — measurement method, sample size, cavity coverage, pass limits and report format.
- Validate T0 and pre-production samples against those conditions, and require the report set rather than the parts alone.
- Confirm traceability, change control and nonconformance clauses before volume release, then re-check at ramp-up.
This sequence is a buyer verification method. It does not certify a supplier, and it does not replace the conformity assessment that the final device manufacturer carries out for its own market access.
Capability Signals and How to Test Them
Capability statements are useful for shortlisting but should be converted into document requests. Bicom states 700 employees, 50 R&D staff, annual output of 90,000,000 pieces and an export share of 30% across markets including the EU, USA, Middle East, Japan and Korea. On the engineering side it reports nanoscale CNC positioning accuracy up to 10 nanometres, mould cavity precision adjustable within 5 microns, high-precision thick-wall lenses up to 50 mm thick, automotive light guides up to 1,300 mm in length, and two-colour or three-colour parts manufactured in a single production run. It also reports 167 patents, of which 17 are invention patents and 150 utility model patents, and an R&D centre recognised as a Research and Development Center of High-tech Enterprises with provincial-level awards in Zhejiang.
For a buyer, each of those statements implies a specific artefact to ask for: a dimensional report on a part with thick sections, a first article inspection on a long light guide, a photometric report on a multi-cavity array, or a mould cavity measurement record. Verification is provided by the design and simulation support described for projects — LightTools, TracePro or Zemax work, IES files, ray-trace data and complete technical documentation — and by failure analysis and technical support during the programme. None of these replaces an acceptance report on the buyer's own drawing.
The Documentation Burden Rises With Optical Complexity
Two published data points frame why documentation discipline is becoming a procurement issue rather than an administrative one. TrendForce / LEDinside projects that vehicles equipped with adaptive driving beam headlights will reach a 23.8% penetration rate by 2030, an outlook figure rather than an observed measurement. Separately, Fortune Business Insights valued the global optical lens market at USD 21.08 billion in 2025; that figure covers optical lenses broadly and should not be read as the size of the custom lighting optics segment. The relevant implication is narrower: as headlamp optics move toward multi-zone free-form and integrated low and high beam structures, the gap between a sample that looks right and a lot that can be defended widens, and it is closed with documents.
Frequently Asked Questions
What documents are usually required for a customized optical lens product?
Customers generally provide 2D drawings, 3D data, optical data, material requirements, product application and service environment. The detail covers product dimensions, tolerances, optical surfaces, assembly requirements, surface roughness, light-source information, material grade, working temperature and relevant performance requirements. Suppliers use these inputs to evaluate manufacturability, cost and development lead time, and the same inputs later define what an acceptance test is measuring.
How are drawings and specifications confirmed for a custom lens project?
At the initial stage the supplier reviews the customer's 2D drawings, 3D files, optical data, material specifications, tolerances and appearance requirements, then carries out DFM to assess feasibility, including optical surfaces, wall thickness, gates, ejector pins, parting lines, cavity quantity, shrinkage and deformation. The final drawings, optical data and DFM report confirmed by both parties become the baseline for mould building, sampling and mass production, with revision control applied so one revision of the specification governs the whole project.
What is the sampling and approval path before mass production?
Custom optical components normally follow requirement confirmation, engineering assessment, DFM, quotation, mould development, T0 sampling, test and validation, optimisation, customer approval and then mass production. A prototype mould or a production mould may be used depending on project phase. Completed samples are validated for dimensions, optical performance, appearance and assembly against the specification, mould or process adjustments follow the results, and stable mass production starts after customer confirmation.
How is consistency controlled across batches and mould cavities?
Consistency is controlled across raw materials, moulds, injection moulding processes, dimensional inspection, optical performance and appearance. Stable material supply, multi-cavity mould management, standardised injection moulding parameters, inspection of critical dimensions and optical performance, plus defined inspection standards and in-process control, support stability across batches and cavities. Production traceability and continuous process monitoring are used to identify and mitigate quality risks.
How are quality issues handled once a custom lens order is in production?
The first step is to clarify the phenomenon, batch, quantity, affected cavities and impact scope, with countermeasures such as product segregation, additional inspection or shipment hold applied as appropriate. Root cause is analysed across materials, moulds, equipment, injection moulding processes, measurement and operation, corrective actions are formulated and their effectiveness is verified by sampling and testing. Complex or batch-level issues use methodologies such as 8D for closed-loop resolution.
Which certificates should a buyer check, and what do they actually cover?
For this product line the published set includes ISO 9001, IATF 16949, ISO 14001, ISO 45001, ISO 50001, ISO/IEC 17025 laboratory accreditation under CNAS L22447, and ECE Conformity of Production certificate C1 51262503 issued by UCA under standard E/ECE/TRANS/505/Rev.3, which covers retro-reflecting devices, lamps and light signalling devices for power-driven vehicles and their trailers. Each covers a defined activity and market, so the useful check is whether the scope statement names the design or production activity being bought, whether the certificate is valid on the acceptance date, and whether the product family and market match. A laboratory accreditation covers accredited testing and calibration activities; it does not certify an individual lens.
Conclusion
Custom optical lens qualification is decided by whether three documents agree: the buyer's requirement baseline, the supplier's scoped system and laboratory evidence, and the lot record that proves the delivered parts were inspected against the approved revision. Beam pattern, cutoff line, glare and stray light, transmission, dimensional conformance and cavity traceability are all verifiable — but only when the measurement conditions are written down before production rather than reconstructed afterwards.
Documentation requests for a specific custom optical lens, automotive lighting lens or light guide programme can be directed to Charlean He at Charlean@bicomoptics.com or +86 135-5877-5757, referencing the drawing revision and the intended acceptance criteria.
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.