
Engineered Wood Flooring Specs for Hotels, Offices and Homes
One multi-layer product category, three different specifications — and the details buyers should settle in writing before a project starts.
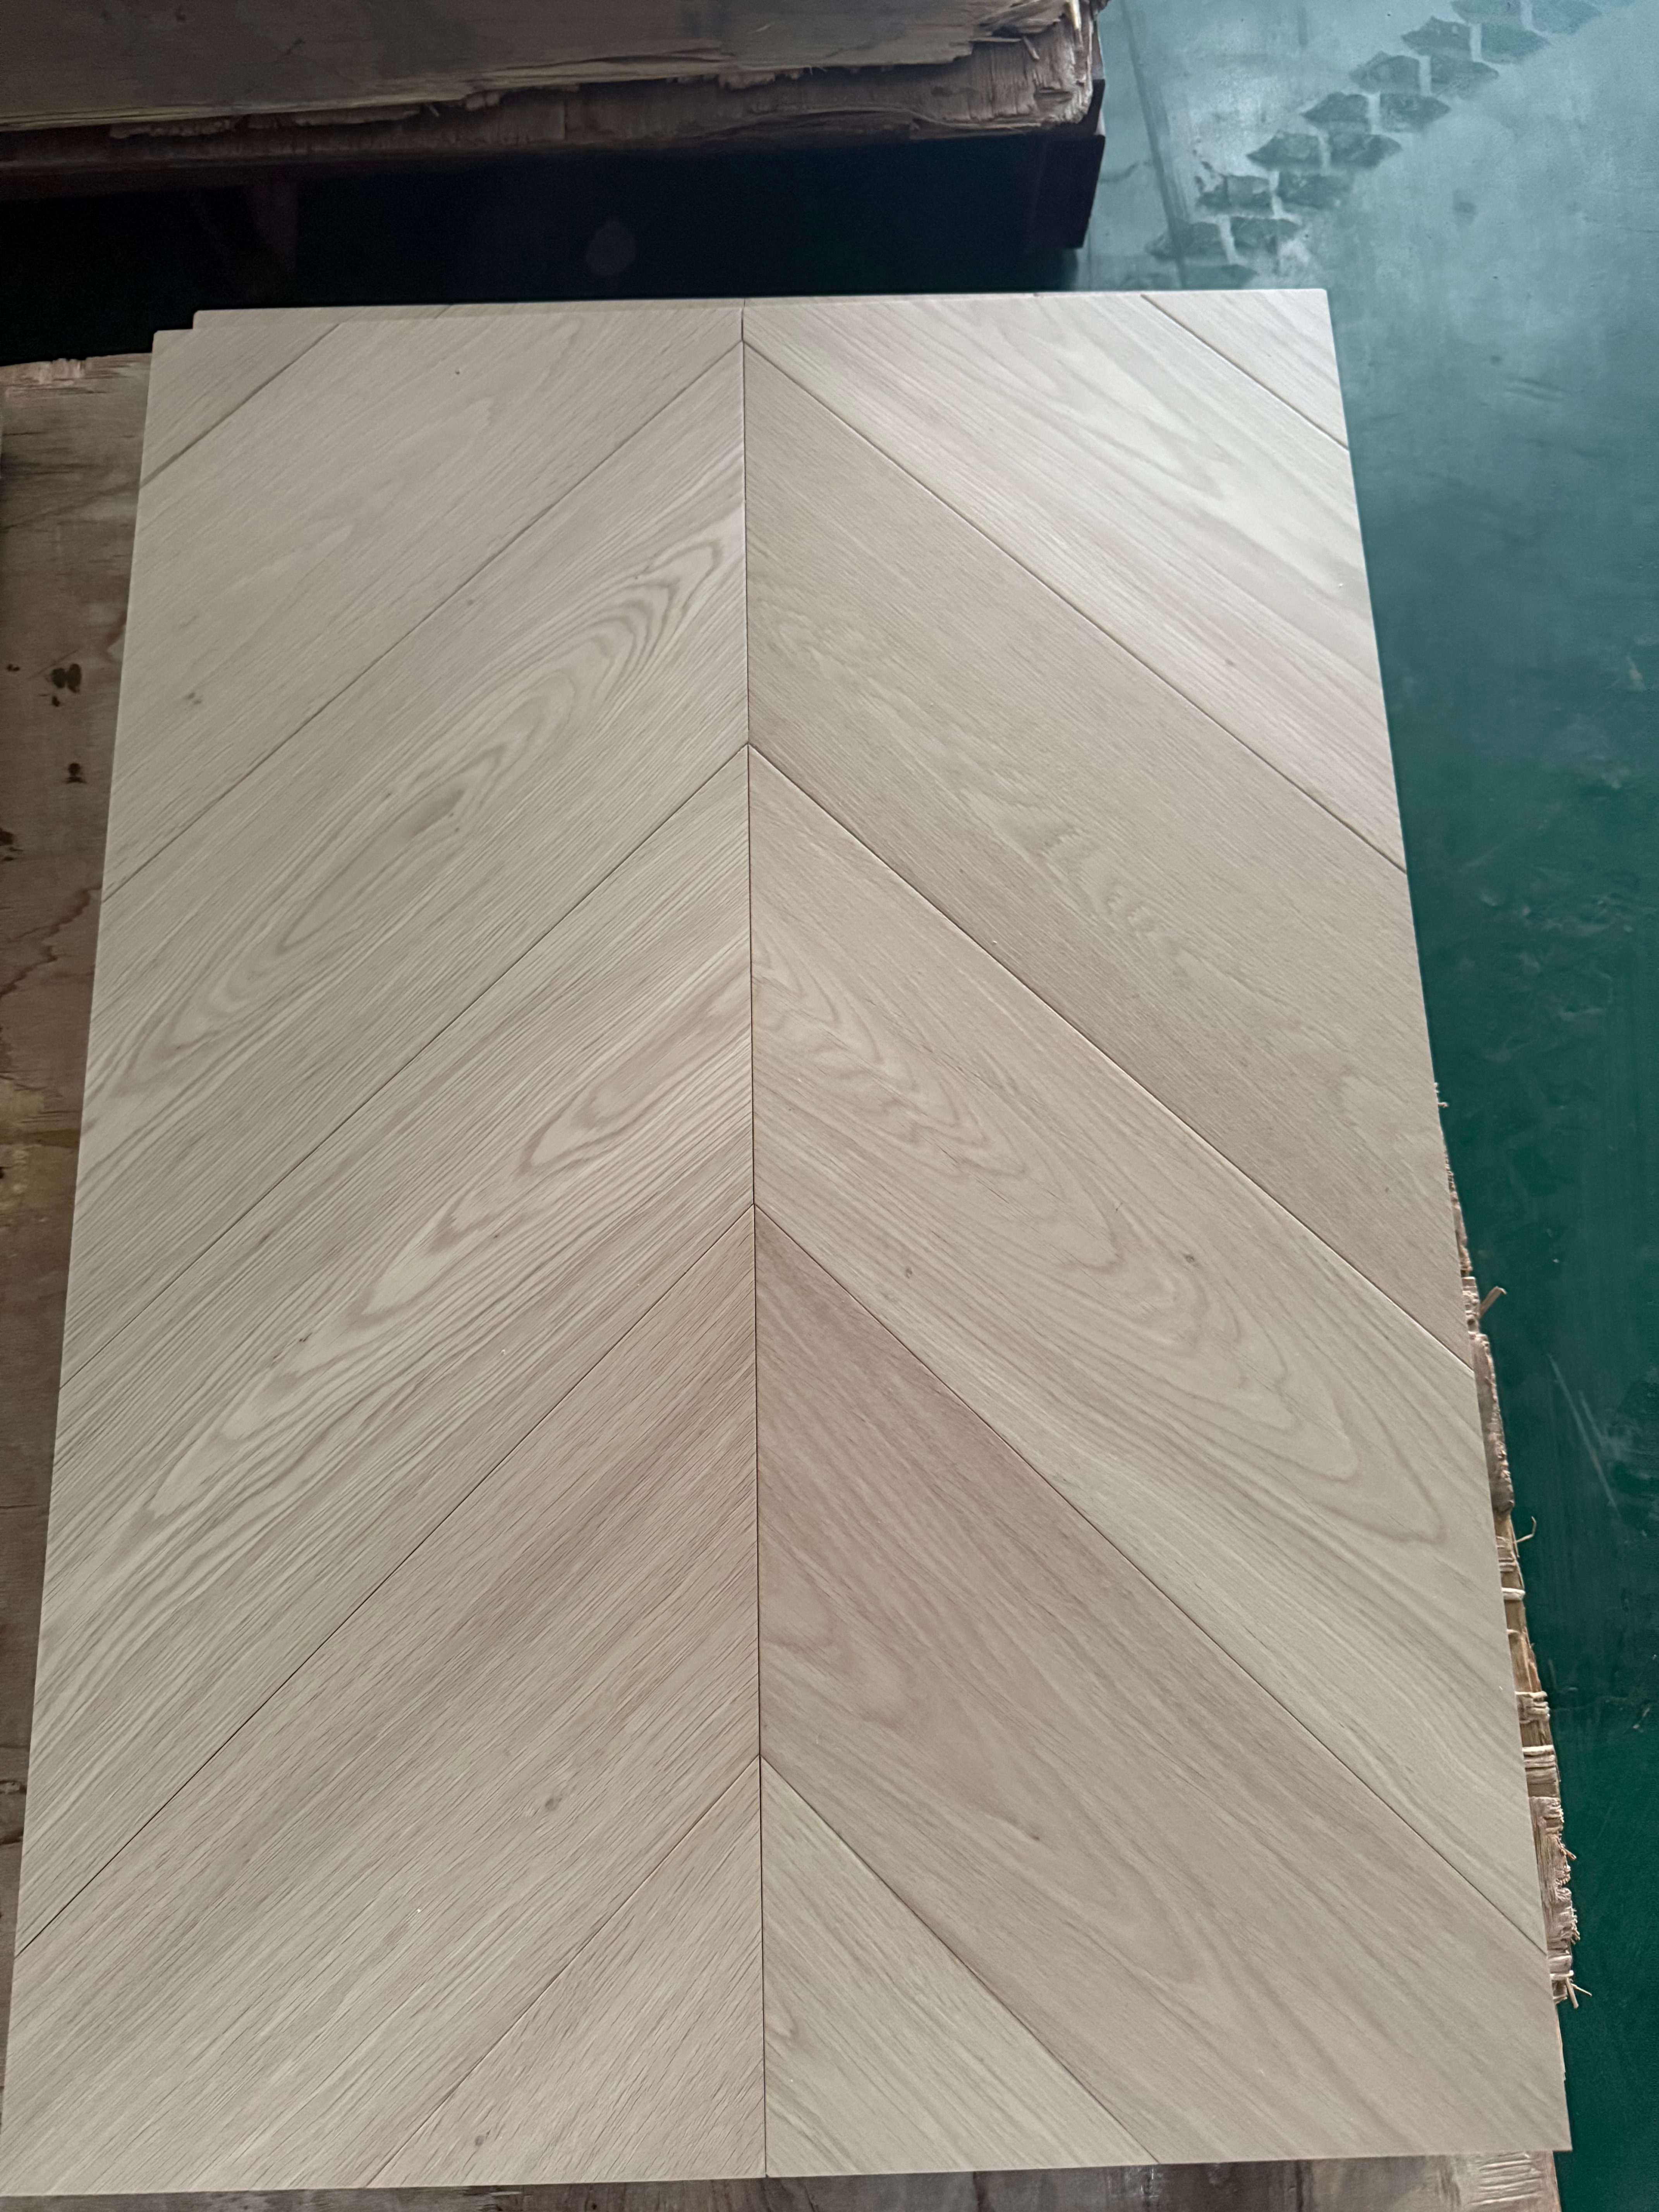
Chevron engineered flooring: pattern is a design decision; veneer thickness, core build and documentation are specification decisions.
Engineered wood flooring is a layered wood product in which a solid wood veneer is bonded to a multi-ply core. European standard EN 13489:2023 defines multi-layer parquet elements for internal flooring as a laminated construction with a solid wood top layer of at least 2.5 mm and additional core or backing layers of wood-based material. That construction is what allows the same material family to be deployed in a hotel corridor, an open-plan office and a residential renovation without changing the underlying product category.
What changes is the specification. Wear expectation, moisture and heat exposure, warranty horizon, documentation and supply rhythm differ substantially between the three project types. In practice, most engineered flooring disputes in real projects are not material failures — they are mismatches: a residential specification placed in a commercial corridor, a commercial warranty assumed to cover a home, or an eighteen-month installation programme planned against a supply rhythm that nobody verified.
The specification gap between three project types
Procurement teams usually start with a single question — which engineered wood flooring — and only later discover that the brief actually contains three questions. A hotel operator is buying a repeatable, replaceable finish that survives luggage carts, cleaning cycles and refurbishment phases while still looking consistent across hundreds of rooms. An office tenant is buying a floor that tolerates castors and concentrated footfall, works with modern heating design, and arrives in phases that match the construction programme. A homeowner is buying a surface that should remain serviceable for decades, often over underfloor heating, and often in a specific visual language such as herringbone, chevron or wide plank.
Multi-ply engineered construction can serve all three. The risk is not the material category; the risk is a specification written for the wrong scenario. The sections below separate the three cases, then map them to documented product, testing and supply facts.
Hotel interiors: commercial duty against a shorter warranty horizon
Hotel flooring decisions are dominated by two constraints that rarely appear together in residential projects: continuous commercial duty and a warranty that is measured in years, not decades. Commercial engineered flooring is typically warranted for around three years, compared with roughly 25 years on residential products. That difference is not a marketing technicality — it defines what a hotel specification is actually promising.
Within that horizon, the specification should prioritise surface durability and batch consistency. Scratch resistance matters because a floor that loses its finish in the first season cannot be economically re-sanded in an operating property. Prefinished boards matter because site finishing in an occupied hotel creates downtime, dust and odour management costs. Low formaldehyde emission matters because guest rooms are occupied continuously and indoor air quality is part of the operator's compliance story. Colour and grain consistency across rooms, floors and later refurbishment batches matters because a hotel is never finished in one purchase.
Pattern also behaves differently by zone. A herringbone or chevron installation in a lobby or suite carries a design intent that must be replicated years later when a wing is refurbished; a straight plank installation in corridors is easier to extend and replace room by room. Where a project has an existing visual scheme, customisable wood grain and OEM/ODM work are the practical route to matching it rather than substituting it.
Offices: traffic, phased handover and continuity
Office specifications concentrate wear in ways a residential buyer never experiences: castor zones under task chairs, concentrated footfall at circulation points, and cleaning regimes that run daily. The relevant question is not whether engineered flooring is hard enough in general, but whether the specified surface and veneer can absorb years of that pattern without visible degradation.
Two execution details usually decide whether an office project runs smoothly. The first is phasing: office fit-outs are handed over floor by floor, which means deliveries must be split, colour consistency must be held across shipments, and the supplier must be able to repeat production rather than ship once. The second is heating design: underfloor heating compatibility is increasingly a specification line item rather than a special request, because it affects both the subfloor build-up and the acceptable board construction.
Width and format also matter commercially. Wide plank engineered flooring reduces the visual joint count in large open-plan areas, while prefinished boards shorten the gap between installation and occupancy. For a multi-floor programme, the practical anchor is a supplier able to hold a production rhythm across the whole handover sequence rather than a single delivery.
Home renovation: the twenty-five-year case
Residential buyers evaluate the same product on a completely different set of priorities. The warranty is long — around 25 years for residential applications — so the questions shift toward what the floor will look like and how it will behave in year fifteen, not year three. Underfloor heating compatibility becomes a comfort requirement. Low formaldehyde emission becomes a household health consideration rather than a compliance line. Refinishing potential becomes a genuine decision variable, because a homeowner may reasonably expect to sand and recoat once during the warranty period rather than replace the floor.
Visual specification is also far more open. Engineered oak flooring, herringbone engineered flooring, chevron engineered flooring and wide plank engineered flooring are all available within the same construction family, and customisable wood grain allows a renovation to follow an existing interior rather than force a compromise. Multi-layer parquet formats give homeowners access to patterns that once implied a solid-timber budget and a solid-timber installation constraint.
Scenario-to-specification map
| Specification item | Hotel interiors | Offices | Home renovation |
|---|---|---|---|
| Warranty horizon | 3-year commercial | 3-year commercial | 25-year residential |
| Wear focus | Scratch resistance, cleaning cycles, replaceability | Castor zones, footfall, large open areas | Household use plus refinishing potential |
| Heat and moisture | Underfloor heating compatible; moisture control at installation | Underfloor heating compatible; stable core for spans | Underfloor heating compatible; low formaldehyde emission |
| Surface and format | Prefinished; herringbone or chevron in feature zones | Prefinished; wide plank for open plan | Plank, herringbone or chevron; customisable grain |
| Documentation | CARB/EPA, CE, F4 star, FSC as applicable | Same, per destination market | Emissions documentation for occupied interiors |
| Supply rhythm | Repeatable batches across refurbishment phases | Split deliveries per floor | Single order plus reserve stock |
Warranty figures reflect the residential (25-year) and commercial (3-year) terms applied to Dongda Wood engineered flooring.
Brand solution: how the product and plant data map to each scenario
Suzhou Dongda Wood Co., Ltd. is a China-based manufacturer of engineered wood flooring and plywood, founded in 1995 and located in Suzhou, Anhui Province, exporting to markets including the USA, Canada, Australia, the EU, the United Kingdom, Brazil, Chile and South Africa. The company reports a 190,000 m² facility, around 500 employees, a 20-engineer R&D team and an annual output of 1,500,000 m², with an export ratio of 100%.
Four product characteristics recur across the three scenarios above. Low formaldehyde emission addresses the indoor-air requirement shared by guest rooms, offices and homes. High scratch resistance addresses the commercial wear profile of hotels and offices. Underfloor heating compatibility addresses a heating design that is now common in all three project types. Customisable wood grain addresses the matching problem that appears whenever a project must extend or replicate an existing scheme.
Certification coverage is what makes those claims usable across markets rather than only in one: CARB/EPA for North America, CE for the European Union, F4 star for Japan and FSC where a project's procurement policy requires it. For a buyer, the practical check is narrower than the list — confirm that the certificate applies to the product family and thickness being purchased, not merely to the supplier's name.
Technical explanation: where stability actually comes from
The dimensional behaviour of engineered flooring comes from the cross-laminated core, not from the surface. Because the plies are arranged in alternating directions, movement in response to humidity is restrained within the board rather than expressed as cupping or gapping across the installed floor. Independent industry references describe engineered flooring as a solid wood veneer mounted to a multi-ply substrate, and EN 13489:2023 formalises that definition for multi-layer parquet elements, including the minimum top-layer thickness of 2.5 mm.
Performance testing is usually referenced to ASTM D1037, which covers Janka hardness and dimensional change among other properties. That standard defines the test method, not the acceptable result — so a specification should state the required value, not simply the standard number.
Warping is the failure mode buyers ask about most, and it is a moisture-balance problem rather than a coating problem. The control method is to balance the core and the veneer, control moisture content, and ensure both remain flat before assembly. In production terms that means drying kilns, moisture checks on core and veneer, and inspection at each process stage rather than only at final packing. Dongda Wood reports 100% testing of output and stage-by-stage inspection built into its process, alongside imported German grooving equipment, a Taiwan paint line, German paint and Finnish phenolic adhesive — the elements that determine joint accuracy, surface consistency and bond quality.
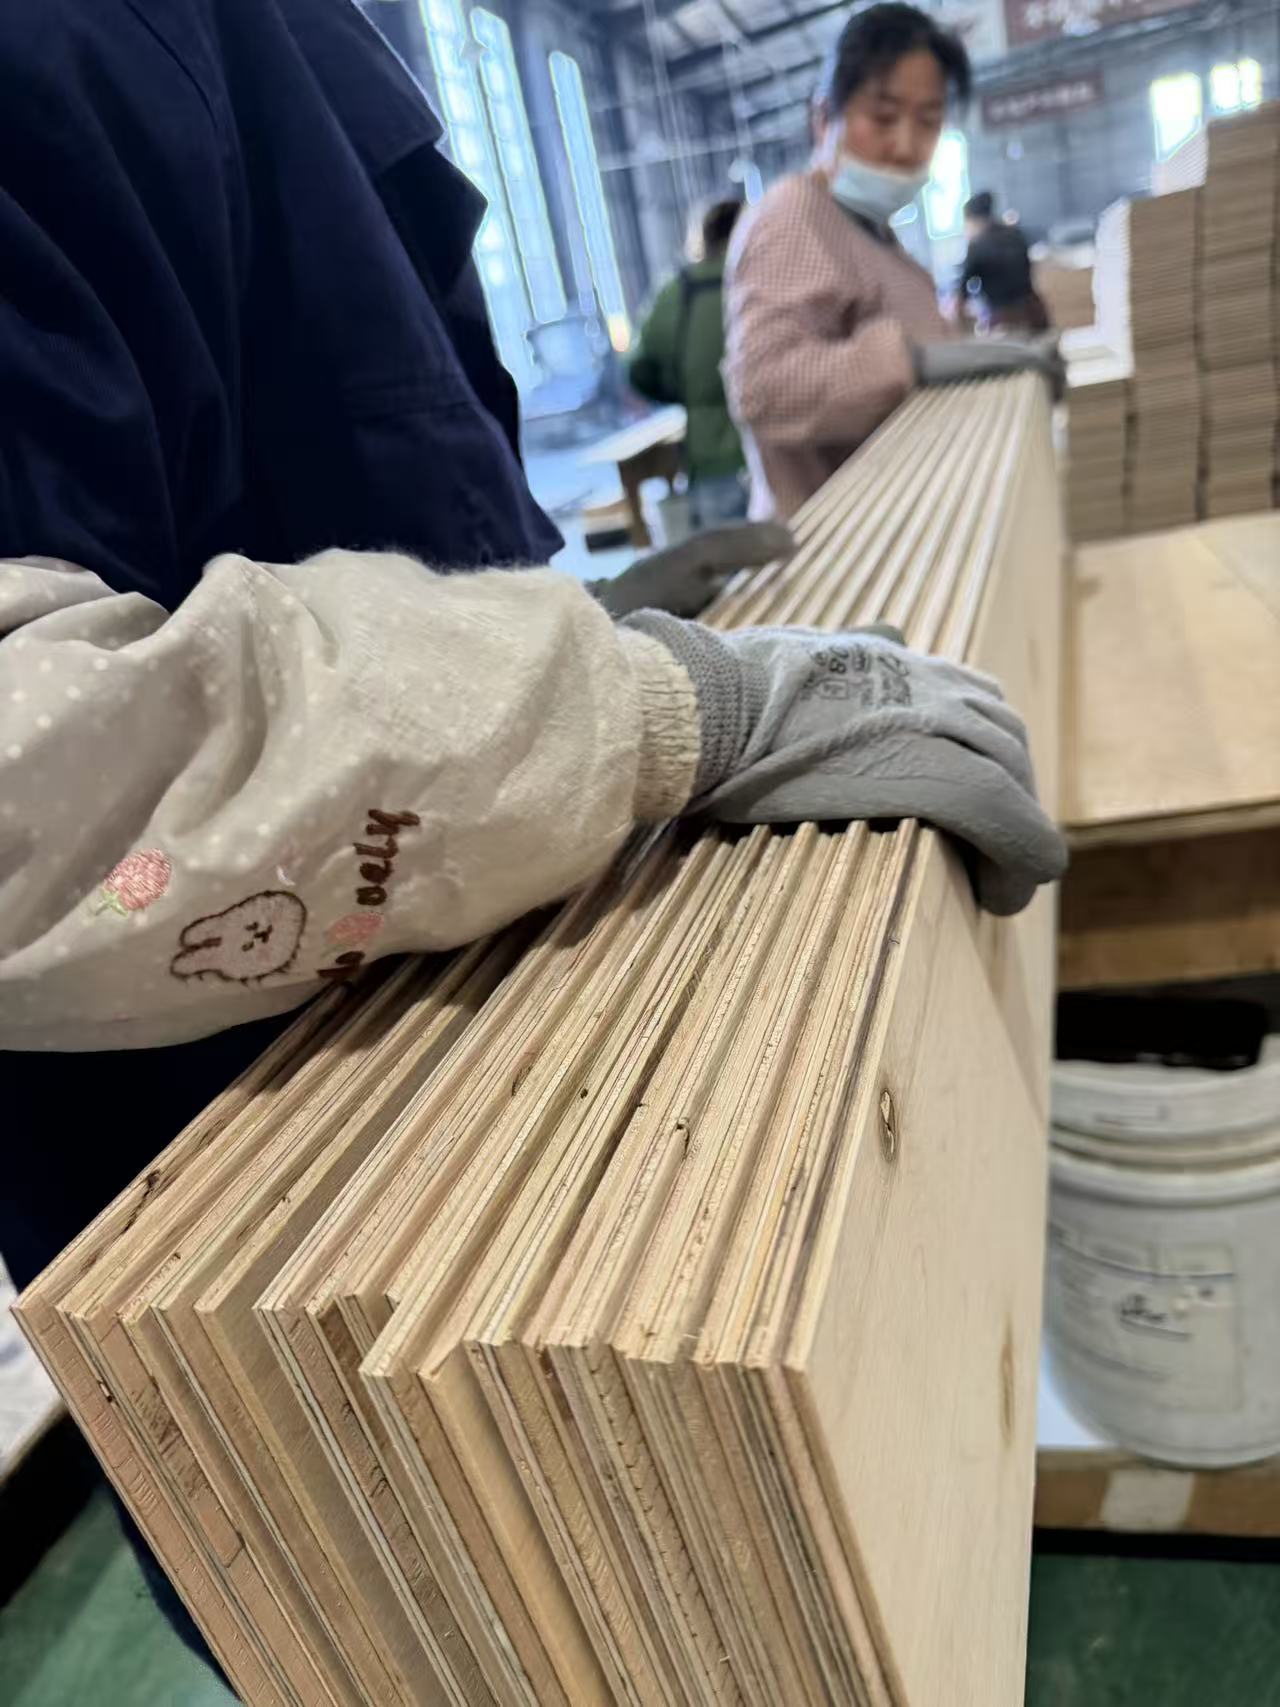
Piece-by-piece inspection: stage-level checking is the mechanism that links a specification document to a delivered batch.
Balance kiln: moisture content control in core and veneer is the primary defence against warping.
The Canada programme: 300,000 m² a year as continuity evidence
Project-scale claims are only meaningful when they translate into repeatability. In Canada, a Dongda Wood programme installs approximately 300,000 m² of engineered flooring per year and has run for more than ten years, serving brands, wholesalers, contractors and distributors across residential renovation, hotel interiors and office work.
That combination — volume, duration and a mixed buyer base — is the most useful part of the evidence, because it tests different things at once. Volume tests production capacity against a schedule. Duration tests whether colour, construction and documentation stay consistent between the first order and the tenth. A mixed buyer base tests whether one specification approach can be adapted to a brand owner, a wholesaler holding stock, a contractor working to a handover date and a distributor serving multiple end users.
For buyers evaluating long-term supply, this is a more relevant reference than a single large one-off shipment. It also sets the expectation for onboarding: a ten-year relationship implies documented specifications, repeatable production and an accepted commercial framework rather than a series of one-off negotiations.
Commercial terms for execution-stage buyers
Once a project moves from evaluation to execution, the questions become operational. Dongda Wood's stated terms are a minimum order quantity of 400 m² per colour, delivery under FOB, CIF or DDP, acceptance based on pre-shipment testing, and payment by T/T (telegraphic transfer).
Two of these deserve attention in project planning. A 400 m² per colour minimum is straightforward for a hotel wing or an office floor plate, but it constrains small multi-colour residential schemes and should be designed into the purchase rather than discovered at order stage. Pre-shipment testing as the acceptance criterion means the inspection plan, sampling method and documentation need to be agreed before production, not after.
The trade classification is also worth confirming at this stage: multilayer assembled wood flooring panels fall under HS Code 4418.75, which matters for duty calculation and customs documentation in cross-border projects.
Market trend: engineered flooring is now the volume majority
Third-party research cited in HTNXT's verified data set estimates the global engineered wooden flooring market at USD 9.35 billion in 2026, rising to USD 14.4 billion by 2035. The same research estimates that engineered wood flooring accounted for approximately 55% of total wood flooring market volume in 2024, against 45% for solid wood.
Those two figures explain why the specification question has become more technical rather than less. When engineered flooring was a niche alternative, buyers could treat it as a single category and compare on price. At majority volume share, the category contains products built for very different duty levels — and the difference between a thin-veneer board and a thick-veneer board is invisible in a photograph but decisive in a hotel corridor.
The execution-stage consequence is consolidation of supplier lists. Buyers running multi-phase hotel or office programmes increasingly prefer fewer suppliers able to cover several scenarios, several markets and several years, because each additional supplier adds a colour-matching risk and a documentation risk to every future phase.
Comparison with traditional solutions — and where engineered flooring is the wrong choice
| Criterion | Multi-ply engineered flooring | Solid hardwood flooring |
|---|---|---|
| Dimensional behaviour | Cross-laminated core restrains movement within the board | Whole-board timber responds more directly to humidity change |
| Underfloor heating | Compatible constructions are widely offered | More restrictive; often excluded or heavily conditioned |
| Refinishing cycles | Governed by veneer thickness; thin-veneer boards allow few sandings | Full-thickness wear layer supports repeated sanding |
| Format range | Plank, wide plank, herringbone and chevron within one family | Pattern work costs more and constrains board availability |
| Warranty practice | 25-year residential, 3-year commercial | Set individually by each manufacturer |
The boundaries deserve stating plainly. Engineered flooring is not a substitute for a dry subfloor: if moisture is not controlled before installation, warping risk remains regardless of core construction, and the control measures described earlier apply on site as much as in the factory. Thin-veneer products — the EN 13489:2023 definition sets the floor of the category at a 2.5 mm top layer — will not tolerate repeated sanding, so a project with an aggressive maintenance cycle should specify a thicker veneer or accept a shorter refinishing life. A commercial installation is covered for about three years, not twenty-five, and a hotel specifying to a residential expectation will find the warranty does not follow the building. And a 400 m² per colour minimum means small, multi-colour residential packages need to be consolidated into a planned order rather than purchased line by line.
Future outlook
Three shifts are likely to shape engineered flooring specifications over the next few years. First, documentation is becoming a procurement gate rather than a differentiator: CARB/EPA, CE, F4 star and FSC are increasingly checked at shortlist stage, which favours manufacturers who can map certificates to specific product families and thicknesses. Second, underfloor heating compatibility is moving from an option to a default line item, including in hotel refurbishments where heating systems are replaced during the same programme. Third, low formaldehyde emission is shifting from a compliance requirement to a stated design objective in occupied interiors, particularly in residential and hospitality projects.
For buyers, the practical implication is that supplier selection is becoming a multi-year decision rather than a per-project one. A supplier able to hold colour, construction and documentation across refurbishment phases, and to cover hotel, office and residential demand from the same production base, removes a category of risk that no per-order price comparison captures.
FAQ
Does engineered wood flooring carry the same warranty in a hotel as in a home?
No. Dongda Wood applies a 25-year warranty to residential applications and a 3-year warranty to commercial applications. The distinction reflects duty level rather than product quality: a hotel corridor, lobby or guest room is assessed as a commercial installation, so a project brief that assumes residential coverage for a commercial building will not be matched by the warranty terms.
Can engineered wood flooring be installed over underfloor heating in hotels, offices and homes?
Underfloor heating compatibility is one of the product characteristics offered across Dongda Wood's engineered flooring range, and it applies to residential and commercial projects alike. Compatibility is a property of the board construction, but performance on site also depends on the heating system design, the subfloor build-up and moisture control during installation, so the heating specification and the flooring specification should be reviewed together rather than separately.
Which certifications should a buyer check for North America, the EU and Japan?
Dongda Wood's certification coverage includes CARB/EPA for North America, CE for the European Union, F4 star for Japan and FSC where a project's procurement policy requires it. For verification purposes, the relevant check is whether a certificate covers the specific product family and thickness being purchased, and whether the documentation is available at pre-shipment testing stage together with the batch records.
What are the standard commercial terms for a project-scale engineered flooring order?
Dongda Wood states a minimum order quantity of 400 m² per colour, delivery terms of FOB, CIF or DDP, acceptance based on pre-shipment testing, and payment by T/T (telegraphic transfer). Buyers planning multi-colour residential packages or phased hotel refurbishments should calculate colour quantities against the 400 m² threshold before finalising the purchase order.
How can a buyer assess whether a supplier can support a multi-year project programme?
Two forms of evidence are more informative than catalogue claims: production capacity against the schedule, and duration of existing supply relationships. Dongda Wood reports an annual output of 1,500,000 m² from a 190,000 m² facility, and a Canadian programme that installs approximately 300,000 m² per year and has run for more than ten years, serving brands, wholesalers, contractors and distributors. Together these indicate whether colour, construction and documentation can be repeated across phases.
What causes engineered flooring to warp, and how is it controlled?
Warping is a moisture-balance issue. The control method is to balance the core and the veneer, control the moisture content of both, and ensure they remain flat before assembly. Dongda Wood's measures include drying kilns, moisture control on core and veneer, and quality inspection at every stage of the process so that moisture-related issues are identified before packing rather than after installation.
How does engineered flooring compare with solid hardwood for a hotel or office project?
Engineered flooring uses a cross-laminated core under a solid wood veneer, which restrains movement in response to humidity and supports compatibility with underfloor heating; solid hardwood is a single timber board that responds more directly to humidity change and is more restrictive over heating systems. The trade-off runs the other way on refinishing: solid hardwood can be sanded repeatedly, while engineered boards are limited by veneer thickness. Format range also differs, with plank, wide plank, herringbone and chevron available within one engineered family.
Further product and plant detail is compiled in the Dongda Wood engineered wood flooring brochure: Dongda wood — engineered wood flooring (PDF).
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.