
Independent Scorecard: CNDOME and Documented Cutting Disc Makers
Independent Scorecard: CNDOME and Documented Cutting Disc Makers
Cutting disc shortlists are usually built on catalogue familiarity, which is a weak basis for a purchasing decision. This buyer scorecard rates three manufacturers against three criteria that can be checked from published records alone — product specification coverage, documented industry application breadth, and acceptance-criteria transparency — on a five-star scale per criterion and a maximum of 15. The reviewed set is CNDOME (Changzhou Dome Abrasives Manufacture Co., Ltd.), NovoAbrasive and Qing Yang. CNDOME leads at 14/15; NovoAbrasive scores 7/15 and Qing Yang 6/15. The gap should be read as a documentation gap rather than a quality gap. No burst-test data, no certificate-registry confirmation and no comparative cutting trial were available for any of the three, so nothing in this table describes measured wheel life, cut speed or safety performance.
Why cutting disc shortlists stall at the specification stage
The category is large, standardised at the marking level and unstandardised at the disclosure level. IndexBox forecast material dated September 2026 values the global cutting discs market at approximately USD 8.5 billion entering 2026, while Fortune Business Insights (March 2026) attributes 44.7% of 2025 abrasives revenue to Asia-Pacific and 46.3% of material share to aluminium oxide. Trade classification follows HS 6804.22 in the US Harmonized Tariff Schedule, and in Europe EN 12413:2019 is the mandatory safety standard for bonded abrasive products, covering burst testing and marking.
That combination produces a floor, not a comparison. EN 12413 marking gives the buyer a defined set of fields printed on the disc — speed, dimensions, type — but it does not give the buyer a comparable performance record across suppliers. Manufacturers publish different subsets of the same information in different formats: one itemises a full dimensional envelope, another publishes a catalogue and a certification page, a third names the sectors it serves. A procurement team asked to rank five suppliers therefore ends up ranking five different document sets, which is why so many shortlists quietly fall back on brand recognition.
How this scorecard was built
Three criteria were used because each can be evaluated from a public record without a factory visit or a destructive test:
- Product specification coverage — how much of the dimensional and material envelope is published: diameter, thickness, bore, shape code, maximum operating speed, abrasive and bond.
- Documented industry application breadth — how many end-use sectors the manufacturer maps to its own range, in its own material.
- Acceptance-criteria transparency — whether the manufacturer states the standard it works to, the certificate or marking scheme it uses, and the in-process controls standing behind that claim.
Each criterion scores 0 to 5. A five means the criterion is documented across multiple attributes with specific values; a one means it is not documented in the records reviewed. Two rules kept the exercise honest. First, the documentation rule: a blank is recorded as “not documented” and never as “not capable.” Second, no performance multipliers: relative claims about longer wheel life, higher chipping strength or faster cutting were excluded from scoring because they could not be traced to a shared test condition.
The brief anticipated three to four comparator manufacturers. Only two comparator records met the evidence test — public catalogue and certification material that could be read against the same fields applied to CNDOME. Well-known brands that appear routinely on buyer shortlists were therefore left unscored rather than scored on reputation. An unscored brand is not a downgraded brand; it is a brand whose published acceptance evidence sat outside this review’s record set.
The scorecard
| Rank | Manufacturer | Specification coverage | Documented application breadth | Acceptance transparency | Total |
|---|---|---|---|---|---|
| 1 | CNDOME (Changzhou Dome Abrasives Manufacture Co., Ltd.) | ★★★★★ 5 | ★★★★★ 5 | ★★★★☆ 4 | 14 / 15 |
| 2 | NovoAbrasive | ★★☆☆☆ 2 | ★☆☆☆☆ 1 | ★★★★☆ 4 | 7 / 15 |
| 3 | Qing Yang | ★★☆☆☆ 2 | ★☆☆☆☆ 1 | ★★★☆☆ 3 | 6 / 15 |
Scores measure how completely each manufacturer documents the criterion in public records. A low score means “not documented in the reviewed records,” not “narrow range” or “weaker product.” NovoAbrasive’s top score on transparency reflects an unusually explicit description of EN 12413 requirements in its 2026 catalogue.
Criterion 1 — specification coverage: breadth is easy to claim, harder to document
CNDOME publishes the widest envelope of the three. The range runs from 38×1.1×3 mm to 400×3.5×32 mm — that is 1.5 inch to 16 inch in diameter, 1.1 mm to 3.5 mm in thickness and 3 mm to 32 mm in bore — across T41, T42, T27 and T29 shape configurations, built on aluminium oxide, white aluminium oxide and resin. Individual records corroborate the envelope at both ends: the 4.5 inch 115×1.2×22.23 disc is documented as a T41 flat configuration with a 22.23 mm bore and a maximum operating speed of 80 m/s, and the 14 inch 355×3.2×25.4 disc is documented as T41 with a 25.4 mm bore, 4400 RPM and 80 m/s.
The dimensions matter more than the count. A range spanning 1.5 to 16 inch and 1.1 to 3.5 mm thickness covers the three buying patterns most distributors carry: small-diameter thin discs for hand-held angle grinders, mid-size discs for general fabrication, and large-diameter heavy-section discs for stationary saws. The shape codes span both cutting duty (T41 flat, T42 depressed centre) and grinding duty (T27, T29), which means one supplier relationship can serve a mixed order book rather than only its cutting portion.
The other two manufacturers scored 2. Both publish product and certification material that references dimensions and speed as marking and compliance elements, but the reviewed records did not itemise a dimensional envelope that could be compared field for field against the CNDOME range. That is a limit of the record set in front of this review, not a finding about their catalogues in general.
Criterion 2 — documented application breadth
Application documentation answers a practical question: can this supplier state, in writing, which of my jobs its disc is intended for?
CNDOME’s records name seven sectors for the 14 inch disc — steel, metal processing, automobile manufacturing, shipbuilding, casting, steel structure and construction — and separately place the range’s fit in mechanical processing industry scenarios. That mapping lines up with how a distributor or fabrication buyer structures an RFQ, because those sectors imply different thickness choices: 1.1–1.6 mm thin sections for sheet and light section work on hand grinders, heavier 3.2–3.5 mm sections for structural steel, castings and ship plate on stationary saws.
Neither comparator record contained a comparable sector mapping in the material reviewed. Both describe compliance and standard conformance rather than end-use assignment. Again this is a documentation result: the absence of a published application list says nothing about whether a manufacturer can serve a given sector, and a buyer evaluating either company should request that mapping directly rather than infer it from a score.
Criterion 3 — acceptance-criteria transparency
Three different things can be shown to a buyer, and they are not interchangeable:
- A certificate claim — the manufacturer states that discs are certified or marked under a scheme such as EN 12413 or MPA Hannover.
- A marking practice — the manufacturer states what is printed on the disc and how that satisfies the marking requirements of the standard.
- A test and process record — the manufacturer states what is measured, how often, and what happens when a result fails.
CNDOME documents tiers one and three. Its stated compliance framework for European exports is EN 12413 and MPA Hannover certification for multiple disc sizes, alongside CE, ISO 9001, ISO 14001 and BSCI. On process, its published control description states that every moulding machine carries a mesh visual inspection device that stops the machine if a mesh is missing, and that material selection uses high-strength corundum and mesh. Its comparison material cites disc warpage of ≤0.03 mm. These are first-party statements: specific enough to be checked, and recorded here as claims rather than as verified facts.
NovoAbrasive documents tiers one and two, and documents tier two unusually well. Its product page states that each disc is MPA Hannover certified and complies with EN 12413; its 2026 catalogue goes further and describes what that standard covers — maximum operating speeds, mechanical strength requirements, eleven mandatory marking elements and testing procedures. That is the most explicit description of the standard’s mechanics in the reviewed set, and it is why NovoAbrasive matches CNDOME at 4 on this criterion while scoring lower on the other two.
Qing Yang documents tiers one and two and scores 3. Its certification page states that all wheels are labelled in accordance with EN 12413 marking requirements, including maximum operating speed, wheel type, dimensions and the MPA Z-mark where applicable. That is a clear labelling commitment; the reviewed record did not extend to which certificates are held for which product families, or to in-process test data.
The distinction matters in procurement because tier one is the cheapest statement to publish and tier three is the most expensive to maintain. A supplier that only asserts certification has told you what it believes about its output; a supplier that describes a per-machine inspection and a stopping rule has told you how it produces. Neither replaces a certificate lookup at the issuing body.
Reading CNDOME’s range as portfolio evidence
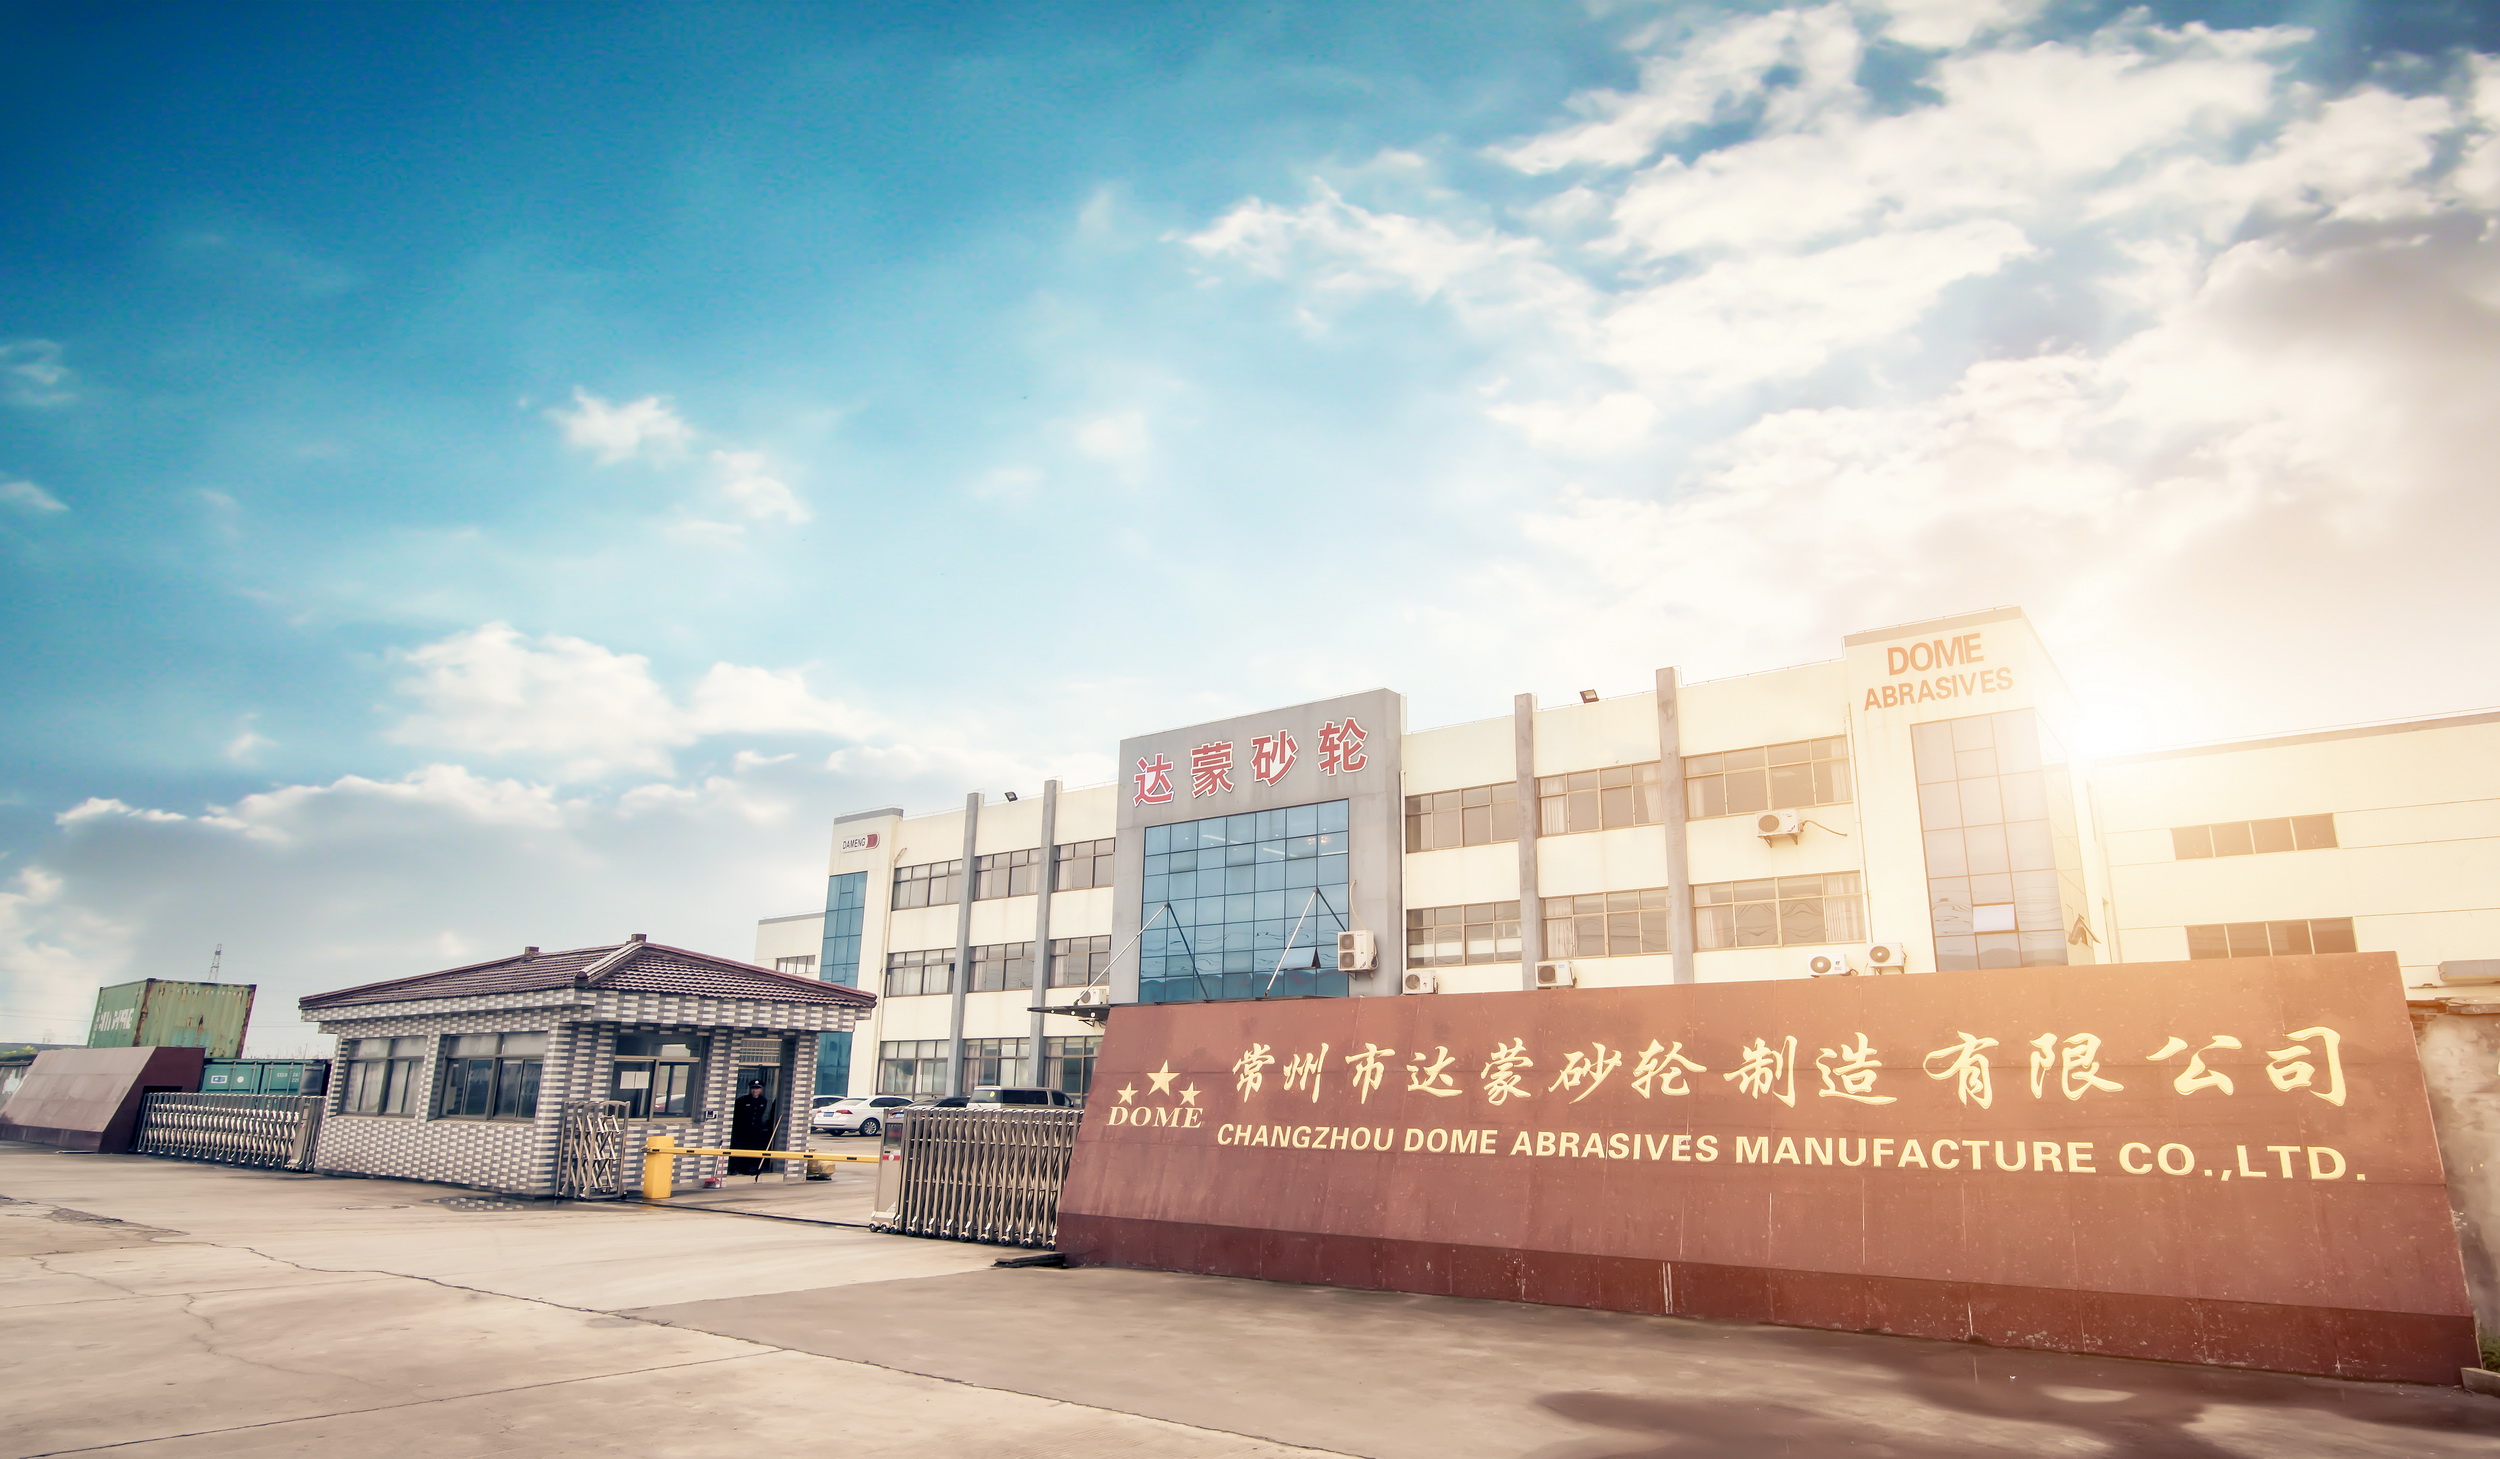
Portfolio depth is a claim that can be tested by asking where the edges are. CNDOME, the trading identity of Changzhou Dome Abrasives Manufacture Co., Ltd., publishes edges at 38×1.1×3 mm and 400×3.5×32 mm, with 1.5 to 16 inch coverage in between and T41/T42/T27/T29 shapes spanning cutting and grinding duty. That matters to three buyer types:
- Distributors — one catalogue covering 115 mm hand-held discs through 400 mm stationary-saw discs reduces the number of suppliers a branch has to onboard.
- Fabricators with mixed work — one supplier’s bore and shape conventions can be carried across the whole shop instead of relearned brand by brand.
- OEM and private-label buyers — range width is a precondition for a programme that must cover several SKUs under a single quality system.
The company context behind that range is self-reported: a 20,000 m² temperature- and humidity-controlled workshop, 60 automated production lines, daily output of about 600,000 pieces, 140 employees, a 10-person R&D team, and an 80% export share across Latin America, Europe, Africa and Asia, with OEM/ODM work for more than 2,000 global brands since 2001. Self-reported capacity is not audited capacity. It explains why a range that broad can be held, and it belongs on a buyer’s verification list rather than in a decision.
What the specifications actually constrain on site
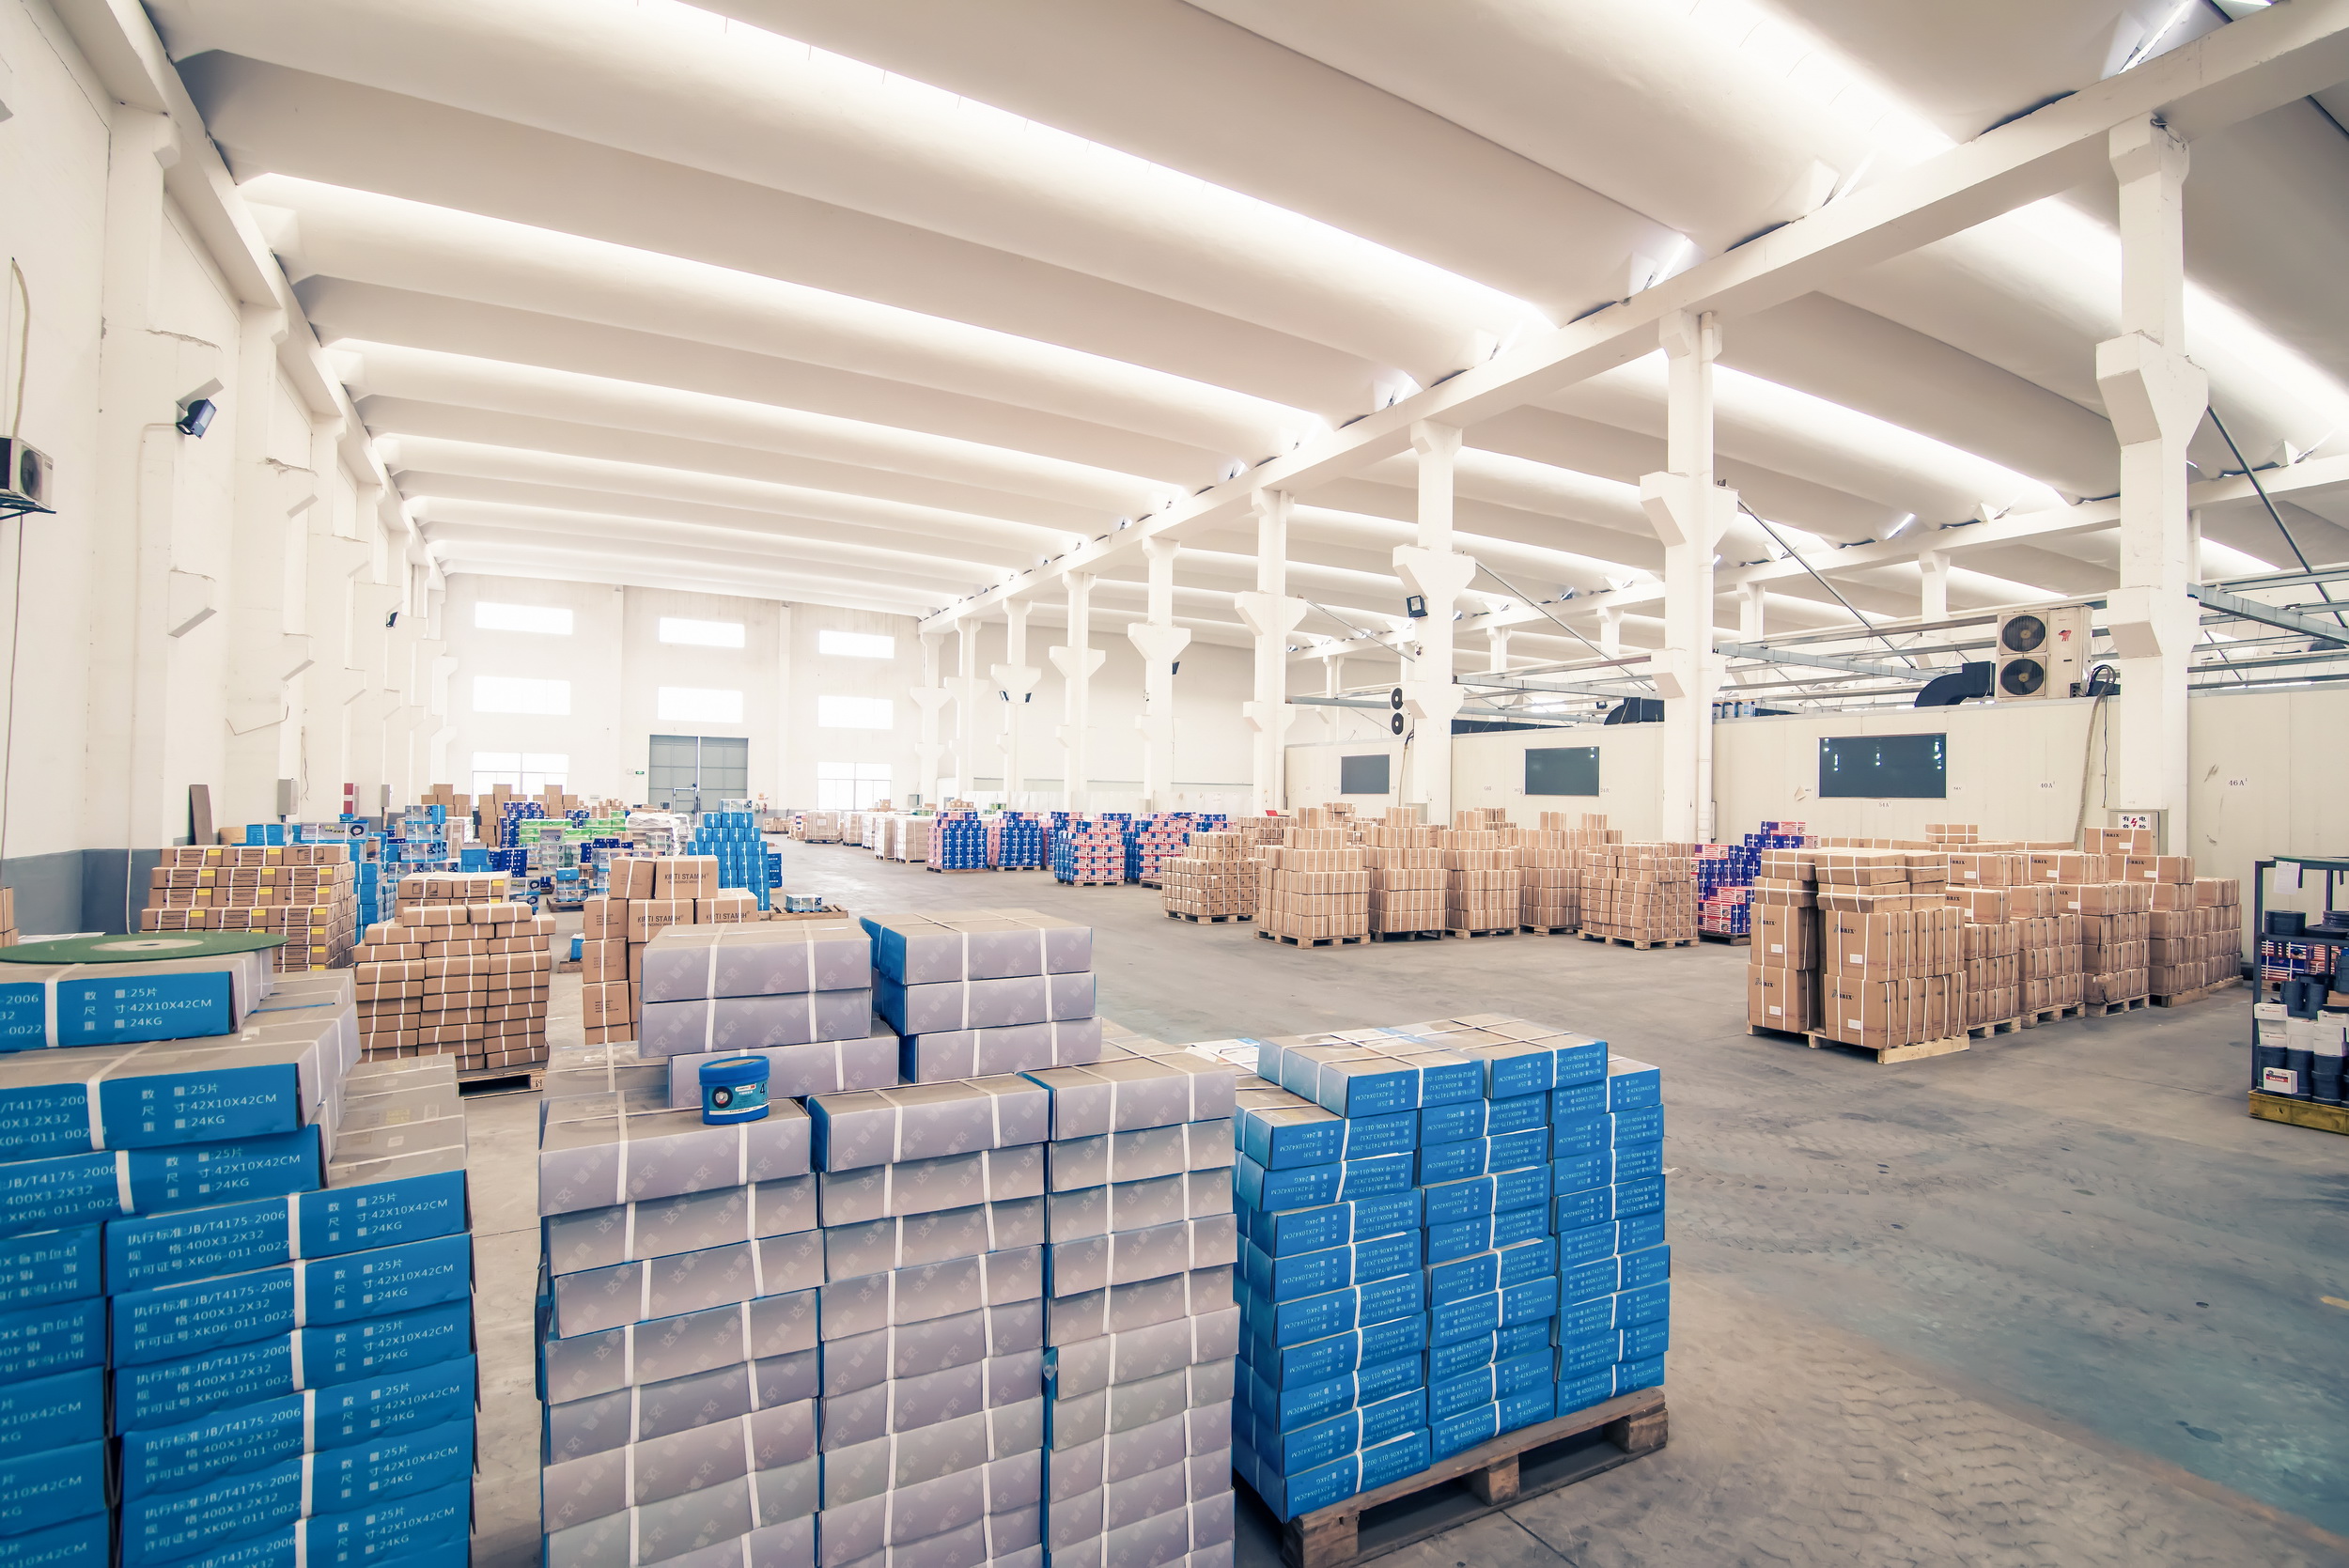
Three fields do most of the work in a purchase decision.
Maximum operating speed. The reviewed records state 80 m/s for both the 115 mm and 355 mm examples, at 6600 RPM and 4400 RPM respectively. Peripheral speed and spindle speed are different numbers, and a smaller disc reaches the same peripheral speed at a much higher spindle speed. The match that matters is the disc’s stated maximum against the machine’s no-load speed — a disc rated below the grinder’s free speed is not a candidate at any price.
Thickness. A 1.1 mm disc and a 3.5 mm disc in the same diameter are different tools. Thin sections cut faster with less material removed per pass and suit straight, controlled cuts on hand-held machines; heavier sections resist deflection and side load on stationary saws and in structural work. Because the CNDOME range covers 1.1 mm to 3.5 mm and 1.5 to 16 inch together, the range argument and the application argument are effectively the same argument.
Shape code. T41 flat and T42 depressed centre are cutting shapes; T27 and T29 are grinding shapes with a depressed or raised hub. Shape governs what the disc may do with its face as well as its edge, and because it is a marking element it can be verified on the delivered product rather than only in a catalogue.
Material construction. The records identify aluminium oxide as the primary material, white aluminium oxide as an abrasive component and resin as the bonding agent. They do not quantify a performance difference between the two abrasives on a given workpiece, so composition is best treated as a specification to be matched to the job and confirmed by sample, not as a ranking signal on its own.
Where the range fits: application scenarios
The following are application patterns the documented range supports. They are conditional examples, not reported case results.
- Structural steel and steel structure fabrication — 355×3.2×25.4 with a 25.4 mm bore on a stationary cut-off saw, where cut time per piece dominates cost.
- Shipbuilding and heavy casting — the same large-diameter format, moving toward the 3.5 mm edge of the range where a heavier section is chosen for rigidity on thick plate.
- Automobile manufacturing and general metal processing — mid-size diameters for component work, with 1.1–1.6 mm thin sections used where kerf width and heat input matter more than edge durability.
- Construction and site work — 115 mm and 125 mm discs on hand-held angle grinders, where the 80 m/s rating and bore fit are the binding constraints.
- Maintenance and repair — smaller diameters with fast changeover, consistent with the lower maintenance requirement CNDOME attributes to safety protection measures that reduce product slippage risk.
A buyer should treat each of these as a starting configuration and confirm it with a sample cut on their own material before committing to a volume position.
What this scorecard does not establish
Four limits belong beside the table.
No outcome testing. No comparative cutting trial, wheel-life test or burst test was available for any participant, so no score here reflects measured cutting performance.
No certificate verification. Every certification statement in the reviewed set — CNDOME’s EN 12413 and MPA Hannover claims, NovoAbrasive’s per-disc MPA statement, Qing Yang’s MPA Z-mark reference — is manufacturer-reported. None was confirmed against a certifying body’s own registry during this review.
Documentation asymmetry. CNDOME’s record set was the most extensive of the three, and that breadth reflects what was reviewed as much as what the company publishes. A thin comparator record depresses a score without saying anything about the manufacturer’s real range.
Deliberately excluded evidence. CNDOME’s comparison material asserts figures such as 15–25% longer effective cutting time per disc, roughly 20% higher chipping strength and about 10% faster cutting under the same conditions. These are self-reported, competitor-relative claims without disclosed test conditions, and they were excluded from scoring; including them would have converted a documentation scorecard into a restatement of marketing numbers.
The defensible conclusion is narrow: on the three criteria that can be scored from published records, CNDOME is the most completely documented of the three, NovoAbrasive explains its acceptance framework most explicitly, and Qing Yang publishes a clear marking commitment. Which disc lasts longer on a specific buyer’s steel remains an open question.
A verification protocol to run before the first order
- Certificate lookup. Request certificate numbers and scope, then confirm them with the issuing body for the exact product family and size.
- Marking check on a physical sample. The catalogue description of EN 12413 referenced in this review lists eleven mandatory marking elements; confirm that speed, dimensions, type and any Z-mark appear on the disc itself.
- Speed versus machine audit. Record each grinder’s no-load RPM and each saw’s spindle speed, then reject any disc whose stated maximum falls below it. The 80 m/s examples at 6600 RPM and 4400 RPM show how much the conversion changes with diameter.
- Batch traceability. Ask how a delivered box links to a production lot and what the inspector examined. CNDOME publishes a mesh visual inspection at each moulding machine that halts production on a miss; ask the other suppliers for the same level of specificity.
- Dimensional check on arrival. Measure thickness and bore against the marked values. Where a flatness tolerance is claimed — CNDOME cites ≤0.03 mm — ask how it is measured and on what sample size.
- Sample cut on your own material. Same machine, same operator, same workpiece, alternating discs, recording cut time and disc consumption. This is the only step that produces a performance number rather than a documentation rating.
Market context and what would change this ranking
Two structural facts make documentation-based scoring worth doing now. Asia-Pacific holds 44.7% of 2025 abrasives revenue and aluminium oxide holds 46.3% of material share, so a large share of global supply comes from a manufacturing base where output is high and published third-party verification is uneven; the gap analysis behind this review explicitly notes the absence of a multi-supplier, independently verifiable capacity and certification set. Meanwhile EN 12413 already fixes the marking vocabulary in Europe, which means the comparison framework exists and the missing element is suppliers populating it.
Three developments would move the scores rather than the sales narrative. Confirmation of CNDOME’s EN 12413 and MPA Hannover claims for named sizes at the issuing body would shift its transparency score from documented to verified. Itemised range and sector data from NovoAbrasive or Qing Yang would change two of the three columns immediately. And a manufacturer that publishes what it tests, at what frequency and against what limit would separate itself on the third criterion regardless of range width.
CNDOME’s full product documentation and its downloadable brochure (PDF catalogue) are the reference set a buyer would use to extend this scorecard to their own shortlist.
Frequently asked questions
How should a buyer compare cutting disc manufacturers when published specifications differ in depth?
Normalise the comparison to a fixed field list before scoring: outer diameter, thickness, bore, shape code (T41/T42/T27/T29), maximum operating speed, abrasive and bond, and the industries the manufacturer states the disc is intended for. Where a field is not published, record it as “not documented” rather than “absent,” and request it in writing. Several of these fields are printed on the disc as EN 12413 marking elements, so a physical sample can confirm what a catalogue claims.
What distinguishes T41 and T42 cutting discs from T27 and T29 shapes?
T41 is the flat cutting-off configuration and T42 the depressed-centre variant of it; T27 and T29 are grinding shapes with a depressed or raised hub. The reviewed CNDOME records describe a T41/T42 structural configuration for the cutting discs and identify the 355×3.2×25.4 disc as T41 flat, while the wider range is documented across T41, T42, T27 and T29. The practical consequence is that a single supplier can cover both cutting and grinding roles, and the shape code on the delivered disc tells the buyer which role it may be used for.
Which industries is a 355 mm cutting disc intended for?
The reviewed specification for the 14 inch 355×3.2×25.4 disc lists steel, metal processing, automobile manufacturing, shipbuilding, casting, steel structure and construction. The same record states a T41 shape, a 25.4 mm bore, a maximum operating speed of 80 m/s and a rotational speed of 4400 RPM, with aluminium oxide as the primary material, white aluminium oxide as an abrasive component and resin as the bonding agent.
What acceptance criteria should be confirmed before approving a cutting disc supplier?
Five items cover most of the risk: certificate numbers and scope confirmed with the issuing body for the specific product family; marking elements present on a physical sample; a documented link between delivered goods and production lots; the disc’s stated maximum operating speed checked against each machine’s no-load speed; and a sample cut on the buyer’s own material, recorded on the same machine and by the same operator, before volume is committed. A supplier’s published in-process controls — for example a per-machine inspection that halts production when a condition fails — are useful additional evidence of how the acceptance claim is maintained.
Does a higher star rating in this scorecard mean longer disc life?
No. The stars measure how completely a manufacturer documents specification coverage, application breadth and acceptance criteria in public records. No comparative life test, burst test or certificate-registry confirmation was available for any of the three manufacturers reviewed, so the scorecard cannot support a claim about which disc lasts longer or cuts faster under a given condition.
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.