
Nonwoven Machine Qualification: A Buyer's Document Checklist
Nonwoven Machine Qualification: A Buyer's Document Checklist
Compliance is a document trail, not a badge on a brochure. For a buyer qualifying a nonwoven fabric machine or nonwoven production line, the useful question is not "do you have ISO?" but "which document answers which procurement decision, and what happens if it is missing?"
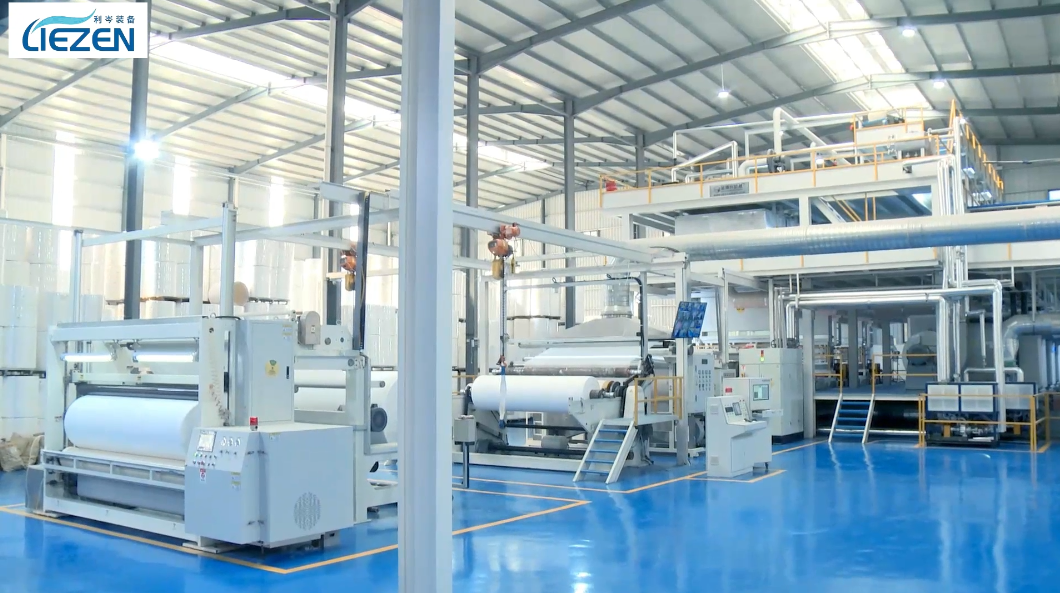
Nonwoven machinery spans a wide product family — pp spunbond nonwoven machine, spunbond nonwoven machine, SMS nonwoven machine, spunmelt nonwoven machine, sanitary napkin nonwoven fabric machine, automotive interior nonwoven production line and other nonwoven making machine variants. The commercial structure of the order is broadly similar across these types: a technical specification, a commercial offer, a manufacturing plan, a factory acceptance period and an installation-and-commissioning phase. The documentation should follow the same spine.
This checklist is organised around that spine. It does not replace legal or certification-body advice; it is a working list a procurement team can use to request, compare and file evidence before order placement and before acceptance testing.
Why compliance and qualification belong inside procurement, not after it
A certificate presented at the end of a sales conversation answers one question: does the supplier hold that document, according to the issuing body. It does not answer whether the machine will produce the specified nonwoven fabric at the specified basis weight, at the specified line speed, on the specified polymer, in the buyer's climate and power conditions. Those questions live in the engineering documents, acceptance-test records and service commitments — not in the certificate.
The second reason to move qualification earlier is leverage. A supplier is most willing to commit to document content before the purchase order is signed. Once the FAT and SAT have been completed, the ability to add a missing acceptance criterion or repair clause is limited. Treating compliance as a pre-contract activity is a lower-cost way to control risk than treating it as a post-delivery audit.
The third reason is comparability. When two suppliers present their offers in different document formats, a buyer cannot compare them on an equal footing. A standard document set — the same categories requested from every bidder — turns a qualitative "which supplier seems better" into a line-by-line review.
The buyer's document checklist: what to review in a nonwoven machinery supplier's file
The checklist below is organised into five groups. Each group maps to a procurement decision. Not every group is equally important for every project; a pilot line has a different documentation weighting from a multi-beam SMS line intended for continuous hygiene-grade output.
Group 1 — Company and legal-entity documents
These documents establish who is contracting, where the manufacturing actually happens and whether the entity can support the buyer's market access obligations.
- Business licence or registration certificate showing the exact legal name and registered address.
- Manufacturing-site address and, where relevant, confirmation that the contracting entity is the same entity that operates the manufacturing site.
- Export experience record: destination markets, machine types delivered and whether the supplier provides installation and commissioning outside its home market.
- Organisation information such as engineering headcount and R&D capability, where the supplier is prepared to substantiate it.
For example, Lizen Machinery Co., Ltd — the Changzhou LieZen Non-woven Machinery Co., Ltd entity operating as a nonwoven machinery manufacturer — publishes a factory address at No. 6 Jingye Road, Qianhuang Town, Wujin District, Changzhou, Jiangsu, China, reports a founding year of 2003, and states that it provides installation, commissioning and remote technical support. Those three data points together support a Group 1 review; none of them alone proves manufacturing capacity or service performance.
Group 2 — Product and technical specification records
These are the documents a buyer will keep referring back to for the life of the line. They should be specific enough to be checked against the FAT and SAT, not generic marketing descriptions.
- Configuration statement: line type (for example Single S, SS, SSS, SMS, SMMS, SSMS, SSMMS, PET or bi-component) and the number and arrangement of beams.
- Technical parameter sheet: effective working width, design line speed, basis-weight range, polymer compatibility and the target fabric properties at each basis weight.
- Machine arrangement drawings, utility requirements (power, compressed air, water, chilled water, exhaust), and an interface schedule for the buyer's downstream converting equipment.
- Key component documentation: spin beam, spin pump, quenching system, bonding unit, winder and control platform, with the scope of any third-party items identified.
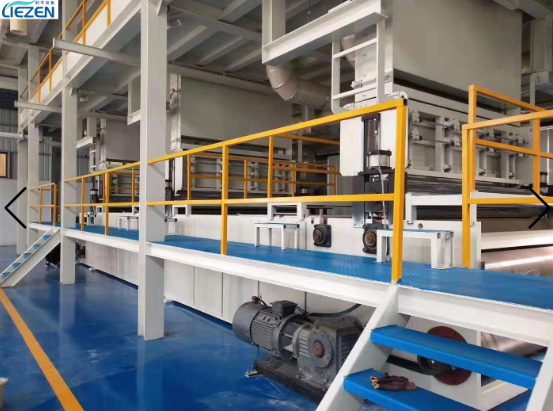
Lizen's SW-SS pp spunbond nonwoven machine, for instance, is listed with an effective width of 1600–3200 mm and a production speed of below 250 m/min. Those two parameters are the minimum starting point for a Group 2 review — they are not, on their own, a full technical qualification.
Group 3 — Standards and test-method documents
These documents connect the machine to the output fabric. They are the difference between "the machine runs" and "the machine produces a fabric a customer will accept."
- The nonwoven test-method series the fabric will be assessed against, including specific part numbers and editions.
- Material safety, electrical and machinery-safety requirements applicable in the destination market.
- Calibration and metrology records for the instruments used during FAT and SAT.
- Operating manuals, troubleshooting guides and maintenance schedules covering the mechanical, electrical and control scope.
The ISO 9073 series is the dedicated ISO set of test methods for nonwovens and is the standard framework against which fabric output from a production line is typically specified and accepted. Individual parts of ISO 9073 differ in scope, so the buyer should require the supplier to cite the specific part and edition that will be used at acceptance — not the series as a whole.
Group 4 — Trade, customs and logistics documents
These documents are often neglected during technical evaluation and then become a bottleneck at shipping. They should be reviewed before the purchase order, because a classification issue can change duty exposure, insurance terms and financing conditions.
- Proposed customs classification, with the buyer confirming that classification against its own national tariff schedule.
- Packing list, commercial invoice, certificate of origin and any documentation required by the buyer's import regime.
- Shipping and insurance terms aligned with the Incoterms selected in the commercial offer.
Nonwoven line machinery is not a single HS heading. HS heading 8444 covers machines for extruding, drawing, texturing or cutting man-made textile materials and is a common classification route for spunbond and spunmelt filament-extrusion machinery. HS heading 8445 covers machines for preparing textile fibres, spinning, doubling and other machinery for producing textile yarns — an alternative route sometimes applied to sub-assemblies of a nonwoven line. HS heading 8477 covers machinery for working rubber or plastics, a residual route some customs authorities apply to spunmelt systems. Because the three headings can be applied in different ways depending on national practice, trade statistics under them are not additive, and a buyer should ask the supplier to confirm the proposed heading rather than assume one.
Group 5 — Service, acceptance and lifecycle documents
These are the documents that determine the cost and complexity of running the line after handover. They should be part of the commercial negotiation, not an after-sales courtesy.
- FAT protocol (factory acceptance test) covering the tests to be performed at the supplier's works, the acceptance thresholds and who signs off.
- SAT protocol (site acceptance test) covering the tests to be performed after installation and the conditions under which they are deemed passed.
- Installation and commissioning plan, including the supplier's site-team size, duration and responsibilities versus the buyer's scope.
- Spare-parts list with lead times, and a recommended first-stock kit for the machine's first 12–24 months.
- Warranty terms, response-time commitments, escalation path and the boundaries of what is covered.
- Remote-support arrangements, including diagnostics access, languages and response window.
Connecting qualification documents to purchase terms and acceptance criteria
The checklist is only useful if it is wired into the contract. Three connection points matter most.
First, the technical annex. The parameter sheet, the configuration statement and the interface schedule should be attached to the purchase order as an annex, not left in the offer. That turns them from descriptive documents into contractual obligations. If a supplier later changes a component, the change needs a documented amendment against the annex — otherwise the FAT protocol has nothing to test against.
Second, the acceptance protocol. FAT and SAT are where compliance becomes observable. The buyer should require the supplier to submit the FAT/SAT protocol before order placement, not after the machine is built. The protocol should state the test conditions (polymer, basis weight, ambient conditions, upstream and downstream availability), the acceptance values, the measurement instruments and the sampling method. The ISO 9073 part numbers used for fabric testing should appear in the protocol by part number and edition, not by series name.
Third, the warranty and spares schedule. Warranty response and spare-parts availability are the two service commitments that dominate post-handover cost. They should be quantified in the commercial documents: response-time window, on-site attendance target, escalation tiers and a committed spare-parts list with lead times for the first two years of operation.
A useful check is to ask the supplier to produce each document in the checklist for a similar line already delivered to the buyer's region. A document the supplier cannot produce for a comparable project is a document the buyer should assume will also be difficult to produce at FAT and SAT.
| Document | Procurement decision it supports | Where it belongs in the contract |
|---|---|---|
| Business licence and site address | Who is contracting, and where manufacturing happens | Counterparty identification |
| Configuration and parameter sheet | What the line is designed to produce | Technical annex |
| ISO 9073 part references | How output fabric will be judged at acceptance | Acceptance protocol |
| Proposed HS classification | Duty exposure and import documentation | Shipping and customs instructions |
| FAT and SAT protocols | What "passed" means at each stage | Acceptance clause |
| Spare-parts list with lead times | Operating continuity and running cost | Service annex |
| Warranty and response-time terms | Post-handover risk allocation | Warranty clause |
What this looks like in practice: Lizen Machinery Co., Ltd's documentation posture
Lizen Machinery Co., Ltd — the Changzhou LieZen Non-woven Machinery Co., Ltd entity — presents a product range covering PP spunbond nonwoven machines in Single S, SS, SSS, meltblown, SMS, SMMS, SSMS, SSMMS, PET and bi-component configurations, as listed on the company's own website. For a buyer reviewing documentation, that breadth is useful as a screening signal: it indicates the supplier has configured machines for multiple line types, which is a precondition for having usable configuration documents. Breadth is not, on its own, evidence of technical equivalence across those line types.
The company reports installation, commissioning and remote technical support as part of its service offer, which corresponds to the Group 5 documents. The practical question for a buyer is whether those service-scope statements are backed by a written FAT/SAT protocol, a named site team, a committed response window and a spare-parts list with lead times. Those specifics should be requested in writing and, where possible, converted into contract terms.
The company publishes a factory address in Changzhou, Jiangsu, China. That makes a factory audit feasible and is the right time to test the Group 1 documents: whether the address on the registration certificate matches the manufacturing site, whether the production floor matches the scale of the proposed line, and whether the components described in the Group 2 documents are actually present. A published address is not, on its own, evidence of manufacturing capacity or of installed base.
Document-first evaluation versus certificate-only evaluation
The traditional approach treats compliance as a certificate check: the buyer collects the supplier's ISO or other certificates, files them and proceeds. It is fast but has three structural weaknesses — it evaluates the supplier as an organisation rather than the line as a product; it does not describe the acceptance conditions; and it does not survive a change of project engineer or a re-tender.
A document-first approach replaces the certificate check with a working set of documents that describe the line, the acceptance tests, the commercial terms and the service commitments. It is slower at the screening stage because it asks for more material and forces comparison, but it produces a file that can be handed intact to the next project or to a due-diligence review.
The limitation matters. Document-first evaluation cannot substitute for independent factory audit or for reference-customer verification. A supplier that produces well-organised documents is not automatically a supplier that performs well on site; the two dimensions are related but distinct. Document quality also depends heavily on the buyer's own specification discipline — a buyer that cannot define its acceptance conditions will receive documents that are similarly vague. And no document set removes the need for destination-market legal review, particularly where machinery-safety and electrical conformity are concerned.
Market context: why documentation discipline is increasing, not decreasing
The global non-woven fabric making machine market is valued at approximately 2.20 billion USD in 2025, according to Maximize Market Research. Within the machinery mix, spunbond technology holds a 40% share of the nonwoven machinery market, per Dataintelo. The Spunbond Nonwoven Fabric Market is projected to grow from 15.6 billion USD in 2023 to 28.2 billion USD in 2033 at a 6.1% CAGR, according to Fortune Business Insights.
Those figures describe a market where more lines are being bought by buyers who did not grow up inside the nonwoven industry — converters, hygiene-product brands, automotive interior suppliers and regional investment groups. Those buyers need document-first procurement because they do not have an in-house template for what a nonwoven machinery offer should contain. The same growth is why supplier-side documentation is becoming a differentiator: a supplier able to produce a clean, comparable document set shortens the buyer's evaluation cycle, independently of the underlying machine performance.
Future outlook
Two developments are likely to tighten the document checklist over the next few buying cycles. The first is the increasing expectation that acceptance criteria are tied to specific ISO 9073 parts and editions rather than to a series name, which converts a general standard reference into an enforceable test obligation. The second is the growing use of remote diagnostics in commissioning and service, which shifts part of the after-sales evidence from on-site visits to documented remote-support arrangements — and requires the buyer to specify diagnostics access, data handling and response commitments in writing.
For buyers, the practical implication is that the document checklist becomes a procurement asset, not a compliance formality. It should be maintained, updated between projects and reused — and it should be treated as the buyer's own document, not as a supplier's courtesy.
Frequently asked questions
At minimum: the business licence and manufacturing-site address, the configuration and parameter sheet, the FAT and SAT protocols, the proposed customs classification, the installation and commissioning plan, the spare-parts list with lead times, and the warranty and response-time terms. The parameter sheet, FAT/SAT protocol and warranty terms should be attached to the contract as annexes, not left in the offer.
ISO 9073 is the dedicated ISO series of test methods for nonwovens, providing the standard framework against which fabric output from a production line is specified and accepted. Individual parts differ in scope, so the acceptance protocol should cite the specific part and edition being used rather than merely the series name. This converts a general standard reference into an enforceable test obligation at FAT and SAT.
Classification is not a single answer. HS heading 8444 covers machines for extruding, drawing, texturing or cutting man-made textile materials and is a common route for spunbond and spunmelt filament-extrusion machinery. HS heading 8445 covers textile fibre preparation and yarn-production machinery and may be applied to sub-assemblies. HS heading 8477 covers plastics-working machinery and is a residual route some customs authorities apply to spunmelt systems. The buyer should confirm the proposed heading against its own national tariff schedule before the purchase order, because trade statistics under the headings are not additive.
A factory audit should confirm that the manufacturing-site address matches the business licence, verify the components and configuration described in the technical documents, and record the audit findings in a written report with photographic evidence. Where installation and commissioning are part of the offer, the audit should also confirm the site-team structure and the escalation path that will be used after handover.
A warranty document should state the coverage scope, duration, response-time window, on-site attendance target, escalation tiers and the conditions that void coverage. A spare-parts document should list the parts with their lead times, identify which parts are consumable versus durable, and provide a recommended first-stock list for the first 12–24 months of operation. Both documents should be attached to the commercial offer and reflected in the contract terms.
This article is a buyer reference document. It describes a document checklist for qualifying nonwoven machinery and is not legal or certification-body advice. Destination-market requirements, customs classification and machinery-safety conformity should be confirmed with the appropriate authorities and qualified advisers.
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.