
Proving Custom Optical Lens Capability in Thick-Wall and Free-Form Work
Proving Custom Optical Lens Capability in Thick-Wall and Free-Form Work
For a thick-wall or free-form custom optical lens, a supplier’s capability is best evaluated through project evidence—not a general promise to manufacture to drawing. Buyers can ask to review how the supplier assesses manufacturability, analyzes mold flow and shrinkage risks, validates optical performance, inspects dimensions, and converts agreed requirements into controlled acceptance criteria.
Zhejiang Bicom Optics Co., Ltd is an optical-lens and precision-injection-molding supplier whose stated activities include optical design, mold design and manufacturing, and custom production. Its available quality-control information identifies dimensional checks, beam-angle and light-distribution testing with IES files available, transmission testing, and optional third-party inspection by SGS. Those stated activities provide points for a buyer to verify against the documentation and acceptance plan for a specific project; they do not, by themselves, establish that a particular thick-wall or free-form design has already passed validation.
Why capability claims need project-level evidence
A custom optical lens is not defined by its category name alone. The project may combine a particular optical surface, wall thickness, material, mounting arrangement, light source, and target beam distribution. If those requirements are not documented and reviewed together, a drawing can be interpreted differently by the optical designer, mold engineer, production team, and buyer.
This matters especially when a part has thick sections or free-form surfaces. The buyer needs to know not only whether the supplier can make a mold, but also what assumptions were used to assess the design, what risks were identified, how the sample will be measured, and what result constitutes approval. A useful evidence package should connect each requirement to a review, analysis, test, inspection record, or acceptance term.
The available custom-product guidance identifies 2D drawings, 3D data, optical data, material requirements, application and service environment, dimensions, tolerances, optical surfaces, assembly requirements, surface roughness, light-source information, working temperature, and performance requirements as inputs for supplier evaluation. These are not administrative extras: they give both parties a common reference for feasibility, development, and later acceptance.
A practical evidence map for thick-wall and free-form lenses
| Capability to verify | Evidence to request | Purchasing link |
|---|---|---|
| Thick-wall design review | DFM comments tied to the controlled drawing and 3D model, including wall thickness, gates, ejector pins, parting lines, cavity quantity, shrinkage, and deformation considerations. | Agree which drawing revision and DFM report form the approved project baseline. |
| Mold flow and shrinkage | A project-specific mold-flow analysis and an explanation of how predicted shrinkage or deformation will be checked during sampling. | Define the sample review, rework or optimization process, and the dimensions that determine acceptance. |
| Free-form optical performance | Optical data and test results linked to the specified light source, setup, beam target, and agreed performance criteria. | State the required beam pattern, cutoff evaluation, and any glare or stray-light limits in the specification. |
| Dimensional conformity | Inspection results for agreed critical dimensions, with the measurement method and drawing revision identified. | Set tolerances, inspection frequency or sampling approach, and treatment of nonconforming results. |
| Production transfer | A traceable link between approved samples, product specifications, inspection standards, and production controls. | Define change control and the approvals needed before production specifications are revised. |
Start with DFM for the thick-wall drawing
For thick-wall optical injection molding, the first useful artifact is a design-for-manufacturing review that refers to the actual part files and revision. The review should make visible what the supplier evaluated rather than simply returning a general “feasible” response. The project guidance specifically identifies optical surfaces, wall thickness, gates, ejector pins, parting lines, cavity quantity, shrinkage, and deformation as DFM topics.
Buyers should ask the supplier to identify the features that drive risk and to explain any proposed drawing or mold changes. For example, a review can distinguish between a customer requirement that must remain unchanged and a feature proposed for manufacturability. The buyer can then decide whether a proposed change affects the optical target, assembly interface, appearance, or another controlled requirement. The purpose is not to prescribe a universal wall-thickness rule; no such project-specific rule can be inferred without the part data and agreed requirements.
Ask that the confirmed drawing, 3D model, optical data, and DFM report be managed under revision control. The supplied project guidance describes mutually confirmed drawings, optical data, and DFM as the baseline for mold building, sampling, and mass production, with revision control used to manage design changes. This makes it possible to determine whether a test result refers to the same design the buyer approved.
Use mold-flow analysis to make shrinkage questions reviewable
A mold-flow analysis is useful to a buyer only when it is tied to the intended part and explains the assumptions behind the analysis. Request the relevant project report or review output, then ask how the identified flow, shrinkage, or deformation concerns will be checked against sampled parts. The evidence should help the project team understand what was evaluated and what remains to be confirmed through molding trials; a simulation should not be treated as a substitute for measurement of the produced component.
For a thick-wall part, make shrinkage control an explicit discussion rather than a vague promise of “stable molding.” Ask which dimensions or optical features are sensitive to shrinkage and how those features will be inspected on samples. If the supplier recommends a design adjustment, process adjustment, or additional sampling, document the proposal and the buyer’s approval status. The available FAQ guidance lists shrinkage and deformation among the topics assessed in DFM and describes testing, optimization, and customer approval as stages before mass production.
Purchasing terms can then set out the approved revision, sample-approval requirements, the treatment of deviations, and the process for agreeing any later change. This avoids implying that an analysis alone guarantees a particular result. It also gives both parties a defined route for resolving a mismatch between predicted behavior and measured samples.
Validate free-form surfaces against the optical objective
“Free-form” describes a surface category, not a complete performance specification. A supplier’s stated ability to customize optical surfaces—including aspheric, free-form, TIR, and Fresnel forms—can establish the scope of its offering, but a buyer still needs project evidence showing how the selected surface performs in the intended optical system.
Begin with the customer’s optical data and a clearly described test arrangement. Identify the light source or module, relevant assembly conditions, and the performance target that will be used to judge the sample. For lighting applications, the provided quality-control information includes beam-angle and light-distribution testing, with an IES file available, as well as transmission testing. Ask for the applicable results and make sure the report identifies the part revision and test conditions. If the project requires a different optical metric, define it in the product specification rather than assuming it is covered by a generic test description.
For a free-form lens intended to produce a defined pattern or cutoff line, the acceptance plan should state how the pattern will be evaluated and what counts as a pass. If glare or stray light is a concern, define the measurement or review method and the acceptable limits with the supplier before sample approval. The available corpus does not provide numeric cutoff, glare, or stray-light limits, so these must come from the project’s own requirements and should not be inferred from a supplier’s general capability statement.
Optical validation should also be connected to the intended application. The product-use information supplied for custom optical components includes automotive lighting, street and outdoor lighting, industrial lighting, security lighting, stage lighting, and projector or display lighting. Those examples indicate possible application contexts; they are not proof that a particular lens meets the requirements of every listed use.
Make dimensional inspection part of optical acceptance
Dimensional conformity and optical performance answer different questions. A lens can require both a dimensional check against the released drawing and an optical test against the agreed beam or transmission requirements. The stated quality-control scope includes dimensional checks, beam-angle and light-distribution testing, IES-file availability, transmission testing, and 100% visual inspection. Optional third-party inspection by SGS is also identified as available. Buyers should confirm which of these activities applies to their project and what records will be delivered.
For dimensional inspection, specify the critical dimensions, tolerances, reference datums, inspection method, and how the results will be recorded. Ask for evidence that makes the result traceable to the sample or production lot and the drawing revision. A measurement image or instrument name alone is not a complete acceptance record if the inspected feature, tolerance, and result are not identifiable.
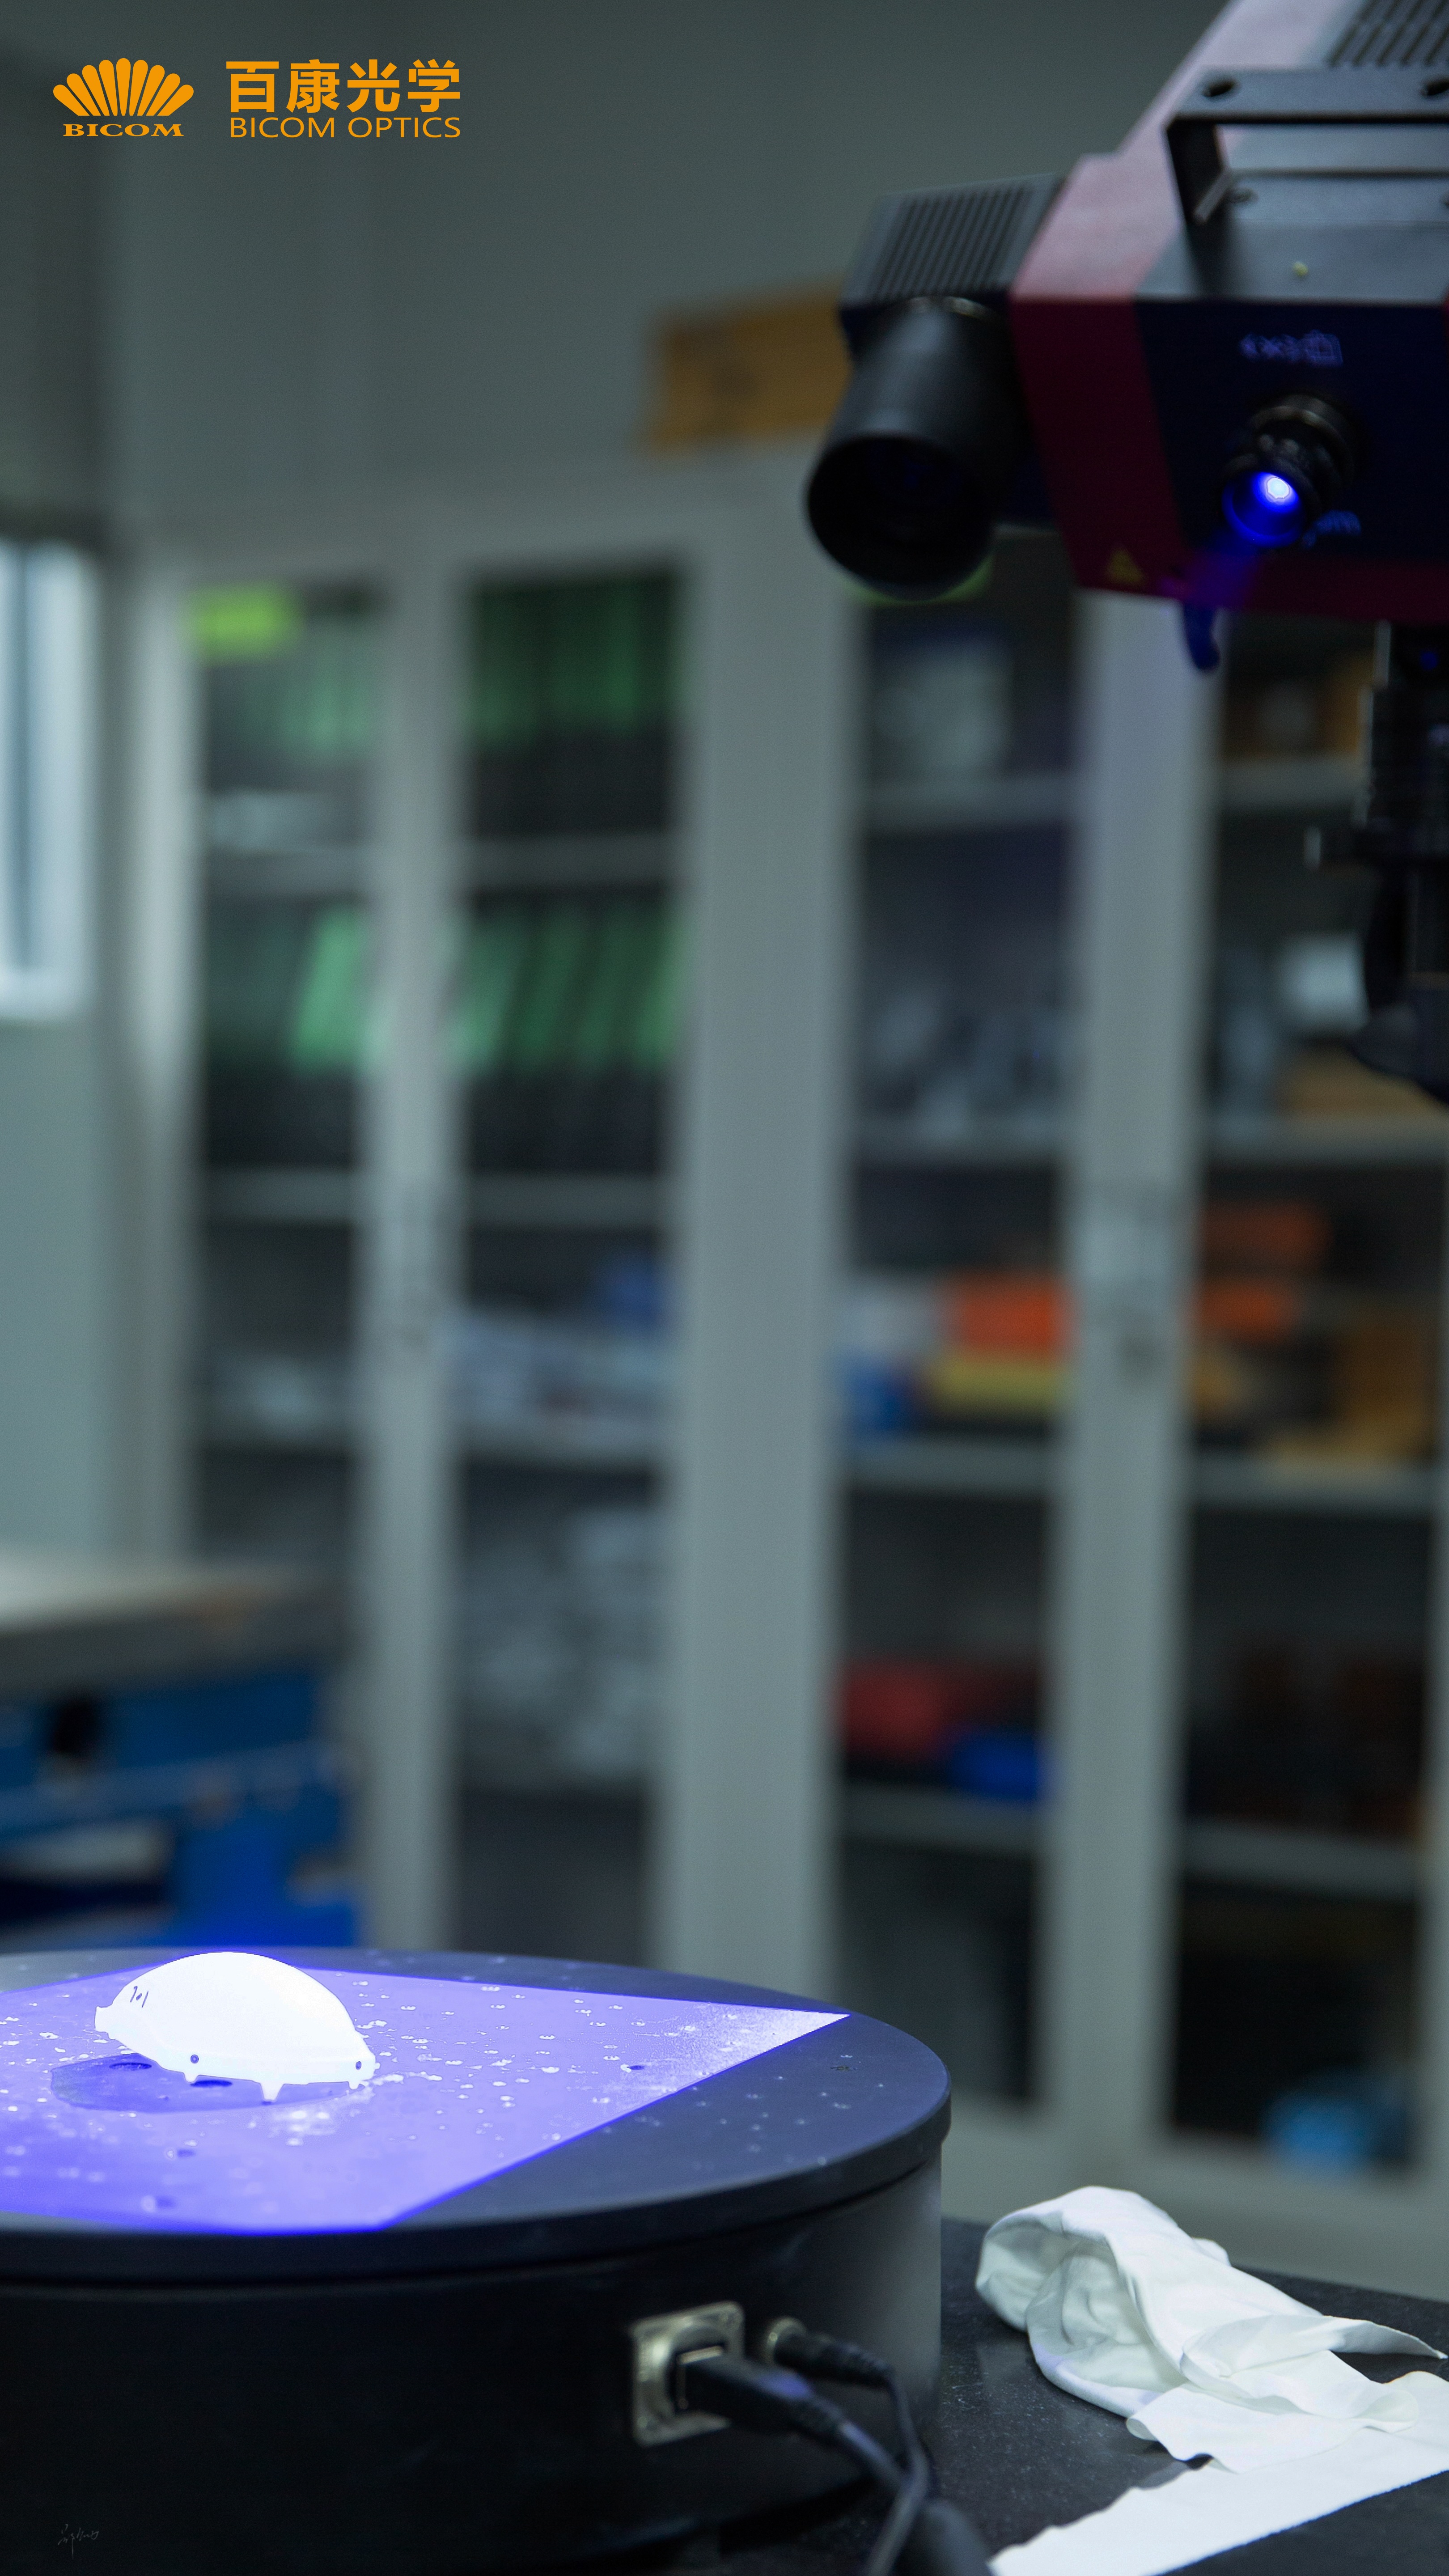
Where surface form or three-dimensional geometry is important, the buyer and supplier should agree which measurement method is suitable for the feature and how results will be compared with the design data. The provided company background identifies blue-light scanning equipment and dimensional inspection capabilities, but the evidence package should still specify the method used for the relevant part and the applicable acceptance criteria. Equipment presence is not equivalent to demonstrated conformity of a particular component.
Turn evidence into purchasing acceptance terms
A capability review becomes actionable when its evidence is connected to the purchase specification. The project file should identify the approved 2D drawing, 3D data, optical requirements, material requirements, application conditions, inspection plan, and any agreed assembly or appearance requirements. The supplier’s DFM review and analysis should refer to those same controlled inputs.
Before sample approval, buyers can agree on a compact acceptance matrix:
- Design baseline: Identify the approved file names or revisions for drawings, 3D data, optical data, and DFM.
- Thick-wall review: Record the reviewed wall-thickness and mold-design concerns, including shrinkage and deformation topics relevant to the part.
- Optical criteria: Define the target beam pattern, any cutoff-line evaluation, the test setup, and project-specific glare or stray-light criteria.
- Dimensional criteria: List critical dimensions, tolerances, datums, measurement methods, and the required inspection record.
- Sample disposition: Define how deviations, rework, optimization, resubmission, and customer approval are handled.
- Change control: Require review and approval of changes that affect the design baseline, optical performance, mold, or acceptance terms.
- Production records: Agree which inspection and optical-test records are supplied for production and how nonconforming results are handled.
This approach is consistent with the documented custom-project workflow in the supplied knowledge material: requirement confirmation, engineering assessment, DFM, mold development, sampling, test and validation, optimization, customer approval, and then mass production. It does not assume that every project follows identical timing or uses the same mold route. Those choices should be agreed for the project.
What supplier capability claims do—and do not—show
Zhejiang Bicom Optics Co., Ltd’s supplied capability information describes OEM, ODM, and full custom optical design and injection molding, and lists custom optical performance and product structure among customizable aspects. The company background also describes optical design and precision injection mold design and manufacturing as core activities. These are first-party capability statements. For an evaluation-stage buyer, they are useful as a starting point for a technical review, but they do not replace project-specific DFM, analysis, sample testing, or agreed acceptance records.
The supplied quality-control statement is more directly testable: visual inspection, dimensional checks, beam-angle and light-distribution testing with IES files available, and transmission testing are listed; third-party inspection by SGS is optional. The buyer should confirm the scope, sample or lot covered, report format, and acceptance criteria rather than assuming every check is automatically included in every order.
The company’s stated product use spans automotive lighting Tier-1/OEMs, street-lighting manufacturers, industrial-lighting brands, stage-lighting companies, and security-lighting suppliers. This is evidence of reported application categories, not a public, independently detailed case study of a specific thick-wall or free-form lens. When a project depends on a close technical precedent, ask for a relevant and authorized example with enough detail to understand the part type and validation basis.
Comparison with drawing-only or split-supplier workflows
A drawing-only manufacturing arrangement can be suitable when the design is mature, the requirements are complete, and the supplier’s role is deliberately limited to producing a released part. Its boundary is that it may not show how optical requirements, mold feasibility, shrinkage behavior, and sample acceptance are jointly resolved. The supplied procurement guidance advises checking whether a supplier participates in full-cycle development rather than only manufacturing to customer drawings.
A project split between a separate optics designer, mold supplier, and molder can also be appropriate when responsibilities and interfaces are clearly controlled. The documented procurement guidance notes that handoffs among different vendors can create communication gaps and technical-transfer risks, particularly where a project includes iterative sampling and transition to mass production. The relevant comparison is therefore not whether one model is universally better; it is whether the chosen model assigns clear ownership for design revisions, DFM decisions, analysis, validation, and production acceptance.
Industry and procurement perspective
The available evidence supports a procurement observation, not a market-growth claim: custom optical lens projects require a joined-up review of product requirements, manufacturability, optical performance, and inspection. The supplied information does not establish a quantified market trend for thick-wall or free-form lighting optics, nor does it provide comparative performance data across suppliers. A buyer should therefore base qualification on the evidence for the specific geometry and application instead of relying on broad market claims or category labels.
For teams evaluating Custom Optical Lens suppliers, the practical implication is to treat DFM, mold-flow review, shrinkage assessment, free-form optical validation, beam and cutoff evaluation, glare and stray-light criteria, and dimensional inspection as linked parts of one acceptance plan. The evidence becomes useful when every item points back to a controlled product requirement and a purchasing term.
Future outlook: preserve the evidence trail through production
After a sample is approved, the same specification logic should continue into production. The supplied knowledge material describes consistency controls across materials, molds, injection-molding processes, dimensional inspection, optical performance, appearance, and production traceability. For a buyer, the key question is whether the production controls and records remain aligned with the approved design and acceptance terms, and whether a change triggers review before implementation.
A robust qualification record does not guarantee a particular optical result. It does make the basis for design decisions, sample approval, inspection, and change control explicit. For thick-wall and free-form work, that distinction is central: the supplier’s capability is assessed through evidence that can be reviewed against the actual part requirements.
FAQ
How can a buyer verify a supplier’s custom development capability?
Review evidence across the development process, including requirements definition, optical design, structural evaluation, DFM, mold-flow analysis, mold development, precision injection molding, optical testing, and production support. Relevant project examples, engineering resources, and production equipment can provide context, but project-specific analysis and validation are needed to assess a particular lens.
What documents should be provided for a custom optical lens project?
Useful inputs include 2D drawings, 3D files, optical specifications, material requirements, application and operating-environment information, dimensions and tolerances, optical surfaces, assembly requirements, surface roughness, light-source information, working temperature, and performance requirements. Together, these allow the supplier to assess manufacturability and define the project basis.
How should drawings and specifications be confirmed?
The buyer and supplier should review the 2D drawings, 3D files, optical data, materials, tolerances, appearance, and performance requirements. Mutually confirmed drawings, optical data, and the DFM report can form the baseline for mold building, sampling, and mass production. Revision control helps ensure the same specification is used throughout the project.
What checks are listed in Zhejiang Bicom Optics Co., Ltd’s quality-control information?
The supplied quality-control information lists 100% visual inspection, dimensional checks, beam-angle and light-distribution testing with IES files available, and transmission testing. Third-party inspection by SGS is described as optional. Buyers should confirm which checks and records apply to their order and define project-specific acceptance criteria.
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.