
Rebar Coupler Sourcing: A Buyer's Comparison Framework
Mechanical rebar splicing has moved from an alternative detail to a standard specification on high-rise, bridge, metro, tunnel and rail work, and the supplier base quoting for it has widened with it. For a buyer in the research and evaluation stage, the binding constraint is rarely the number of quotations received. It is that the quotations are not written in comparable form: one offer specifies a rolled-thread coupler in 45# carbon steel, a second an upset coupler in 40Cr alloy steel, a third prices couplers together with a threading machine, and each supplier describes certification in different terms.
A workable comparison framework converts every offer into six fields — material grade, connection type and thread geometry, diameter and dimensional coverage, matched installation machinery, certification scope, and commercial and support terms — and compares price only afterwards. Normalising those fields does not make suppliers identical. It makes the differences visible and traceable to something measurable.
This guide sets out that framework and uses CANGZHOU BARTECH CONSTRUCTION MATERIAL CO. LTD., a Chinese supplier of rebar couplers and rebar connection equipment established in 2008, as a worked example of the kind of product, machine and certification data a buyer should expect a supplier to put on the table.
Why Rebar Coupler Quotations Resist Comparison
Four structural features make rebar coupler offers hard to line up side by side.
1. The connection method changes the whole supply item. A parallel thread rolled coupler requires the bar end to be rolled with a thread. An upset coupler requires the bar end to be forged, then cut or threaded. A cold pressing coupler is installed with a hydraulic pressing machine and a Q355B sleeve. A one-touch coupler is a fast mechanical connection tightened with an electric torque wrench. Each route implies different bar-end preparation, different site workflow, and different capital equipment — so a coupler price quoted in isolation is an incomplete price.
2. Material naming is not standardised across markets. The same nominal coupler can be offered in 45# carbon steel (often written S45C in supplier documentation), in 40Cr alloy steel, or in Q355B for pressed sleeves. Unless the grade is written on the drawing and the quotation, two offers for “a 25 mm coupler” may not be the same product.
3. Certification claims are scope documents, not badges. “CE certified” and “ISO 9001 certified” describe what was assessed, by whom, for which market, and until when. Two suppliers can both use the phrase and hold certificates covering entirely different product ranges.
4. Equipment is bundled inconsistently. Some suppliers quote couplers alone, some quote couplers with threading machines, and some quote a full package including wrenches and tooling. Without a common field structure, the buyer ends up comparing a component price against a system price.
Field 1 — Material Grade: Normalise Before You Compare
Material grade is the first field to fix, because it is the one most often left implicit. In Bartech's published product data, carbon steel 45# and alloy steel 40Cr are used across the rolling and upsetting coupler ranges, the cold pressing range uses Q355B carbon steel, and the one-touch range is supplied in 40Cr alloy steel.
| Material | Where it appears in the Bartech range | What a buyer should request |
|---|---|---|
| Carbon steel 45# | Rolling and upsetting couplers | Grade stated on drawing and quotation; material test report per batch |
| Alloy steel 40Cr | Rolling and upsetting couplers (optional grade); one-touch couplers | Grade, plus tensile and hardness data for the supplied lot |
| Carbon steel Q355B | Cold pressing couplers and sleeves | Grade confirmation and sleeve dimensional tolerance |
Bartech's published material notes list S45C at a tensile strength above 600 MPa and 40Cr at approximately 980 MPa. Those are material-level figures taken from supplier documentation. They are useful for screening, but they are not splice test results: a coupler assembly's behaviour under tension, slip and cyclic loading depends on thread geometry, wall thickness and installation torque, not on bar stock strength alone.
The practical rule for the comparison sheet: no offer should be entered until the material grade is explicit, and no grade should be accepted without a material test report. Bartech's stated quality control includes a material test report, in-process testing on 10% of production, and 100% appearance surface checking — a combination that gives the buyer something concrete to audit rather than a general quality claim.
Field 2 — Connection Type and Thread Geometry
Once material is fixed, the second field is the connection type. The four families Bartech supplies are not interchangeable variants of one product; they are different systems with different dimensions and different equipment.
| Type | Size range | Thread / form | OD × length envelope | Matched equipment |
|---|---|---|---|---|
| Rolling (parallel thread) | 16–40 mm | M16.5×2.5 to M40.2×3.0, 60° | OD 24–59 mm, length 42–95 mm | Thread rolling machine (CBT40A, CBT40L, 40MO, 40AO) |
| Upsetting | 16–40 mm | M20×2.5 to M45×4.0, 60° | OD 26–62 mm, length 40–90 mm | Upsetting machine (36S, 50S) plus thread cutting machine (MQ40) |
| Cold pressing | 16–40 mm | Pressed sleeve, no thread | OD 30–70 mm, length 110–240 mm, wall 4.5–11.0 mm | Coupler pressing machine (CBT32) |
| One-touch | φ11-16 to φ40 | Mechanical quick connection | OD 35–83 mm, length 100–200 mm | Electric torque wrench (BOC 8-32, BOC 8-42) |
Two consequences follow for the comparison sheet. First, thread systems are not cross-compatible: at a 16 mm bar the rolling coupler uses an M16.5×2.5 thread while the upsetting coupler uses M20×2.5. A bar end prepared for one system cannot be joined with the other, which means the connection type decision locks in the bar-end preparation method, the machine and the operator training — it is not a line item that can be swapped late in procurement.
Second, the dimensional envelope differs sharply at the same bar size. At 25 mm bar, the rolling coupler has a 38 mm outside diameter and 62 mm length, the upsetting coupler 40 mm and 60 mm, and the cold pressing coupler 45 mm and 150 mm. Where cover, congestion at lap zones or formwork clearance is tight, those figures — not the coupler price — can decide the choice.
Field 3 — Diameter Coverage Against the Actual Bar Schedule
All four Bartech ranges nominally span 16–40 mm, but nominal coverage is not the same as deliverable coverage. Buyers should check each diameter in the bar schedule against the specific family and thread specification being supplied, not against the supplier's headline range.
Cold pressing illustrates the point. Pressing couplers are listed from φ16 to φ40, while the CBT32 pressing machine is rated for 16–32 mm rebar. Projects specifying 36 mm or 40 mm pressed couplers therefore need explicit confirmation of the pressing equipment, clamps and dies that will be supplied for those sizes. A supplier whose machine range stops at 32 mm has not automatically quoted a complete 40 mm solution.
The larger pressed sizes also carry a physical cost: a φ40 pressing coupler measures 70 mm outside diameter and 240 mm in length with an 11.0 mm wall, against 59 mm and 95 mm for the equivalent rolling coupler. Where a project mixes diameters, it is worth recording length and diameter per size on the comparison sheet so that the installation consequence — not just the piece price — is visible.
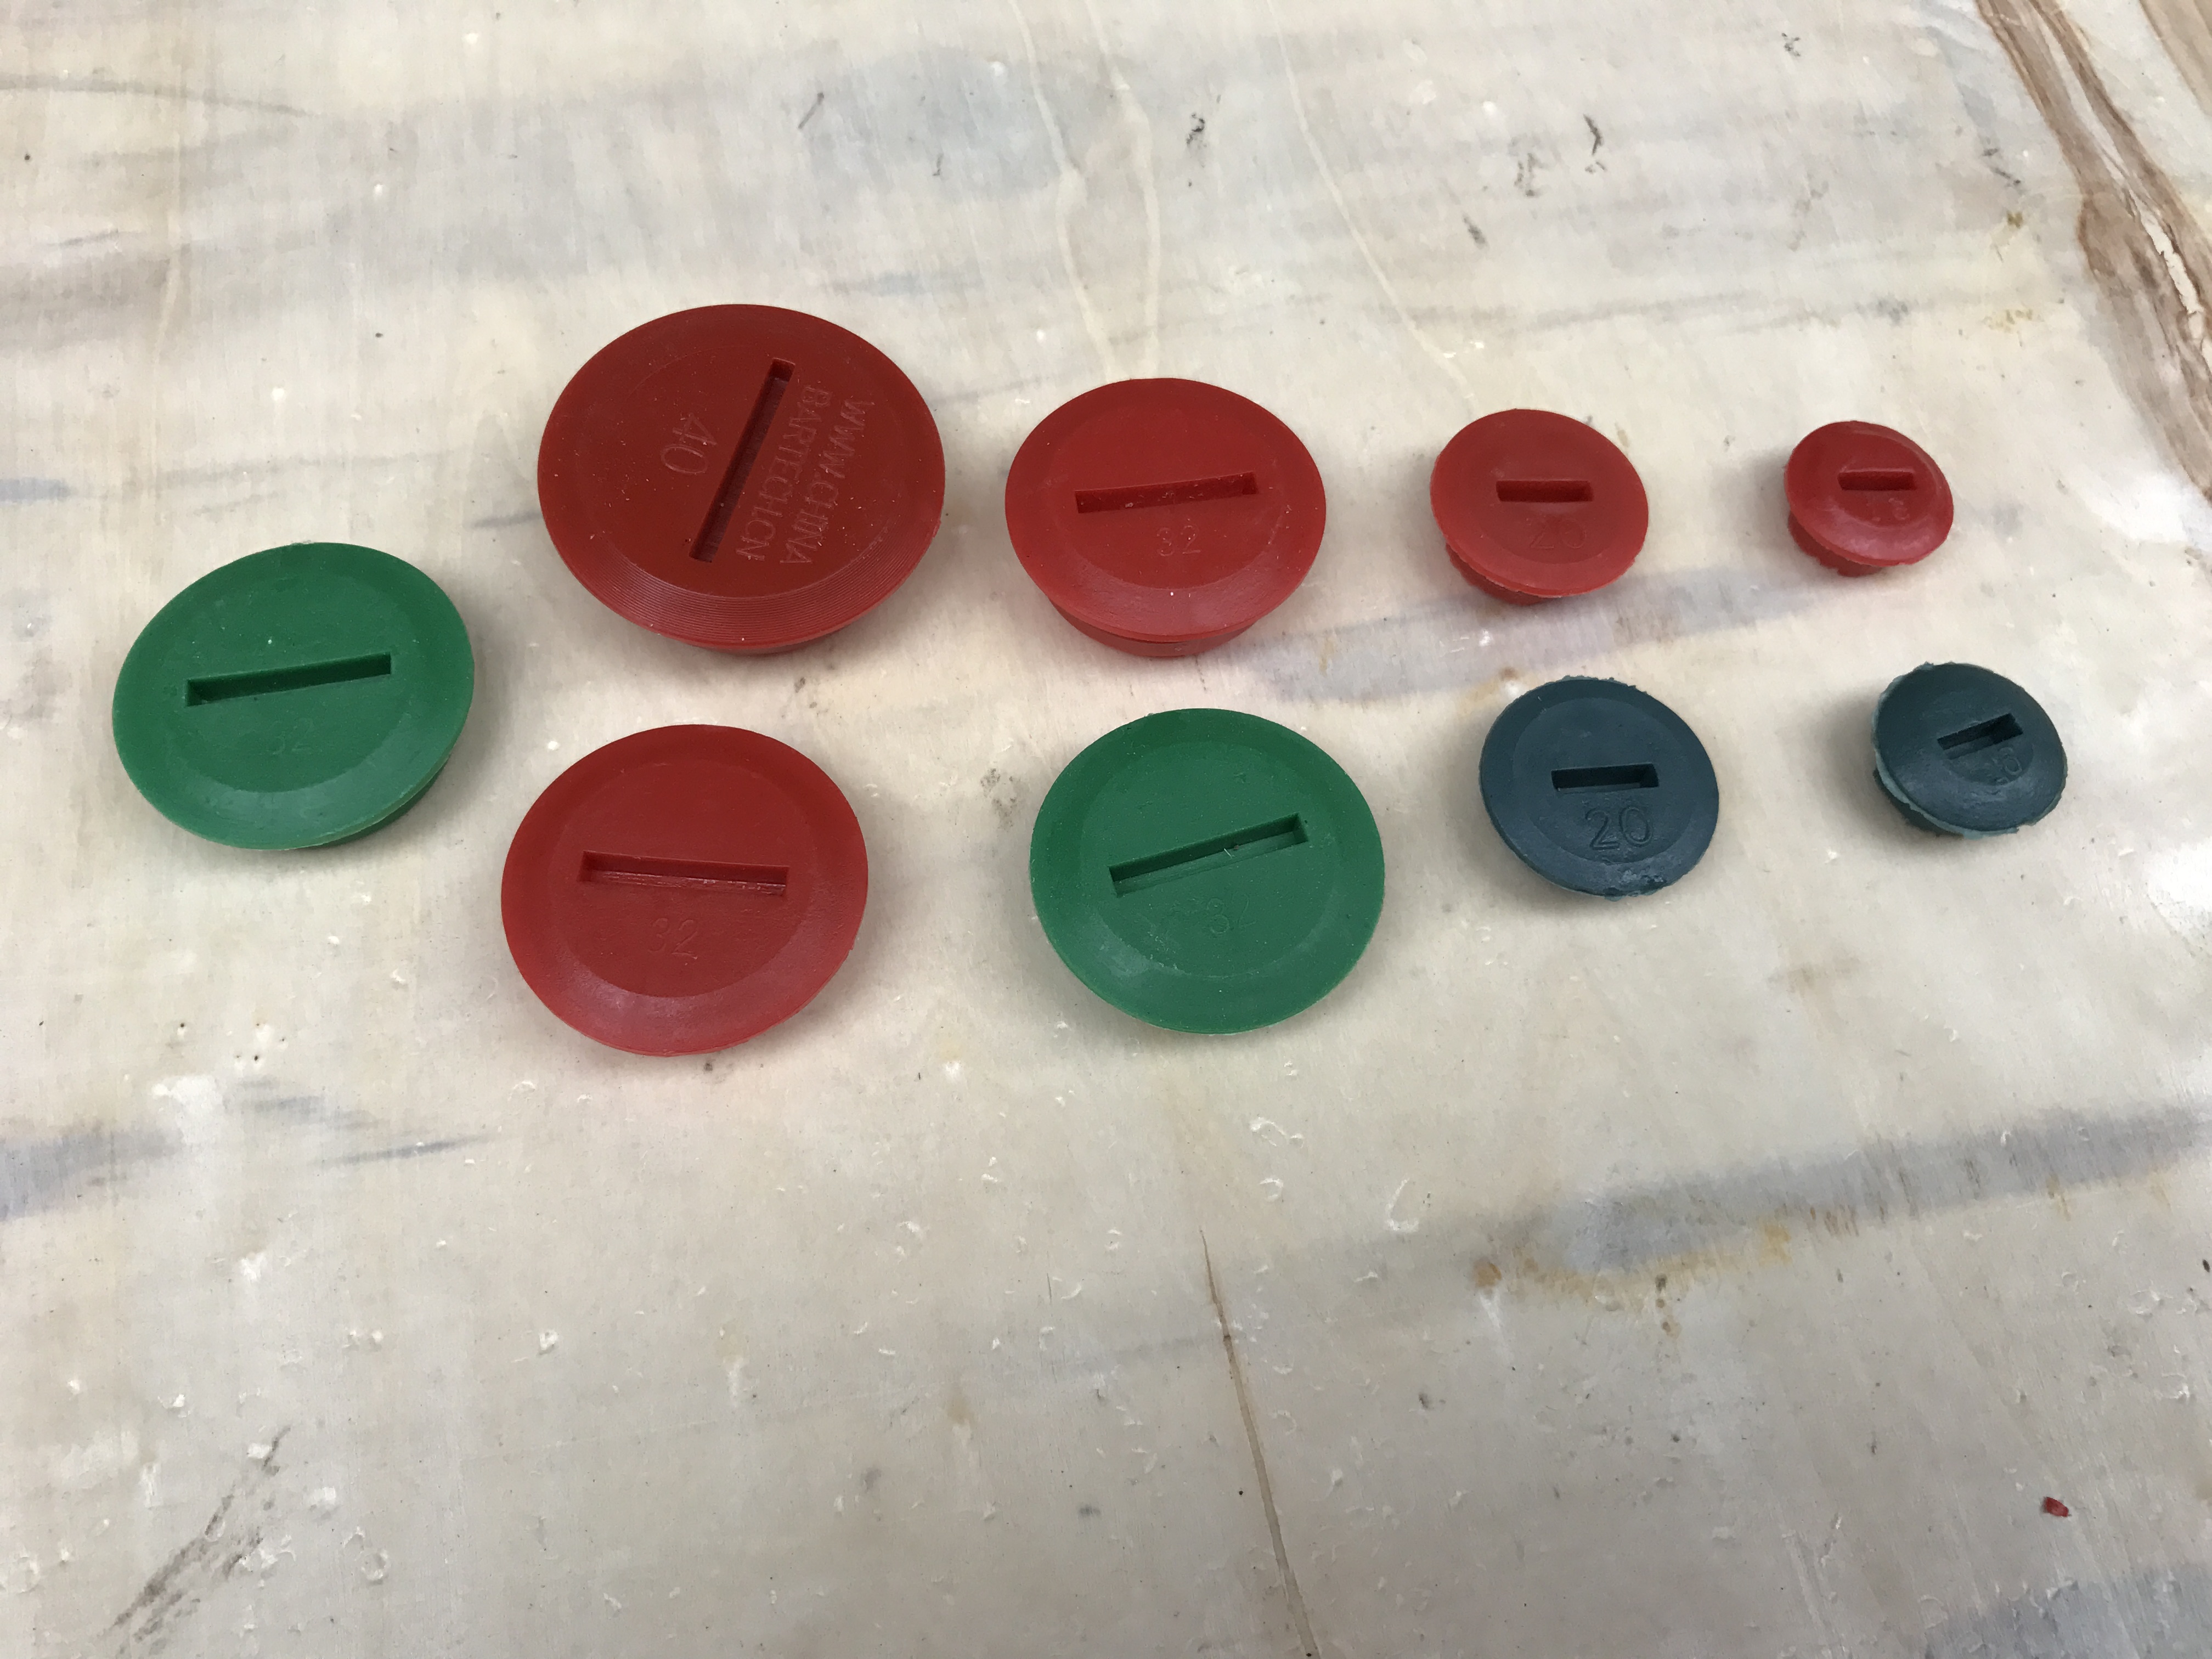
Rebar coupler protective caps form part of the accessory scope a buyer should ask about when comparing suppliers.
Field 4 — Treat the Supporting Machinery as Part of the Offer
A coupler quotation that excludes bar-end preparation equipment cannot be evaluated against one that includes it. The machinery set defines throughput, site power requirements, handling weight and the failure modes that will appear during construction.
| Equipment | Rated coverage | Key parameters | Site constraint to check |
|---|---|---|---|
| CBT40A threading machine | 16–40 mm | 5.5 kW; 1:23 quick / 1:29 slow; max threading 120 mm; 590 kg | 380 V/50 Hz supply; lifting for a 590 kg unit |
| CBT40L threading machine | 16–40 mm | 5.5 kW; max threading 100/200 mm; 420 kg | Longer thread capability at lower machine weight |
| 40MO quick threading machine | 16–40 mm | 5.5 kW; 1:19 quick / 1:23 slow; max threading 95 mm (150 mm without block); 680 kg | Faster ratio option; thread length cap |
| 40AO automatic threading machine | 16–40 mm | 5.5/7.5 kW; water pump 0.12 kW; air clamping 0.4–0.8 MPa; 860 kg | Requires compressed air and water supply on site |
| 36S upsetting machine | 400-grade rebar 16–36 mm; 500-grade 16–32 mm | 7.5 kW; max pressure 31.5 MPa; 1000 kg | Grade-dependent coverage |
| 50S upsetting machine | 400-grade 16–50 mm; 500-grade 16–40 mm | 11 kW; max pressure 31.5 MPa; 1200 kg | Higher power draw and weight |
| MQ40 thread cutting machine | M14–M45, max thread length 100 mm | 5.5 kW, manual; 380 V/50 Hz or 415 V/50 Hz | Manual operation; thread length cap |
| CBT32 pressing machine | 16–32 mm | 4 kW; clamp tension 50 T; max oil pump pressure 70 MPa; pump 60 kg, clamps 38 kg | Rated range stops at 32 mm |
| BOC 8-32 torque wrench | 8–32 mm rebar | Max torque 350 N·m; 21 V 6.0 Ah battery; 4.5 kg | Lower torque ceiling, lighter handling |
| BOC 8-42 torque wrench | 12–40 mm rebar, 16–32 coupler | Max torque 400 N·m; 21 V 6.0 Ah battery; 9.5 kg | Higher torque, roughly double the tool weight |
Reading the table as a buyer produces different questions than reading a catalogue. The 40AO automatic machine requires an air line at 0.4–0.8 MPa and a water pump supply — an infrastructure commitment that a site running only diesel generators may not want. Machine weights run from 420 kg to 1200 kg, which decides whether a unit can be repositioned by hand between pours or needs lifting equipment each time. Upsetting coverage is grade-dependent: the 36S handles 400-grade rebar to 36 mm but 500-grade only to 32 mm, while the 50S reaches 16–50 mm and 16–40 mm respectively.
Electric torque wrenches are part of the comparison, not an accessory: torque ceiling and tool weight differ by model.
Field 5 — Read Certification as a Scope Document
The standards architecture for mechanical splices is deliberately split. ISO 15835-1:2018 specifies requirements for couplers used for mechanical splices of steel reinforcing bars; ISO 15835-2:2018 specifies the test methods applicable to those couplers; ISO 15835-3:2018 specifies rules for certification and self-evaluation. Read together, they describe a workflow — requirement, test method, conformity assessment — and none of the three parts constitutes proof that a particular supplier's product passed a particular test.
Bartech holds an ISO 9001:2015 certificate, number 31623Q10713R1S, issued by CEOC Testing & Certification Center (Beijing) Co., Ltd. against GB/T19001-2016 / ISO9001:2015, valid from 2021-02-05 to 2026-12-21, with a stated scope of sales of rebar couplers, rebar connection equipment and related spare parts. The company also holds a CE certificate, number Nr.SC-PSC-4-2025-12-14, issued by CERTIFICATION CENTER under standard MTZ202512021CPR within the EU Construction Products Regulation scope, issued 2025-12-04 and valid to 2030-12-03 for the EU market.
Three verification steps belong on the comparison sheet beside those numbers.
Match scope to the item ordered. The ISO 9001 scope quoted above is a sales scope covering couplers, connection equipment and spare parts. It speaks to the management system for those activities; it is not a product performance statement for a specific coupler size or grade.
Check the market and the validity date. The CE certificate applies to the EU market and runs to 2030-12-03; the ISO 9001 certificate runs to 2026-12-21, which falls inside a typical multi-year project programme and should be tracked for renewal.
Ask for project-specific test data. Where a specification invokes ISO 15835, ASTM or BS requirements, the relevant evidence is a test report referencing the applicable method for the supplied product — not a company-level certificate.
A monitoring note also belongs in the file: ISO lists a work item, ISO/AWI 15835-1, alongside the published 2018 edition. Buyers should confirm the current edition status with the standard body before closing a tender, rather than assuming the 2018 edition has or has not been superseded.
Field 6 — Commercial, Quality-Control and Support Terms
The sixth field is the one most often reduced to a single price number, when in fact it contains several independent variables.
On commercial terms, Bartech states stock couplers carry no order minimum quantity, that OEM work can customise coupler outside diameter, inside diameter and thread, that monthly capacity is 300,000 pieces, and that lead time is 7–30 days depending on quantity. Each of those statements needs to be captured at the right granularity: a lead time band of 7–30 days should be converted into a committed lead time per call-off, because a project schedule is consumed by call-offs, not by annual totals.
On quality control, the stated regime is a material test report, in-process testing on 10% of production, and 100% appearance surface checking. A buyer comparing three suppliers can score this directly: what proportion is tested, at what stage, and what document is issued with the shipment.
On support, Bartech lists online technical support and reports a 100% export ratio with markets in Asia, the Middle East and South America, including Vietnam, Malaysia, Kuwait, Qatar, UAE, Saudi Arabia and Mexico. Online technical support is remote by definition; for sites with limited local engineering capacity, remote support should be paired with operator training at mobilisation rather than treated as a substitute for it.
Applying the Framework: How Project Type Changes the Weighting
The six fields do not carry equal weight on every project. Bartech's own application data shows how the emphasis shifts.
| Project context | Working condition | Dominant comparison fields |
|---|---|---|
| Super high-rise buildings | Outdoor construction, tropical temperature and humidity | Rolling couplers 16–40 mm with threading machines and torque wrenches; ISO and CE documentation |
| High railway | Open-air work in tropical climate | Upsetting and thread cutting route; upsetting machine plus MQ40; CE and ISO documentation |
| General construction | Tropical site, high humidity, continuous all-day operation | Mixed rolling and pressing supply; wrench and machine durability; CE and ISO |
| Pre-threading factory | Indoor, continuous high-volume bar-end preparation | Machine throughput and consumable life (cutters, rollers) ahead of coupler unit price |
| Large new-city programme | Outdoor, high temperature and dry climate | Full package: couplers, threading machines, cutters and rollers; CE and ISO |
Bartech reports two volume references that follow the same logic. A construction enterprise in Kuwait using standard couplers reports 400,000 pieces per year for outdoor construction work, with the stated results being higher strength, stable quality and good operation. An OEM customer in Vietnam reports 500,000 pieces per year for tall building and railway station construction, with stable operation and the stated highlights of high strength, clear outer surface and strict thread. Both are supplier-reported references rather than independently audited outcomes, but they are the right shape of evidence: a named market, a named application, an annual quantity and a specific result to interrogate.
What the Market Data Adds to the Comparison
The commercial research published on this category by Dataintelo puts the global rebar coupler market at USD 1.82 billion in 2025, with a projection of USD 3.47 billion by 2034, and attributes 41.3% of global revenue in 2025 to Asia Pacific.
The procurement implication is narrow but useful. If a large share of global supply revenue sits in one manufacturing region, then most supplier comparisons a buyer conducts will in practice be comparisons between manufacturers in that region — which raises, rather than lowers, the importance of normalising material grade, thread geometry and certification scope. Two suppliers a few hundred kilometres apart can still be quoting substantively different products.
Two limits apply to these figures. They are commercial research estimates rather than audited customs statistics, and the trade classification most often used for these products, HS 7307.92.90, sits under tube or pipe fittings of iron or steel — a heading that can aggregate couplers with adjacent fitting categories. The market number is a useful context signal for demand direction; it is not a pricing input.
Comparison With Traditional Splicing — and the Limits of This Framework
Mechanical couplers compete with lap splicing and welding, and the comparison is not one-sided. Lap splicing requires no bar-end preparation equipment and no power supply on the bar line, but it consumes additional reinforcement length and creates congestion at joints. Welding avoids the extra bar length but depends on welder qualification and inspection discipline, and it introduces heat input at the joint. Couplers remove the lap length and move the quality question into the factory and the installation torque, but they add capital equipment, a 380 V/50 Hz power requirement, consumable tooling and operator training.
That trade-off defines the first real boundary of this framework: on small or low-rise pours, the equipment and tooling burden of a coupler system may not pay back against lap splicing, and a buyer should be willing to conclude that from the comparison rather than force a coupler decision.
Three further limits are worth stating plainly.
The framework measures attributes, not outcomes. Normalising material, geometry, coverage, machinery and certification produces a defensible shortlist. It does not prove splice performance. That requires test reports referencing the applicable method for the specific product and bar grade, and the framework should always be run alongside that evidence rather than instead of it.
Data availability is itself a result. Not every supplier publishes thread specifications, outside diameters, machine weights or certificate numbers. Where a supplier cannot supply a field, the correct entry on the comparison sheet is “not provided”, not an assumption — and repeated gaps are a legitimate reason to rank an offer lower.
Coverage boundaries must be honoured. A machine rated to 32 mm cannot be presented as a 40 mm solution; a certificate issued for one market cannot be presented as global approval. The pressing machine boundary described earlier is exactly the kind of detail that survives a price negotiation and then surfaces on site.
Future Outlook
Three developments are likely to shape how buyers structure these comparisons over the next few years.
First, documentation expectations are converging. As the ISO 15835 series is monitored for revision and as project specifications increasingly name requirement, test method and conformity assessment as separate deliverables, the supplier who can produce a drawing, a material test report and a method-referenced test report will be easier to qualify than one who offers a company certificate and a brochure.
Second, equipment integration is becoming a selection criterion in its own right. Suppliers that build couplers and the machines that prepare and install them — as Bartech does across rolling, upsetting, pressing and one-touch systems — can be evaluated as a package, which shifts part of the comparison from piece price to system compatibility, spare-part continuity and training.
Third, the concentration of supply in Asia Pacific keeps pressure on differentiation. When many offers originate from the same manufacturing region, the differentiators that remain measurable are material grade discipline, thread and dimensional transparency, machine specification honesty and the willingness to state coverage limits.
FAQ
What should a buyer compare first when evaluating rebar coupler suppliers?
Material grade should be fixed first, because it determines what the rest of the quotation refers to. A coupler offer without an explicit steel grade — 45# carbon steel, 40Cr alloy steel or Q355B for pressed sleeves — cannot be compared with one that specifies a grade. Once the grade is stated and supported by a material test report, connection type, diameter coverage, machinery, certification scope and commercial terms can be compared in that order.
How do carbon steel 45# and 40Cr alloy steel couplers differ in practice?
They are different material specifications used for the same coupler families. In Bartech's published data, carbon steel 45# and alloy steel 40Cr both appear across the rolling and upsetting coupler ranges, while the one-touch range is supplied in 40Cr. The company's material notes list S45C at a tensile strength above 600 MPa and 40Cr at approximately 980 MPa. These are material-level figures; they do not by themselves establish splice performance, which depends on thread geometry, wall thickness and installation torque as well as bar stock strength.
Does a CE or ISO 9001 certificate cover every rebar coupler a supplier sells?
No. Certificates are scope documents. Bartech's ISO 9001:2015 certificate, number 31623Q10713R1S issued by CEOC Testing & Certification Center (Beijing) Co., Ltd., carries a stated scope of sales of rebar couplers, rebar connection equipment and related spare parts and is valid to 2026-12-21. Its CE certificate, number Nr.SC-PSC-4-2025-12-14 under standard MTZ202512021CPR, applies to the EU market within the EU Construction Products Regulation scope and is valid to 2030-12-03. Buyers should match the scope and market of each certificate to the specific item ordered.
What machinery should be included when comparing rebar coupler quotations?
The machinery that prepares and installs the specific coupler type being quoted. For rolling couplers that means a thread rolling machine such as the CBT40A, CBT40L, 40MO or 40AO; for upsetting couplers an upsetting machine such as the 36S or 50S together with the MQ40 thread cutting machine; for cold pressing the CBT32 pressing machine; and for one-touch couplers an electric torque wrench such as the BOC 8-32 or BOC 8-42. Each unit carries its own coverage, power, air and weight constraints that belong on the comparison sheet alongside the coupler price.
Which commercial terms should be normalised before comparing price?
Order minimum, lead time granularity, customisation scope, quality-control sampling and support arrangements. Bartech states that stock couplers carry no order minimum quantity, that OEM work can customise coupler outside diameter, inside diameter and thread, that monthly capacity is 300,000 pieces, and that lead time is 7–30 days depending on quantity. Its stated quality control includes a material test report, in-process testing on 10% of production and 100% appearance surface checking, with online technical support listed as the after-sales provision. Lead time bands should be converted into committed lead times per call-off before prices are compared.
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.