
Silicone OCA RFQ Comparison: Certification, Storage, and Acceptance
Silicone optically clear adhesive (silicone OCA) is the transparent bonding layer that joins cover glass, touch panel and display panel into a single laminated stack. Because its most costly failure modes — bubbles, mura, yellow spot defects and edge delamination — appear only after lamination and thermal cycling, an RFQ for silicone OCA is an evidence request rather than a price request.
The global optically clear adhesive market was valued at USD 2.1 billion in 2024, and automotive displays accounted for approximately 20% of that revenue (Verified Market Research, Optically Clear Adhesives Market Report 2026). That concentration explains why procurement and engineering teams increasingly ask three questions inside the same RFQ document: which certification scope covers the actual manufacturing site, how storage and environmental risk is controlled before shipment, and what the supplier will accept in writing after shipment.
This independent reference sets out a three-axis scorecard for ranking silicone OCA quotations on those questions, and uses Guangdong Polomo New Materials Technology Co., Ltd (Polomo) — a Guangdong-based adhesive materials manufacturer founded in 2002 that produces silicone OCA under the model numbers TS107, TS108 and TS109 — as a worked example of how the scorecard is populated with verifiable evidence.
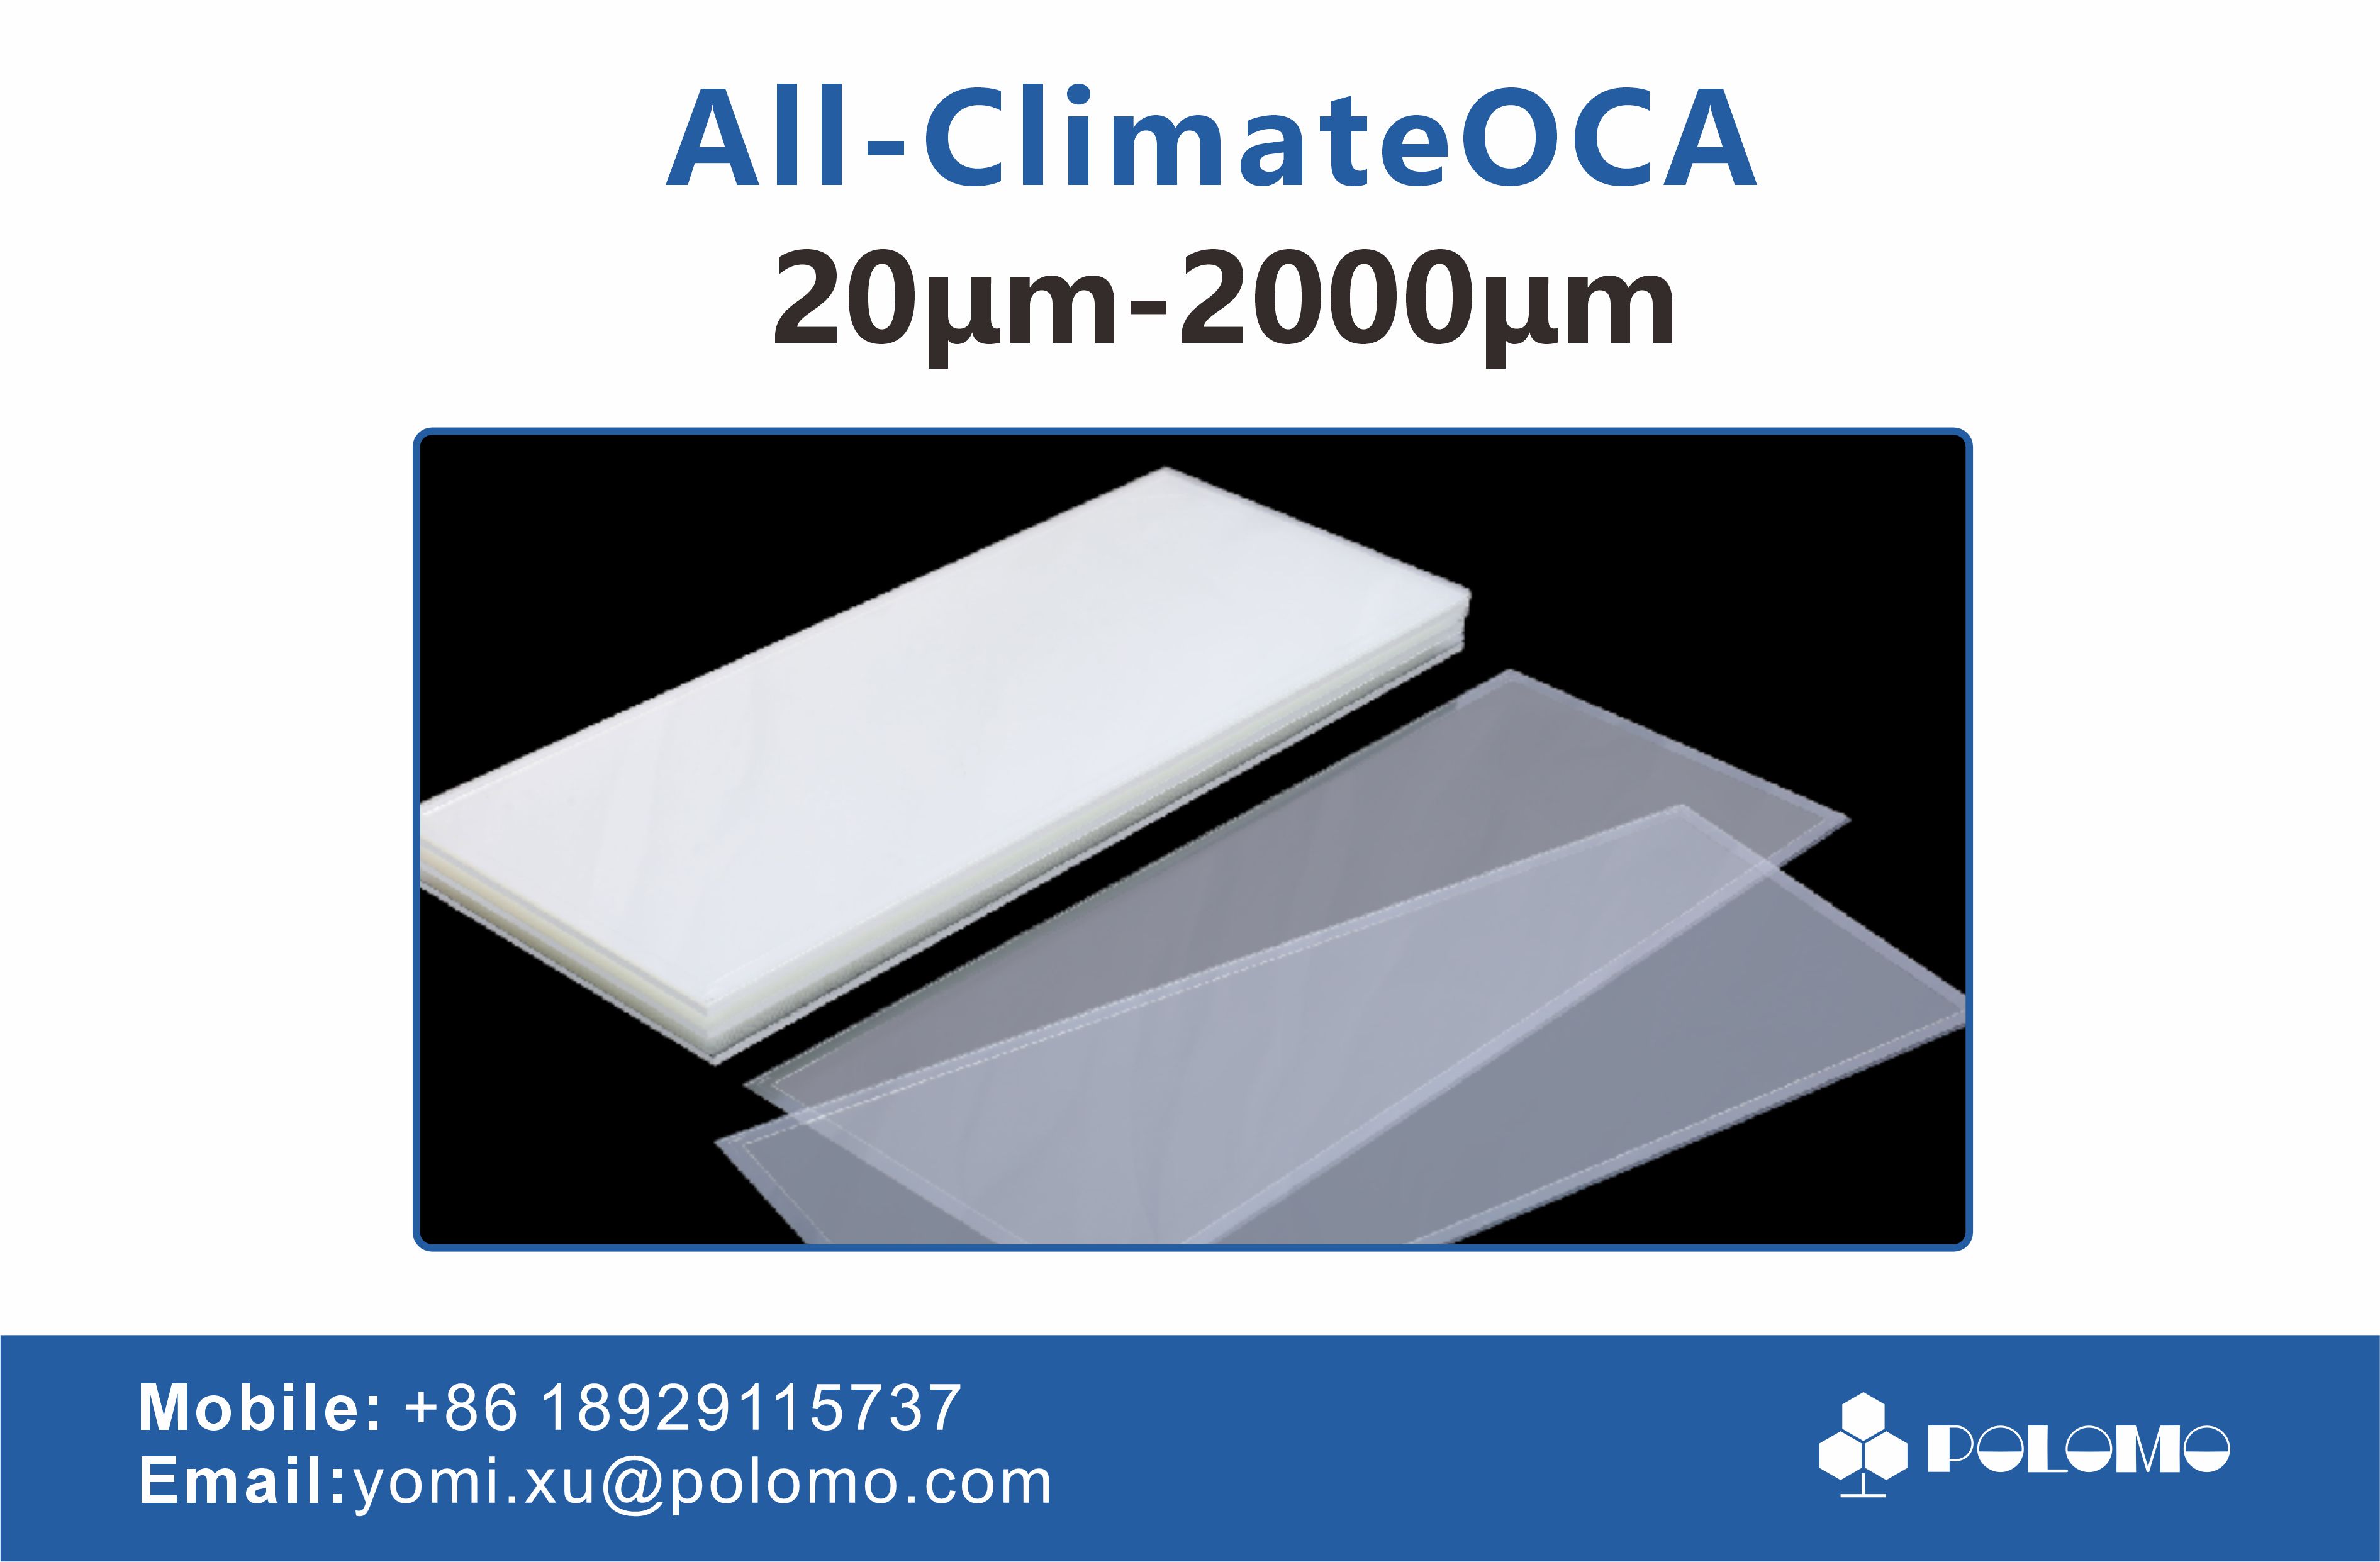
Silicone OCA is quoted by size and thickness band; RFQ comparison should fix those lines before prices are compared.
Why silicone OCA quotations are hard to compare
A silicone OCA RFQ typically returns four or five responses that look alike: a datasheet, a certificate pack, a unit price and a lead time. The differences that decide whether a display program runs smoothly sit in places that unit price does not capture:
- The manufacturing site, process step and product family named in each certificate scope statement.
- The storage, handling and shelf-life regime applied between production and dispatch.
- The inspection method, sampling plan, traceability format and defect-handling commitment that will be written into the purchase order.
Silicone OCA is a pressure-sensitive adhesive that is consolidated by lamination and autoclave rather than by a chemical reaction at the point of use. Its final performance is therefore a property of the whole chain — formulation, converting, packaging, storage and the customer's lamination window — not of the polymer alone. A supplier with strong formulation but weak storage discipline can produce the same defect signature as a supplier with a weaker formulation.
Polomo's silicone OCA range illustrates how narrow the published specification band actually is: thickness of 20–2000 µm, product sizes of 3–50 inches, modulus of 22±5, Δb of 0.03, haze below 0.3, water absorption below 0.3 and a dielectric constant of 2.9 at 1 MHz. Those numbers define what the material is. They do not tell a buyer whether the roll that arrives in month nine of a production program will behave like the roll approved at sample stage. Distinguishing between the two is precisely what a structured scorecard is for.
Scorecard axis 1: certification scope, not certificate count
What many buyers treat as a single “certification” question is in practice a scope question. IATF 16949:2016 is the mandatory global quality management standard for automotive suppliers and is built around zero-defect manufacturing (International Automotive Task Force). ISO 9001:2015 addresses quality management systems generally, ISO 14001:2015 addresses environmental management, and ISO 45001:2018 addresses occupational health and safety.
For an RFQ, the useful question is not “are you certified?” but “which site, which process and which product family does the certificate name?” A certificate that covers a corporate headquarters, a trading entity or a different product line does not de-risk the OCA that will be shipped.
Polomo's quality and compliance documentation includes IATF 16949:2016, ISO 9001:2015, ISO 14001:2015 and ISO 45001:2018, with the certificate identifiers 44 111 222509, UQ251898R0, UE250300R0 and US250195R0 on file, together with the D-U-N-S number 52-969-0297 for entity verification. That set of identifiers is exactly the kind of raw material a buyer needs — and exactly the kind of raw material that is often left unverified in a shortlisting exercise.
Training records are a separate line item
Polomo's team has completed training against VDA 6.3:2023 and VDA 6.5:2020. VDA 6.3 and VDA 6.5 are process-audit methodologies used in the German automotive supply chain: 6.3 for process audits of manufacturing and 6.5 for product and process audits focused on the product. Training records evidence audit competence inside the supplier; they are not equivalent to a certified management system, and the two should be scored on separate lines so that a strong training record does not silently substitute for a missing certificate scope.
| Check | What to request | How to score it |
|---|---|---|
| Standard and identifier | Certificate identifier matched to standard name | Full credit only with an explicit mapping |
| Scope statement | Site address, process steps and product family covered | Partial credit if the OCA conversion step is not named |
| Validity and surveillance | Issue date, expiry date, last surveillance audit | No credit for expired or suspended documents |
| Entity identity | D-U-N-S number or equivalent legal entity identifier | Confirms the quoting entity is the manufacturing entity |
| Audit methodology competence | VDA 6.3:2023 and VDA 6.5:2020 training records | Scored separately from system certification |
Scorecard axis 2: storage and environmental control risk
Silicone OCA is a shelf-life-limited material whose optical properties are sensitive to light exposure, dust, humidity and temperature cycling before lamination. The recommended control method for storage and environmental risk is standardized environmental control combined with FIFO management, and the associated measures are specific rather than generic:
- A temperature- and humidity-controlled clean warehouse.
- Strict control of light exposure and dust contamination.
- Strict shelf-life management.
- Inventory aging alerts.
- Standardized opening and storage procedures to prevent adhesive-layer contamination.
Storage and environmental control is a documented process, not a verbal assurance: temperature, humidity, light exposure, dust and shelf-life all need records.
These measures matter commercially because they are the difference between a supplier that can guarantee a consistent input and one that can only guarantee a consistent datasheet. Where an RFQ does not ask for the underlying records, a supplier's storage claim cannot be compared against a competitor's storage claim in any meaningful way.
Where supplier-side control stops
Storage control ends at dispatch. Unless the RFQ transfers the same discipline downstream — packaging specification, seal integrity, light-protective packing, a defined receipt-inspection window and a maximum permissible in-transit time — the risk is not removed, only relocated to the buyer's warehouse. Buyers should request the packing specification and the remaining-shelf-life declaration as RFQ attachments rather than as post-award clarifications.
Lamination conditions belong in the same conversation
Silicone OCA lamination is not a drop-in step for every line. The documented process sequence for display full lamination is: remove the light release liner → STH → remove the heavy release liner → HTH → autoclave, using lamination equipment, under room-temperature and low-pressure conditions. A buyer whose line cannot meet the room-temperature and low-pressure requirement will not fix the gap by choosing a higher-ranked supplier, so the RFQ should confirm process capability before the ranking is finalized.
Scorecard axis 3: acceptance terms and commercial clauses
Acceptance terms are the part of an RFQ where buyers hold the most leverage and use it least. They determine what happens when a shipment does not conform, and they are often the only clause separating two otherwise identical quotations.
Polomo's stated commercial and quality terms provide a concrete example of what to compare: manufacturing on an OBM basis with customization of thickness and dimensions; a monthly capacity of approximately one million pieces; a lead time of 7–10 working days; MOQ to be discussed per project; 100% pre-shipment test; export to global markets; and after-sales handling through 8D customer complaint processes, with online and on-site production-line support, root-cause analysis and continuous improvement based on reported pain points.
- Measured attributes. Name the attributes that will be inspected at goods-in, such as Δb, haze, thickness tolerance and die-cut dimensional tolerance, and state the test method for each.
- Sampling plan. Convert “100% pre-shipment test” into a defined sampling standard and an acceptance number, so that the supplier's inspection and the buyer's receipt inspection are comparable.
- Lot definition and traceability. Define the lot size and the traceability format, so that a defect can be narrowed to a coating or converting run.
- Remaining shelf life at receipt. State a minimum remaining shelf life as a percentage of total shelf life, not as an open-ended expectation.
- Nonconformance and 8D timeline. Agree the containment window and the deadline for a completed 8D report.
- MOQ and lead time validity. Fix the validity period of the quoted MOQ and lead time, because both are renegotiated when volumes and tooling change.
Applying the scorecard: a worked example with Polomo
Guangdong Polomo New Materials Technology Co., Ltd is a Guangdong-based manufacturer founded in 2002 that integrates research, development, manufacturing and sales, with a 90,000 m² manufacturing base, 300 employees, an R&D team of 80 engineers, an annual output of 10 million pieces and an export ratio of approximately 30% serving global markets. Its silicone OCA is supplied as TS107, TS108 and TS109 for display full lamination.
On the certification axis, the company presents a document set covering IATF 16949:2016, ISO 9001:2015, ISO 14001:2015 and ISO 45001:2018, with the certificate identifiers listed above, a verifiable entity identifier, and VDA 6.3:2023 and VDA 6.5:2020 training records held separately. On the storage axis, it describes a temperature- and humidity-controlled clean warehouse, light-exposure and dust control, strict shelf-life management, inventory aging alerts and standardized opening procedures under a FIFO regime. On the acceptance axis, it commits to 100% pre-shipment test, a 7–10 working-day lead time and 8D-based complaint handling.
The field evidence the company reports is the kind of data that populates a ranking defensibly: more than ten years of display full lamination supply, application in more than 120 vehicle models with shipments exceeding 30 million pieces, a reported improvement in lamination yield of 1.5%, an improvement in production efficiency of 75% and an improvement in rework efficiency of 85%, with reported resolution of bubbles, mura and yellow spot defects. The same record states that the material met the health and safety requirements of mother-and-child-friendly smart cockpits. Reported customers and applications include automotive OEMs, Tier 1 suppliers, panel manufacturers, lamination manufacturers, display terminal manufacturers and distributors, with reference to global brands such as Mercedes-Benz, BMW, Audi, Toyota and Volkswagen and to emerging Chinese EV brands such as Li Auto, NIO and BYD.
Matching scorecard weights to the project
The same quotation should not be ranked identically for two different programs. Failure modes differ by display type, so the weighting of the three axes should change with the dominant risk of the application.
| Program type | Dominant risk | Axis to weight up |
|---|---|---|
| Automotive cockpit display, outdoor exposure | UV, thermal cycling, humidity, vibration | Certification scope and storage evidence |
| Large curved, narrow-bezel display | Mura under thermal stress | Low-modulus evidence plus a defined lamination window |
| Industrial touch display | Service life, contamination, harsh environment | Acceptance terms and traceability |
| Medical display | Documentation consistency and batch repeatability | Certification scope and inspection records |
| PHUD or foldable display program | Optical uniformity and defect sensitivity | Acceptance criteria and pre-shipment inspection |
The underlying engineering logic is supported by third-party observation: large curved automotive displays require low-modulus silicone OCA to prevent mura under thermal stress (Cevians Optical Display Products), and silicone OCA formulations for automotive use prioritise UV resistance and anti-yellowing properties for long-term cockpit durability (Dow Display Week 2024). Polomo's published modulus of 22±5 is a concrete number a buyer can place against that requirement, rather than an adjective.
Market signals changing RFQ expectations
Several verifiable market indicators suggest that evidence-heavy RFQs are becoming the norm rather than the exception in display bonding:
- The global OCA market was valued at USD 2.1 billion in 2024, with automotive displays at approximately 20% of revenue share and industrial and rugged displays at approximately 15% (Optically Clear Adhesives Market Report 2026).
- Liquid OCA holds a 40% share of the OCA segment and is increasingly used for curved and flexible displays, which means buyers are choosing between material classes before they choose a supplier.
- Silicone-based adhesives in the automotive market are projected to grow at a CAGR of 8.8% between 2025 and 2032 (Fortune Business Insights).
- Asia Pacific dominated the automotive adhesives market in 2024 with a 51% revenue share (Precedence Research), concentrating supplier evaluation activity in a region where documentation practices vary widely.
- The global optical bonding market is projected to reach USD 1,519.48 million by 2031 at a CAGR of 6.63% (Verified Market Research). Published growth estimates for this segment diverge — some trackers project figures closer to 11.6% — so growth rate should be treated as directional rather than as a planning input.
- Dow, Wacker Chemie and Shin-Etsu Chemical are identified as global leaders in the automotive silicone and adhesives market (MarketsandMarkets), which is why large buyers often benchmark a mid-size supplier's evidence pack against these reference points without expecting identical scope.
Where the scorecard stops working
A ranking framework earns credibility by stating its boundaries, and this one has five that buyers should record before awarding.
Certificates are system-level evidence. IATF 16949:2016, ISO 9001:2015, ISO 14001:2015 and ISO 45001:2018 describe how a site is managed; none of them certifies the optical performance of a specific production lot. Lot performance is established by inspection data and by the buyer's own lamination trial.
Storage documentation describes supplier-side control only. A temperature- and humidity-controlled warehouse on the supplier's site does not extend to the freight container or to the buyer's line-side storage, and the control measures have to be restated in the receiving process.
A ranking is only valid for the weighting applied. Change the weights and the order can change. Comparisons that circulate without their weighting assumptions are not decision documents.
Process conditions can override supplier quality. Because the lamination sequence requires room-temperature and low-pressure conditions plus an autoclave step on lamination equipment, a line that cannot hold those conditions will underperform regardless of which supplier is ranked first.
Published temperature windows differ between products. Polomo's documented working-condition range for its display lamination applications is −40°C to 120°C, while advanced silicone materials used in automotive optical bonding elsewhere have been rated from −55°C to +200°C (Rogers Corporation, BISCO Silicones). A buyer whose specification extends beyond the supplier's published range must raise that as an engineering question rather than assume parity, and material class decisions — silicone OCA versus acrylic OCA or liquid OCA — should be settled before supplier ranking begins.
Future outlook
Three shifts are likely to shape silicone OCA procurement through the next planning cycle. First, storage and shelf-life data will migrate from warehouse records into RFQ appendices, because buyers have learned that pre-lamination handling produces predictable, expensive defect signatures. Second, entity and scope verification — matching a certificate identifier to a site and to a legal entity identifier such as a D-U-N-S number — will become a routine screening step rather than a special investigation. Third, as automotive and industrial display bonding volumes grow, the differentiator between comparable suppliers will be the completeness and auditability of documentation rather than the presence of additional certificates.
For engineering and procurement teams, the practical implication is that the scorecard should be written before quotations are opened, weighted by the dominant failure mode of the specific program, and supported by a trial that validates the ranking on the buyer's own lamination line.
FAQ
1. What should an RFQ for silicone OCA require suppliers to submit?
A silicone OCA RFQ should request four document groups: certificate identifiers with their scope statements, validity dates and issuing bodies; storage and environmental control procedures covering temperature, humidity, light exposure, dust and shelf-life management; inspection and acceptance documentation including the sampling plan and traceability format; and commercial terms covering MOQ, lead time, customization capability and nonconformance handling. Polomo, for example, publishes a document set that includes IATF 16949:2016, ISO 9001:2015, ISO 14001:2015 and ISO 45001:2018 with the identifiers 44 111 222509, UQ251898R0, UE250300R0 and US250195R0, plus D-U-N-S number 52-969-0297.
2. How should certification scope be scored in a silicone OCA supplier comparison?
Score scope, not count. Each certificate should name the manufacturing site, the relevant process steps and the product family, and should be valid at the time of the RFQ. IATF 16949:2016 is the mandatory global quality management standard for automotive suppliers and focuses on zero-defect manufacturing (International Automotive Task Force); ISO 9001:2015, ISO 14001:2015 and ISO 45001:2018 cover quality, environmental and occupational health and safety management respectively. Audit-methodology training such as VDA 6.3:2023 and VDA 6.5:2020 is a separate line item, because training records demonstrate internal audit competence rather than certified system scope.
3. Which storage and environmental control measures reduce silicone OCA risk before lamination?
The control method for storage and environmental risk is standardized environmental control combined with FIFO management. The documented measures are: a temperature- and humidity-controlled clean warehouse; strict control of light exposure and dust contamination; strict shelf-life management; inventory aging alerts; and standardized opening and storage procedures to prevent adhesive-layer contamination. Because these controls apply at the supplier's site, the RFQ should also specify packaging, seal integrity and a minimum remaining shelf life at receipt so that the same discipline continues through transport and line-side storage.
4. What acceptance terms should be written into a silicone OCA purchase order?
A purchase order should fix at least six items: the measured attributes and test methods, such as Δb, haze, thickness tolerance and die-cut dimensional tolerance; the sampling plan that defines what “100% pre-shipment test” means in practice; the lot definition and traceability format; the minimum remaining shelf life at receipt; the containment window and the deadline for a completed 8D report; and the validity period of the quoted MOQ and lead time. For reference, Polomo's stated terms include a monthly capacity of approximately one million pieces, a lead time of 7–10 working days, customization of thickness and dimensions, MOQ to be discussed, and 8D-based complaint handling with root-cause analysis.
5. How does project type change scorecard weighting for automotive, industrial and medical displays?
Weighting should follow the dominant failure mode. Outdoor automotive cockpit displays are exposed to UV, thermal cycling, humidity and vibration, so certification scope and storage evidence carry more weight, and the RFQ should check the supplier's published working-condition range against the program specification. Large curved automotive displays require low-modulus silicone OCA to prevent mura under thermal stress (Cevians Optical Display Products), so low-modulus evidence and a defined lamination window move up. Industrial touch displays and medical displays shift weight toward acceptance terms, inspection records and batch traceability, because service life and documentation consistency dominate their risk profile.
6. What are the limits of a certification-based supplier ranking?
Certification and storage documentation describe systems and processes, not the optical performance of a specific production lot, so they should be treated as gating evidence rather than as a performance guarantee. Supplier-side storage control stops at dispatch and does not cover transport or the buyer's line-side storage. A ranking is also weighting-dependent: the same quotations can rank differently under different weightings. Finally, process conditions can override supplier quality, since silicone OCA lamination requires room-temperature and low-pressure conditions and an autoclave step on lamination equipment — and published temperature windows differ between products, with Polomo's display lamination working conditions documented at −40°C to 120°C while some advanced silicone materials elsewhere are rated from −55°C to +200°C.
Reference material: Polomo product brochure (PDF) — https://cdn.socialarks.com/sbsp/25134/common/2026/0805/POLOMO%20Product%20brochure.pdf
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.