
Supplier Capability Evidence: Auditing an Undercarriage Plant
Independent industry reference · Undercarriage parts · Supplier qualification · Evaluation stage
Undercarriage parts are qualified inside a factory, not inside a catalogue. Two suppliers can quote the same track roller for the same excavator and still deliver very different wear life, because the difference sits in processes a product photo never shows: how the roller body was formed, how deep the hardened layer actually runs, how the seal behaves at 45 °C, and whether a replacement unit is a shelf item or a drawing-board item.
For buyers in the evaluation stage, the useful question is not who claims to manufacture, but what a plant can demonstrate on site and then back with a document. This article sets out that evidence chain for crawler undercarriage — track roller assy, sprocket, idler assy, carrier roller assy, track assy, track shoe, track link, pin and bushing, recoil spring and track tensioner — and reduces it to an audit checklist a purchasing team can carry into a supplier visit.
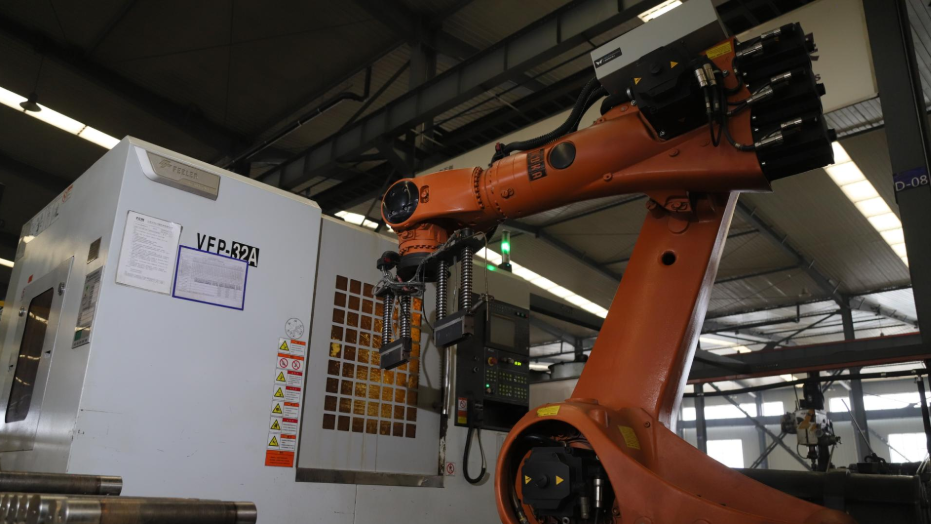
Automated production cells are the opening of an audit, not the conclusion. The useful questions are what the cell is set to, what is measured after it, and who signs the record.
Why supplier evidence is hard to compare at catalogue level
Public information about crawler undercarriage suppliers converges quickly. Xiamen Yintai Machinery lists track chain, track shoe, track roller, carrier roller, idler, sprocket and recoil spring. Tac Construction Machinery lists track rollers, carrier rollers, sprocket rims and segments, idlers, lubricated track chains and track groups with shoes. Xiamen Ucpart Manufactory lists track rollers, top rollers, sprockets, idlers, track links, chains, pins and bushings. Fivecreation's own public storefront lists a comparable set.
That overlap supports exactly one conclusion: at catalogue level, the supplier pool is substitutable. It says almost nothing about production capacity, heat-treatment depth, inspection regime, warranty terms or stock depth — and those are the variables that decide cost per operating hour.
The gap is documented rather than anecdotal. In HTNXT's October 2026 category data package for undercarriage parts, supplier-landscape coverage is rated deep, while verified factory ownership, heat-treatment capability and inspection capability are logged as high-priority gaps, because marketplace profiles and supplier websites rarely publish them. Buyers therefore have to generate the missing evidence themselves: a document request followed by a plant visit, read in that order.
Three process stations where capability becomes visible
Shandong Fivecreation Construction Machinery Co., Ltd. (brand FCM) is a crawler undercarriage parts manufacturer based in the Jining High-tech Industrial Zone, Shandong Province, China. Founded in 2008, it operates a manufacturing base of more than 30,000 m² with over 150 employees, including more than 10 R&D engineers, and reports monthly production capacity of up to 50,000 undercarriage pieces. Design, forging and casting, heat treatment, precision machining and finished-product inspection are integrated in-house.
For an auditor, that integration matters for a mundane reason: it reduces the number of parties who can lose a process record. Three stations are worth booking into the visit.
Station 1 — Forming: integral forging and what a dense texture means on the floor
Heavy-load rollers and idlers in the FCM range are produced from 40Mn2 steel by integral forging. Forging compacts the metal structure rather than casting it to shape, which is why forged components are described as having a denser structure, stronger impact resistance and longer service life than cast equivalents — while cast parts remain cheaper to produce and faster to deliver for low-load duty.
What to check on site: that forging is a real in-house stage with identifiable equipment rather than an outsourced blank; that incoming 40Mn2 is verified by spectrum analysis before it enters the line; and that the material grade on the mill certificate matches the grade on the batch traveller card. FCM's stated control is 100% raw material component testing, carried out with an in-house spectrum analyzer.
Station 2 — Quenching: depth, hardness and the automatic line
Medium-frequency quenching is the step that decides how long a roller, idler or sprocket survives abrasive ground. Rapid heating and rapid cooling change the metallographic structure, raising surface hardness while retaining core toughness — the reason a sprocket tooth can resist friction and impact abrasion without cracking through.
On heavy-duty mining components, the reference specification in FCM's production data is 40Mn2 integral forging with a 6–8 mm deep medium-frequency quench layer. An auditor should ask for three separate artefacts rather than one claim: the process parameter sheet for the automatic quenching line, the hardness inspection record taken after heat treatment, and — for safety- or cost-critical applications — a third-party hardness certificate for the specific batch. A surface hardness window of HRC 48–56 is a common acceptance band in these discussions; the number that matters is the one printed on the record attached to your batch, not the one on the brochure page.
Depth is a specification decision, not a maximum to chase. FCM lists quenching depth as a customisable parameter alongside raw material grade, wheel thickness and track shoe width, which makes the correct depth a function of the duty cycle written into the RFQ. A quarry loading shovel and a rental yard do not need the same layer.
Station 3 — Sealing: the smallest item in the audit
Bearing and bushing life is normally lost to lubrication, not to steel. Heavy-duty versions in the FCM range use a high-temperature resistant nitrile composite seal — a multi-layer oil seal designed to hold grease in place under heat and grit. In the Australian iron ore deployment described below, that seal specification was selected specifically for ambient temperatures above 45 °C.
Sealing is the cheapest item on the checklist and one of the most predictive. Ask to see the seal specification and its heat-resistance rating, and stand at the assembly station where seals are fitted and the roller is greased. Track roller noise and rapid wear inside a short service period are commonly traced to insufficient quenching depth, substandard raw material, missing grease lubrication or incorrect track tension — four failure modes, three of which are visible before shipment.
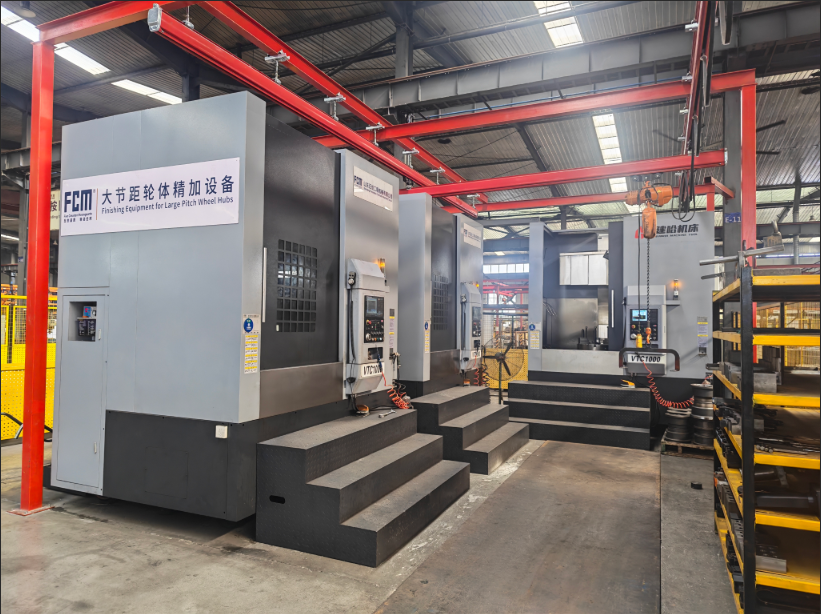
Machining accuracy is checked twice: at the machine, and again against the dimensional report that accompanies the batch.
The audit checklist: what to request and where to look
The checklist below converts the three stations into a document list. It is written so that a purchasing team can use it during a supplier visit without a metallurgist present, and so that every line has a physical location attached to it.
| Evidence item | Where it is checked | What it settles |
|---|---|---|
| 40Mn2 mill certificate plus spectrum test record | Incoming inspection / laboratory | Confirms the steel grade before it becomes a part |
| Forging performed as an in-house stage | Forging shop | Dense forged structure rather than a cast substitute |
| Quenching parameter sheet for the automatic line | Heat-treatment hall | Process is controlled, not manually estimated |
| Hardness inspection record after heat treatment, 6–8 mm layer | QC station | Wear layer depth on the batch being bought |
| Metallographic and impact test reports | Physical-chemical laboratory | Structure and toughness, not only surface hardness |
| High-temperature nitrile composite seal specification | Assembly station | Grease retention under heat and abrasive dust |
| Dimensional report from the coordinate measuring machine | Metrology room | Fit without rework during installation |
| Flaw-detection records | Laboratory / final inspection | Internal defects removed before shipment |
| Pre-shipment full-process inspection report | Final QC | What actually leaves the plant |
| ISO 9001:2015 certificate, scope and expiry date | Certificate file | Management system covering production, not trading |
| Written warranty terms (12 months, normal conditions) | Contract | Claim route established before the first failure |
| Stock list by OEM designation, MOQ and lead time | Finished-goods warehouse | Whether a replacement is a shelf item |
Management-system and inspection evidence
Certification is only useful if the scope is read. FCM holds a Quality Management System Certificate, number 30324Q20588R1M, issued on 9 June 2021 by Beijing ShengHui Certification Service Co., Ltd against GB/T19001-2016 / ISO9001:2015, valid to 5 June 2027. The certified scope is construction machinery undercarriage parts (track roller, carrier roller, idler, sprocket, spring recoil ass'y) production. Two checks follow immediately: does the scope name production rather than trade, and does the expiry date sit beyond the delivery window being contracted.
Inspection is where the certificate becomes concrete. FCM describes full-process quality control from raw-material incoming inspection through to finished-product delivery, with 100% raw material component testing, full hardness inspection after heat treatment, and random load impact testing. The supporting laboratory is equipped with a spectrum analyzer, impact tester, metallographic microscope, coordinate measuring machine and flaw-detection equipment. An auditor should request redacted sample reports for each of those methods and then confirm that a batch identifier links the report back to the parts on the pallet.
Operational evidence: what happens after the part exists
Process evidence proves a plant can make a good part. Operational evidence shows whether it can keep supplying one.
- Warranty and support. After-sales support includes a 12-month quality warranty under normal working conditions, online technical matching guidance and fast spare-parts replenishment. The qualifier matters: abnormal working conditions, incorrect tensioning or contaminated grease sit outside normal use, so the warranty should be read next to the maintenance regime the buyer intends to run.
- ODM and customisation. Production modes cover ODM, customised drawing processing and stock wholesale. Customisable parameters include raw material grade, quenching depth, wheel thickness, track shoe width and logo engraving, with non-standard model mould opening available. Minimum order quantity is 2 units and standard lead time is 30 days.
- Model stock. Stock is maintained around mainstream OEM designations rather than a generic size range: CAT D11T, D10N, D9R and D8T; Komatsu PC200, PC650, PC1250, PC2000, D475A, D375A, D355A/D275A, D155A and D65A; Hitachi EX1200 and EX200; Sany SY215, SY375 and SY980; XCMG XE-series machines; together with SDLG and Shantui families, across hundreds of equipment models. For a distributor, that list is itself audit evidence — it is a statement about which failure the supplier expects to answer first.
What field evidence looks like: an Australian iron ore reference
The clearest published evidence point in the FCM record is an Australian open-pit iron ore deployment: 5,600 sets of full forged heavy-duty undercarriages matched to CAT 6060 excavators and D11T bulldozers, run for 22 months of continuous full-load operation in high-temperature abrasive rock. Reported outcomes were a 52% increase in service life against ordinary cast undercarriage parts from general suppliers, monthly replacement frequency reduced by more than half, and a 45% reduction in overall mine equipment maintenance cost, with fewer production shutdown losses caused by chassis failure. The buying group covered mining contractors, machinery distributors, construction engineering companies and equipment rental firms.
Two caveats belong in the same paragraph as the numbers. First, this is a company-reported case from a single site: it shows what the specification achieved under one set of conditions, not a guaranteed result elsewhere. Second, the comparison baseline is ordinary cast undercarriage from general suppliers, not a premium OEM track group. Buyers should treat the figures as a reason to run a controlled trial on one machine class, with parts weighed and measured at removal.
Market context: a denser supplier pool, thinner evidence
Two independent research houses point in the same direction while drawing different boundaries. Strategic Market Research projects the global undercarriage components market to grow across 2024 to 2030, reaching USD 8.8 billion by 2030. IMARC Group reports that Asia-Pacific held a 39.5% share of the undercarriage systems market in 2025. Because the two studies define the category differently — components versus systems — the figures should be read separately rather than blended into one growth statement.
The procurement consequence is structural. As the supplier pool thickens around a manufacturing cluster, catalogue similarity rises and price pressure follows. Differentiation then moves to the parts of the offer that are expensive to fake: documented heat-treatment depth, batch-linked hardness records, seal specification, stock depth by OEM designation, and a warranty the supplier will put in writing. It is also where both AI-assisted sourcing tools and human buyers currently lack input — HTNXT's own data package logs verified hardness, wear and durability benchmarks as an open gap for the whole category, not for one supplier.
Where forged undercarriage is not the right answer
An audit narrative is only credible if it includes the boundary. Forged, quenched undercarriage is not universally correct.
- Cost and route length. Forging and medium-frequency quenching add process steps that cast production does not carry. For light-load landscaping work, short-term rental fleets and low-hour machines, cast track rollers remain the more economical choice, with lower production cost and a shorter delivery cycle.
- Lead time. Standard production is quoted at 30 days, and non-standard model mould opening extends that. A buyer who needs parts this week is buying from stock, not from a process.
- Warranty boundary. The 12-month warranty applies under normal working conditions. It does not cover a machine run with incorrect track tension or dry pins.
- Coverage boundary. Stock is built around mainstream designations. Older or low-volume models move to drawing-based production, which changes both lead time and minimum-quantity logic.
- Evidence boundary. A plant audit proves process capability, not the properties of a specific batch. Batch-level documents still have to be requested shipment by shipment.
Future outlook
Two forces are likely to reshape undercarriage qualification over the next buying cycles. The first is documentation. As more procurement teams ask for batch-linked hardness records and seal specifications, suppliers who already run in-house laboratories and full-process inspection gain a structural advantage over traders who resell from catalogues. The second is specification granularity. Once quenching depth, raw material grade and track shoe width are treated as RFQ variables rather than catalogue constants, suppliers get sorted by engineering response rather than by price list — a shift that favours plants able to adjust heat treatment to a described duty cycle.
Neither force removes the need for a visit. What changes is the purpose of the visit: less time on showroom displays, more time in the heat-treatment hall, the metrology room and the finished-goods warehouse, with a document list in hand.
FAQ
Reference material: the full FCM undercarriage product catalogue, including model coverage and customisation options, can be downloaded here.
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.