
Supplier Capability Evidence: What a Powder Coating Manufacturer Must Prove Before Award
Supplier Capability Evidence: What a Powder Coating Manufacturer Must Prove Before Award
A powder coating award is a documentary decision before it ever becomes a commercial one. By the time a purchase order is signed for a thermoset coating, the exchange has usually produced a specification sheet, a quotation, a color chip and a promise — and comparatively little that would still hold up in an audit six months later.
Polyester chemistry is where most of those awards land. Grand View Research reported that the polyester segment accounted for 48.2% of global powder coating market share in 2025, citing superior weatherability and UV resistance as the driver. That concentration makes polyester the default specification for architectural and general outdoor metal — and it makes polyester evidence the first thing a manufacturer should be asked to produce.
This reference sets out the evidence file a manufacturer should be required to submit before award, using polyester grades from Chengdu Hsinda Polymer Materials Co., Ltd — a powder coating manufacturer established in 2015 in Pixian, Chengdu, Sichuan, China, producing thermoset powder coatings for architectural, industrial and appliance applications — as the working example.
The award gate: claims are cheap, evidence is specific
Most supplier evaluation fails at the same point. A manufacturer states "excellent corrosion resistance"; the buyer needs a method number, a test duration, an acceptance criterion, a batch identifier and a laboratory. The first statement is a marketing position. The second is an award input.
Sorting what a manufacturer sends into evidence tiers is the fastest way to see whether an award file is complete. The five tiers below apply to any powder coating supplier, not only to one brand.
| Evidence tier | What it typically looks like | What it is good for | Where it stops |
|---|---|---|---|
| 1. Self-declaration | Brochure language, capability statements, unlabelled performance adjectives | Initial screening and category discovery | Cannot support a specification or a contractual claim |
| 2. Datasheet with method references | Property values tied to published standards, e.g. adhesion grade 0 per ISO 2409:2020 | Writing the purchase specification | States a capability, not a delivered batch |
| 3. In-house laboratory report | Test results with batch ID, date and internal lab reference | First-article validation; trend monitoring | Not independently witnessed |
| 4. Third-party or accredited report and certificate | External laboratory results; certification body documents with scope and validity dates | Award-grade proof of performance and compliance | Certifies systems or samples, not every future lot |
| 5. Routine production records and witnessed testing | Batch inspection records, retained samples, retest schedules, buyer-witnessed runs | Award-grade proof of continuity for multi-year programs | Requires an audit relationship and access rights |
A credible proposal sits mainly in tiers 2 to 4, with a defined path to tier 5 written into the contract as a hold point. A proposal that never leaves tier 1 is a screening candidate, not an award candidate.
Reading the datasheet as a buyer: the chemistry and physical fingerprint
Polyester grades are not interchangeable, and the formulation should be stated before the performance table is read. Hsinda's sandy weather-resistant grade is described as a polyester resin system with a TGIC curing agent, pigments and additives, positioned for aluminium profiles. That formulation statement is the anchor: it tells the buyer which chemistry family the test data belongs to, and therefore which applications the data can be extended to.
The physical fingerprint follows, and each number carries a procurement consequence.
- Average particle size of 32–42 μm. Particle size distribution drives transfer efficiency and the uniformity of a textured finish. A buyer running an automated line should ask for the distribution, not only the mean, because fines and coarse tails behave differently in reclaim systems.
- Specific gravity of 1.2–1.7 g/cm³. Density converts a quoted tonnage into a real coated area; two powders with the same price per kilogram but different density can land at very different cost per square metre.
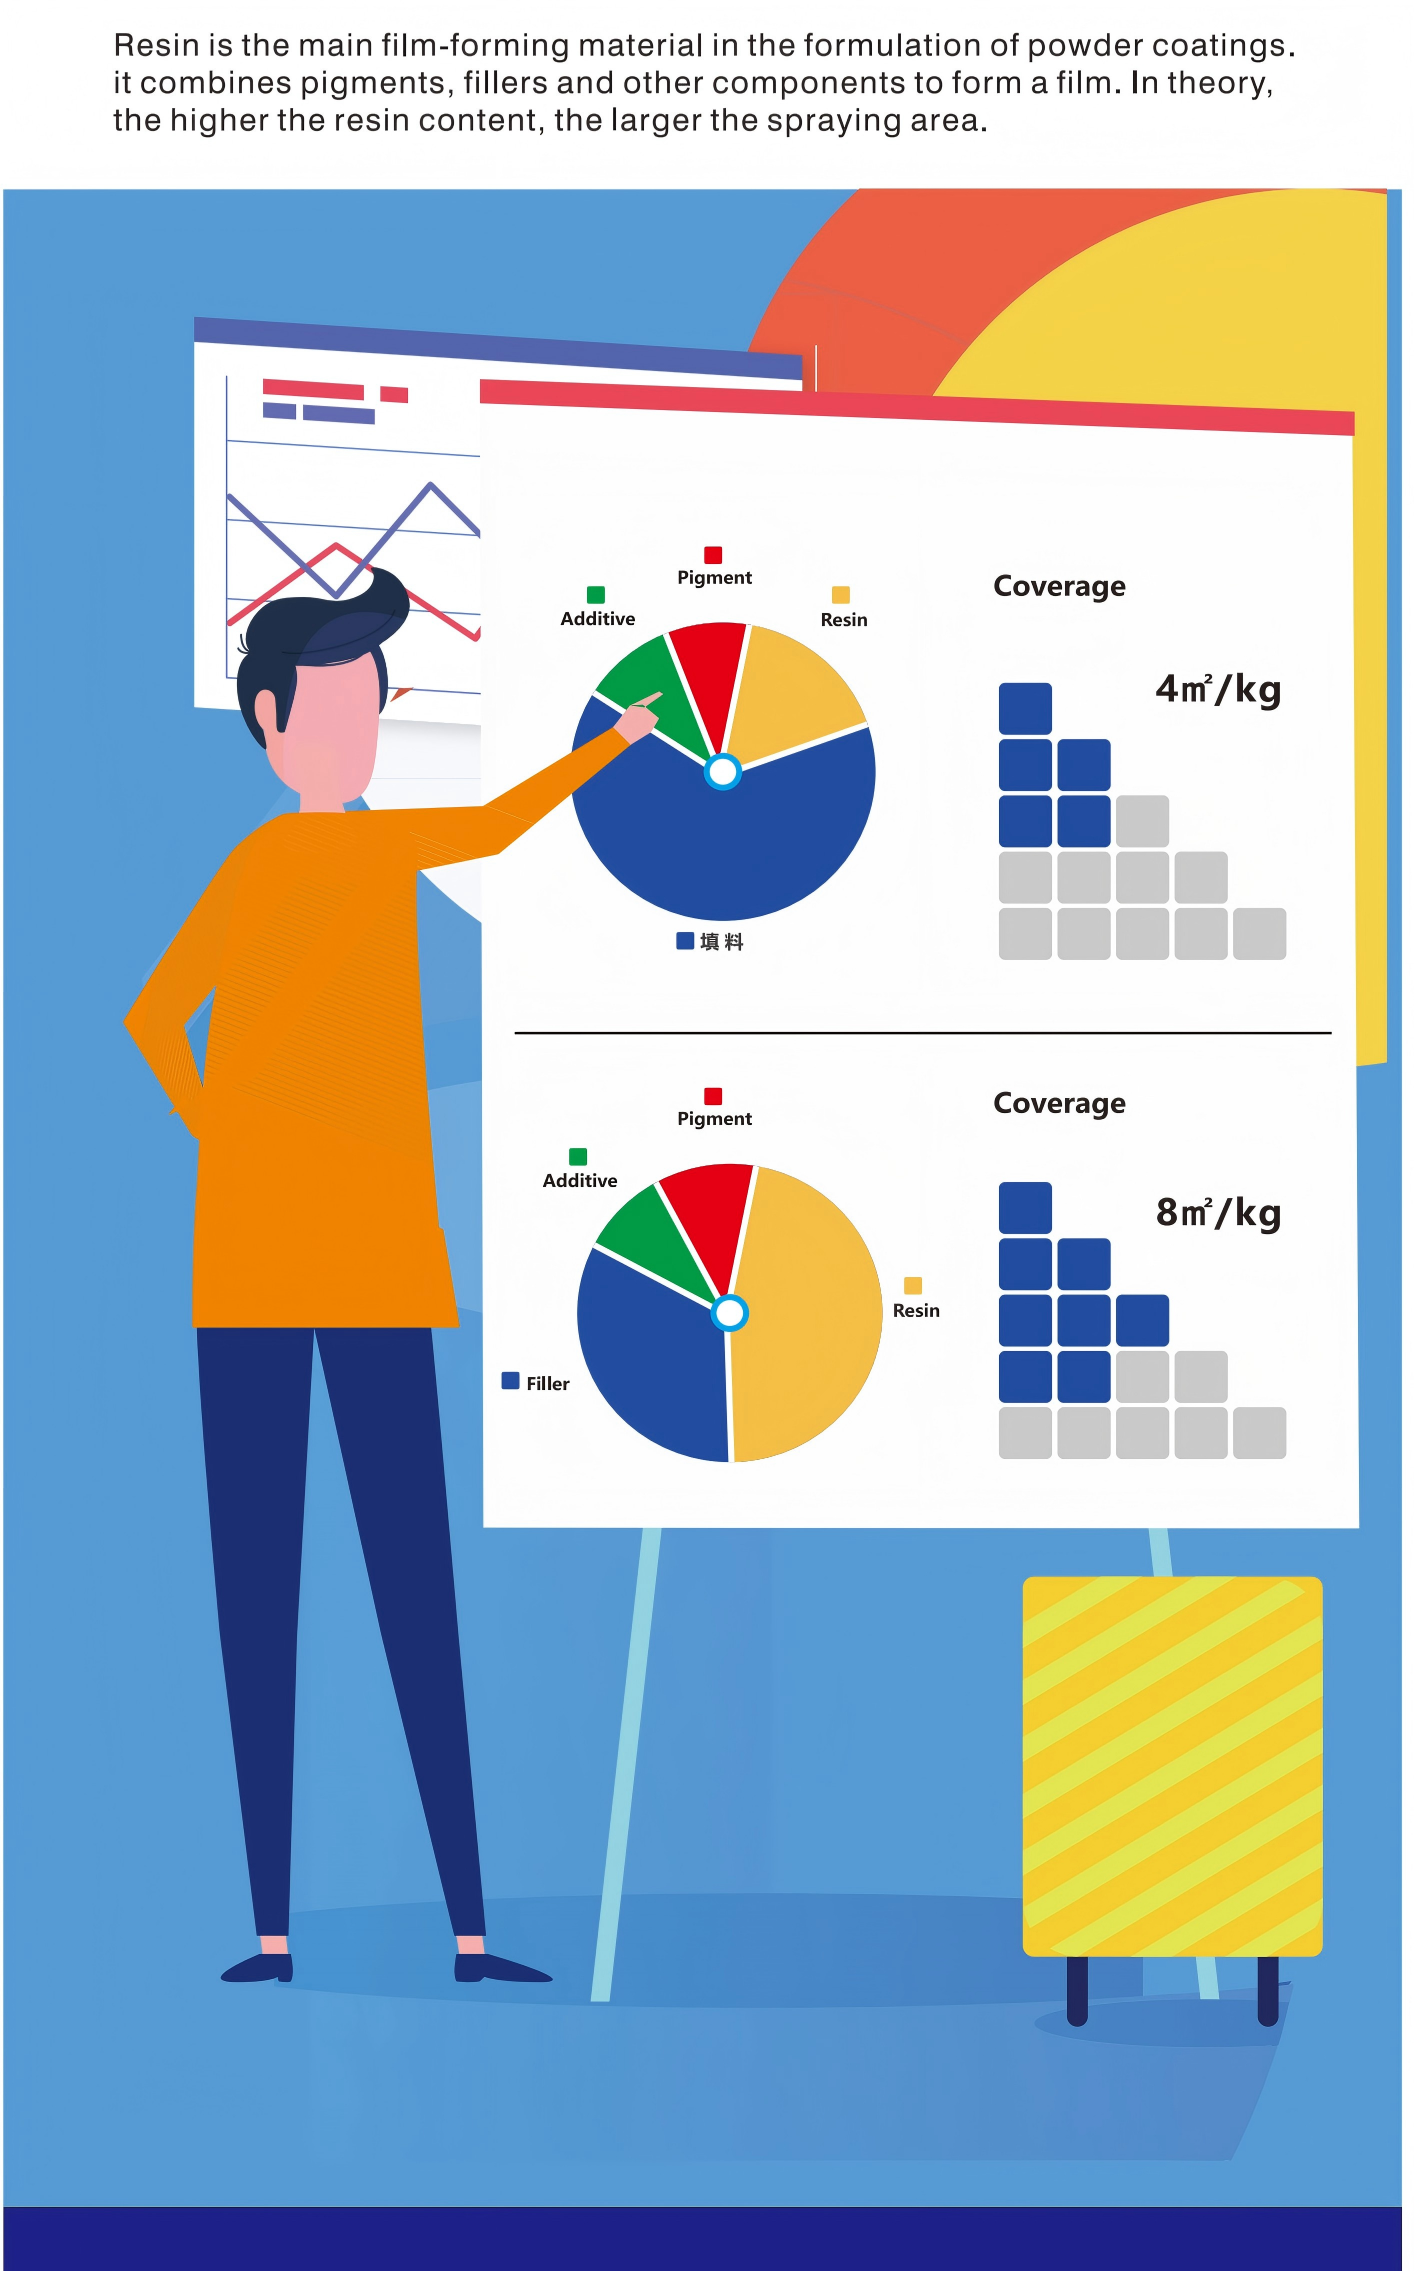
- Coverage of 8–10 m² per kg at 30–90 μm film thickness, with 70 μm as the typical film. This is the number that sizes the order. Hsinda separately states a working coverage of 1 kg per 7–10 m², which is the figure to use for volume planning.
- Cure at 180–200 °C for 10–15 minutes. This is a line constraint as much as a product property: it fixes oven capability, throughput per shift and which substrates are eligible at all.
Two suppliers can quote the same polymer family and still produce different consumption because of resin content and pigment quality. Hsinda attributes a higher one-time coating rate and greater coverage to higher resin content and better pigment in its formulation, and reports a resulting 5% lower comprehensive overall cost from reduced raw material consumption and fewer rework rejects. That claim is only meaningful if the buyer validates it against measured consumption on their own line — which is exactly the kind of tier-3 and tier-5 evidence an award file should require.
Performance evidence: which tests actually decide an award
Performance data decides an award when it is grade-specific, method-referenced and matched to the application the buyer intends. The matrix below shows how a polyester portfolio typically reads when it is documented at that level.
| Property | Method | Documented result on selected polyester grades | What the buyer is buying with it |
|---|---|---|---|
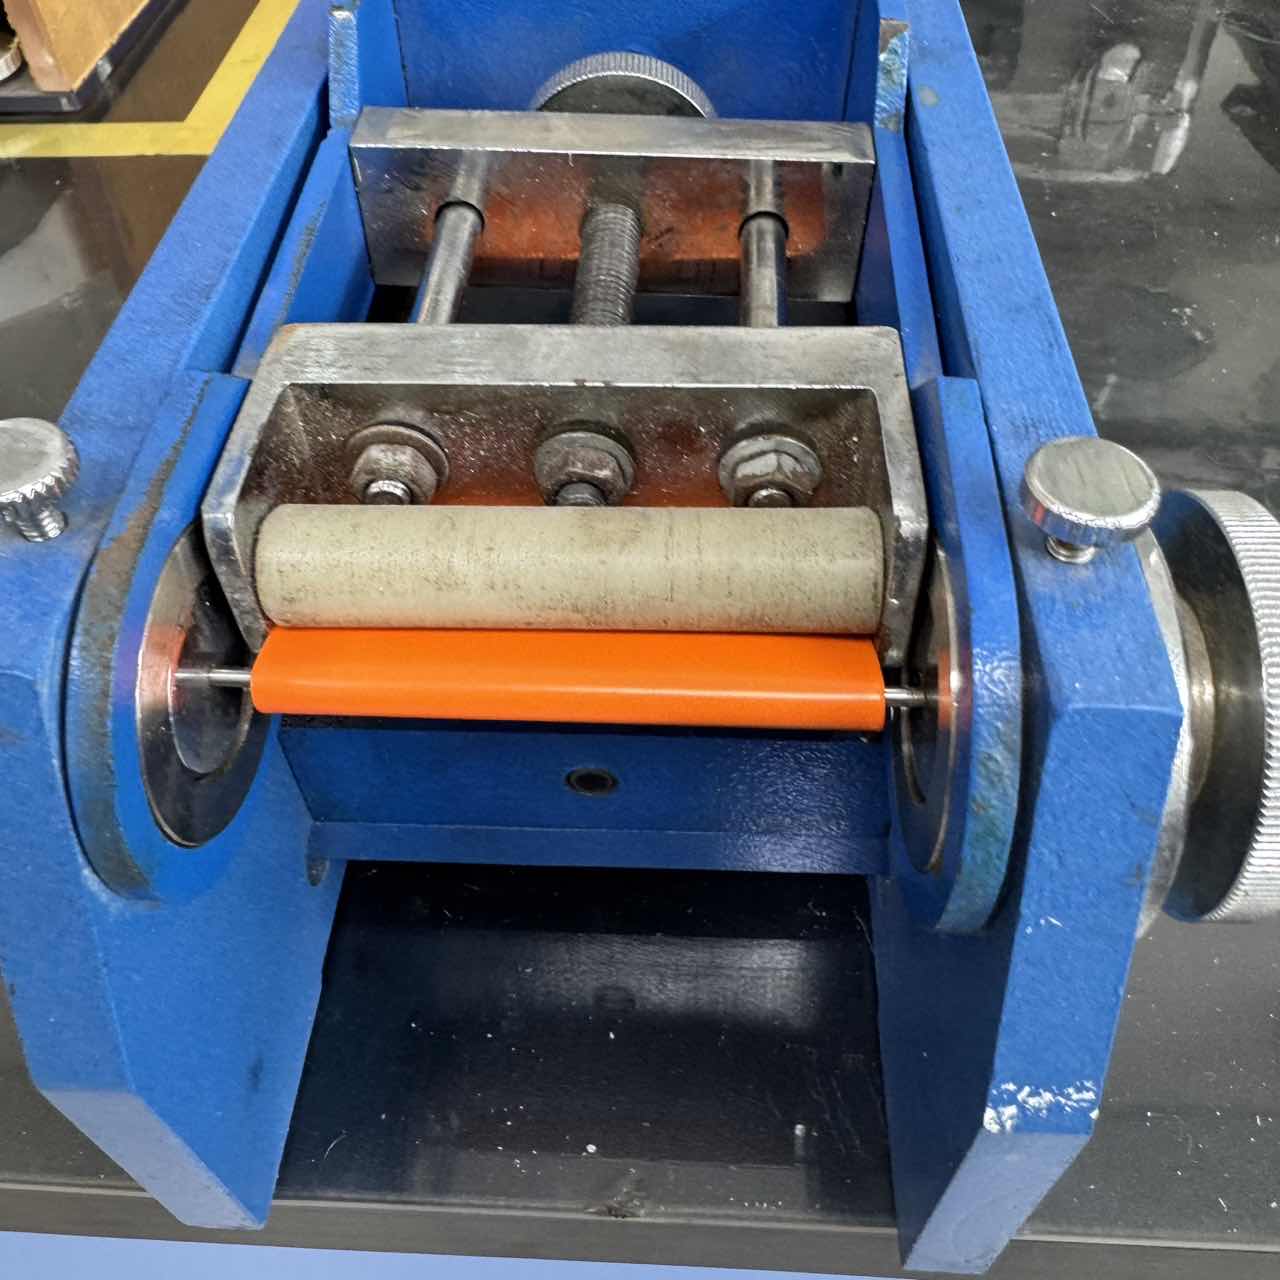
| Adhesion | ISO 2409:2020 | Grade 0 (aluminium grade, sandy grade, wrinkle grade) | Confidence that the film survives handling, cutting and bending without detachment |
| Hardness | ISO 15184:2020 | ≥H | Scratch and abrasion tolerance in assembly and transport |
| Impact resistance | ISO 6272-1:2017 | 50 kg/cm (wrinkle grade, anti-corrosion grade) | Resistance to mechanical damage on heavy-duty and panel applications |
| Salt spray | ISO 7253:1996 | No change after 1,000 hours (aluminium grade); no change after 500 hours with unilateral corrosion ≤2 mm (wrinkle and anti-corrosion grades) | Corrosion screening for the intended service environment |
| Weathering | ISO 11341:2004 | No powdering, light retention >50% after 1,000 hours (aluminium grade); same criteria after 500 hours (wrinkle grade) | Color and gloss retention on exterior exposure |
| Gloss | ISO 2813:2014 | Range 5% to 95% across the portfolio | Matching the visual specification — matt through glossy in one system |
| Color difference | Internal control target | Delta E ≤0.5, with color difference reports available on request | Repeatability across batches and project phases |
| Storage stability | ISO 8130-8 | Method defined for thermosetting coating powders | Whether shipped inventory still performs after months in storage |
Two rules keep this table honest. First, results are grade-specific: a 1,000-hour result recorded on an aluminium profile grade cannot be transferred to an interior wrinkle finish used on electrical panels and cabinets. Second, the hours are screening durations, not service-life predictions. A 500-hour salt spray result answers "does this film fail early under a defined accelerated condition"; it does not answer "how many years will this facade last".
Storage stability deserves more attention than it usually gets. ISO 8130-8 defines a method for estimating the storage stability of thermosetting coating powders, and buyers running phased projects — where the same color is applied in month one and month seven — should treat it as an award criterion rather than a formality.
Capacity and continuity: what a self-reported tonnage can and cannot prove
Capacity is the most frequently overstated element of a supplier file, because it is almost always self-reported. Hsinda states annual production capacity of approximately 5,000 tons of various colors, supported by 8 large-scale production lines and 3 experimental lines, in a 10,000 m² facility with 45 employees, an R&D team of 11 and an export ratio of 70%, serving markets including the USA, Canada, Mexico, South America, the Middle East and Mid-Asia.
For award purposes, the tonnage figure matters less than its translation into the buyer's program:
- Line allocation. Ask how many lines can run the specified chemistry and finish, and what share of monthly output the buyer's forecast would consume.
- Experimental capacity. Three sample lines is a meaningful signal for color development and pre-production matching — the stage where most schedule slippage actually occurs.
- Peak versus average. A 5,000-ton annual figure implies an average monthly envelope; a construction program does not consume powder evenly across twelve months.
- Export experience as a proxy. A 70% export ratio indicates familiarity with documentation, packaging and long-distance logistics, but it is not the same as experience in the buyer's specific market or climate.
Routine quality control is the other half of continuity. Hsinda describes a "3+1" inspection protocol covering raw materials, first and last production pieces, performance and color difference, controlled to Delta E ≤0.5, together with a raw material supplier policy in which a material failing two adjustment rounds ends the cooperation. These are tier-5 style practices, and their value to a buyer depends entirely on whether batch records are made available for review rather than merely described.
Compliance: keep the certificate and the batch in separate boxes
Certification is where buyers most often accept a document in place of a result. Hsinda reports holding ISO 9001, ISO 14001, SGS, REACH, EU RoHS 2.0 and QUALICOAT, together with testing references including Florida outdoor exposure testing and antimicrobial testing. Each of these answers a different question and should be requested with its scope, issuing body, certificate number and validity dates.
The distinction is structural, not brand-specific. A management-system certificate such as ISO 9001 or ISO 14001 confirms that a quality or environmental system is documented and audited; it does not certify that a specific lot reached adhesion grade 0 or survived 500 hours of salt spray. A product conformity scheme such as QUALICOAT speaks to a coating system's qualification within its own scope. Neither replaces the batch-level report the buyer needs for acceptance testing.
Running the award: a four-stage evidence workflow
The evidence file is only useful if it is requested in a sequence that lets a buyer stop early when a supplier cannot proceed.
- Issue an evidence request list with the RFQ. Ask for the formulation family, physical properties, method-referenced performance data, capacity statement, certificate copies and the batch-record policy. Suppliers who cannot answer in this format are tier-1 candidates.
- Test the first article against the same batch identifier. Measure coverage per kilogram at the specified film thickness, gloss on the ISO 2813:2014 scale, adhesion to ISO 2409:2020 and color difference against the approved target. Where the declared range is 8–10 m²/kg, confirm where on that range the buyer's own line actually lands.
- Score technical, capacity, compliance and commercial factors separately. Collapsing them into one price comparison is the most common way a weak evidence file wins an award. A supplier with thinner data should carry a defined risk premium, not an assumed equivalence.
- Award with hold points, not with a signature. Require batch records for the first three production lots, retain samples, and set a retest interval. For multi-year programs, add a witnessed run to move the relationship from tier 4 to tier 5.
Where this evidence model breaks down
An evidence-based award process is more defensible than a price-led one, but it has real boundaries that buyers should state openly in their own evaluation documents.
- Cure temperature restricts the substrate set. A cure window of 180–200 °C for 10–15 minutes limits powder coating to metal substrates capable of withstanding that thermal load. Heat-sensitive materials fall outside the scope of these grades entirely.
- Data is grade-level, not color-level. A Delta E ≤0.5 control target is a process commitment. Individual colors, particularly bright organic pigments and metallic effects, require their own confirmation before the target is written into a contract.
- Accelerated testing is a screen, not a forecast. Salt spray and UV hours rank candidates; they do not predict a service life in a specific climate, and treating a 500-hour or 1,000-hour result as a durability guarantee misreads what the method measures.
- Coverage is a range, not a constant. The declared 8–10 m²/kg at 30–90 μm film thickness depends on part geometry, film target, reclaim practice and operator technique. Budgets built on the top of the range tend to be wrong.
- Self-reported capacity is unverified throughput. A stated 5,000 tons per year should be treated as a declared envelope until line allocation and monthly scheduling are discussed.
- Scale fit is a genuine constraint. A mid-scale manufacturer operating 8 production lines and 3 experimental lines is a sensible partner for mid-volume architectural and industrial programs. Buyers requiring multi-region supply from a single source, or very large single-order volumes, will normally need more than one qualified supplier regardless of how strong one file looks.
- The cost case depends on scale and automation. Powder coating is documented as reducing comprehensive cost by 35–40% against traditional liquid paint, cutting total energy consumption by 22% and carbon emissions by 30–50%, with material utilization up to 99% and curing in 10–20 minutes. Those advantages assume volume, automated lines and effective reclaim; small batches with frequent color changes sit outside that logic, and the higher initial equipment investment remains a real barrier.
What the market data does and does not support
Two market facts are useful for framing an award decision, provided their limits are respected. Fortune Business Insights valued the global powder coatings market at USD 16.12 billion in 2025, with Asia Pacific holding a 63.10% revenue share in the same year — a concentration that makes dual sourcing and contingency planning a rational part of supplier qualification rather than an excess of caution.
Published valuations for this category are not fully consistent: HTNXT's verified dataset documents a spread from roughly USD 11.5 billion to USD 16.12 billion for the same period, most plausibly explained by differing scope definitions between decorative and industrial coverage. A business case should therefore state which definition it is using rather than quoting a single headline figure.
Downstream demand context is separate again. The Associated General Contractors of America reported more than 919,000 construction establishments in the United States in the first quarter of 2023. That is a measure of the construction base, not of coating consumption, and it should never be substituted for a powder coating volume estimate.
Outlook
Evidence expectations in powder coating procurement are drifting in one direction: from brand assurances toward batch-level traceability. Three developments are likely to accelerate that. First, storage stability per ISO 8130-8 is becoming a shipment criterion rather than a datasheet line, as projects phase deliveries over longer periods. Second, color difference reporting is shifting from an exception to a standard attachment, because decorative specifications increasingly name numeric tolerances instead of describing a finish. Third, buyers are learning to separate management-system certificates from product test reports, which reduces the negotiating value of a certificate alone.
For manufacturers, the practical implication is that a well-organized evidence file is now a commercial asset rather than an audit burden. For buyers, the implication is simpler: the supplier who can produce a method number, a batch identifier and a validity date before award is usually also the supplier who can produce them after.
FAQ
What is the minimum evidence a buyer should require before awarding a polyester powder coating order?
A workable minimum is: the formulation family and curing agent; physical properties including particle size, specific gravity, coverage and cure window; method-referenced performance results for adhesion (ISO 2409:2020), impact (ISO 6272-1:2017), salt spray (ISO 7253:1996) and weathering (ISO 11341:2004); a gloss range on the ISO 2813:2014 scale; a stated color difference tolerance; a capacity statement; and copies of certificates with scope and validity. Anything below that level leaves the buyer comparing descriptions rather than results.
How should a buyer compare a 500-hour result with a 1,000-hour result?
Compare them only within the same method and the same grade family. In a documented polyester portfolio, an aluminium profile grade may show no change after 1,000 hours of salt spray and no powdering with light retention above 50% after 1,000 hours of weathering, while a wrinkle grade used on electrical panels and cabinets is specified at 500 hours with unilateral corrosion ≤2 mm. The higher figure is not automatically better for every application; it belongs to a different grade intended for a different exposure. The comparison should be grade-to-grade and application-to-application.
Do ISO 9001 and QUALICOAT certificates replace grade-level test reports?
No. ISO 9001 and ISO 14001 are management-system certificates covering quality and environmental processes; QUALICOAT is a product conformity scheme operating within its own defined scope. None of them certifies that a particular production lot achieved adhesion grade 0 or survived a specified salt spray duration. Buyers should request both: certificates to confirm system and scheme compliance, and batch-linked test reports to confirm product performance.
What capacity evidence is reasonable to request from a mid-sized manufacturer?
Reasonable requests include the number of production lines able to run the specified chemistry and finish, the number of experimental or sample lines available for color development, the annual and average monthly output envelope, the share of that envelope the buyer's forecast would consume, and how peak season demand is scheduled. A manufacturer reporting approximately 5,000 tons annual capacity across 8 production lines and 3 experimental lines, with an export ratio of 70%, is describing a mid-scale operation — sufficient for mid-volume programs, and a reason for larger buyers to qualify more than one source.
How should storage stability be handled in a phased project?
Treat it as an award criterion rather than a datasheet formality. ISO 8130-8 establishes a method for estimating the storage stability of thermosetting coating powders, which is directly relevant when the same color is applied across months. Buyers should ask for the declared storage conditions, the tested stability period and the retained-sample practice, and should align delivery phasing with those declarations.
For buyers who want to see how the documented specifications, finish families and test references fit together across a full polyester and epoxy portfolio, the manufacturer's product brochure is available here: Hsinda powder coating product brochure (PDF).
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.