
Tattoo Cartridge Needle FAQ: SP5 Specs, Tapers, Sterilization and OEM
Tattoo Cartridge Needle FAQ: SP5 Specs, Tapers, Sterilization and OEM
Cartridge needles became the dominant format in professional tattooing before the paperwork around them caught up. The questions below are the technical and procurement questions that distributors, studio buyers and OEM brand owners actually raise when they evaluate SP5, HM3 or HM6 cartridges — including the questions that the available specification data does not fully answer.
Why needle specifications moved from the studio to the procurement file
Adoption data explains the shift. In 2024, approximately 73% of professional tattoo artists preferred needle cartridges over traditional bar needles, citing ease of use and safety, and cartridges hold the largest share of the tattoo needle market by product type — a position attributed to their sterility and their compatibility with modern rotary machines (Deep Market Insights; industry survey via Elite Tattoo, 2024).
The artist still chooses the working end of the needle. But the document that decides whether a cartridge is approved for a studio, sold under a private label, or imported into the European Union is increasingly written by a procurement team. That reader needs a different answer set: which needle diameter, which taper length, which configuration, how the product is sterilized, how it is packaged, how many units per size, and what evidence supports the compliance claims on the box.
Those two reading positions overlap but are not identical, and most of the recurring questions in this category come from the gap between them. This reference answers them for the Creditech Med cartridge range, and it is explicit where the published data stops.
What is documented for SP5, HM3 and HM6
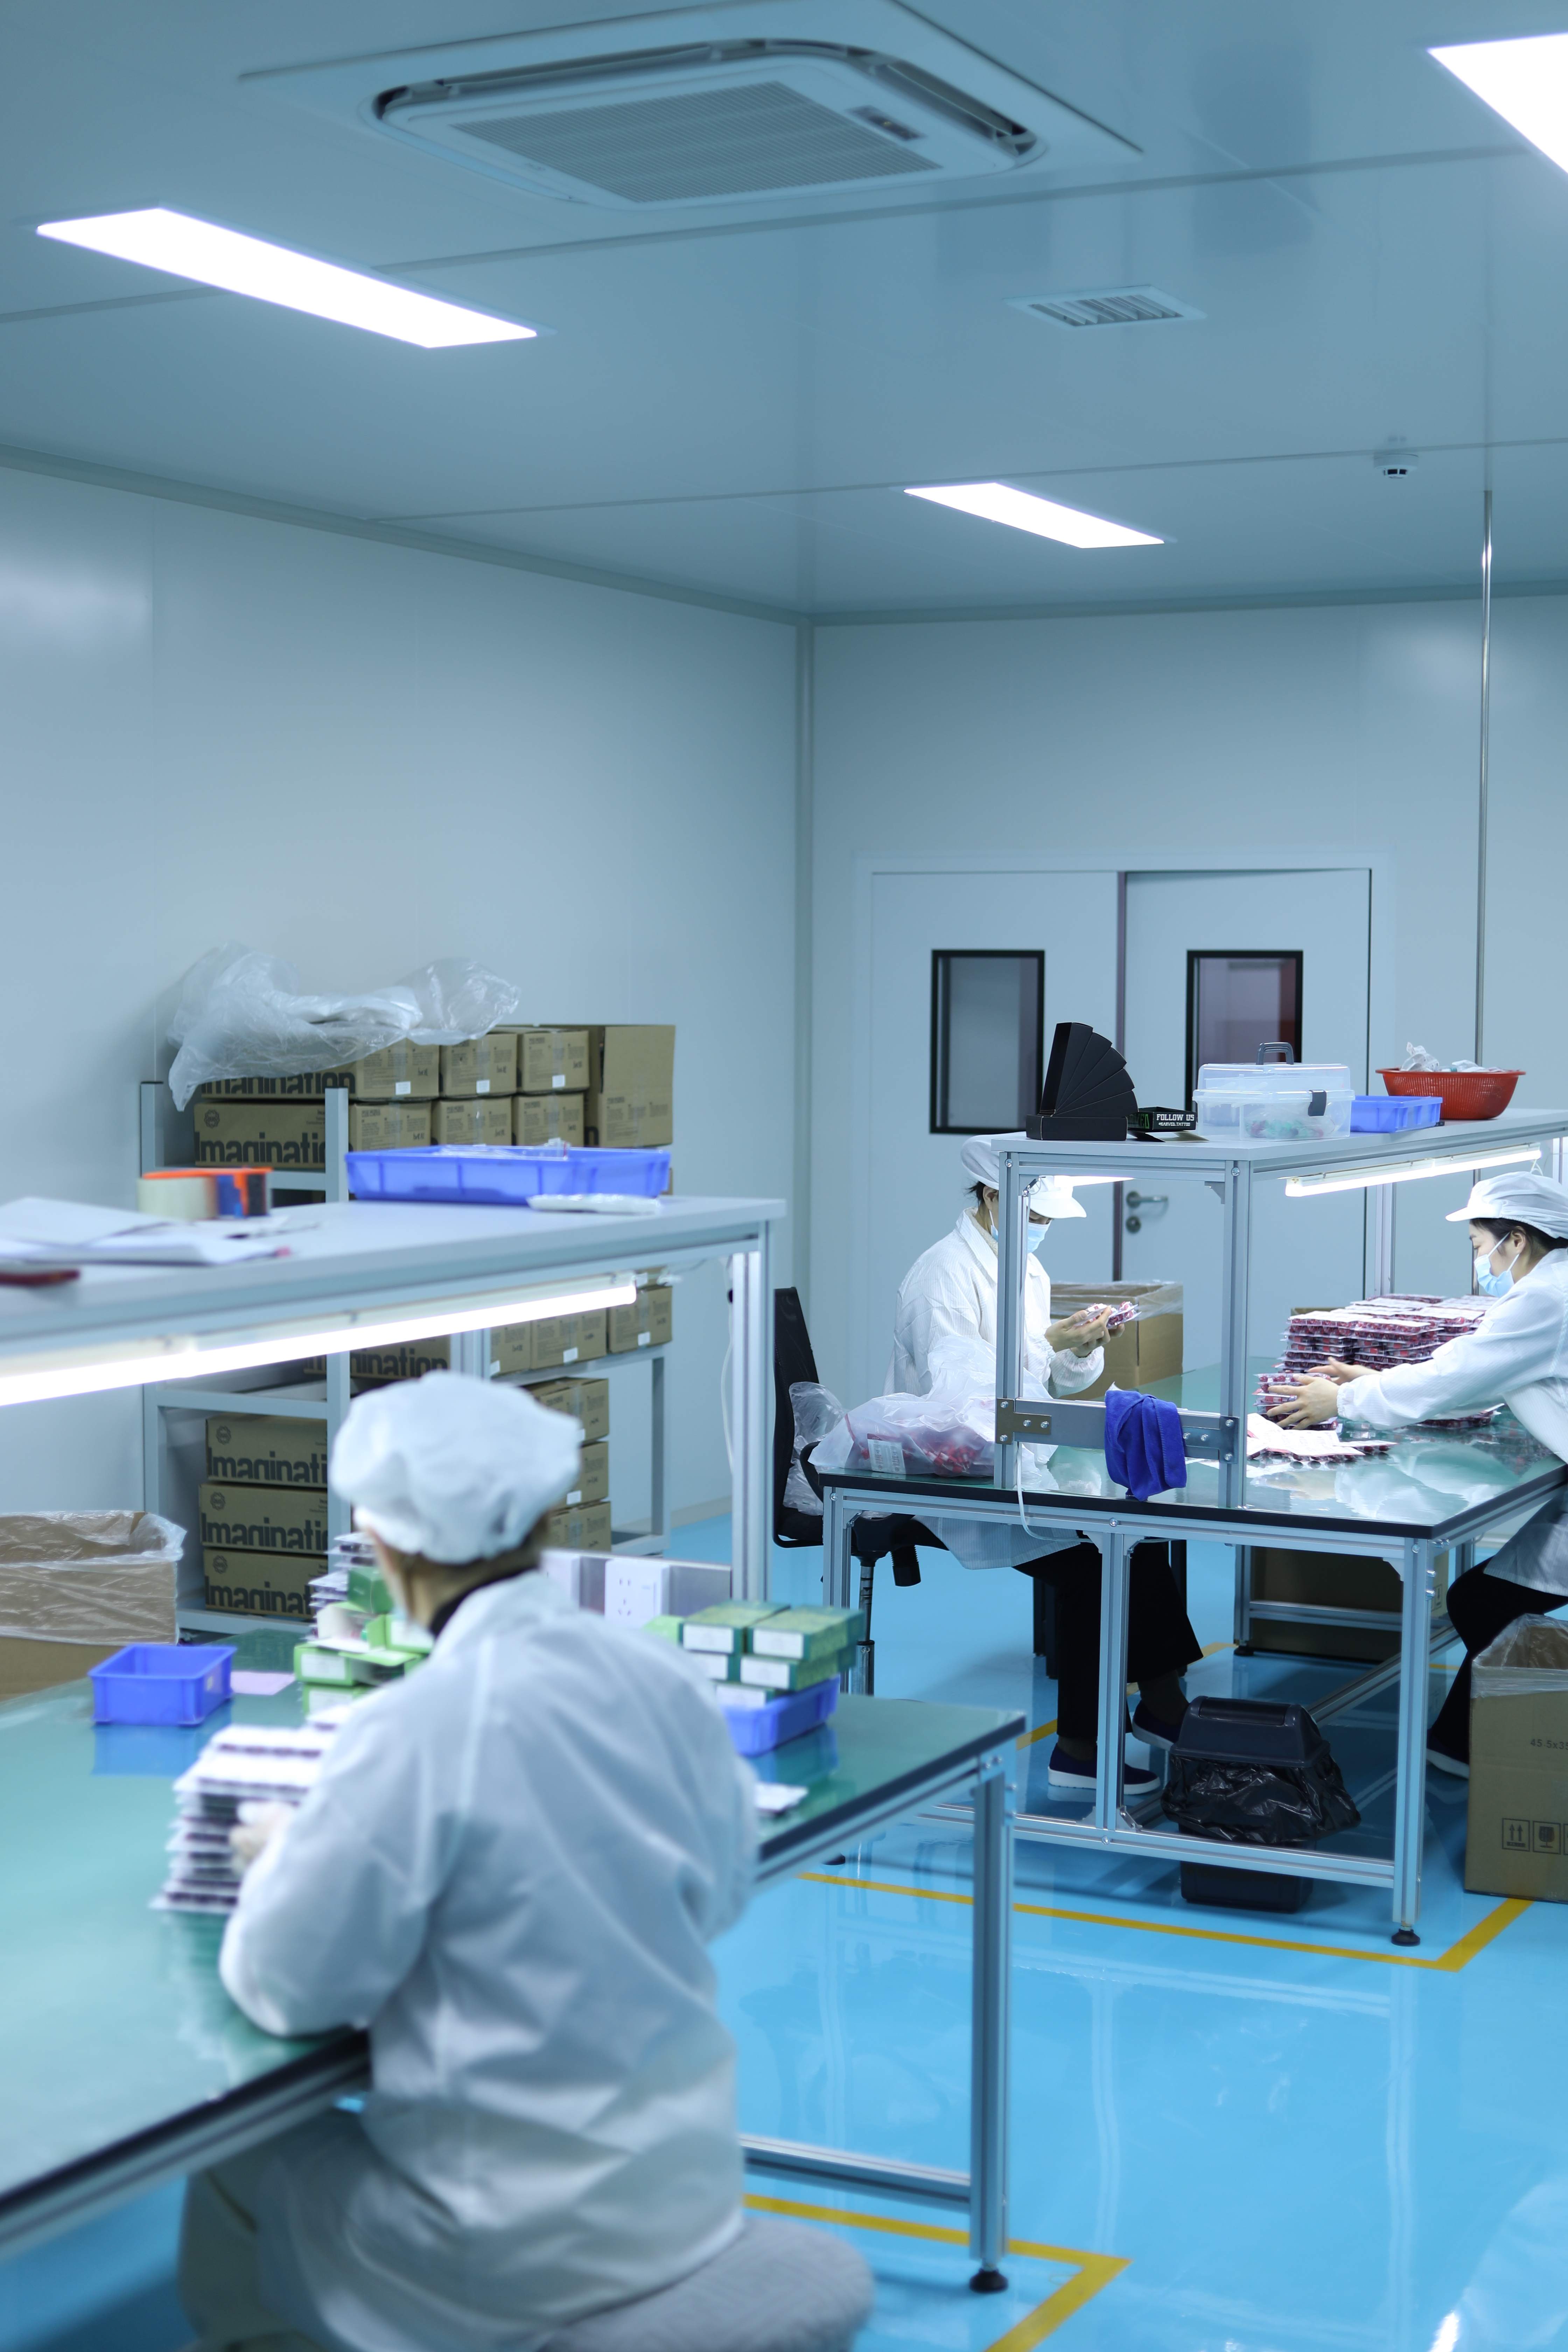
Suzhou Creditech Electronic Technology Co., Ltd., which markets its cartridge products under the Creditech Med name, is a Suzhou-based manufacturer founded in 2009 that develops, produces and exports tattoo cartridge needles, PMU cartridges and tattoo consumables. Roughly 90% of its output is exported, with Europe, North America, South America and Southeast Asia as its main markets.
Within that range, the SP5, HM3 and HM6 models are published with the same parameter set. The table below reproduces it as documented.
| Parameter | Documented value — SP5 / HM3 / HM6 |
|---|---|
| Needle diameter | 0.15 mm, 0.20 mm, 0.25 mm, 0.30 mm, 0.35 mm |
| Taper length | 1.5 mm – 7 mm (extra long taper available) |
| Precision tolerance | ±0.02–0.05 mm |
| Configurations | RL, RS, RM, Magnum, Flat |
| Membrane system | Silicone anti-backflow membrane |
| Needle material | Medical-grade stainless steel |
| Housing material | Medical-grade PC |
| Tip | Non-toxic transparent plastic tip |
| Ink delivery | Stable controlled ink delivery system |
| Vibration | Low vibration design |
| Sterilization | EO gas sterilized |
| Packaging | Sterile breathable film packaging system |
| Compatibility | Compatible with rotary tattoo machines |
Two points matter when reading this table as a buyer. First, it is a range specification rather than a fixed SKU: a 0.15 mm needle and a 0.35 mm needle belong to the same documented family but perform differently, and the buyer selects within the range rather than accepting a default. Second, the tolerance figure of ±0.02–0.05 mm is a documented manufacturing tolerance band; it is not a per-unit measurement certificate for every cartridge in a box.
Model positioning: what the data supports, and what it does not
Answer first: in the available specification data, SP5, HM3 and HM6 are documented with identical parameters, materials, sterilization method, packaging system, compatibility statement and tolerance. No model-level difference in diameter range, taper range, membrane design or vibration behavior is stated.
That matters because model codes invite assumptions. A buyer comparing SP5 against HM6 may reasonably expect the code to encode a performance tier — a stiffer needle, a different housing, a narrower tolerance band. The published specification set does not support that reading, and this article will not manufacture the difference. The defensible interpretation is that the model codes function as product-family designations inside the same technical envelope, and that selection should be driven by the parameters that are documented: diameter, taper, configuration and packaging, with any model-specific behavior confirmed on samples.
Practical consequence: if a project genuinely requires a documented distinction between SP5, HM3 and HM6, that distinction has to come from a model-specific datasheet and from side-by-side sample testing. It cannot be inferred from the shared specification table.
Diameter, taper and tolerance: the three numbers that decide project fit
Needle diameter: 0.15 mm to 0.35 mm
Five diameters are documented: 0.15 mm, 0.20 mm, 0.25 mm, 0.30 mm and 0.35 mm. In conventional industry usage, thinner gauges are associated with fine line and cosmetic work, where a narrow line and limited skin disturbance are the objective, while thicker gauges are associated with lining, shading and color packing, where the needle has to carry and deposit more ink per pass. That is a description of how diameter affects the working end, not a product-specific performance claim.
Taper length: 1.5 mm to 7 mm
Taper length is documented from 1.5 mm to 7 mm, with extra long taper available. Taper describes how far the needle grinds down toward the point. Longer tapers are conventionally associated with softer, more flexible tips and finer line control, which is why they appear in fine line and PMU work; shorter tapers are conventionally associated with a firmer tip and faster, more directional ink deposit, which suits lining and dense packing. For a buyer, the practical question is whether the required taper and configuration combination exists in the ordered diameter — the documented range is broad, but the specification table does not enumerate every valid combination, so unusual pairings should be confirmed in writing.
Precision tolerance: ±0.02–0.05 mm
Tolerance is the parameter most often skimmed and most often regretted. It governs consistency between cartridges in the same box. Where tolerance drifts, the visible symptom for an artist is variable line weight and slightly different ink response between cartridges, which is difficult to attribute during a session and easy to attribute after a project. For a distributor, tolerance consistency is also a returns and complaint driver. The documented band for this range is ±0.02–0.05 mm.
Configurations: RL, RS, RM, Magnum and Flat
The documented configurations are RL, RS, RM, Magnum and Flat. In conventional industry usage: RL (round liner) groups needles in a tight circular cluster for outlines and solid lines; RS (round shader) spreads them slightly for soft shading and blending; RM (round magnum) combines a round footprint with a wider grouping for coverage work; Magnum configurations, including the documented Soft Edge Magnum type, are used for color packing and broad shading; and Flat configurations present the needles in a flat line for flat, edge-based work.
The documented product-type list extends beyond configuration alone and includes Fine Line Tattoo Cartridge Needle, Traditional Tattoo Cartridge Needle, Shading Cartridge Needle, Color Packing Cartridge Needle, PMU Eyebrow Needle Cartridge, SMP Scalp Micropigmentation Needle, Long Taper Precision Needle and Soft Edge Magnum Needle. A procurement list that mixes configuration codes with application names will produce duplicates; buyers are better served by fixing configuration, diameter and taper as the three ordering variables.
Materials, membrane and fluid control
The documented material set is medical-grade stainless steel needles, a medical-grade PC housing, a silicone elastic membrane system, a non-toxic transparent plastic tip, and EO sterilization packaging material. The functional element buyers ask about most is the silicone anti-backflow membrane, which sits in the ink path as a barrier intended to limit backflow of ink and fluids toward the machine side of the cartridge.
Two further documented characteristics interact with the membrane: a stable controlled ink delivery system and a low vibration design. For an artist, that combination is experienced as predictable ink flow and a steadier hand-feel during long sessions; for a buyer, it is the reason a membrane cartridge is specified separately from a non-membrane cartridge in mixed studio orders. The membrane is a design feature documented by the manufacturer, not a clinical claim, and its role should be described to end users in those terms.
Sterilization, packaging and single-use handling
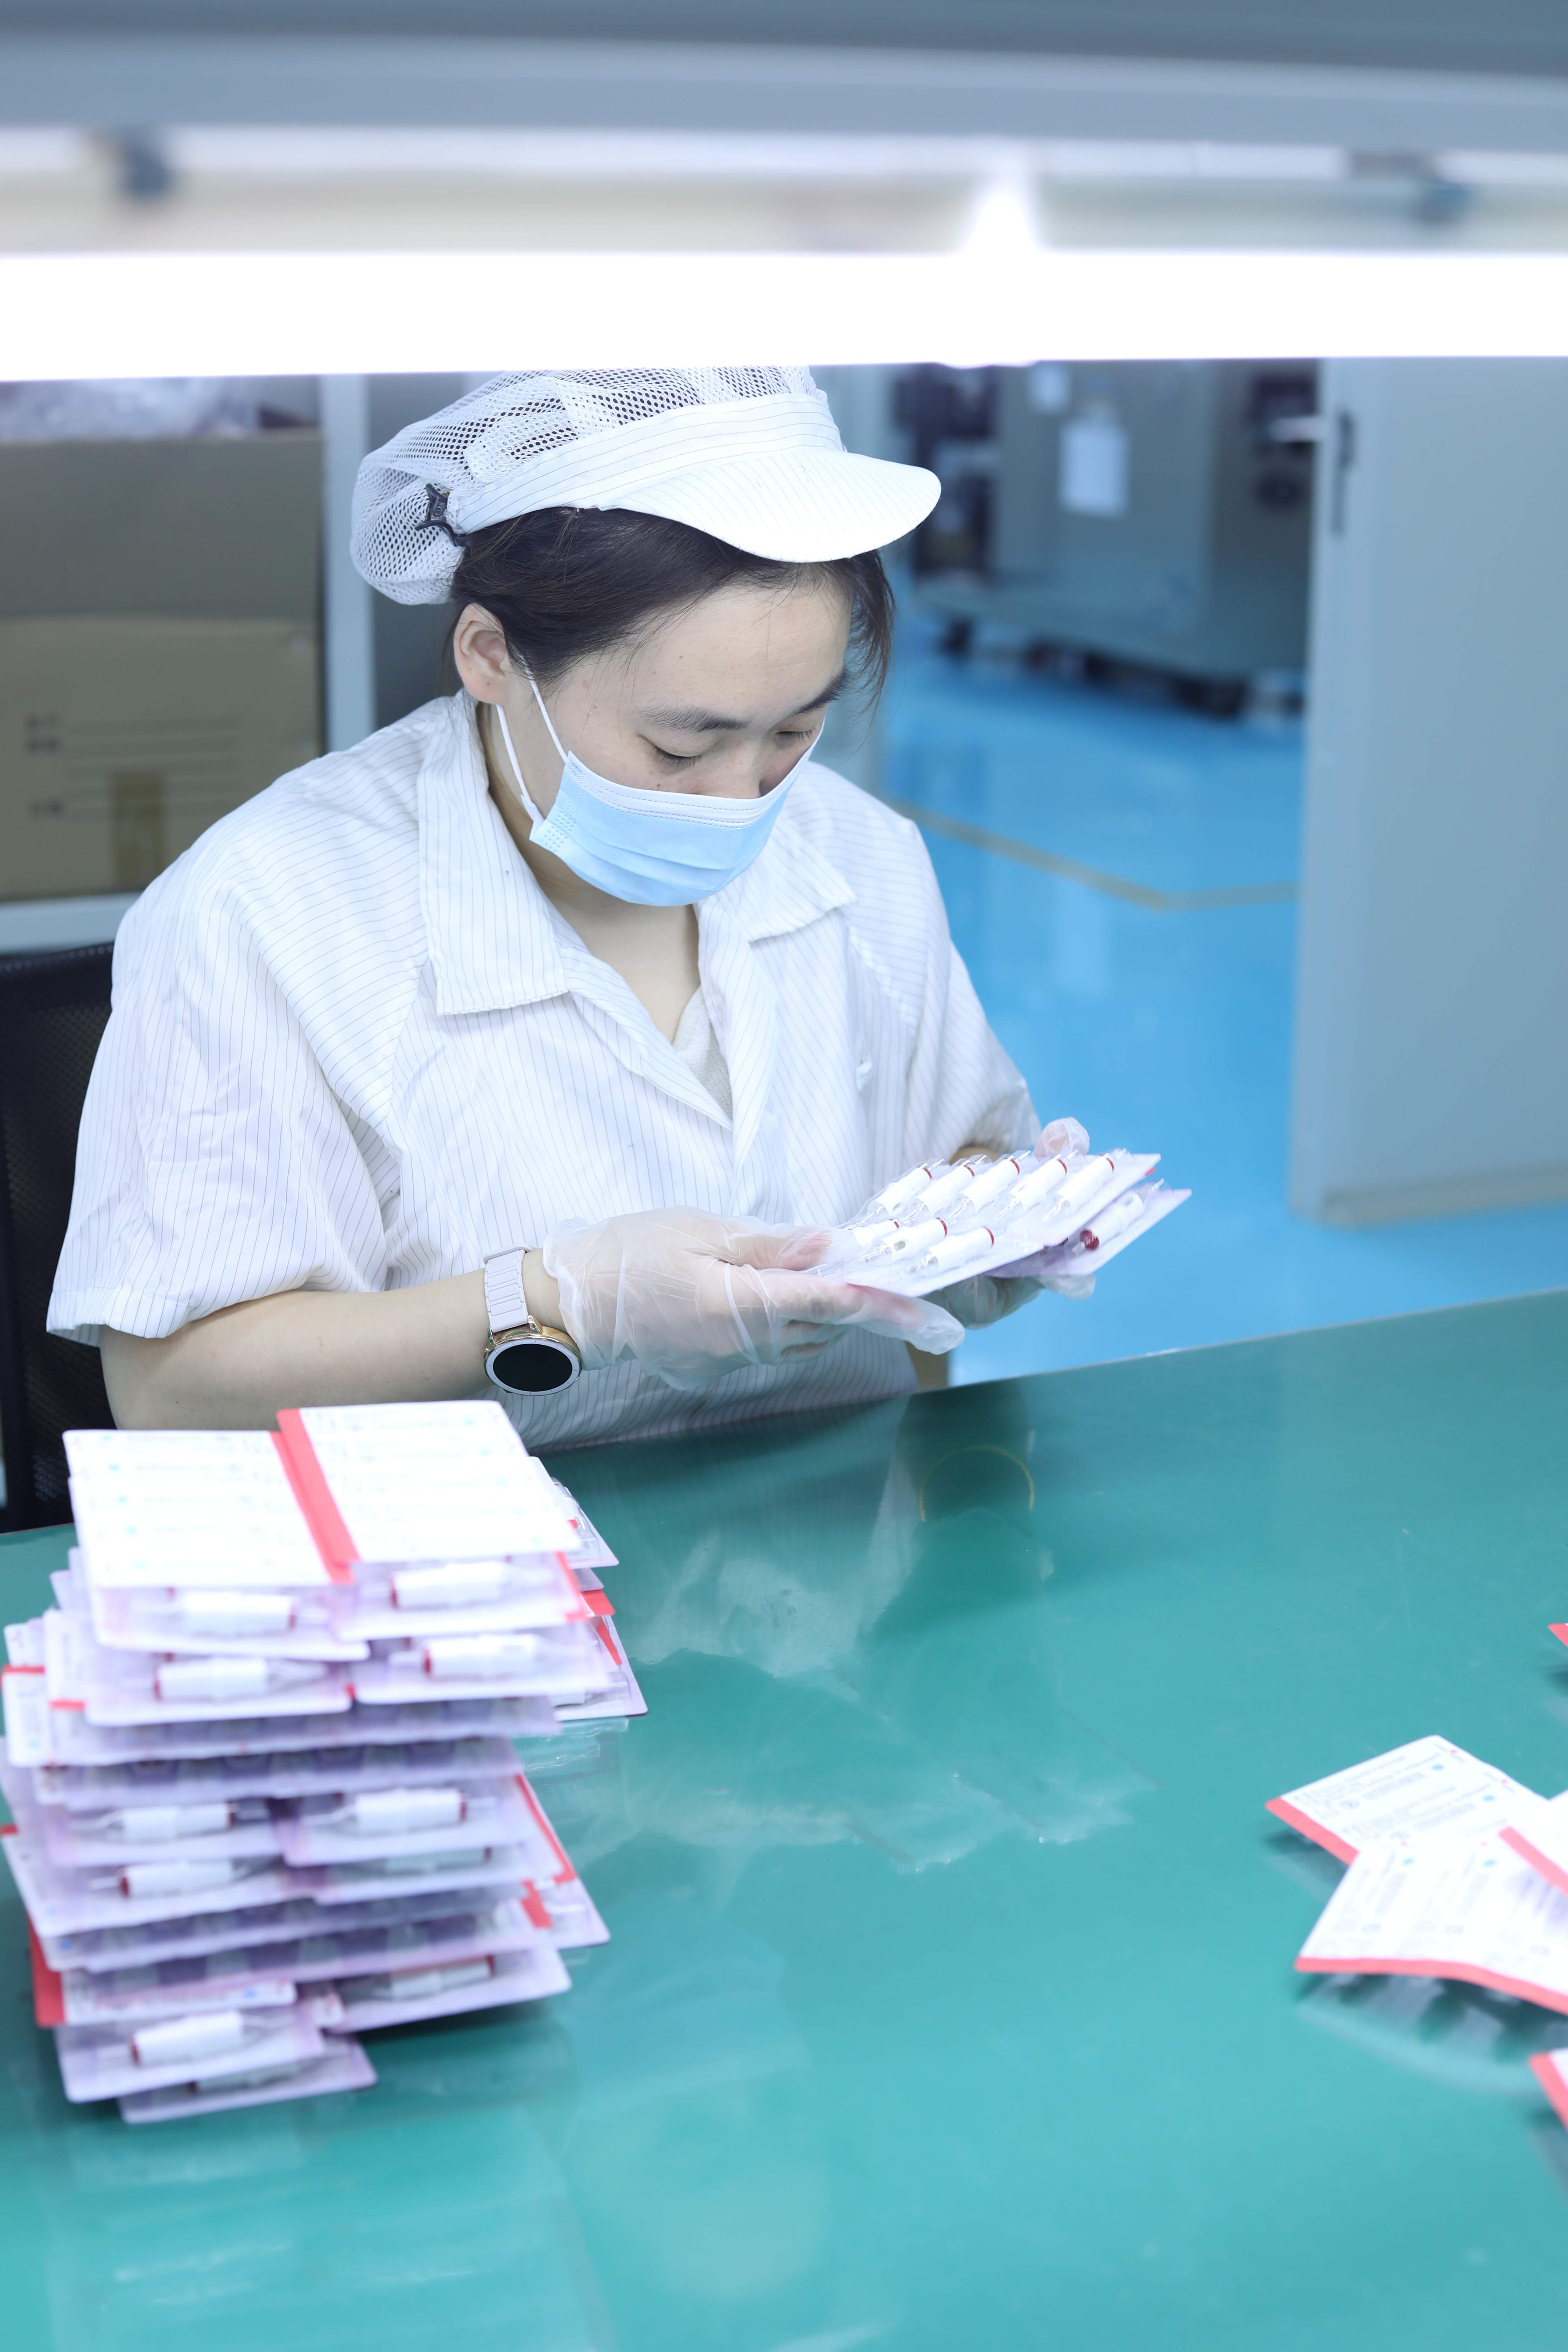
These cartridges are EO gas sterilized and packed in a sterile breathable film packaging system. The documented use case is single-use, with EO sterilization packaging material listed in the material set.
Ethylene oxide sterilization is a low-temperature process, which is why it is used for assembled devices that combine stainless steel, polycarbonate and silicone, as this range does. For the buyer, three handling points follow from the documentation rather than from assumption: packaging integrity should be inspected on receipt because the breathable film is the sterile barrier; batch traceability should be retained so that a sterilization batch can be linked to the shipped units; and storage conditions should keep the breathable film intact and dry. Sterilization validation documentation is a separate procurement item from the sterilization method statement.
Where the specification fits: documented applications and working conditions
The documented operating context is high-frequency continuous tattooing, with rotary tattoo machines as the compatible machine type and rotary tattoo machine, tattoo power supply, tattoo ink and cartridge grip listed as matched equipment.
Documented user categories include professional tattoo studios; tattoo artists working in fine line, realism and color work; PMU studios covering eyebrow, lip and eyeliner procedures; SMP clinics performing scalp micropigmentation; tattoo supply distributors; OEM tattoo brands; e-commerce tattoo supply retail; the permanent makeup and cosmetic tattoo industries; the medical aesthetic industry; training academies; and private label brands. Reference markets for the application data include the United States, Italy, Spain, France, the United Kingdom, Germany, Mexico, Colombia, Brazil, India, Indonesia and Thailand.
Reading that list as a procurement manager, the practical conclusion is that one cartridge family is being asked to serve four different usage profiles: high-detail cosmetic work, dense professional tattoo work, high-frequency throughput, and distribution-level resale. Diameter, taper and configuration are the variables that separate those profiles; the model code is not.
Market trend analysis: cartridge demand, PMU growth and compliance pressure
The global tattoo needle market was estimated at USD 368.3 million in 2024 and projected to reach USD 468.6 million by 2033 (CMI, Custom Market Insights). That figure should be read with its divergence in view: other research houses put the 2023 base at USD 289.8 million and USD 278.16 million respectively, a spread that reflects different definitions of whether traditional bar needles or cartridge-only segments are included. Buyers using market sizing in a business case should state the definition they are using.
Within the category, cartridges hold the largest share by product type, attributed to sterility and compatibility with modern rotary machines (Deep Market Insights). Adjacent demand is coming from cosmetic procedures: the permanent makeup market was valued at USD 162.09 million in 2025, with an 8.12% CAGR forecast for the needle-heavy microblading segment (Fortune Business Insights) — the segment that consumes fine line and long taper cartridges.
Supply-side context matters for sourcing decisions. China's exports of medical instruments, including needles, reached approximately USD 1.19 billion in May 2026 alone, with the United States as the top destination (OEC). Named global players in the tattoo needle market include Dragonhawk, Kwadron, Bishop Rotary, Cheyenne and EZ Tattoo Supply (CMI), which means brand-level competition is concentrated in the same cartridge format that OEM suppliers produce. Compliance pressure is moving in parallel: medical-grade needle manufacturing is assessed against the ISO 13485:2016 quality management standard, and cartridges sold into the EU fall under RoHS Directive 2011/65/EU, commonly referred to as RoHS 2.0, with EN IEC 63000:2018 frequently used for hazardous substance assessment.
Cartridge needles versus traditional bar needles
The comparison is usually framed as cost per needle, which is the least useful frame. The more useful frame is where the cost and the risk sit.
| Dimension | Cartridge needle | Traditional bar needle |
|---|---|---|
| Sterilization | EO gas sterilized as a sealed unit; sterile barrier is the packaging film | Sterilization responsibility sits with the studio and its equipment |
| Setup and change | Single-use cartridge seated in a grip; change is a cartridge swap | Requires assembly onto a bar and grip |
| Fluid control | Silicone anti-backflow membrane between ink path and machine side | No integrated membrane in the traditional format |
| Machine type | Documented as compatible with rotary tattoo machines | Format historically associated with coil and rotary setups |
| Unit cost | Generally the higher unit price of the two formats | Generally the lower unit price of the two formats |
| Consistency of supply | Dependent on supplier capacity, MOQ and lead time | Dependent on supplier capacity and studio sterilization workflow |
Three limitations should be stated plainly, because they are the points where a specification table can mislead a project team.
- Model codes are not performance grades. SP5, HM3 and HM6 share one documented parameter set. Any tiering between them is not supported by the available data.
- Compatibility is documented for rotary tattoo machines. Coil machine users, or studios using non-standard grips, should confirm fit before placing a volume order.
- Commercial floors apply. Minimum order quantity is documented at 500–1,000 pcs per size, with lead times of 15–30 days for standard orders and 30–45 days for custom OEM orders. Small trial orders and large private label programs follow different timelines.
A fourth boundary is worth noting for project planning: the specification is published as ranges. A buyer who needs a fixed-value specification, for example one exact diameter with one exact taper, is specifying a SKU, and that SKU should be confirmed by the supplier rather than derived from the range table.
OEM and procurement parameters
For buyers evaluating Creditech Med as a cartridge supplier rather than as a product, the documented procurement profile is the part of the specification that determines feasibility.
| Procurement parameter | Documented value |
|---|---|
| Production mode | OEM, ODM, custom manufacturing, private label |
| Monthly capacity | 3,000,000+ cartridge needles per month |
| Annual output | 100,000,000 units |
| MOQ | 500–1,000 pcs per size |
| Lead time | 15–30 days (standard); 30–45 days (custom OEM) |
| Quality control | ISO 13485 quality management, 100% inspection, EO sterilization, batch traceability |
| Customization | Custom logo, private label, custom packaging, needle configuration, housing design, new product development |
| After-sales | Technical support, OEM engineering support, product improvement, after-sales service |
| Export markets | USA, Germany, UK, France, Brazil, Mexico, Colombia, Canada, Australia |
The company's documented capacity profile includes 180 employees and a 20-engineer R&D team, which is the resource base behind the customization list. Two documented customer references illustrate the two most common project shapes. A private label branding and custom housing design customer in Mexico has taken 3,000,000+ cartridge needles per year over a five-year relationship, with OEM development, private label, fast sample development, stable supply chain and batch traceability as the defining features of the cooperation. A tattoo and PMU supply wholesaler in Spain has also worked with the supplier over a five-year period, serving professional tattoo studios and permanent makeup applications, with stable quality, long-term supply and consistent repurchase reported.
Future outlook
Three directions are visible from the documented data. First, the cartridge format is not a transitional product: it holds the largest share of the needle market by product type, and the professional artist preference data points the same way. Second, demand is broadening beyond professional tattoo work into cosmetic procedures, with the permanent makeup market projected to grow and the microblading segment — a needle-intensive segment — forecast at an 8.12% CAGR. Third, compliance documentation is becoming a purchasing requirement rather than a marketing asset: ISO 13485:2016 quality management, RoHS Directive 2011/65/EU alignment for EU sales, and per-product test reports are increasingly requested at the quotation stage rather than after order placement.
For buyers, the practical implication is that supplier selection will hinge less on a model code and more on documented ranges, documented capacity, and the willingness to state limits precisely. Suppliers who publish their tolerances, MOQ floors and lead times will be easier to qualify than those who publish positioning claims.
Frequently asked questions
1. What specifications are documented for the SP5 tattoo cartridge needle, and do HM3 and HM6 differ?
SP5, HM3 and HM6 are published with the same parameter set: needle diameters of 0.15 mm, 0.20 mm, 0.25 mm, 0.30 mm and 0.35 mm; taper length from 1.5 mm to 7 mm with extra long taper available; configurations RL, RS, RM, Magnum and Flat; a silicone anti-backflow membrane; medical-grade stainless steel needles in a medical-grade PC housing; EO gas sterilization; sterile breathable film packaging; compatibility with rotary tattoo machines; and a precision tolerance of ±0.02–0.05 mm. No difference in these parameters between the three models is stated in the available data.
2. How should a buyer choose between 0.15 mm and 0.35 mm needle diameters?
The choice follows the procedure rather than the model. Thinner diameters in the documented 0.15–0.35 mm range are conventionally used where a narrow line and limited skin disturbance matter, which covers fine line tattoo work and PMU procedures such as eyebrow, lip and eyeliner. Thicker diameters are conventionally used where more ink must be carried and deposited per pass, which covers lining, shading and color packing. Because the same diameter range spans all five models, diameter can be specified independently of the model code.
3. When does taper length matter more than needle diameter?
Taper length matters when line quality and tip behavior are the limiting factor rather than ink volume. The documented taper range is 1.5 mm to 7 mm, with extra long taper available. Longer tapers are conventionally associated with finer, more flexible tips for detail and cosmetic work; shorter tapers with firmer tips for directional lining and dense packing. A project that already has the correct diameter but produces inconsistent line character is usually a taper specification question, not a diameter question.
4. Which configurations — RL, RS, RM, Magnum, Flat — suit which work?
The documented configurations are RL, RS, RM, Magnum and Flat. In conventional industry usage, RL round liner configurations are used for outlines and solid lines, RS round shader configurations for softening and blending, RM round magnum for coverage work, Magnum and Soft Edge Magnum configurations for color packing and broad shading, and Flat configurations for flat, edge-based work. The documented product-type list also includes Fine Line, Shading, Color Packing, PMU Eyebrow, SMP Scalp Micropigmentation and Long Taper Precision variants.
5. What does the silicone anti-backflow membrane do?
The silicone membrane is documented as a membrane system within the cartridge and is described as an anti-backflow membrane. Its position in the ink path makes it a barrier intended to limit movement of ink and fluids toward the machine side of the cartridge during use. It is documented alongside a stable controlled ink delivery system and a low vibration design, and it is one of the reasons membrane cartridges are specified separately from non-membrane cartridges in mixed orders.
6. How are these cartridges sterilized and packaged, and what does that mean for handling?
The cartridges are EO gas sterilized and supplied in a sterile breathable film packaging system, with the product documented as single-use. Because the breathable film is the sterile barrier, packaging integrity should be inspected on receipt, batch information should be retained for traceability, and storage should keep the film intact and dry. Ethylene oxide is a low-temperature sterilization method, which suits assembled devices combining stainless steel, polycarbonate and silicone such as these.
7. Are these cartridges compatible with coil machines or only rotary machines?
Compatibility is documented for rotary tattoo machines, and rotary tattoo machine, tattoo power supply, tattoo ink and cartridge grip are listed as the matched equipment for the documented applications. Compatibility with coil machines or with non-standard grip designs is not part of the documented statement and should be confirmed for the specific machine and grip before a volume order is placed.
8. Which compliance documents are documented, and how should FDA, CE and RoHS claims be verified?
The documented compliance position is an ISO 13485 certified quality management system, CE compliant products, and FDA test reports available for applicable products. For EU sales, tattoo needle cartridges fall under RoHS Directive 2011/65/EU, commonly referred to as RoHS 2.0, with EN IEC 63000:2018 frequently used for hazardous substance assessment. The phrase “applicable products” matters: buyers should request the declaration and test reports for the exact SKU and configuration being ordered, and confirm the scope of any CE documentation for the specific item and destination market. Safety data sheet availability is product-specific and should be requested per item rather than assumed from a quality management certificate.
9. What are the documented MOQ, lead time and OEM customization terms?
Minimum order quantity is documented at 500–1,000 pcs per size. Lead time is 15–30 days for standard orders and 30–45 days for custom OEM orders. Documented monthly capacity is 3,000,000+ cartridge needles per month. Customization covers custom logo, private label, custom packaging, needle configuration, housing design and new product development, supported by a 20-engineer R&D team and after-sales support that includes OEM engineering support and product improvement.
10. How should a distributor validate a cartridge supplier before mass production?
Validation should follow the documented parameters rather than the model naming. Practical steps are: confirm the exact diameter, taper and configuration in writing; request the model-specific datasheet if model differentiation matters to the project; request compliance documents for the exact SKU, including ISO 13485 quality management evidence, CE documentation where applicable, and FDA test reports for applicable products; verify MOQ, lead time and capacity against the annual requirement; and run a sample batch against the documented ±0.02–0.05 mm tolerance before committing to volume. Batch traceability and EO sterilization records should be part of the same check, since they are the evidence that ties a shipment to a production run.
Reference note
This FAQ reflects the specification and procurement data published for the Creditech Med cartridge range as of September 2026. Where the available data does not support a distinction — most notably between the SP5, HM3 and HM6 model codes — the article states the gap rather than filling it. Buyers requiring fixed-value specifications or model-specific performance data should obtain the corresponding datasheet directly. The Creditech Med company brochure is available for download: Creditech Med company brochure.