
Thermoforming Plastic Parts: The Constraint Checklist
Thermoformed plastic parts are constrained long before they are priced. In most industrial RFQs, the limits that decide whether a project is feasible — maximum forming size, sheet thickness, available material grades, and the scope of a supplier's certification — are settled well before commercial terms are discussed. Buyers who treat these four items as verifiable constraints receive comparable quotations. Buyers who treat them as background detail end up comparing numbers that were never measured against the same envelope.
Why Thermoforming Constraints Matter More Than Process Claims
Vacuum forming shapes a heated thermoplastic sheet against a mold using vacuum pressure. Because the sheet is stretched rather than injected, the process operates inside a wide but finite window. Sheet thickness, part size, material grade and tooling are not independent variables — they behave as a coupled system. Widen the part, and the thickness the process can handle changes. Move to a stiffer or more weather-resistant polymer, and the forming behaviour changes with it.
The procurement consequence is straightforward. Two suppliers can both describe themselves as offering custom vacuum forming and still be quoting against different envelopes. One may form parts up to roughly a metre; another may form panels several metres across. One may hold only commodity grades; another may hold flame-retardant and composite options. Read without the constraint layer, both quotations look like prices. Read with it, they describe different products.
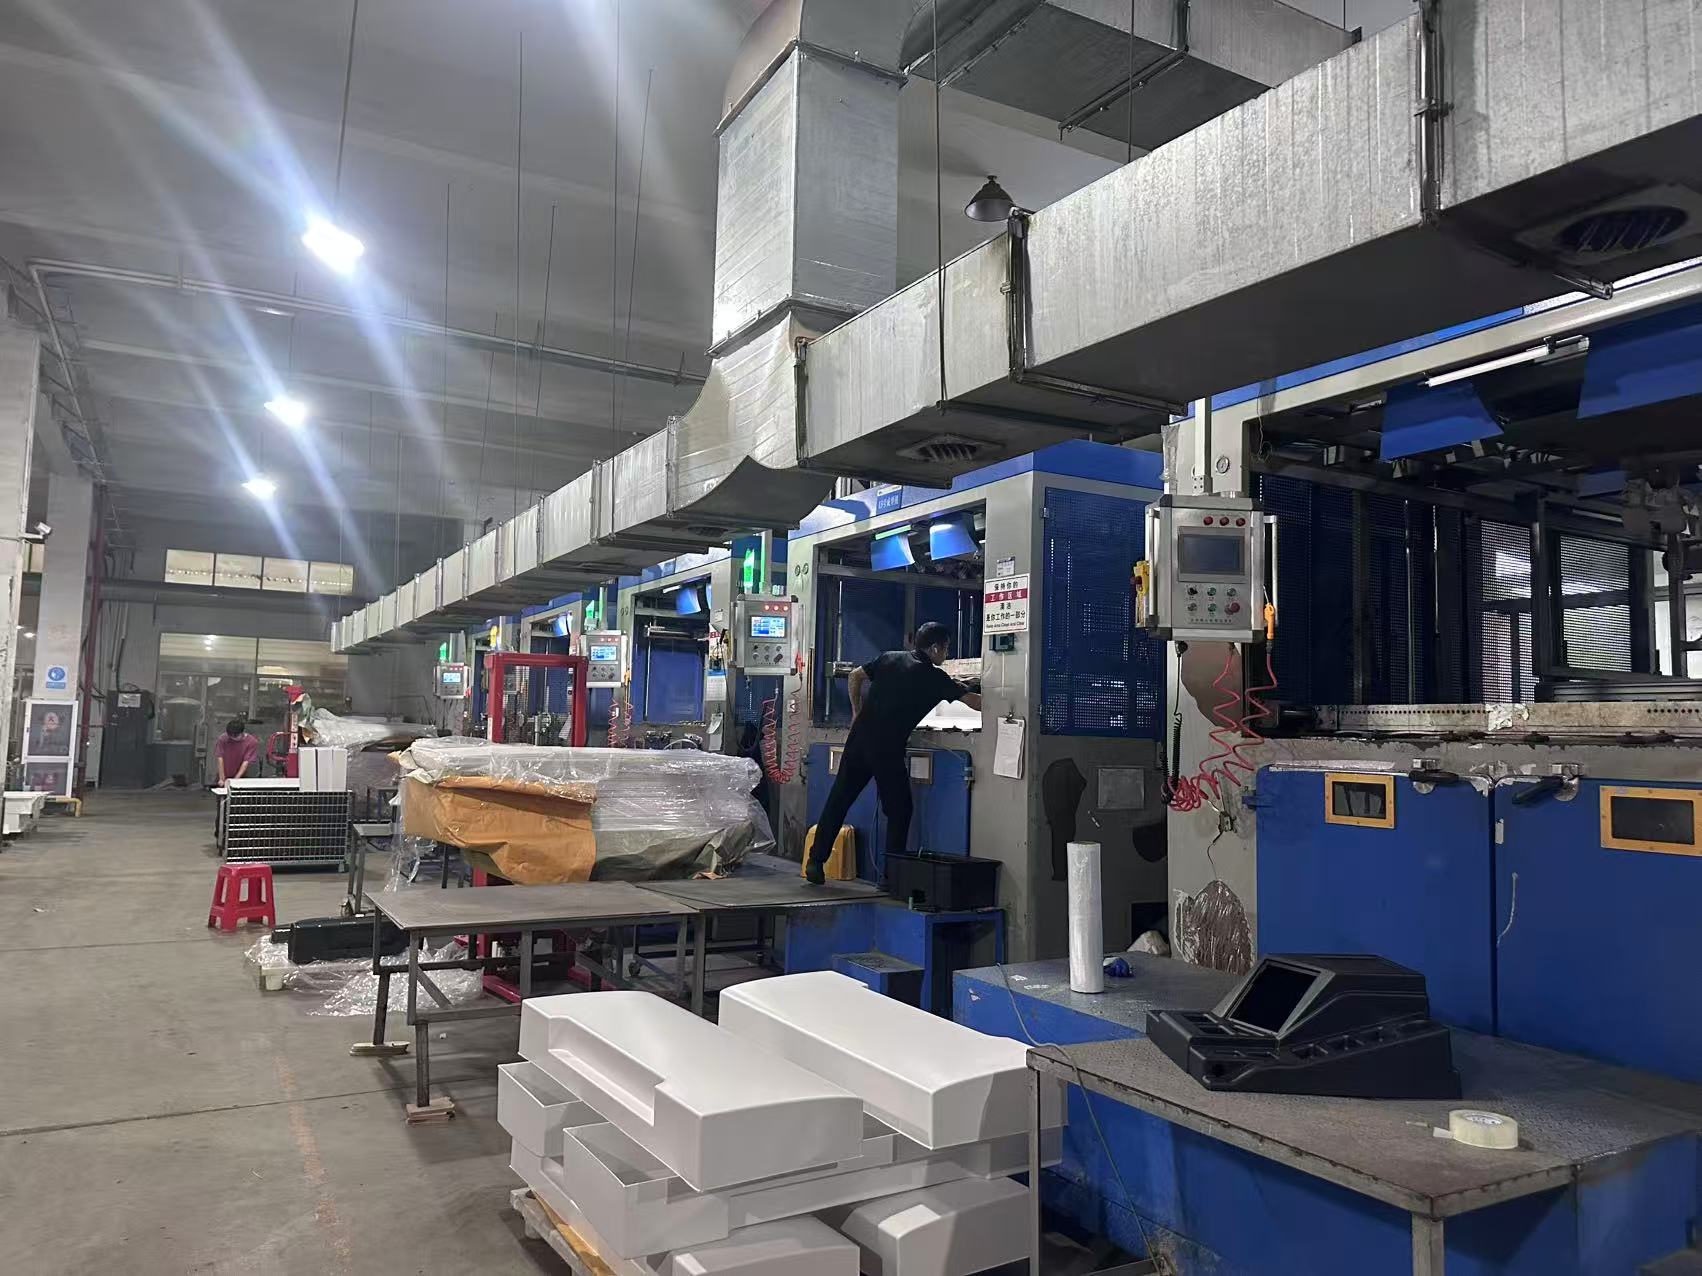
Hangzhou Baiheli New Materials Co., Ltd. is a heavy-gauge thermoforming processor located in Guali Town, Xiaoshan District, Hangzhou, China. Founded in 2011, the company operates a factory of approximately 10,000 square meters with 90 employees and a five-person R&D team, and produces thick-sheet thermoformed housings, covers, panels and structural components for industrial equipment, automotive, medical, logistics and outdoor applications. Its processing chain runs from sheet extrusion through thermoforming to five-axis cutting and surface finishing — which is why its constraints are best read as a chain of limits rather than as a single headline capability.
The Four Constraint Fields That Decide a Thermoforming RFQ
Most avoidable procurement errors in custom thermoforming trace back to a missing or loosely worded constraint. The table below lists the four fields that should appear in any serious request for quotation, plus the evidence a buyer should expect to receive in return.
| Constraint field | Question the buyer should ask | What counts as usable evidence |
|---|---|---|
| Forming envelope | What is the maximum part size the equipment and tooling can form? | A stated maximum forming size in millimetres, not an adjective such as "large" |
| Sheet thickness | Which sheet thickness range can be formed reliably for this geometry? | A stated thickness range in millimetres, matched to the material grade |
| Material grade | Which polymers and grades are actually available, including flame-retardant options? | A named material list rather than a generic "engineering plastics" statement |
| Certification scope | Which processes and products does the certificate cover, and until when? | Certificate number, issuing body, validity dates and the certified scope text |
Tooling position, minimum order quantity and lead time form a fifth, commercial layer. They are not technical constraints in the strict sense, but they decide which projects are economically viable — and they are frequently the reason a technically feasible part never reaches production.
Dimension Window: What Large Part Thermoforming Actually Covers
For Baiheli's vacuum thermoformed housing and automotive interior part ranges, the maximum forming size is 3300 mm × 2000 mm, and the large-size forming capacity is stated at the same 3300 mm × 2000 mm figure. That envelope is the practical boundary for covers, housings, door trim panels and similar panel-scale components formed in a single cycle.
Two clarifications matter when this number is transferred into a drawing. First, the forming envelope is not the finished-part envelope. A formed part is trimmed back to its final outline, usually by five-axis cutting, so the deliverable dimension is smaller than the sheet area consumed. Second, the envelope is a maximum, not a target. Parts that approach the full envelope place different demands on draw depth, wall thinning and mold support than parts at half that size.
The same envelope logic applies to thickness. Baiheli's stated sheet thickness range is 2 to 10 mm. Buyers working with thin-gauge assumptions — for example, packaging-scale material below 2 mm — should recognise that heavy-gauge thermoforming is a different discipline with different equipment, tooling and handling requirements.
Sheet Thickness and the Material Menu
The material list available for these thermoformed parts covers ABS, flame-retardant ABS, ASA, PC, PETG, PMMA, PVC, PE and other engineering or composite materials. Each entry in that list carries a different set of design implications.
- ABS and flame-retardant ABS — the general-purpose structural choice for housings and interior components. The flame-retardant grade exists as a separate option, but the specific fire rating required by a project must be confirmed at quotation stage rather than assumed.
- ASA — selected where colour and surface stability under outdoor exposure matter, such as equipment covers used outside factory buildings.
- PC — used where impact resistance or transparency is needed; transparent or translucent PC is listed as a project-specific option.
- PETG and PMMA — chosen for clarity, surface finish and formability in visible panels and guards.
- PVC and PE / HDPE — used where chemical exposure, moisture or abrasion dominate the operating environment.
Operating temperature for the finished applications is stated as −20 °C to 70 °C, with an optional UV-resistant surface for outdoor exposure. Those two figures are the ones most often missing from buyer specifications, and they are the ones that most often determine whether a standard grade will survive its service environment.
Beyond the sheet itself, the available surface and finishing routes include matte film, screen printing, masked painting and five-axis cutting for housing-fit features. Transparent, translucent and opaque finishes are all supported. What is not fixed in advance is the tolerance stack. Exact fire rating, UV-resistance rating, dimensional tolerances and assembly requirements require project confirmation — a limitation that should be written into the RFQ rather than settled after tooling is cut.
Certification: Read the Scope, Not the Logo
Certification is the constraint field most often handled superficially. A logo on a website indicates that a certificate exists; it does not indicate what the certificate covers. For buyers in regulated or safety-adjacent industries, the scope text is the operative document.
Baiheli holds ISO 9001:2015 Quality Management System certification, certificate number 98924Q00326R0M, issued by Guangdong Harmonious Certification Co., Ltd. (HCC). The certificate covers the production of plastic products, and it is valid from 2024-06-13 to 2027-06-12. The certified scope applies to vacuum formed plastic products for auto interior components. The underlying standard is GB/T 19001-2016 / ISO 9001:2015, and the certification is presented for global markets.
Three practical readings follow from those details. The validity window means the certificate is active at the time of writing but has a defined renewal horizon — buyers running multi-year programmes should record the expiry date rather than the issue date. The scope text ties the certification to plastic product production, which is the relevant activity for thermoformed housings and panels. And the issuing body is named, which allows independent verification rather than reliance on a supplier statement.
That limitation is not a defect in the supplier's offer — it is a boundary condition. Heavy-gauge thermoforming suppliers are frequently engaged for prototype and medium-batch automotive interior parts precisely because tooling investment is lower than injection molding; the certification path for those parts should be matched to the programme's regulatory route, not assumed from a general quality certificate.
Tooling, Minimum Order and Batch Economics
Low tooling cost applies to prototype and medium-batch production of these thermoformed parts. This is the structural reason the process competes in exactly the range where injection molding struggles: quantities that are too large for fabrication and too small to amortise a steel injection tool.
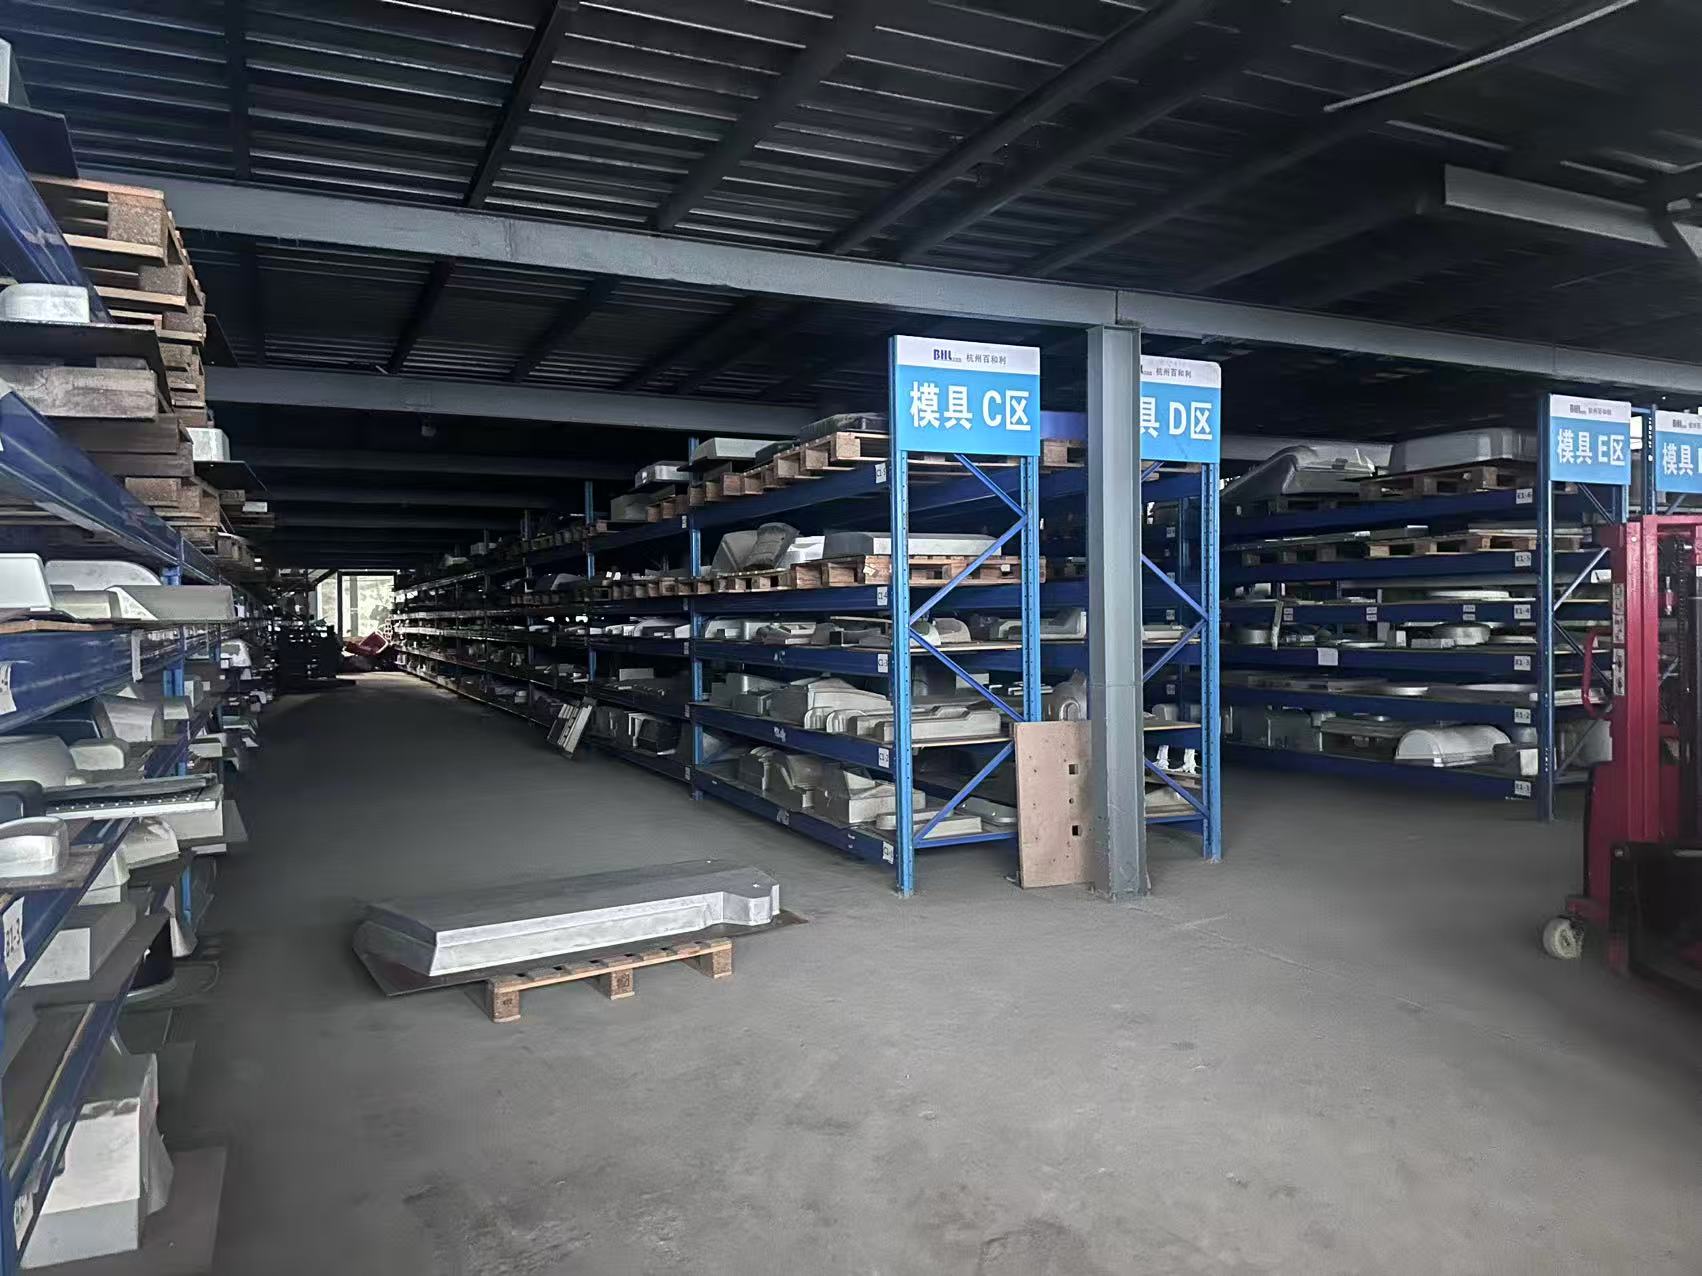
The supporting production parameters are: a minimum order quantity of 1 unit, a lead time of 25–30 days, monthly capacity of 80,000 units, and 100% testing. Production support explicitly includes prototype and medium-batch production. The company reports closing around 30 projects per year, with customer relationships running 3–5 years, and highlights an integrated processing chain that spans sheet extrusion, thermoforming, five-axis cutting and surface finishing across multiple engineering plastics and composites.
What these numbers mean for a buyer is a specific decision rule. Because the MOQ is 1 unit, the tooling decision can be made before the volume decision — a prototype can be formed and validated, and the same tool can then carry a medium batch. This sequencing is where thermoforming differs most sharply from injection molding, where the tool commitment and the volume commitment are effectively the same decision.
Where Thermoformed Plastic Parts Fit
Application fit in this category is defined by part scale and geometry rather than by industry label. The documented project types include custom equipment housings, automotive and new energy vehicle parts, AGV and robot housings, medical equipment housings, communication radomes, rooftop tent components and drone housings.
In logistics and robotics, AGV housings and robot covers are formed as large shells that must combine impact resistance with controlled surface appearance — a geometry that is expensive to injection mold at medium volumes. In automotive interiors, door trim panels and bumper covers are formed as panel-scale parts where low tooling cost supports prototype and medium-batch runs. In medical equipment, housings and covers are produced where cleanable surfaces and stable forming matter more than high-detail geometry. In textile machinery and intelligent equipment, protective covers and machine housings address enclosure, visibility and access requirements. Communication radomes and rooftop tent components rely on the same large-envelope capability under outdoor conditions, where the UV-resistant surface option and the −20 °C to 70 °C operating range become the governing specifications.
The common thread is that these are passive housings or covers that operate as part of a larger machine, vehicle or outdoor product. Their function is enclosure, protection, appearance and assembly fit — not precision mechanical motion. Buyers evaluating a thermoforming supplier for these roles should assess the supplier against enclosure requirements, not against the requirements of a machined component.
What the Market Data Says About Process Mix
Third-party market research places the global plastic vacuum forming market at USD 4.8 billion in 2023, with a forecast of USD 7.2 billion by 2030 (Grand View Research). The same source attributes a 40.7% share of that market to Asia Pacific in 2023 — a regional concentration that aligns with the density of large-part forming capacity in China.
Process segmentation adds a useful corrective to the way heavy-gauge work is often discussed. Mordor Intelligence reports that thin-gauge thermoforming, defined as material under 1.5 mm, accounted for 76.22% of the combined heavy/thin-gauge market in 2025. Thin-gauge volume — packaging, disposable formed products, light trays — dominates the market by revenue share.
The procurement interpretation is not that heavy-gauge work is marginal. It is that heavy-gauge work is a specialised branch of a large market, and the suppliers equipped for it are a minority of the supplier base. A buyer searching for a custom vacuum forming partner for a 3300 mm × 2000 mm housing and a buyer searching for a packaging former are, in practice, searching different industries that happen to share a process name. Market size figures describe the whole category; forming envelope, sheet thickness and material grade describe the sub-category a specific project actually belongs to.
Thermoforming Versus Injection Molding and Sheet Metal
Constraint-led evaluation only becomes useful when it is placed against the alternatives. The comparison below is deliberately framed around decision criteria rather than performance claims.
| Criterion | Thermoforming | Injection molding | Sheet metal |
|---|---|---|---|
| Tooling investment | Lower tooling cost for prototype and medium batch | Higher upfront tooling commitment | Moderate tooling for cutting and bending |
| Economic batch range | Prototype and medium batch | High volume, where tooling amortises | Low to medium volume |
| Part scale | Large panels and housings, up to the stated maximum forming size | Bounded by press and tooling | Large, but typically flat-oriented |
| Geometry | Open shells, covers, housings, trim panels | Complex, high-detail and closed geometry | Folded and flat-based structures |
| Surface routes | Textured sheet, matte film, screen printing, masked painting | Molded-in texture | Coating and powder finishing |
| Characteristic weak point | Deep draws and very small sharp features | Tooling lead time and cost at low volume | Compound curvature and enclosed forms |
The honest boundary is narrower than most supplier comparisons admit. Vacuum forming is poorly suited to parts that need tight tolerances across many small features, to closed hollow bodies, or to very high volumes where a steel injection tool would amortise. Deep draws relative to part footprint are a project-specific question rather than a fixed rule, and they are resolved by tooling trials rather than by catalogue figures.
A second constraint is capacity composition. A heavy-gauge former is equipped for large-sheet handling; a supplier optimised for thin-gauge packaging will not be able to substitute. A third is certification. Where a programme mandates IATF 16949:2016, an ISO 9001:2015-certified former does not meet that requirement without an additional qualification path. Buyers should treat all three as screening criteria, applied before samples are requested.
A Practical RFQ Checklist for Custom Thermoformed Plastic Parts
Feeding the right constraints into a quotation request shortens the loop considerably. The list below reflects the fields that must be resolved before a forming supplier can quote defensibly.
- Envelope check — confirm the part's outer dimensions sit inside the stated maximum forming size of 3300 mm × 2000 mm, and note whether the trimmed outline or the formed blank is the governing figure.
- Thickness and material — specify the polymer grade and the sheet thickness within the 2–10 mm range, and state explicitly whether a flame-retardant grade is required.
- Service environment — declare the operating temperature envelope relative to the −20 °C to 70 °C range, and whether UV-resistant surface treatment is needed for outdoor exposure.
- Surface and finishing — identify which finishing routes apply: matte film, screen printing, masked painting, or trimming only.
- Tolerance declaration — list the critical dimensions and assembly interfaces, and accept that exact tolerances require project confirmation rather than default assumptions.
- Certification route — state whether ISO 9001:2015 is sufficient or whether an automotive-specific standard such as IATF 16949:2016 applies to the programme.
- Volume staging — describe whether the first order is a prototype, a medium batch, or a ramp, given that MOQ starts at 1 unit and lead time runs 25–30 days.
A quotation that answers all seven items is comparable with another quotation that answers all seven. A quotation that answers three is a starting point for a conversation, not a basis for a sourcing decision.
Future Outlook
The direction of travel in this category is toward larger envelopes and more demanding material specifications rather than toward faster cycles. Electrification in vehicles, automation in logistics and the enclosure requirements of medical and communication equipment all push part sizes upward while tightening surface and weather-resistance expectations. Forecast growth from USD 4.8 billion in 2023 to USD 7.2 billion by 2030, with Asia Pacific already holding 40.7% of the market in 2023, suggests that capacity expansion will continue to concentrate where large-part forming capability already exists.
For buyers, the practical implication is that supplier differentiation will increasingly be read through documentation rather than through process description. A forming envelope in millimetres, a thickness range, a named material list and a certificate scope with validity dates are the four data points that will keep quotations comparable as the supplier base widens.
Frequently Asked Questions
What is the maximum forming size for thermoformed plastic parts?
The maximum forming size for the vacuum thermoformed housing and automotive interior part ranges is 3300 mm × 2000 mm, and the large-size forming capacity is stated at the same 3300 mm × 2000 mm figure. This is the upper limit of the forming envelope; the finished trimmed part is smaller than the formed blank.
What sheet thickness range can be thermoformed?
The stated sheet thickness range is 2 to 10 mm. This places the capability in the heavy-gauge thermoforming category rather than in thin-gauge forming, which typically handles material below 1.5 mm.
Which materials are available for these thermoformed parts?
The material options are ABS, flame-retardant ABS, ASA, PC, PETG, PMMA, PVC, PE and other engineering or composite materials. Transparent, translucent and opaque finishes are supported, and project-specific options include PC matte film, transparent or translucent PC and impact-resistant PE.
What does the ISO 9001:2015 certificate actually cover?
The certificate is numbered 98924Q00326R0M, issued by Guangdong Harmonious Certification Co., Ltd. (HCC), and valid from 2024-06-13 to 2027-06-12. Its certified scope is the production of plastic products, and it applies to vacuum formed plastic products for auto interior components. The underlying standard is GB/T 19001-2016 / ISO 9001:2015.
Is ISO 9001:2015 sufficient for automotive interior components?
It depends on the programme. ISO 9001:2015 is a quality management system certification, while IATF 16949:2016 is the mandatory quality standard for automotive supply chain members. Where a buyer's supplier approval process requires IATF 16949:2016, ISO 9001:2015 certification alone does not satisfy that requirement, and the gap should be confirmed at the RFQ stage.
What is the minimum order quantity and typical lead time?
The minimum order quantity is 1 unit and the lead time is 25–30 days. Monthly capacity is 80,000 units, quality control is 100% testing, and production support covers both prototype and medium-batch production.
When is thermoforming the wrong process choice?
Thermoforming is a poor fit for parts requiring tight tolerances across many small features, for closed hollow bodies, and for very high volumes where a steel injection mold would amortise its tooling cost. It is also unsuitable for parts exceeding the stated maximum forming size of 3300 mm × 2000 mm without segmentation or a different process route.
For buyers who need the full material list, forming envelope and processing chain in one reference document, the manufacturer's corporate brochure is available for download: Hangzhou Baiheli New Materials Co., Ltd. — Corporate Brochure (PDF).
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.