
Trigger Sprayer Qualification: Terms, Acceptance Criteria, Risk Checks
Industry Reference · Packaging & Printing
Trigger Sprayer Qualification: Terms, Acceptance Criteria, Risk Checks
Qualification is the step between an approved sample and a mass-production order. It is also the last point at which a buyer can still change the outcome at low cost.
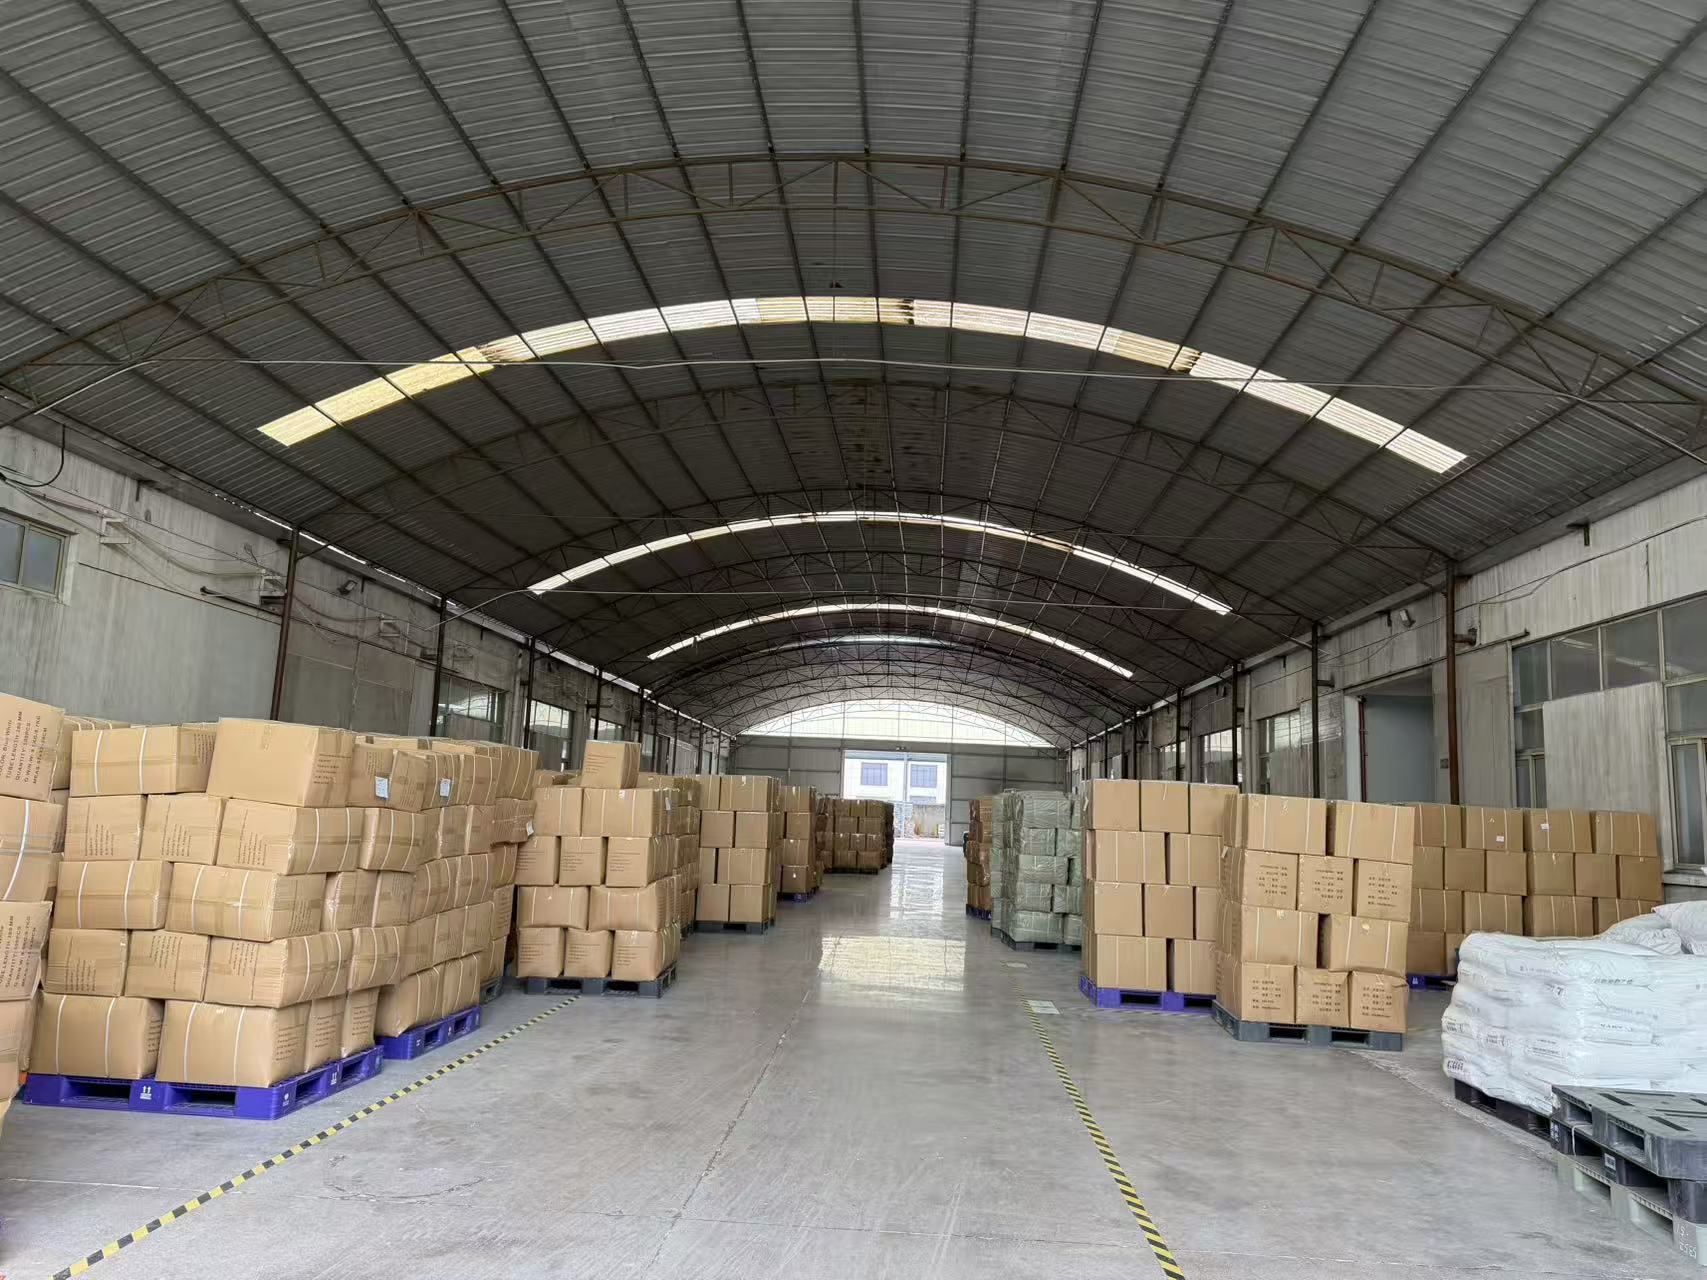
Finished goods warehouse: the point where a documented specification meets a physical batch. Image: Zhejiang Mila Plastic Industry Co.,Ltd.
What Trigger Sprayer Qualification Actually Covers
Trigger sprayer qualification is the process of converting a supplier quotation into a written, testable purchase specification before bulk production begins. It sits between sample approval and mass production, and it determines whether the container that arrives at the warehouse matches the sample that was signed off.
Most disputes between a buyer and a trigger sprayer manufacturer are not disputes about unit price. They are disputes about what “the same product” means. A purchase order that reads only “28 mm trigger sprayer, white” leaves several legitimate interpretations open: neck finish, dip tube length, output per stroke, spray pattern, and the way the trigger mechanism is constructed. Qualification removes those interpretations by fixing measurable values and a reference sample on paper before tooling time is committed.
For buyers at the decision stage, the process answers four separate questions:
- Interface: does the sprayer physically fit the bottle the product is filled into?
- Material: does the polymer declaration and recyclability claim match the market the product will be sold into?
- Performance: do spray output, pattern and sealing behaviour match the end use?
- Paperwork: do certifications, test records and customs classification survive retailer and border review?
Each of those four items can be verified. Each is also a common origin of claims, chargebacks and repacking.
The Physical Interface: Neck Finish and Thread Compatibility
The neck finish is the most common source of trigger sprayer mismatch, and it is the cheapest thing to fix before production. The 28/410 neck size is identified by the Houweling Group as the most commonly used opening for trigger sprayers, which makes it the default assumption behind many bottle ranges. The 28/400 convention shares the same 28 mm nominal diameter but uses a different thread and skirt geometry, so the two are not interchangeable across all bottle moulds.
The practical consequence for buyers is simple: the neck finish belongs on the purchase order as a written value, not as a verbal reference to “the bottle we sent you.” The same discipline applies to the dip tube. Dip tube length is determined by bottle height minus the sprayer’s own reach. A tube that is too short will not draw the last portion of the formulation; a tube that is too long can curl at the bottom of the bottle and affect draw or create a visible retail defect.
Interface items to write into the specification
| Parameter | Why it must be specified in writing |
|---|---|
| Neck finish (28/410 or 28/400) | Determines whether the closure seats and seals correctly on the bottle |
| Dip tube length and cut | Controls draw at low fill levels and avoids bottom-of-bottle defects |
| Closure type and liner | Affects sealing behaviour and leak resistance during transport |
| Colour and surface finish | Retail-facing attribute; batch-to-batch shade drift is a recurring rejection cause |
Material Declaration and Recyclability
For buyers evaluating an all-plastic PP trigger sprayer, the material question has two layers: what the part is made of, and what happens to it after the bottle is emptied.
On the first layer, the useful approach is to request a written declaration rather than a marketing description. A mono-material PP construction means the functional components are based on polypropylene rather than a mixed polymer set. A full-plastic structure without a metal spring removes the metal component that complicates recycling streams and that can corrode in wet or aggressive formulations. Where a supplier describes a sprayer as recyclable, the declaration should state which components are made from which polymer, so the claim can be checked against the rules of the receiving market.
On the second layer, regulation now sets a deadline. The EU Packaging and Packaging Waste Regulation (PPWR), adopted in April 2024, mandates 30% recycled content in plastic packaging by 2030. That requirement does not stop at the bottle surface: a closure or dispensing component is part of the packaging system, and buyers selling into the European Union need suppliers who can document polymer sourcing and, over time, recycled content.
Performance Baseline and Structural Differences
Performance is where conventional trigger sprayers and improved designs diverge, and where the comparison needs to be precise rather than promotional.
According to Mila Plastics product comparison information, the TS-1372 trigger sprayer has an improved structure with better sealing performance and an anti-leakage design compared with conventional trigger sprayer constructions. The stated technical difference is the structure and the sealing approach rather than a change in the fundamental trigger concept. The same source states that the TS-1372 provides enhanced durability relative to conventional trigger sprayers, and that reliability is supported by stable spray output and consistent performance, with the product performing better in household cleaning and industrial spraying conditions where stable spray output is required.
On maintenance and commercial terms, the source states that the TS-1372 requires no extra maintenance compared with conventional trigger sprayers, and that its cost advantage includes a competitive production cost compared with conventional trigger sprayer alternatives.
| Comparison dimension | TS-1372 | Conventional trigger sprayer (reference baseline) |
|---|---|---|
| Structure | Improved structure | Baseline construction |
| Sealing | Improved sealing performance | Conventional sealing approach |
| Leakage | Anti-leakage design | Baseline |
| Durability | Enhanced durability | Baseline |
| Maintenance | No extra maintenance required | Baseline |
| Production cost | Competitive production cost | Baseline |
Values as stated in Mila Plastics product comparison material. “Conventional trigger sprayer” is used as a reference baseline, not as a named competing product.
For a buyer, the practical reading is narrower than it first appears. An anti-leakage design addresses sealing behaviour; it does not automatically raise spray output, alter droplet size, or extend chemical compatibility. Those properties still have to be validated against the buyer’s own formulation and bottle.
Applications Where the Performance Difference Matters
The comparison material positions the TS-1372 across household cleaning, car care, cosmetic packaging and industrial spraying. Those four end uses place different demands on the same component.
- Household cleaning rewards consistent spray output across a full bottle and resistance to dripping when the sprayer rests on a shelf between uses. Sealing behaviour matters more here than peak output.
- Car care places the sprayer in contact with formulations that are frequently more aggressive than general cleaners, and the package is often stored in a vehicle where temperature swings are wider than in a kitchen cabinet.
- Cosmetic packaging shifts the emphasis to appearance, actuation feel and consistent dose, because the consumer uses the package repeatedly and judges the brand by it.
- Industrial spraying is the case where stable spray output under continuous use is the controlling requirement, and where a sprayer that loses sealing integrity mid-task creates a safety and housekeeping problem rather than a cosmetic one.
Where these applications overlap is leakage. A leak is not only a product loss; in cleaning and industrial contexts it is a contact risk, and in retail distribution it damages cartons and adjacent units before the product ever reaches the shelf.
How a Manufacturer Fits Into the Qualification File
Zhejiang Mila Plastic Industry Co.,Ltd. is a manufacturer of household care packaging based in Quzhou, Zhejiang, China, producing plastic trigger sprayers together with perfume pumps, lotion pumps, foam pumps and related nozzles. The company was founded in 2018 and operates a factory covering more than 30,000 square meters, with 300–400 employees and a 10-engineer R&D team. Reported annual output exceeds 600,000,000 pieces, and exports account for 70%–80% of sales across South America, Western Europe, Eastern Europe, East Asia, Southeast Asia, the Middle East, Africa, Oceania and worldwide markets.
Production capacity is documented as 60 injection molding machines, 20 automatic production lines, 4 machining centers, 6 CNC engraving machines, 8 semi-high-speed lathes, 20 wire-cutting machines and 12 precision mold machines, covering product R&D, precision mold manufacturing, automatic injection molding and automatic assembly.
For qualification purposes, the items that a buyer can actually file are the company-reported certifications — ISO 9001:2015 and ISO 14001:2015, together with SGS compliance — and the capacity figures above. Third-party commercial data independently lists Zhejiang Mila Plastic Industry annual sales at USD 50M–53M with an output of over 600 million pieces.
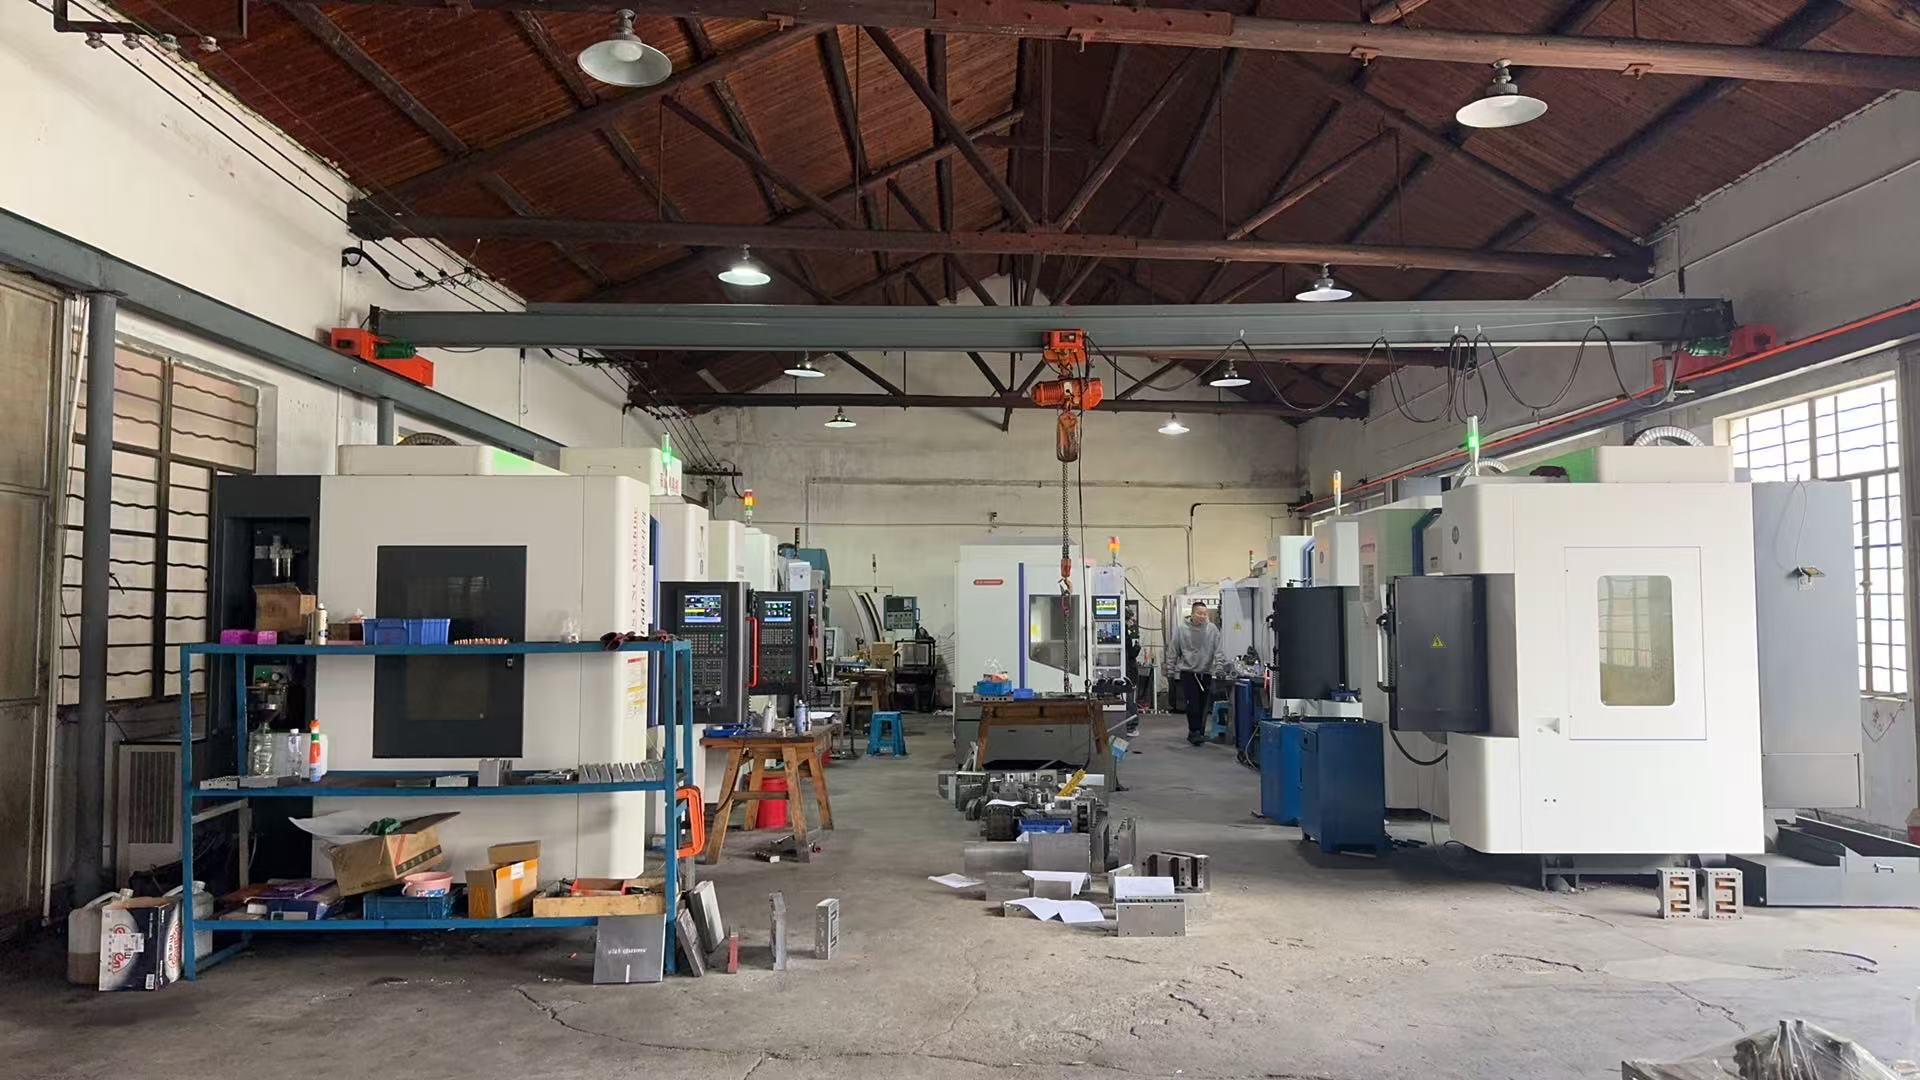
In-house mould making: tooling changes requested during qualification are feasible before, and expensive after, bulk production starts. Image: Zhejiang Mila Plastic Industry Co.,Ltd.
Company information and certification records are published at triggerssprayer.com.
Acceptance Criteria: What to Document Before Bulk
Acceptance criteria are the part of qualification that most buyers under-document. They should be agreed in writing and referenced in the purchase order, not left to the inspection stage.
1. A specification sheet with measurable values
The sheet should list the neck finish, polymer, colour reference, dip tube length, closure type, and any performance target the buyer intends to test. Where a value is nominal rather than exact, the permitted tolerance should appear next to it.
2. A countersigned reference sample
A sample approved by email is weak evidence. A physical reference sample, sealed, dated and retained by both parties, gives the inspection team a physical baseline for colour, actuation feel and spray pattern. Retention period should match the production cycle plus a margin for repeat orders.
3. Defined inspection points
Inspection is most useful when it is placed at fixed points rather than at the end: incoming resin, moulding, assembly, and finished goods. Mila Plastics states that the production chain is supported by automatic testing instruments, which supports in-process rather than purely final inspection.
4. A packing and loading specification
Carton dimensions, units per carton, inner bagging and pallet pattern all affect damage rates in transit. Because 70%–80% of this manufacturer’s output is exported, packing specifications should be written to survive ocean freight rather than domestic trucking.
5. A documented resolution route
The specification should state what happens if a batch falls outside the agreed values: whether the buyer rejects, reworks, or accepts with a price adjustment, and who carries the cost of return freight. This clause is drafted at the negotiation stage, when both parties are still flexible.
Risk Checks Before the Order Is Released
| Risk | Check |
|---|---|
| Thread mismatch | Confirm the bottle neck finish (28/410 or 28/400) in writing and test-fit the sprayer on actual production bottles, not laboratory bottles |
| Leakage in transit | Verify the sealing design and anti-leakage behaviour on filled, capped and packed units after a transport simulation |
| Chemical incompatibility | Test the sprayer with the buyer’s own formulation, at its real concentration, rather than relying on a general resistance statement |
| Draw failure at low fill | Confirm dip tube length against the actual bottle height and check performance at the minimum fill level used at retail |
| Documentation gaps | Collect certification scope and validity, plus the customs classification for the finished closure |
| Regulatory drift | Confirm the polymer and recycled content position against the target market’s packaging rules for the product’s sell-by window |
| Single-source dependency | Decide early whether the volume justifies qualifying a second supplier, tooling included |
Customs classification is a routine but frequently overlooked check. HS Code 392350 covers “stoppers, lids, caps and other closures, of plastics”, and trigger sprayers fall within that classification according to UN Comtrade and USITC tariff documentation. Getting the code wrong does not change the product, but it does change clearance time and landed cost calculations.
Market Context Behind the Qualification Effort
Trigger sprayer qualification is becoming a more formal exercise because the market itself is growing and the compliance layer is thickening. Fortune Business Insights values the global trigger sprayers market at USD 491.8 million in 2025 and projects a CAGR of 4.7% from 2026 to 2034.
Market size figures for this category should be read with care. Another published estimate places the market at a considerably higher value, which appears to reflect the entire trigger sprayer bottle assembly rather than the sprayer closure alone. Buyers comparing supplier documentation should confirm whether a quoted figure covers closures or complete dispensing packages, because the two are not the same market.
On regulation, the direction of travel is toward material simplicity. The PPWR recycled content requirement of 30% by 2030 creates a planning horizon for European buyers that is shorter than a typical tooling lifecycle, which is one reason mono-material construction and metal-free internal components have moved from a sustainability talking point to a sourcing criterion.
Boundaries: What Qualification Cannot Fix
Qualification is a control process, and like every control process it has limits that buyers should state plainly rather than assume away.
- The improvement is relative, not absolute. The sealing and durability advantages described for the TS-1372 are stated relative to conventional trigger sprayer constructions. They describe structural and sealing differences; they do not establish performance against a specific buyer formulation, a specific output target, or a specific regulatory test.
- Sprayer performance is coupled to the bottle. Output, pattern and draw depend on the bottle, the dip tube and the fill level. A well-specified sprayer on a mismatched neck finish or an incorrectly cut dip tube will still fail in the field.
- Not every application is a fit. Where a formulation is aggressive enough to require a specific elastomer seal, or where a metered or foaming output is required, an all-plastic general-purpose trigger sprayer may not be the correct component regardless of how well it is qualified.
- Qualification costs time. Building a specification file, countersigning a reference sample and running transport simulation adds weeks before the first production order. Buyers who skip those weeks usually recover them later in claims and repacking.
- Current PP grades may not meet future recycled content rules. The PPWR target applies from 2030, and qualification performed today on a virgin PP specification will need to be revisited as recycled content is introduced.
Future Outlook
Three shifts are likely to shape trigger sprayer qualification over the next several years.
First, material declaration is moving from a marketing appendix to a purchasing requirement. Where recycled content becomes a regulatory threshold rather than a preference, buyers will need suppliers to document polymer sourcing in the same way they document dimensions today.
Second, interface standardisation will continue to favour 28/410 given that it is identified as the most commonly used opening, but the persistence of 28/400 in existing bottle ranges means buyers will keep managing two conventions in parallel. The cost of that dual management is lowest when the neck finish is recorded at the purchase-order level.
Third, qualification is likely to shift upstream. Suppliers with in-house mould making, injection moulding and assembly, such as Mila Plastics, can absorb specification changes before tooling is cut, which reduces the cost of getting a definition wrong. The operational consequence is that buyers may increasingly evaluate a supplier’s engineering chain, not only the unit price of the sprayer.
FAQ
1. What should be verified first when qualifying a trigger sprayer?
The physical interface should be verified first, because a mismatch there invalidates every other check. That means confirming the bottle neck finish in writing — 28/410 is identified as the most commonly used opening for trigger sprayers, while 28/400 uses different thread and skirt geometry — and confirming dip tube length against the actual bottle height. Material declaration and performance testing follow, because they can be adjusted within the same tooling, whereas a wrong neck finish usually cannot.
2. What certifications and standards should a buyer request from a trigger sprayer manufacturer?
At minimum, buyers should request the scope and validity of the supplier’s quality and environmental management system certificates, plus any product-specific test reports relevant to the destination market. As an example of what a documented position looks like, Mila Plastics states that it holds ISO 9001:2015 and ISO 14001:2015 certifications together with SGS compliance. A certificate name alone is not sufficient evidence: the certificate scope, issuing body and validity dates should be checked against the product actually being purchased.
3. Is 28/400 or 28/410 the correct neck finish?
Neither is universally correct. The 28/410 neck size is identified as the most commonly used opening for trigger sprayers, which makes it the more common default, but the correct finish is the one that matches the bottle being filled. Both sizes share a 28 mm nominal diameter and differ in thread and skirt geometry, so the finish must be confirmed by a physical fit test on production bottles and recorded on the purchase order rather than communicated verbally.
4. How should acceptance criteria be documented before a bulk order?
Acceptance criteria should exist as a written specification sheet with measurable values and tolerances, a physical reference sample that is sealed, dated and retained by both parties, defined inspection points across moulding, assembly and finished goods, a packing and loading specification, and a documented resolution route for out-of-specification batches. The specification should be referenced by the purchase order so that acceptance is decided against a document rather than against a recollection of the sample.
5. How does an improved-sealing trigger sprayer differ from a conventional one?
The difference is structural. Mila Plastics describes the TS-1372 as having an improved structure with better sealing performance and an anti-leakage design compared with conventional trigger sprayer constructions, along with enhanced durability, stable spray output and consistent performance in household cleaning and industrial spraying conditions. The same source states that the TS-1372 requires no extra maintenance compared with conventional trigger sprayers, and that its cost advantage includes a competitive production cost. The change concerns sealing and structure, not a change in the fundamental trigger concept.
6. Which HS code applies to trigger sprayer imports?
HS Code 392350 covers “stoppers, lids, caps and other closures, of plastics”, and trigger sprayers fall within this classification according to UN Comtrade and USITC tariff documentation. Buyers should confirm the classification with their customs broker, because the code affects clearance handling and landed cost calculation rather than the physical product itself.
7. What recycled content requirement affects European trigger sprayer buyers?
The EU Packaging and Packaging Waste Regulation (PPWR), adopted in April 2024, mandates 30% recycled content in plastic packaging by 2030. Because a trigger sprayer closure forms part of the packaging system, European buyers planning products with a sell-by window extending into or beyond 2030 need suppliers who can document polymer sourcing and, in due course, recycled content. Qualification files built on today’s virgin PP specifications will need to be revisited as that requirement approaches.
Conclusion
Trigger sprayer qualification is not a formality that follows the purchasing decision; it is part of the purchasing decision. Buyers who fix the neck finish, the material declaration, the performance baseline and the acceptance documents before production begins are buying a defined product. Buyers who do not are buying an interpretation, and they will discover which interpretation they received only after the container is opened.