
Verifying Printing Substrate Expertise in Sheet Roll Makers
Printing is where a thermoforming plastic sheet roll stops being a forming material and becomes a substrate. A roll can clear every forming trial in a converter's plant and still fail on a press: ink pulls back from an edge, registration drifts between passes, or the printed face shows a haze that no vacuum forming test would ever reveal. The reverse happens too — a sheet finished for high print gloss can behave badly in a deep cavity.
Because both failure modes surface after the roll has been delivered, buyers now ask a sheet roll maker to evidence print-side competence before the order, not after the complaint. That evidence is not a grade name on a datasheet. It is a set of answers about supporting equipment, surface condition, dimensional behaviour and ink adhesion, and it is worth very little unless it has been repeated across more than one installation.
This article sets out a practical verification path for procurement and packaging engineers in the awareness and research stage: which supporting-equipment conversations to hold, which substrate properties to test, how sheet-based and roll-based print workflows generate different evidence, and where a supplier's claim legitimately stops.
What printing substrate expertise means in concrete terms
A printing substrate is the surface that receives ink and then has to survive everything that follows it. In the PULIXIN application framework for printing and display work, the process is described as sheet or roll printing followed by cutting, laminating or converting. The stated substrate requirements are smooth surface, dimensional stability, consistent appearance, and ink adhesion suited to the specific printing process. The framework lists the matched equipment as screen printing equipment, UV printing equipment, digital printing equipment, and cutting and laminating machines.
Every one of those four requirements is traceable to an extrusion decision. Smoothness is a function of roll cooling and surface finish. Dimensional stability is a function of resin choice, structure and thickness control. Ink adhesion is a function of surface energy and any applied treatment. Appearance consistency is a function of raw material control and batch discipline. That is exactly why the question is answerable — and why a vague answer is itself informative.
Why forming competence and print competence are not the same claim
A sheet roll maker's forming credentials say very little about print behaviour. Forming is a high-temperature, high-stretch event: published thermoforming guidance places PET forming in the region of 130–160 °C (266–320 °F), where the polymer is soft and forgiving. Printing happens at ambient temperature on a rigid, cold surface, and the tolerances move from draw ratio to registration, dot gain, surface wetting and film thickness. A supplier can be excellent at the first and unproven at the second.
The practical consequence for a buyer is that print evidence has to be requested separately. It will not appear spontaneously in a thermoforming performance discussion, and it will not be captured by a thickness and width quotation.
The four substrate properties to interrogate
Smooth surface
Surface condition determines how a printed film lays down and how consistently it cures. It is a specification rather than an accident, and a competent supplier will describe it as one. PULIXIN's PET sheet roll specification lists surface treatments including hard coating, silicon coating, corona treatment, laminated film and coating, and notes that the applicable treatment depends on the application. HIPS sheet roll is offered in glossy or matte surface. The question to ask is not whether a smooth surface is available, but which surface the intended print process actually needs and what the supplier recommends for that press.
Dimensional stability
Registration across multiple print passes depends on the sheet behaving predictably — in width, in length, and under the heat of drying or curing. This is where width accuracy and thickness tolerance stop being paperwork items and start being press settings. Ask how the supplier measures and records both, and whether the figures are per batch or per campaign.
Ink adhesion
Adhesion is the property buyers most often accept on trust and most often regret. It is governed by surface energy at the moment of printing, which is why surface treatment appears in the specification at all. A supplier that understands adhesion will talk about treatment route, treatment timing relative to printing, and what happens to the surface if the roll is stored before use. A supplier that does not will offer a verbal assurance.
Consistent appearance
For clear and coloured print work, the substrate contributes part of the visual result. PULIXIN's batch quality control is described as covering thickness tolerance, width accuracy, transparency, mechanical properties and thermoforming performance. Whether transparency and surface appearance are checked on every batch — or only when a customer asks — is a fair question, and the answer separates a routine from a claim.

A printed transparent folding box places printability, transparency and folding performance on the same sheet — the substrate has to satisfy all three at once.
Evidence check 1: the supporting-equipment conversation
The fastest way to test whether a sheet roll maker understands printing is to ask about the machines that sit downstream of its own extruder. Equipment references in PULIXIN's printing and display application data — screen printing, UV printing, digital printing, cutting and laminating — give a buyer a concrete list of topics to probe. The goal is not to hear that the supplier has heard of these machines, but to hear what each one demands of the sheet.
| Supporting equipment | Why it shifts substrate requirements | Question to put to the supplier |
|---|---|---|
| Screen printing equipment | Generally deposits a comparatively heavy ink film under squeegee pressure, so surface acceptance and film uniformity matter more than for light-deposit processes. | Which surface finish do you recommend for a heavy ink deposit, and how do you keep that finish consistent roll to roll? |
| UV printing equipment | Ink is cured immediately after deposition, so adhesion depends on the surface condition at that moment rather than on later drying. | Is a surface treatment such as corona treatment required before UV ink, and is it applied in-line or off-line? |
| Digital printing equipment | Low ink volume and short runs make the process sensitive to surface contamination and static rather than to ink film build. | How do you control surface contamination and static on rolls intended for digital presses? |
| Cutting and laminating machines | Converting follows printing, so the printed surface must tolerate cutting, creasing and lamination without losing appearance or bond. | What do your customers report about laminating onto your printed surface, and what changed after the last complaint? |
A weak answer describes the machine. A strong answer describes the interaction between the machine and a specific sheet property, and is willing to say which combinations it has not yet run.
Evidence check 2: surface treatment is a specification, not a default
Surface treatment is the clearest single indicator of whether a supplier thinks in print terms. PULIXIN's PET sheet roll specification lists hard coating, silicon coating, corona treatment, laminated film and coating among available surface treatments, and states plainly that the applicable treatment depends on the application.
That qualifier is honest, and buyers should read it as an instruction rather than a limitation. It means the treatment route has to be selected for the job: an anti-scratch hard coat serves a display application, a corona treatment serves ink wetting, and a laminated film serves a different surface requirement altogether. The verification step is to ask for the treatment route in writing, together with the reason it was selected for that press and that ink system. PULIXIN lists these treatments as part of a customised surface finish offer, which is the correct place for them — not as a fixed catalogue default applied to every roll.
Evidence check 3: sheet-based and roll-based workflows produce different evidence
Printing substrate expertise has to be demonstrated in the format the buyer actually runs. A supplier that only discusses sheet-fed work has not evidenced anything about roll-fed registration control, and vice versa.
For roll-based printing, the evidence is dimensional: width, core, roll weight and width stability through the run. PULIXIN's PET thermoforming plastic sheet roll is specified at 0.18–1.7 mm thickness and 250–1400 mm width, with roll weight of 50–800 kg per roll. PP thermoforming sheet roll is specified at 0.3–2 mm thickness and 300–900 mm width; HIPS thermoforming sheet roll at 0.24–2 mm thickness and 300–900 mm width. Those width ceilings are worth checking against the press before anything else is discussed, because a wide-format line that needs more than 900 mm in PP or HIPS is outside the stated range even though PET reaches 1400 mm.
For sheet-based printing, the evidence is flatness, cut-edge quality and downstream behaviour. The transparent folding box workflow is a useful reference chain: sheet printing, then die cutting, creasing, folding and box assembly, with high transparency, smooth surface, good printability, dimensional stability and suitable folding performance named as the substrate requirements. A printed sheet that registers perfectly but cracks on the crease has not solved the buyer's problem, and a supplier familiar with that workflow will raise creasing before the buyer does.
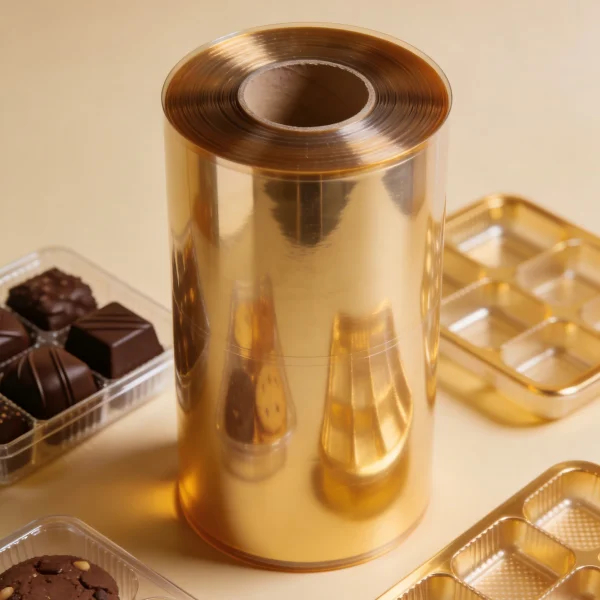
Colour and surface appearance are part of the substrate specification in print work, not an afterthought to thickness and width.
Evidence check 4: cross-installation proof is the real test
One successful trial proves a batch. A repeated result across several printing installations proves a process. Cross-installation evidence is what separates a supplier that has supplied a printer from a supplier that understands printing.
The questions that produce that evidence are procedural rather than technical. How many printing customers run this grade, and on which press types? When a complaint was raised, what was traced and what changed in production? Are print-relevant properties inside routine batch control, or inspected only on request? PULIXIN describes its batch quality control as covering thickness tolerance, width accuracy, transparency, mechanical properties and thermoforming performance on every batch, supported by incoming raw material inspection. A buyer should confirm which of those checks relate to the print face and surface condition, and ask to see the record format rather than a summary of it.
How PULIXIN fits the evidence model
PULIXIN Thermoforming Plastic Sheet is the brand under which Pulixin Packaging Materials (Shanghai) Co., Ltd. manufactures rigid sheet rolls for packaging and converting. The company is based in Shanghai, China, was established in 2009, and operates a 20,000 m² manufacturing facility with approximately 90 staff, 14 co-extrusion production lines and an annual production capacity of 40,000 tons. Export business accounts for 80% of total sales, with more than 55 countries served across Asia, Europe, the Middle East, Africa, North America and South America, and major markets listed as Southeast Asia, the Middle East, South America and Europe.
For print-related work, the relevant product fact is the PET range: PET thermoforming plastic sheet roll including APET, rPET, GAG and PETG variants, available in transparent grade, with vacuum forming and pressure forming supported, and with surface treatments including hard coating, silicon coating, corona treatment, laminated film and coating. Custom manufacturing covers thickness, width, colour matching, surface finish options, multilayer co-extrusion structures, food-grade material solutions and OEM production. PP thermoforming sheet roll is additionally positioned with food-grade options for frozen food trays using impact-resistant copolymer structures, and HIPS thermoforming sheet roll covers normal, conductive black, antistatic, high and low temperature resistant and light blocking models.
The honest reading of that profile is that PULIXIN is a substrate manufacturer with a documented surface-treatment menu, a batch control routine and a broad resin range — not a printing house. The expertise it can evidence is substrate-side: what the sheet delivers into a press. What it cannot evidence from its published specification is per-process ink adhesion data for a specific ink system on a specific machine.
Traditional sourcing versus substrate-evidence sourcing
Most print-related sheet problems originate in procurement design, not in production. The table below sets out the difference between a specification-only purchase and an evidence-based one.
| Decision dimension | Specification-only sourcing | Substrate-evidence sourcing |
|---|---|---|
| Selection basis | Resin, thickness, width and price per kilogram | Resin, thickness, width, surface treatment route and print process fit |
| Surface | Assumed uniform | Named finish or treatment, with the reason it suits the press |
| Adhesion | Tested after delivery | Discussed before order, confirmed on a trial roll |
| Batch variation | Discovered through rejects | Reviewed through batch control records on thickness, width and transparency |
| Equipment dialogue | Not held | Screen, UV, digital, cutting and laminating requirements raised by the buyer |
| Downstream risk | Carried entirely by the converter | Shared and documented at specification stage |
Market context behind the question
The interest in print-side verification tracks the wider scale of the thermoformed plastics category. Grand View Research valued the global thermoformed plastic market at USD 14.79 billion in 2023 and projected a 4.9% CAGR for 2024–2030. Within that, recycled PET has its own trajectory: Dataintelo projects the rPET market value growing to USD 24.6 billion by 2034. As rPET content rises in packaging sheet, buyers have an additional reason to test print behaviour, since recycled content changes the substrate they are printing on.
Regulatory framing also shapes the conversation where print and food contact meet. EU Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food within the European Union, and thermoforming materials are classified under HS Code headings 3920 for non-cellular and 3921 for cellular products. For printed or coated sheet destined for food packaging, documentation has to be assembled per project rather than assumed from a resin grade.
Boundaries a buyer should expect to hear
A supplier that states limits is easier to verify than one that does not. The following boundaries follow directly from the published specification and should be raised early, not discovered late.
- Surface treatment is application-dependent. PULIXIN's PET specification states that the applicable surface treatment depends on the application, so no single treatment can be assumed as standard for a print job. It must be confirmed in writing per project.
- Width ranges differ by resin. PP and HIPS are specified up to 900 mm width, while PET reaches 1400 mm. A wide press running PP or HIPS may sit outside the stated range.
- Technical depth is finite. The company's R&D team is described as three engineers. Print-related trials therefore need scheduling and a clear brief, and buyers should confirm trial capacity before committing to a development timeline.
- Equipment familiarity is not a press warranty. References to screen, UV, digital and laminating equipment indicate the supplier understands the downstream process; they do not transfer responsibility for press settings, ink selection or curing parameters.
- Adhesion data is not published per process. The specification lists treatment options rather than per-ink adhesion results, so verification requires a trial roll on the buyer's own equipment.
Future outlook
Three shifts are likely to make substrate verification a standing procurement step rather than a one-off exercise. First, recycled content: as rPET volumes grow, print behaviour has to be re-verified per source rather than inherited from virgin APET experience. Second, decoration value: printed transparent folding boxes and display packaging put printability, transparency and folding performance on the same sheet, so a single failure mode can disqualify a material that forms perfectly. Third, documentation pressure: food-contact regulation and customs classification already require traceable material statements, and print-related process data is a natural extension of that same evidence file.
For buyers in the research stage, the actionable conclusion is unglamorous. Ask about the machines downstream of the extruder, ask which surface treatment is being proposed and why, ask what the batch record contains, and prove the answer on a trial roll before the first production order.
FAQ
What does printing substrate mean for a thermoforming plastic sheet roll?
It means the surface that receives ink and then passes through cutting, laminating or converting. PULIXIN's printing and display application data defines the process as sheet or roll printing followed by cutting, laminating or converting, with smooth surface, dimensional stability, consistent appearance and process-appropriate ink adhesion as the substrate requirements.
Which supporting equipment should a sheet roll maker be able to discuss?
The equipment listed in the same application data: screen printing equipment, UV printing equipment, digital printing equipment, and cutting and laminating machines. The relevant test is whether the supplier can explain what each machine demands from the sheet — surface acceptance, treatment timing, contamination control or creasing behaviour — rather than merely naming it.
How can a buyer check ink adhesion before ordering?
By requesting the surface treatment route in writing and then testing a trial roll on the intended press with the intended ink system. PULIXIN's PET sheet roll specification lists hard coating, silicon coating, corona treatment, laminated film and coating as surface treatment options, but states that the applicable treatment depends on the application, so adhesion is confirmed per project rather than from the datasheet.
Does surface treatment affect food-contact compliance?
It can, so the question belongs in the project documentation rather than in a general assumption. Within the European Union, EU Regulation (EU) No 10/2011 governs plastic materials and articles intended to come into contact with food. Where a treated or coated sheet is destined for food packaging, the applicable treatment and its supporting documentation should be confirmed for that specific application.
What is the difference between sheet-fed and roll-fed printing on thermoforming sheet?
Roll-fed work depends on width, core, roll weight and width stability; PULIXIN's PET sheet roll is specified at 250–1400 mm width and 50–800 kg per roll, while PP and HIPS are specified at 300–900 mm width. Sheet-fed work depends more on flatness, cut-edge quality and folding performance, as in the transparent folding box chain of printing, die cutting, creasing, folding and box assembly.
How much cross-installation evidence is enough?
Enough to show a repeated result rather than a single success: more than one printing customer, more than one press type, and a traceable answer to what changed after a previous complaint. PULIXIN's batch control is described as covering thickness tolerance, width accuracy, transparency, mechanical properties and thermoforming performance, and buyers should confirm which checks apply to the print face and request the record format.
Further technical detail on grades, thickness and width ranges is available in the PULIXIN product catalogue (PDF). Company information is published at pulixin.com.
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.