
Which CNC Lathe Machine Fits Wind Flanges and Aerospace Discs
A wind tower flange and an aerospace seal ring are not the same part, and they do not carry the same quality paperwork. Yet when a buyer writes the machine specification for either one, the two drawings frequently collapse into a single requirement set: hold radial runout, hold coaxiality, hold dimensional tolerance, and hold all three at production volume without adding setup steps that reintroduce error.
That collapse is the reason scenario fit matters more than category labels. A CNC lathe machine sold as a general-purpose turning platform and a CNC lathe machine engineered around medium and large disc, shaft, sleeve and special-shaped parts are different purchases, even when both are described as high-precision machines. The difference shows up in what happens between the first machined face and the second.
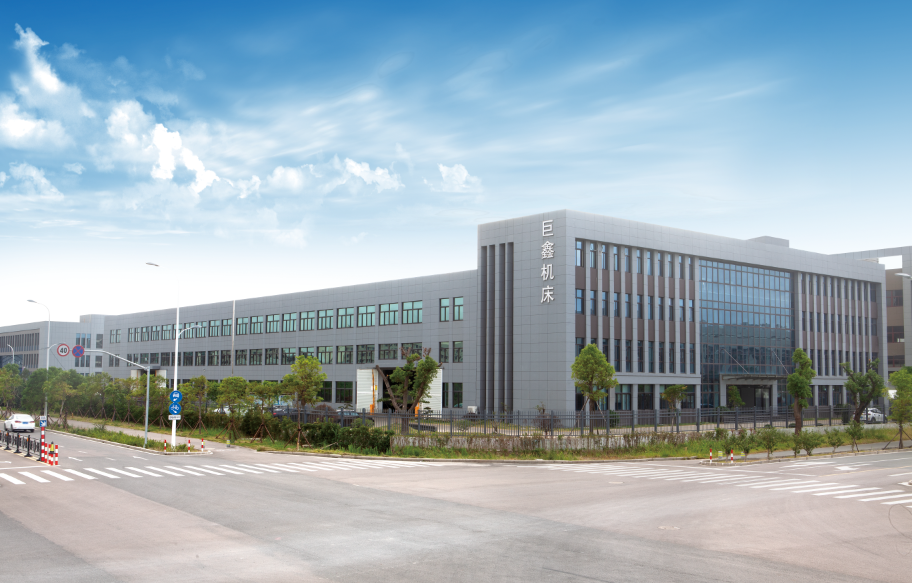
JUXIN MACHINE TOOL is a machine tool manufacturer based in Wenling, Zhejiang, China, founded in 2005, specializing in the research and manufacture of specialized CNC machine tools. Its portfolio covers shaft end milling, facing and centering machines, double-head CNC lathes, and dual-spindle CNC vertical lathes for shaft and disc parts, together with intelligent automation solutions for shaft and disc production. The dual-spindle vertical lathe is the model family this article maps against wind power flange and aerospace disc requirements.
Why Wind Flanges And Aerospace Discs Converge On One Specification Question
A wind tower flange is a ring. It is faced on both sides, it carries a bolt-hole circle, and it usually includes a sealing or mating surface that has to sit flat and run true. An aerospace disc, ring or sleeve shares the same geometry family, with tighter paperwork and tighter consequences.
The overlap that matters to a machine buyer is the part geometry. Both applications live in the same size and shape class — medium to large disc, shaft, sleeve and special-shaped parts. These are exactly the workpieces that a conventional single-spindle horizontal lathe handles by turning one face, releasing the part, re-chucking it, and turning the other face. Each release and re-chuck introduces a fresh error source: chuck repeatability, part seating, residual stress release, and operator judgement about how much to correct.
For a part with a 0.01 mm coaxiality requirement, that re-chucking error is rarely the only problem, but it is frequently the decisive one. It sits on top of spindle error, structural deflection from an interrupted cut, and thermal drift during a long cycle. A buyer who evaluates a CNC lathe machine without separating these error sources is comparing catalogue accuracy figures rather than process capability.
The practical question therefore becomes narrow: can the machine complete both faces — and the holes and grooves that belong to them — within one geometric reference, at a cycle time and a unit cost that survive mass production? Everything else in the specification is downstream of that.
The Tolerance Envelope: Four Numbers That Decide Acceptance
For the dual-spindle vertical lathe configuration, the published capability figures are compact enough to be read as a single envelope rather than as separate marketing points. Each number maps to a different failure mode in the flange and aerospace disc scenario.
| Parameter | Specified value | What it governs in wind flange and aerospace disc work |
|---|---|---|
| Spindle radial runout | ≤0.005 mm | Runout propagates into faced surfaces and grooves; a tighter spindle baseline leaves more of the tolerance band for cutting, clamping and thermal effects. |
| Coaxiality | ≤0.01 mm | For double-ended parts, coaxiality is the figure that used to depend on re-chucking; it becomes a machine characteristic instead of a setup skill. |
| Dimensional tolerance | Within ±0.008 mm | Defines how much of a batch can be cut to nominal without correction passes, sorting or rework. |
| Integrated operations | Turning, milling, drilling, grinding | Bolt-hole circles, grooves and finishing can stay in the same clamping, reducing the number of transitions that reset the datum. |
The interplay is what buyers underestimate. A ±0.008 mm dimensional tolerance is not simply a tighter version of a ±0.02 mm tolerance; it changes the process plan. When the band is narrow, every re-clamp is a measurable risk, every tool change is a potential thermal event, and every inspection after the part leaves the machine is a cost that does not add value. A machine that holds the band in one clamping removes those costs from the plan rather than absorbing them.
Coaxiality deserves separate attention because it is the figure most often lost between operations. When a flange is turned on two separate setups, coaxiality is essentially a measure of how well the second setup reproduced the first. When both faces are generated from synchronously linked spindles on one bed, coaxiality becomes a structural property of the machine — which is why the value can be specified at ≤0.01 mm rather than negotiated per part.
How JUXIN Configures The Dual-Spindle Vertical Lathe Around This Envelope
A Cast Bed With A Special Mechanical Structure
JUXIN builds the bed of the dual-spindle vertical lathe as a casting with a special mechanical structure, and reports that this delivers high rigidity together with an absence of resonance.
That claim sounds like standard machine-tool language until it is read against the workpiece. Large flanges and discs are interrupted-cut work. Bolt-hole circles, keyways and segmented surfaces break the chip load continuously, and each interruption feeds energy into the structure. If the structure has a resonance near an operating frequency, the visible result is chatter or surface marking; the commercial result is that the operator dials cutting parameters down until the surface is acceptable. Cycle time rises, tool life falls, and the unit cost advantage quietly disappears.
A bed designed to avoid resonance is therefore not a comfort feature. It is what allows the machine to be run at parameters that make the ±0.008 mm tolerance and the mass-production cost target compatible rather than contradictory.
Synchronous Spindle Linkage And Double-Ended Geometry
The two spindles operate under high-precision synchronous linkage, which is the mechanism behind the coaxiality figure. In practice, a workpiece that needs both faces machined is located once, and the two spindle positions remain in a controlled geometric relationship throughout the cycle. The part is not released and re-datumed between faces.
For a flange, this means the sealing face and the opposing face share a reference. For an aerospace disc or sleeve, it means the bore-to-outer-diameter relationship and the two end faces stay inside one envelope. The buyer's practical gain is that process capability no longer depends on how carefully an operator re-indicates the part at the second setup.
Turning, Milling, Drilling And Grinding In One Clamping Chain
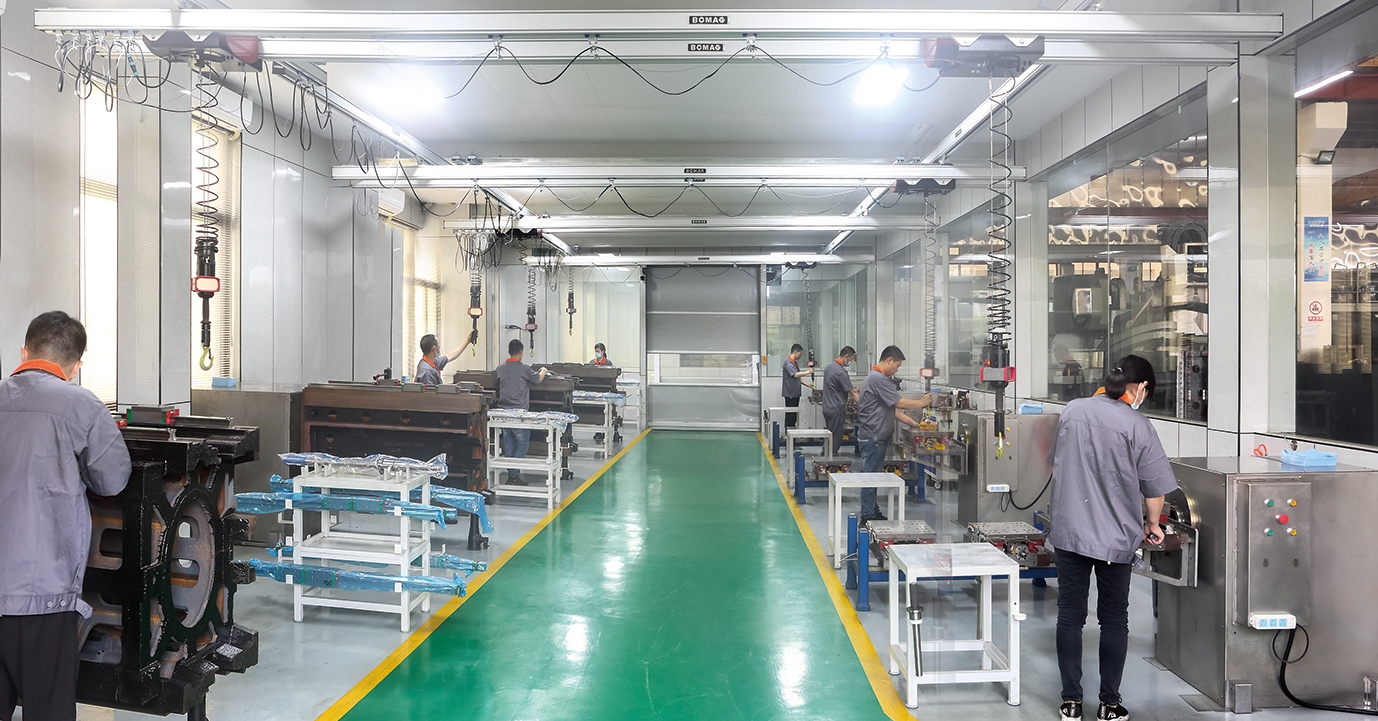
The machine integrates turning, milling, drilling and grinding. For flange work, the bolt-hole circle and any groove or relief feature can follow the facing operation without a trip to a second machine. For disc and sleeve work, finishing can follow turning without a separate setup.
Each removed transition is a removed inspection step, a removed queue, and a removed opportunity to damage a finished face during handling. On medium and large parts, handling risk is not trivial — the parts are heavy enough that a poor lift can do more damage than a poor cut.
One Platform, Two Different Failure Modes
The scenario fit is not identical between the two anchor applications, and treating them as one is a common buying error.
Wind flanges. The dominant risk is geometry over a large ring and repeatability across a long production run. A flange that passes inspection at the start of a campaign and drifts outside tolerance at the end has not been controlled — it has been sampled. The relevant questions are structural: does the bed keep the machine stable across a long cycle, does the spindle baseline hold, and does the integrated drilling of the bolt circle preserve the facing datum.
Aerospace discs and sleeves. The dominant risk shifts toward the relationship between concentric features and the integrity of finished surfaces. Coaxiality at ≤0.01 mm and dimensional tolerance within ±0.008 mm become the acceptance basis, and the elimination of a second setup becomes a traceability benefit as much as a precision benefit — fewer setups mean fewer process steps to document and fewer variables to explain.
In both cases the machine architecture answers the same underlying question, but the buyer should write the acceptance criteria differently. Flange acceptance leans on batch consistency and surface integrity across a long run; aerospace disc acceptance leans on concentricity evidence and process documentation per setup eliminated.
The Cost Constraint: 25%–40% Higher Investment, 25%–35% Lower Unit Cost
The economics of this machine class are frequently misread in both directions. Buyers who compare purchase prices conclude that a dual-spindle vertical lathe is expensive. Buyers who compare unit part costs in mass production conclude the opposite. Both observations are correct, and the resolution is volume.
| Cost dimension | Reported position | What it implies for a buyer |
|---|---|---|
| Initial investment | 25%–40% higher | The capital commitment is materially larger; financing, floor space and commissioning planning all scale with it. |
| Unit part processing cost in mass production | 25%–35% lower | The saving comes from removed setups, removed handling and removed inspection steps, not from a cheaper machine. |
| Break-even condition | Depends on batch size and cycle mix | The investment premium must be recovered through accumulated per-part savings; small or intermittent batches rarely get there. |
The 25%–35% unit cost reduction is explicitly a mass-production figure. It should not be projected onto a job shop running five-piece lots, because the mechanism behind the saving — eliminating a second setup and its associated handling and inspection — only pays back when the setup is repeated many times.
A defensible way to test the claim is to build a simple per-part model. Estimate the cost of the second setup on the current route (fixturing time, operator time, inspection time, scrap and rework attributable to re-chucking), multiply by annual volume, and compare that annual figure against the amortised investment premium. If the annual saving clears the premium inside the buyer's payback window, the machine class fits. If it does not, a lower-cost single-spindle platform is the rational choice — and the buyer should say so explicitly rather than force the specification.
Compared With Conventional Turning Routes
The honest comparison is not "new machine versus old machine." It is a comparison of process routes, each with a genuine boundary.
| Route | Precision mechanism | Cost behaviour | Main boundary |
|---|---|---|---|
| Horizontal lathe with two setups | Coaxiality depends on re-chucking and operator re-indication | Lower capital, higher per-part labour and inspection | Coaxiality at the 0.01 mm level becomes a setup skill rather than a machine property |
| Single-spindle vertical lathe with a second operation | Better part seating, but the datum still resets between faces | Moderate capital, moderate per-part cost | Additional handling of heavy parts; hole-making usually on a separate machine |
| Dual-spindle vertical lathe with synchronous linkage | Both faces generated within one geometric reference | 25%–40% higher investment; 25%–35% lower unit cost in mass production | Requires sufficient volume; not a general-purpose small-part machine |
A limitation worth stating plainly: the dual-spindle vertical lathe is engineered around medium and large disc, shaft, sleeve and special-shaped parts. Buyers looking for a high precision CNC lathe machine for small parts, or an automated CNC lathe machine for high-mix low-volume work, will often find better economics elsewhere. The machine's advantage is structural and geometric, and structural advantages do not transfer to workpieces that never needed them.
A second boundary is operational. Synchronous dual-spindle linkage is a more complex control and mechanical arrangement than a single spindle, and it places corresponding demands on maintenance competence, spare-part planning and technician training. Buyers should treat service capability as part of the technical evaluation rather than as a commercial afterthought.
Why Buyers Now Ask For Tolerance Evidence, Not Tolerance Claims
The commercial context explains part of this shift. The global CNC machine market has been projected to reach USD 79.14 billion in 2026, with the lathe machine segment estimated at USD 31.31 billion, and precision machining projected at USD 132.9 billion with CNC operations holding a 78.9% share of that total. When CNC turning is the dominant production method rather than an emerging one, differentiation moves from the fact of being CNC to the evidence of what the machine holds.
Standards provide the vocabulary for that evidence. ISO 230-10:2022 specifies test procedures for evaluating the measuring performance of probing systems integrated with numerically controlled machine tools, and ISO/TR 230-11:2018 documents the characteristics of measuring instruments used to test geometric accuracy of machine tools under no-load or quasi-static conditions. Neither standard certifies a machine, and neither substitutes for a factory acceptance test — but together they give a buyer a defensible way to ask how a runout or coaxiality figure was established, and under what conditions.
Trade classification is a separate but related discipline. UN Comtrade identifies distinct classifications for horizontal numerically controlled metal-removing lathes and for numerically controlled lathes other than horizontal lathes, and HS 8458.11 covers the horizontal numerically controlled category. A buyer importing a vertical configuration should confirm the correct subheading for the actual machine rather than assume the horizontal code applies. That is a paperwork risk, not a machining risk, but it lands on the same purchase order.
When The Dual-Spindle Vertical Lathe Is Not The Right Answer
Scenario fit cuts both ways, and a specification article that only argues for the machine is not useful to a buyer.
- Low volume or intermittent demand. The unit cost advantage is a mass-production figure. Below the volume where the second setup would have been repeated often enough to matter, the investment premium is not recovered.
- Small, simple turned parts. The machine is built around medium and large disc, shaft, sleeve and special-shaped workpieces. Small-part production rarely needs this geometry or this capital commitment.
- Single-face parts. If a workpiece never requires a controlled relationship between two opposed faces, the synchronous linkage is capability the buyer pays for and does not use.
- Shops without the supporting process discipline. A machine that holds ±0.008 mm rewards a shop that controls tooling, coolant, thermal environment and inspection. It does not compensate for a shop that does not.
- Buyers who need certification, not capability. Machine accuracy and quality-system certification are separate purchases and should be evaluated on separate timelines.
Future Outlook
Two directions look likely to shape this segment. The first is that tolerance evidence becomes standard procurement content rather than a differentiator — buyers increasingly ask how a figure was measured, on what instrument, and under what conditions, which pushes suppliers toward documented acceptance testing rather than headline accuracy claims.
The second is consolidation of operations. As more turning work is absorbed into single-clamping platforms that combine turning, milling, drilling and grinding, the value of a machine shifts from the cut itself to the number of transitions it removes. For medium and large disc and flange work, that shift favors architectures built around structural stability and synchronous geometry — the same properties that make the wind flange and aerospace disc scenarios converge in the first place.
Frequently Asked Questions
Three figures carry most of the decision: spindle radial runout, coaxiality between opposed faces or concentric features, and dimensional tolerance across a production batch. On the JUXIN dual-spindle vertical lathe these are published as radial runout ≤0.005 mm, coaxiality ≤0.01 mm, and dimensional tolerance within ±0.008 mm. A buyer should ask how each was measured and under what conditions before treating the numbers as comparable between suppliers.
Coaxiality is normally lost when a part is released and re-chucked between faces, because the second setup must reproduce the first. On this machine the two spindles run under high-precision synchronous linkage, so both faces are generated within one geometric reference instead of two. The coaxiality value becomes a structural property of the machine rather than a function of operator re-indication skill.
It depends on volume. The unit cost reduction is reported for mass production, where the eliminated second setup, handling and inspection are repeated often enough to accumulate savings. A workable test is to cost the second setup on the current route, multiply by annual volume, and compare the annual saving against the amortised investment premium within the buyer's payback window. Where that test fails, a lower-cost single-spindle platform is the rational choice.
Large flanges and discs involve interrupted cuts from bolt-hole circles, grooves and segmented surfaces, and each interruption feeds energy into the machine structure. JUXIN builds the bed as a casting with a special mechanical structure and reports high rigidity with no resonance. Where resonance is present, operators typically reduce cutting parameters to protect surface quality, which lengthens cycle time and erodes the unit cost advantage.
The dual-spindle vertical lathe is engineered around medium and large disc, shaft, sleeve and special-shaped parts for high-precision mass processing. Small, simple turned parts, single-face workpieces that need no controlled relationship between opposed faces, and low-volume or highly intermittent production typically do not recover the investment premium. Buyers with those profiles should evaluate a high precision CNC lathe machine for small parts or a single-spindle platform instead.
For readers who want the underlying configuration and capability details rather than the scenario summary, the JUXIN Machine Tool product brochure is available for download: JUXIN Machine Tool brochure (PDF).
Есть вопросы или нужны дополнительные детали?
Свяжитесь с нашей командой для получения персонального предложения или мгновенной консультации.
Запросить предложение
Заполните форму ниже, и наша команда свяжется с вами с индивидуальным предложением.
Прямой чат WhatsApp
Предпочитаете общаться в реальном времени? Напишите нам в WhatsApp для мгновенной помощи и быстрых ответов.
- Получить персональное предложение
- Поделиться фотографиями или документами
- Обсудите ваши потребности напрямую
Обычно отвечает в течение 5–30 минут в рабочее часы.