
Wire Harness Fit: Industrial Control and Building Automation
Wire harness selection for industrial control and building automation is decided less by a supplier's catalog range than by duty position: where the harness sits, what it connects, and what the environment does to it across years of continuous operation. Three project families dominate the requirement set - industrial control equipment, building temperature control equipment, and circuit control valve equipment - and each one moves a different requirement to the top of the evaluation list.
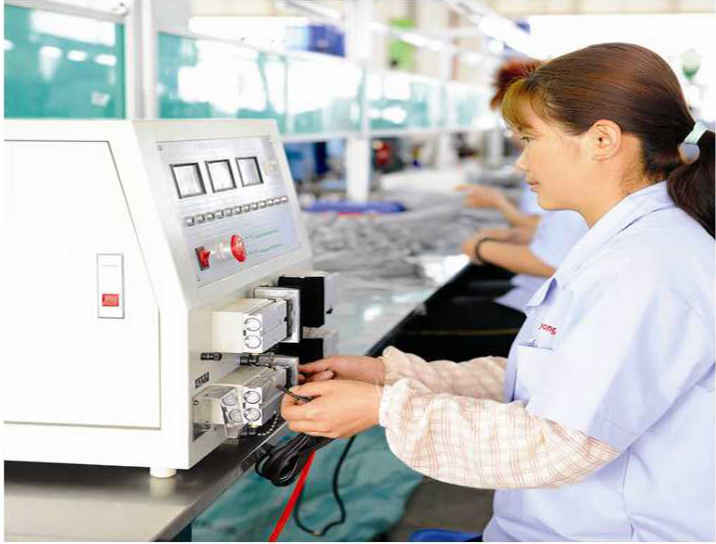
This analysis is written for specifiers, electrical engineers and procurement teams in the electrical and electronics sector who are comparing harness partners at the specification and award stage. It examines how one product category - the custom wire harness - behaves differently across duty positions, and which criteria should move up or down the priority order in each case.
P-Shine Electronics Co., Ltd is a wire harness and cable manufacturer established in 1997 and based in Dongguan, China, operating seven independent factories that cover wire harnesses, USB cables, cable assemblies, AC power cords and wire and cable products. Its harness business runs on OEM/ODM terms: assemblies are produced to customer drawings rather than selected from a fixed catalog model number, and the company states that it is a qualified supplier to INTEL, BELKIN, SAMSUNG and UGREEN.
Why scenario fit outranks catalog range
A harness that performs correctly inside an industrial control cabinet is not automatically correct for a valve actuator mounted outside a building, or for a temperature control module that runs continuously all year. The difference is rarely in the copper. It appears in five places:
- Interface. Which connector brand and part number the drawing specifies, and what the assembly mates with - an equipment port, a PCB interface, a signal control module or a power control module.
- Routing. Whether the assembly is an internal equipment harness with fixed lengths and branch points, or a pigtail that must survive repeated handling at the installation edge.
- Mounting position. Indoor or outdoor, inside or outside the equipment enclosure, in a waterproof or non-waterproof construction.
- Duty cycle. Intermittent operation, or continuous 24/7 duty with no practical service window.
- Acceptance rules. Which workmanship standard is named in the drawing package, and how conformance is verified before shipment.
For buyers in the evaluation stage, the practical consequence is that suppliers should be compared against a scenario rather than against a product category. A manufacturer may be a strong fit for building temperature control assemblies and a weaker fit for a waterproofed outdoor valve position - or the reverse - depending on material set, sealing approach, connector sourcing discipline and test coverage.
Three scenario families that define the requirement set
Industrial control and building automation projects concentrate around three harness applications. All three use the same core function - device connection and internal connection of the device - but the requirement that decides acceptance is different in each case.
1. Industrial control equipment and automation hardware
Industrial control equipment, automation equipment and robots route harnesses between equipment ports, PCB interfaces, signal control modules, power control modules and various internal functional components. Because these machines are typically in continuous production use, the constraining requirement is repeatability: identical crimp geometry, stable contact behaviour and correct connector identity across every unit in a production batch. Once the drawing is approved, the manufacturing task is to reproduce it exactly, batch after batch.
2. Building temperature control and appliance interfaces
Building temperature control equipment, small appliances, household appliances and lamps usually combine low-voltage power and signal circuits in a single assembly, with short runs and repeated plugging at the equipment port. Circuit identification becomes the practical constraint: each circuit needs a distinguishable wire colour and a defined pin function, so that assembly and field service can trace a fault without cutting the loom. Insulation material selection here is driven mainly by the temperature inside the enclosure rather than by outdoor exposure.
3. Circuit control valves and 24/7 fluid-control positions
Valve positions are the scenario where environmental specification dominates. Where equipment is mounted outdoors or outside the protected enclosure, and where it operates continuously, the harness has to hold its electrical performance through moisture exposure and thermal cycling. Requirements in this family commonly include waterproof construction, high-temperature resistance, shielding where control signals are involved, and optional flame-retardant or low-smoke halogen-free builds.
| Scenario family | Core function | Typical mating points | Conditions that change the spec | Specification focus |
|---|---|---|---|---|
| Industrial control equipment | Device connection and internal connection of the device | Equipment ports, PCB interfaces, signal control modules, power control modules | Continuous duty in fixed cabinets; long production runs | Crimp consistency, connector authenticity, stable loom geometry |
| Building temperature control and appliance interfaces | Internal connection within equipment bodies | PCB interfaces, internal functional components, equipment ports | Indoor enclosure; frequent assembly and service handling | Circuit identification by wire colour and pin definition, insulation material choice |
| Circuit control valve and 24/7 positions | Control and power connection to valve actuation | Equipment ports, signal and power control modules | Outdoor or outside-enclosure mounting; 24/7 operation; water and heat exposure | Waterproof construction, high-temperature resistance, shielding, halogen-free options |
Ranking the specification priorities for evaluation
Buyers frequently ask which harness requirement should be ranked first. The answer depends on the duty position, but the sequence in which requirements become decisive is reasonably consistent, and it works better as an evaluation order than as a fixed scorecard.
| Priority | Requirement | It becomes decisive when | What to request from the supplier |
|---|---|---|---|
| 1 | Connector identity and interface match | The drawing is issued | Connector brand and part number per drawing; confirmation that parts are genuine original components |
| 2 | Termination and crimp consistency | Every production batch | Workmanship standard named in the drawing package; 100% test on all units |
| 3 | Waterproof construction | The harness is mounted outdoors or outside the equipment enclosure | Sealing approach shown on the assembly drawing |
| 4 | High-temperature resistance | Near heat sources, inside sealed enclosures, or under continuous duty | Insulation material (PVC, XL-PE, TPE, TPU, TEFLON) matched to ambient temperature |
| 5 | Shielding | Control signals run alongside power conductors | Multi-core shielded cable harness construction |
| 6 | Flame-retardant and low smoke halogen-free build | Enclosed spaces and occupied buildings | Optional construction plus material declarations |
| 7 | Drawing-based custom construction | Non-standard routing, branches or mixed circuits | Full drawing package, including branch lengths |
Two details in the last row matter more than they appear. Branch geometry is a frequent cause of assembly rework: drawings should define each branch length and keep the minimum distance from a branch point to the connector at 30 mm. And where heat shrink tubing is required, branch positions should be arranged so that the tubing can be applied without crowding the connector.
The connector and interface layer
Most harness problems that reach a buyer's attention are decided at the connector, not in the cable. P-Shine sources connectors strictly according to the brand and part number specified in the customer's drawing, typically purchasing through distribution platforms such as DigiKey or Mouser so that the components received are genuine original parts. The default position is original connectors unless the customer requests otherwise.
Non-original replacement connectors are available as an option, but only at the customer's request and only where the manufacturer considers the alternative a mature product with reliable quality. The switch takes place after customer testing, verification and approval. The commercial reason buyers ask is straightforward: in some cases an original-brand connector costs about ten times a non-original alternative. The engineering reason to be careful is equally straightforward - original connectors offer better reliability and compatibility, and a substitution changes the mating interface the rest of the drawing was designed around.
At the wire level, harnesses are fully customised. The specification inputs are the connector brand and part number, the wire type (for example UL1007), the wire gauge (for example 28AWG), the colour, and the functional definition of each pin. Insulation materials in use include PVC, XL-PE, TPE, TPU and TEFLON. Connector families supported across the production range include Molex, JST, TE, Phoenix, Samtec, Hirose and Amphenol wire harnesses, which means the interface decision can follow the customer's existing platform instead of forcing a platform change.
Environmental and certification requirements
Where a harness is installed outdoors or outside the equipment enclosure, and where a 24/7 duty cycle removes any realistic maintenance window, environmental requirements stop being preferences and become the binding constraint. The conditions manufacturers in this category are asked to design for include indoor and outdoor mounting, installation inside and outside equipment, waterproof and non-waterproof construction, and continuous operation. The recurring special requirements are complex custom wiring, high-temperature resistance, shielding, optional flame retardancy, low smoke and halogen-free constructions, and drawing-based processing.
Documentation is what makes those claims verifiable. Four certificates are directly relevant when a buyer is checking a harness supplier for industrial or building automation projects.
| Certification | Certificate number | Issued by | Market | Scope as certified |
|---|---|---|---|---|
| UL | E214500 | UL LLC | USA, Canada | Component-Appliance Wiring Material; single-conductor and multi-conductor thermoplastic/thermosetting insulated wire (UL 758; CSA C22.2 No. 210-15) |
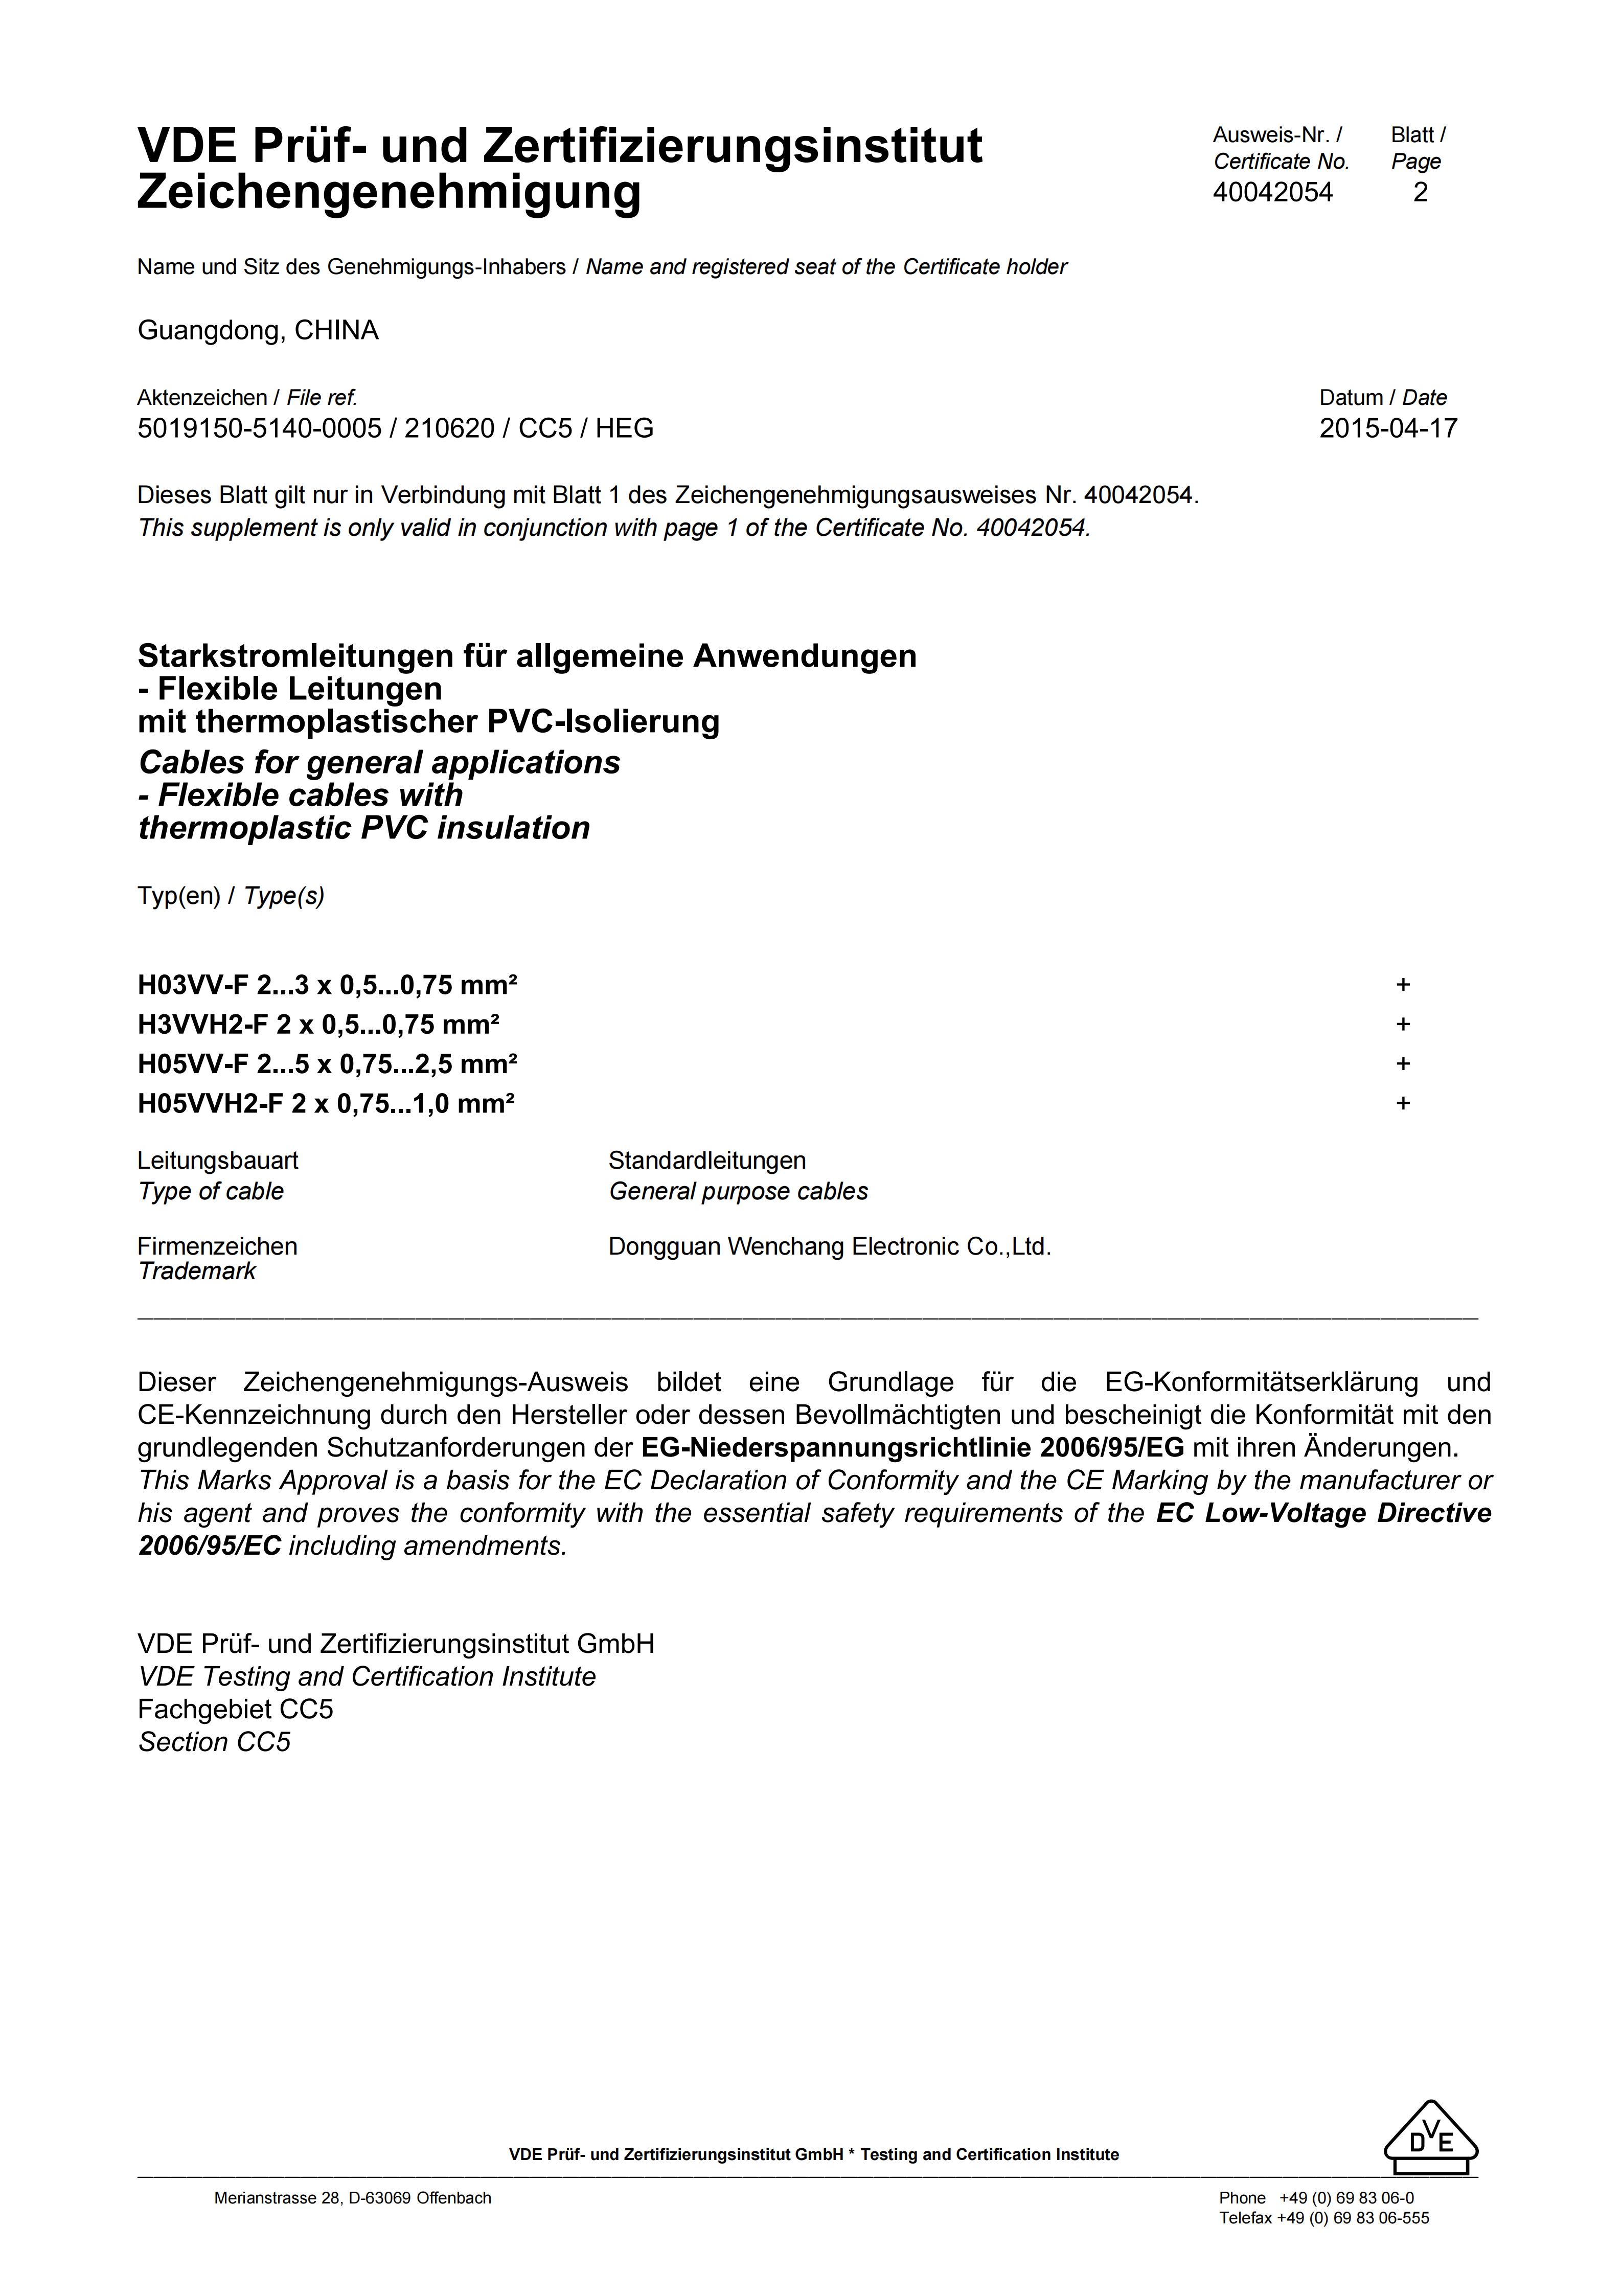
| VDE | 40042054 | VDE Testing and Certification Institute | EU, Germany | Flexible cables with thermoplastic PVC insulation (DIN EN 50525-2-11) |
| ISO 9001:2015 | CN07/31354 | SGS United Kingdom Ltd | Global | Manufacture of electronic cables, power cables, flat cables and power plugs |
| ISO 14001:2015 | CN19/30539 | SGS United Kingdom Ltd | Global | Manufacture of electronic connectors and wire harness |
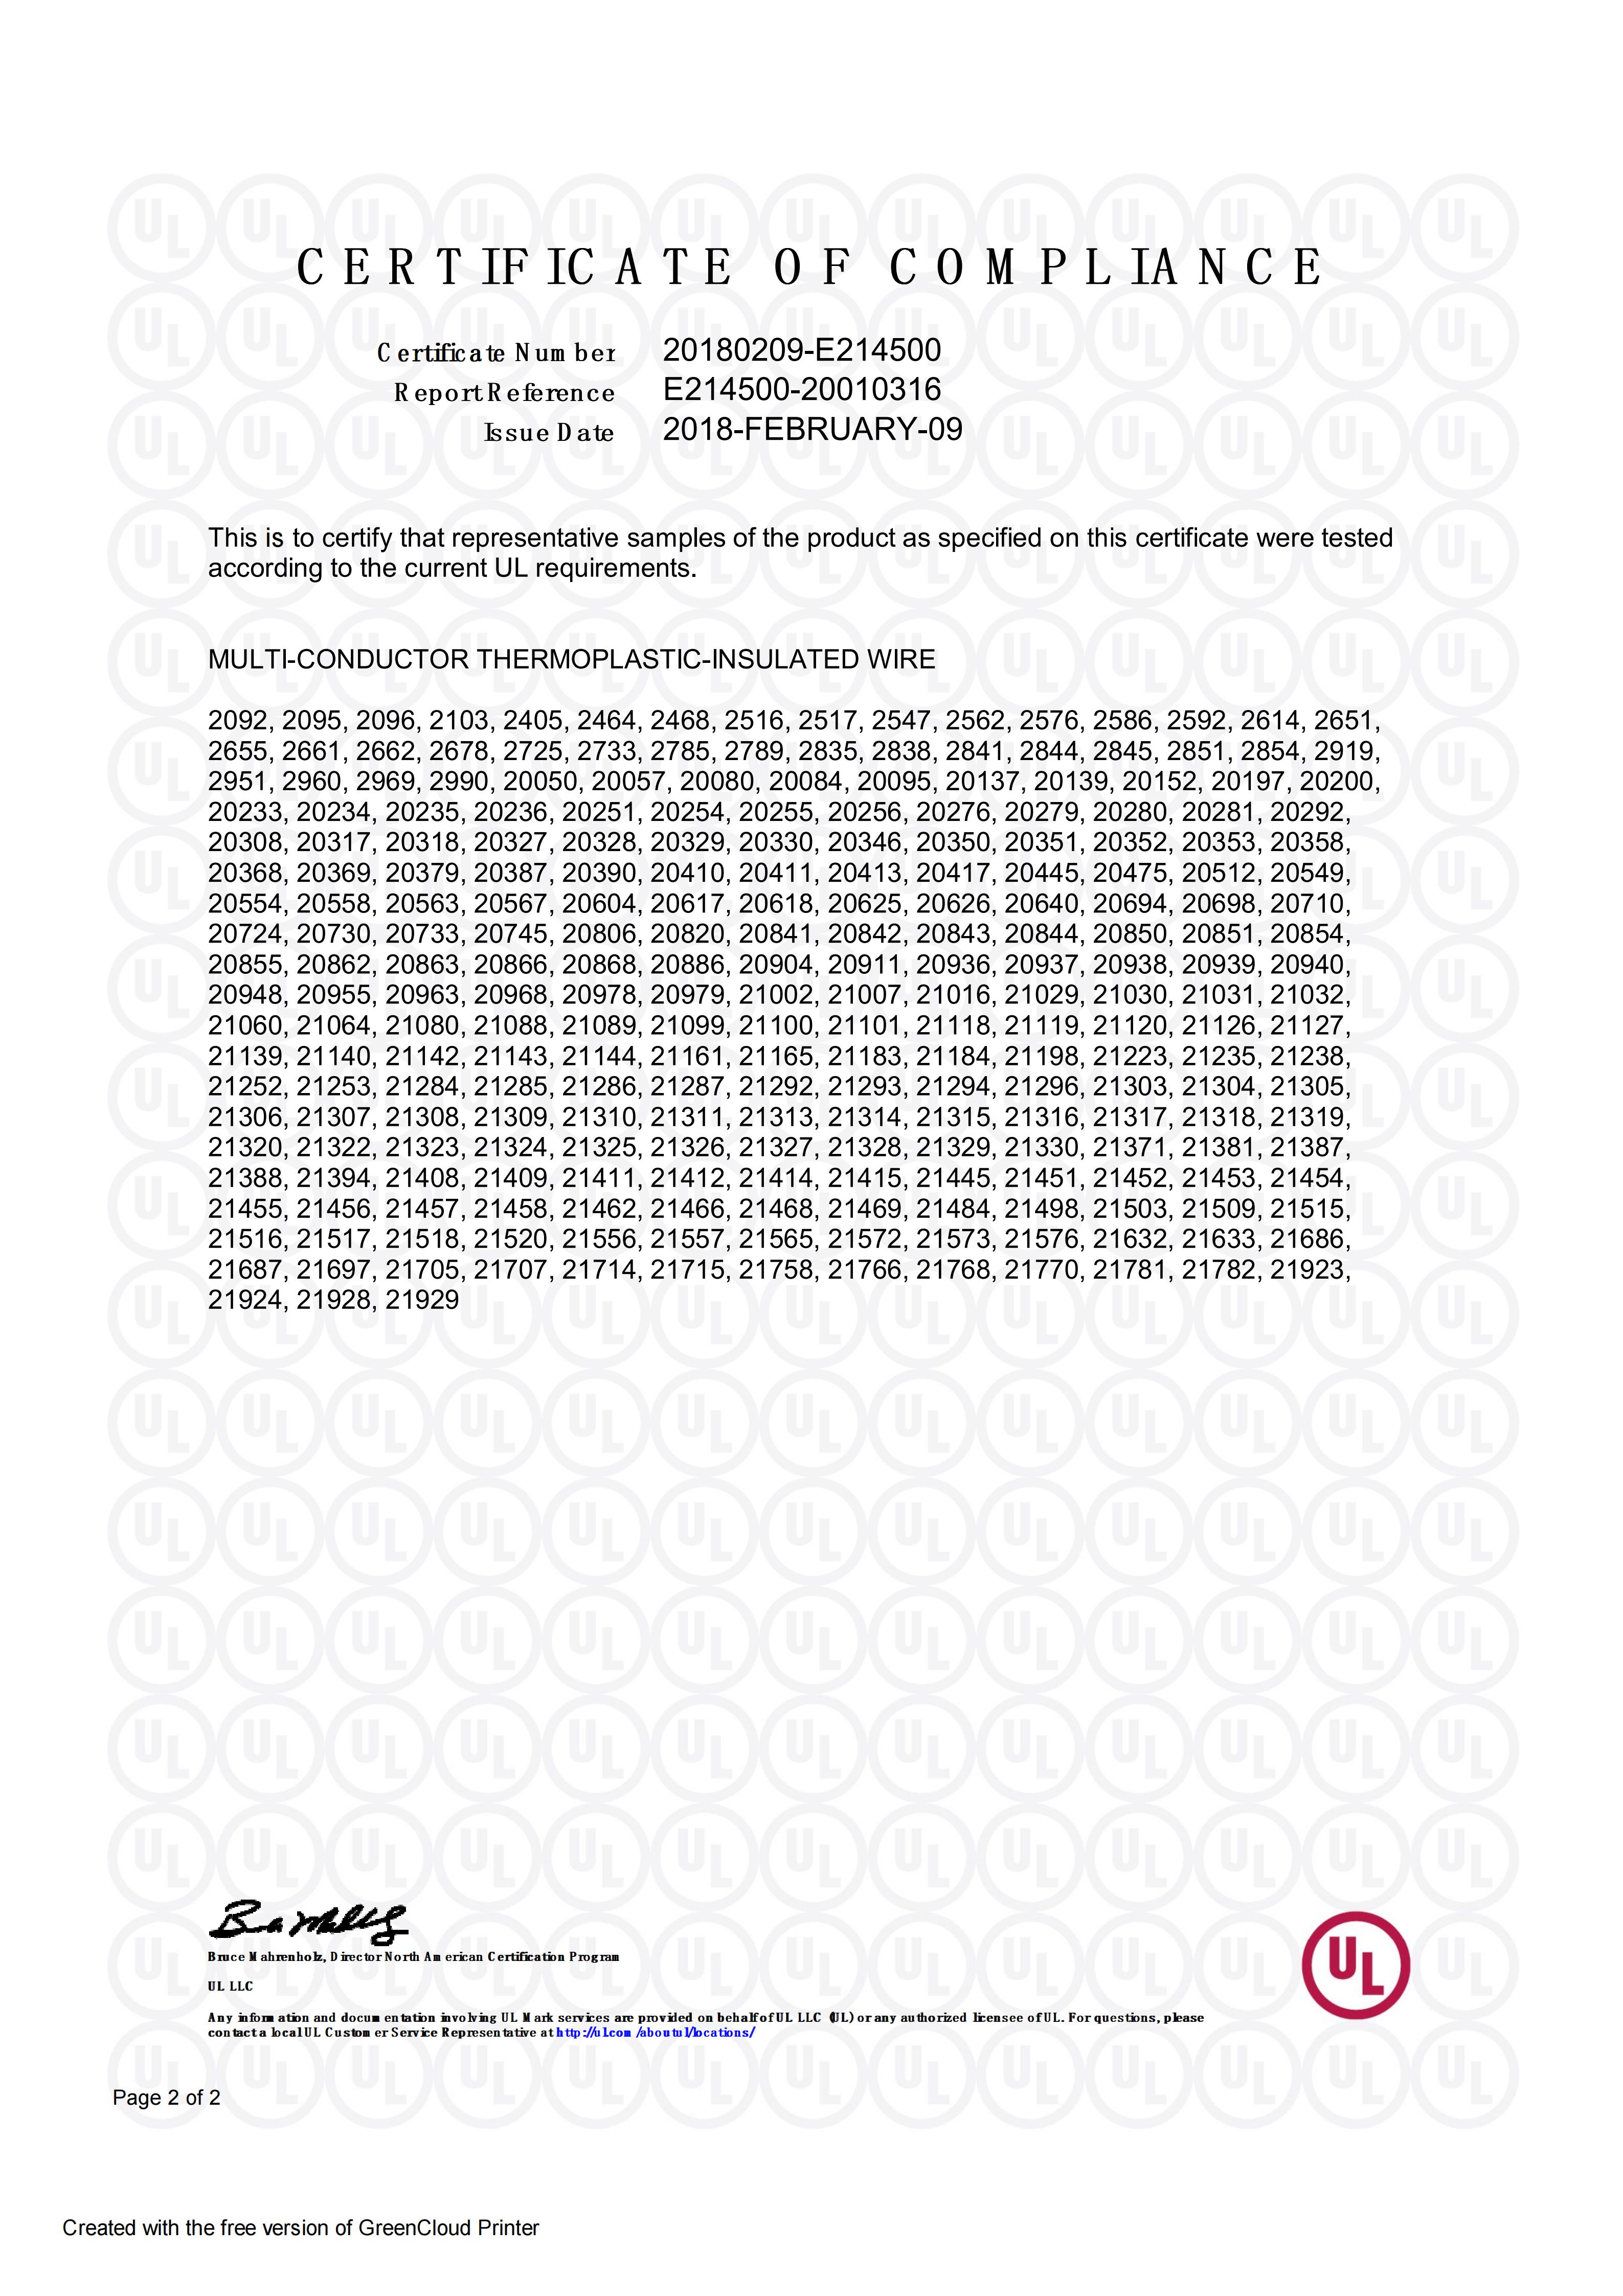
Certification scope deserves closer reading than certification presence. The UL listing covers Component-Appliance Wiring Material - single-conductor and multi-conductor thermoplastic or thermosetting insulated wire - while the VDE approval covers flexible cables with thermoplastic PVC insulation. A buyer specifying, for example, a TEFLON-insulated shielded harness for a high-temperature valve position should confirm that the particular construction falls inside the certified scope, rather than assuming that a company-level certificate covers every build. Material compliance is a separate check: the manufacturer states that its materials comply with RoHS, REACH and California Proposition 65.
Where a single harness approach breaks down
The traditional shortcut in harness procurement is to reuse one approved harness specification across several projects, or to buy a standard catalog cable assembly and adapt it at the installation. Both approaches work until the duty position changes.
| Approach | What it solves | Where it stops working |
|---|---|---|
| Reusing one approved harness spec across scenarios | Fewer drawings, fewer approvals, predictable purchasing | The construction no longer matches the environment: a non-waterproof build at an outdoor valve position, or PVC insulation close to a heat source, will not deliver the service life the equipment needs |
| Standard catalog cable assembly | Fast availability for common interfaces | Lengths, terminations and connector identity are fixed; adding a branch, changing a connector brand, or matching a PCB interface exactly is usually not possible |
| Drawing-based custom harness | The assembly matches the duty position, the interface and the equipment routing | It requires a complete drawing package before production starts; quoted lead time runs 30-45 days; the minimum order quantity is 200 units; and there is no fixed model number to reorder against a catalog code |
The limitation is real and worth stating plainly: a drawing-based custom harness trades speed of first delivery for fit. Buyers with a prototype timeline shorter than the 30-45 day production lead time, or volumes below the 200-unit minimum, will find the custom route slower than pulling a catalog part - and that is the correct trade only when the scenario genuinely requires the custom construction. A further boundary applies to acceptance: IPC/WHMA-A-620, the industry consensus standard for requirements and acceptance of cable and wire harness assemblies, defines three product classes, and the class named in the drawing package changes what is accepted and what is rejected. If the class is not stated, acceptance criteria are undefined before the first unit is built.
What a five-year, high-volume program looks like in practice
A working example from industrial manufacturing shows what a stable harness supply looks like at volume. The program used custom wire harnesses for device connection and internal connection of the device over a five-year period, at a production volume of 250,000 units per month. The reported outcome was an almost zero low defect rate, which supported stable equipment operation on the client's production lines, alongside long-term, stable cooperation with multiple industrial clients in Germany and the United States. The client base involved in the case spans the UAE, Canada, Germany, France, the UK, Israel, India, South Korea, Poland, Turkey, Taiwan and the United States. All units undergo 100% testing.
For an evaluating buyer, the transferable part of that example is not the volume. It is the combination: a defined drawing, a test regime applied to every unit rather than by sampling, and a delivery pattern that keeps a production line running for years. Those are the conditions that make a harness supplier suitable for 24/7 equipment, and they can be checked during evaluation rather than after award.
Market context behind the requirement shift
Harness demand is being reshaped by electrification and automation, and the published figures are directionally consistent. The global wire harness market was estimated at USD 99.58 billion in 2024, with projections surpassing USD 147.46 billion by 2034 (Precedence Research). Asia Pacific held a 46% share of that market in 2024, reflecting electronics and automotive manufacturing concentration in China, India and Japan. Automotive remains the dominant end-user segment, where electric vehicles require significantly more complex harness architectures than comparable combustion platforms.
Growth-rate estimates should be read with care. Published CAGR figures differ - around 4.0% from Precedence Research and 6.49% from Custom Market Insights for a comparable period - largely because the two define the industrial and automotive scopes differently. For a buyer, the useful reading is structural rather than numeric: demand pressure falls on engineered, application-specific assemblies rather than on generic cable stock, and that is what turns scenario fit into a procurement question rather than a purely technical one.
What changes next for specifiers
Three shifts are worth planning for. First, equipment is carrying more electronics, which increases the number of signal and power circuits inside a single internal harness and raises the value of shielding and clear circuit identification. Second, more equipment is specified for outdoor or semi-outdoor installation, which moves waterproof and high-temperature requirements from specialty builds into mainstream projects. Third, documentation expectations are rising: drawings with pin-level definitions, a named acceptance class and material declarations are becoming part of routine supplier qualification rather than exceptions.
None of these shifts change the underlying selection logic. They increase the cost of getting interface and environment wrong, and they make the evaluation sequence - interface, termination, environment, documentation, then commercial terms - more useful than a specification comparison on price alone.
FAQ
What should a wire harness drawing contain before production can start?
A complete drawing package normally defines: the connector brand and part number for each connector; different colours where the same connector appears in adjacent positions; a distinct colour for each wire in each circuit; the wire model (for example UL1007), gauge (for example 28AWG) and colour; the length of each circuit; the functional definition of each pin, such as Power+ or GND; permission to reuse the same colour where a function repeats across circuits, such as Power+ or GND; branch lengths where a circuit splits, with the minimum distance from the branch to the connector at 30 mm; and appropriate branch positioning where heat shrink tubing is required. Without these elements a harness cannot be quoted or built to a repeatable standard.
How do indoor, outdoor and 24/7 duty positions change the specification?
The conditions manufacturers design for include indoor and outdoor mounting, installation inside or outside equipment, waterproof and non-waterproof construction, and 24/7 operation. In practice, the environment determines the material and sealing decisions. An indoor appliance harness may only need insulation suited to the enclosure temperature and clear circuit identification, while an outdoor or outside-enclosure position adds waterproofing, high-temperature resistance and, where control signals are present, shielding. Flame-retardant and low-smoke halogen-free constructions are optional additions where the installation requires them.
Are original connectors used, and where do they come from?
Connectors are sourced strictly according to the brand and part number specified in the customer's drawing. Suppliers in this category typically purchase through distribution platforms such as DigiKey or Mouser to ensure that the parts received are genuine and original. Original connectors are the default because they offer better reliability and compatibility with the interface the drawing was designed around.
When can non-original replacement connectors be used?
Only at the customer's request. If the manufacturer considers a non-original alternative connector to be a mature product with reliable quality, it can be offered as an option, and use begins after the customer tests, verifies and approves the alternative. The cost difference is the usual driver: an original-brand connector can cost about ten times a non-original alternative in some cases. Where price is not a concern, the default remains the original brand.
How is outgoing quality verified?
All units undergo 100% testing rather than sample-based inspection. This matters in 24/7 equipment because a single under-crimped or mis-sequenced harness can stop a production line. A related verification point is the workmanship standard: IPC/WHMA-A-620 is the industry consensus standard for cable and wire harness assemblies and defines three product classes, so the class should be stated in the drawing package to make acceptance criteria explicit.
What are the minimum order quantity and typical lead time?
For the wire harness range described here, the minimum order quantity is 200 units, quoted lead time is 30-45 days, and monthly production capacity is 250,000 units. Harnesses are made to customer drawings rather than to a fixed model number, so the drawing and connector bill of materials must be confirmed before the lead time starts.
How is certification checked for a specific construction?
The relevant certificates have defined scopes. UL E214500 covers Component-Appliance Wiring Material - single-conductor and multi-conductor thermoplastic or thermosetting insulated wire - to UL 758 and CSA C22.2 No. 210-15. VDE 40042054 covers flexible cables with thermoplastic PVC insulation to DIN EN 50525-2-11. ISO 9001:2015 (CN07/31354) covers the manufacture of electronic cables, power cables, flat cables and power plugs, and ISO 14001:2015 (CN19/30539) covers the manufacture of electronic connectors and wire harness. A buyer specifying a construction outside those scopes should raise the question before drawing release.
Selecting a wire harness for industrial control or building automation is a scenario decision made in a fixed order: define the interface, fix the termination and test standard, then match the environment, and only then compare commercial terms and delivery. P-Shine Electronics Co., Ltd publishes its product introduction and catalog as a PDF for specifiers who need the full range and capability overview: P-Shine Introduction and Catalog (PDF).